 English
 Español
 Deutsch
-

Long-Stroke Multi-Stage Progressive Die Automatic Strip Feed Progressive Die Long Travel Follow on Stamping Tool for Sheet Metal Hardware Press Moulding
Long-Stroke Multi-Stage Progressive DieOur custom ...
-
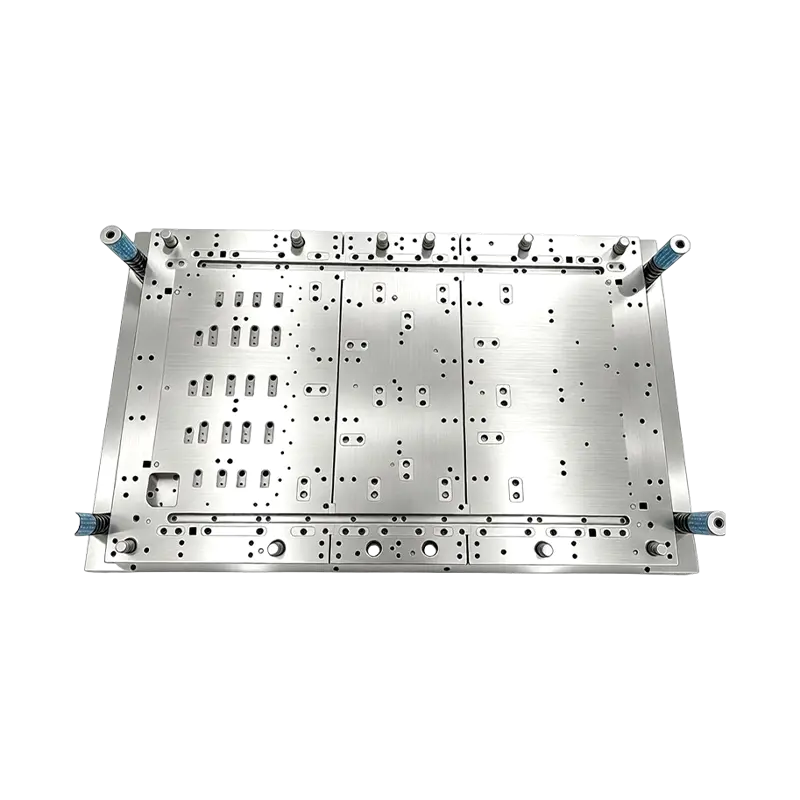
Multi-Station Progressive Stamping Die with Carbide Inserts Custom Multi Station Progressive Stamping Die Carbide Insert Metal Stamping Mold Tool for Equipment Appliances Device Hardware
High Speed Metal Stamping Tool for Precise Equipme...
-

Progressive Stamping Die for Connector & Terminal Parts High Speed Progressive Stamping Die Precision Metal Hardware Stamping Tool mold for Connector Terminal Parts Automotive Components
Progressive Stamping Die for Connector & Termi...
-
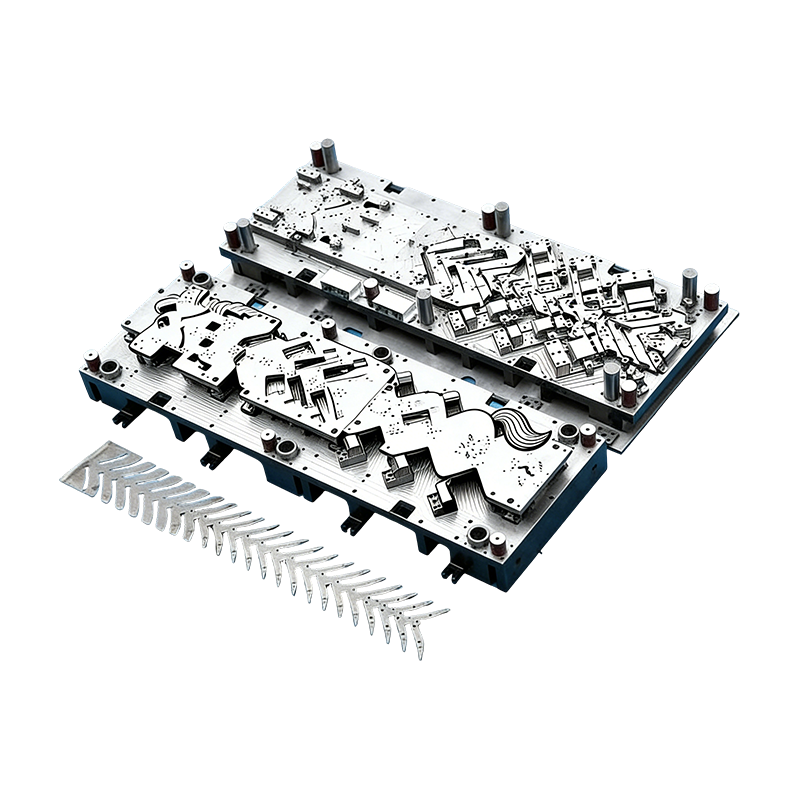
Progressive molds for automotive parts
This Continuous mold for automotive motor housing ...
-
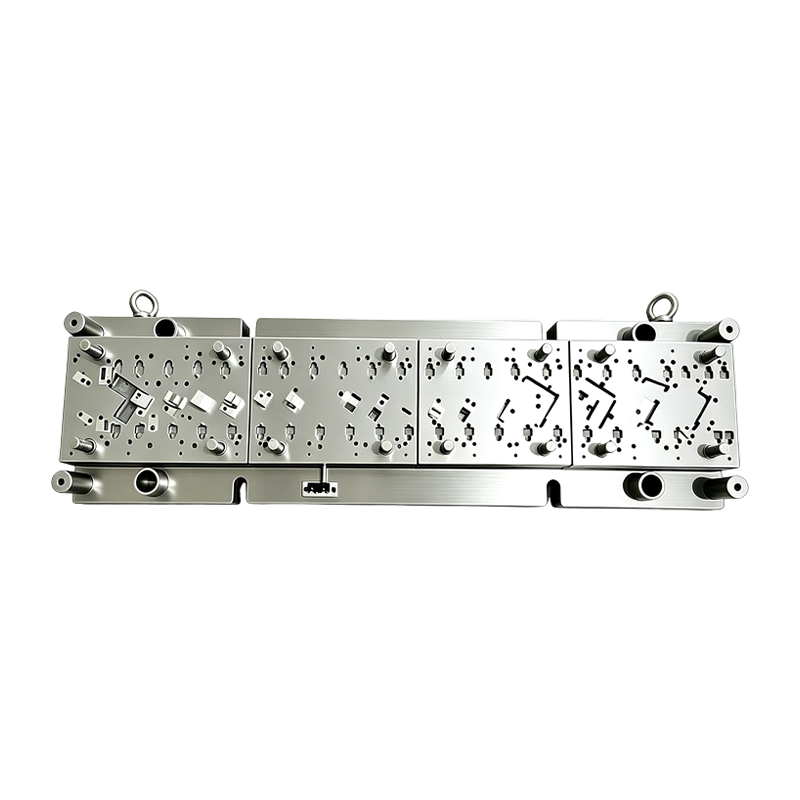
High Speed Progressive Stamping Die Sheet Metal Follow on Press Tool
Multi-operation Metal Stamping Tool for Continuous...
-
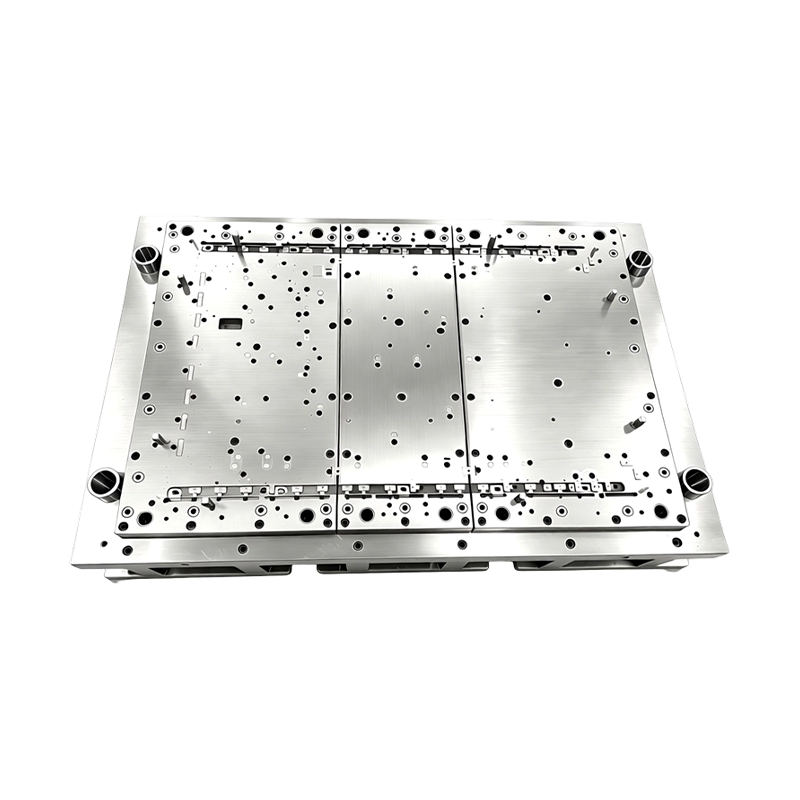
High Precision Stamping Die Multi Station Hardware Progressive Mold Tooling
Precision Metal Stamping Tool for Automotive &...
- E-mail us: [email protected]
- Call us: +86-139 1308 8972

Zhou Mengjie – Technical Sales Specialist
Home / Author / Zhou Mengjie – Technical Sales Specialist / Long-Stroke Multi-Stage Progressive Dies for Complex Sheet Metal Forming
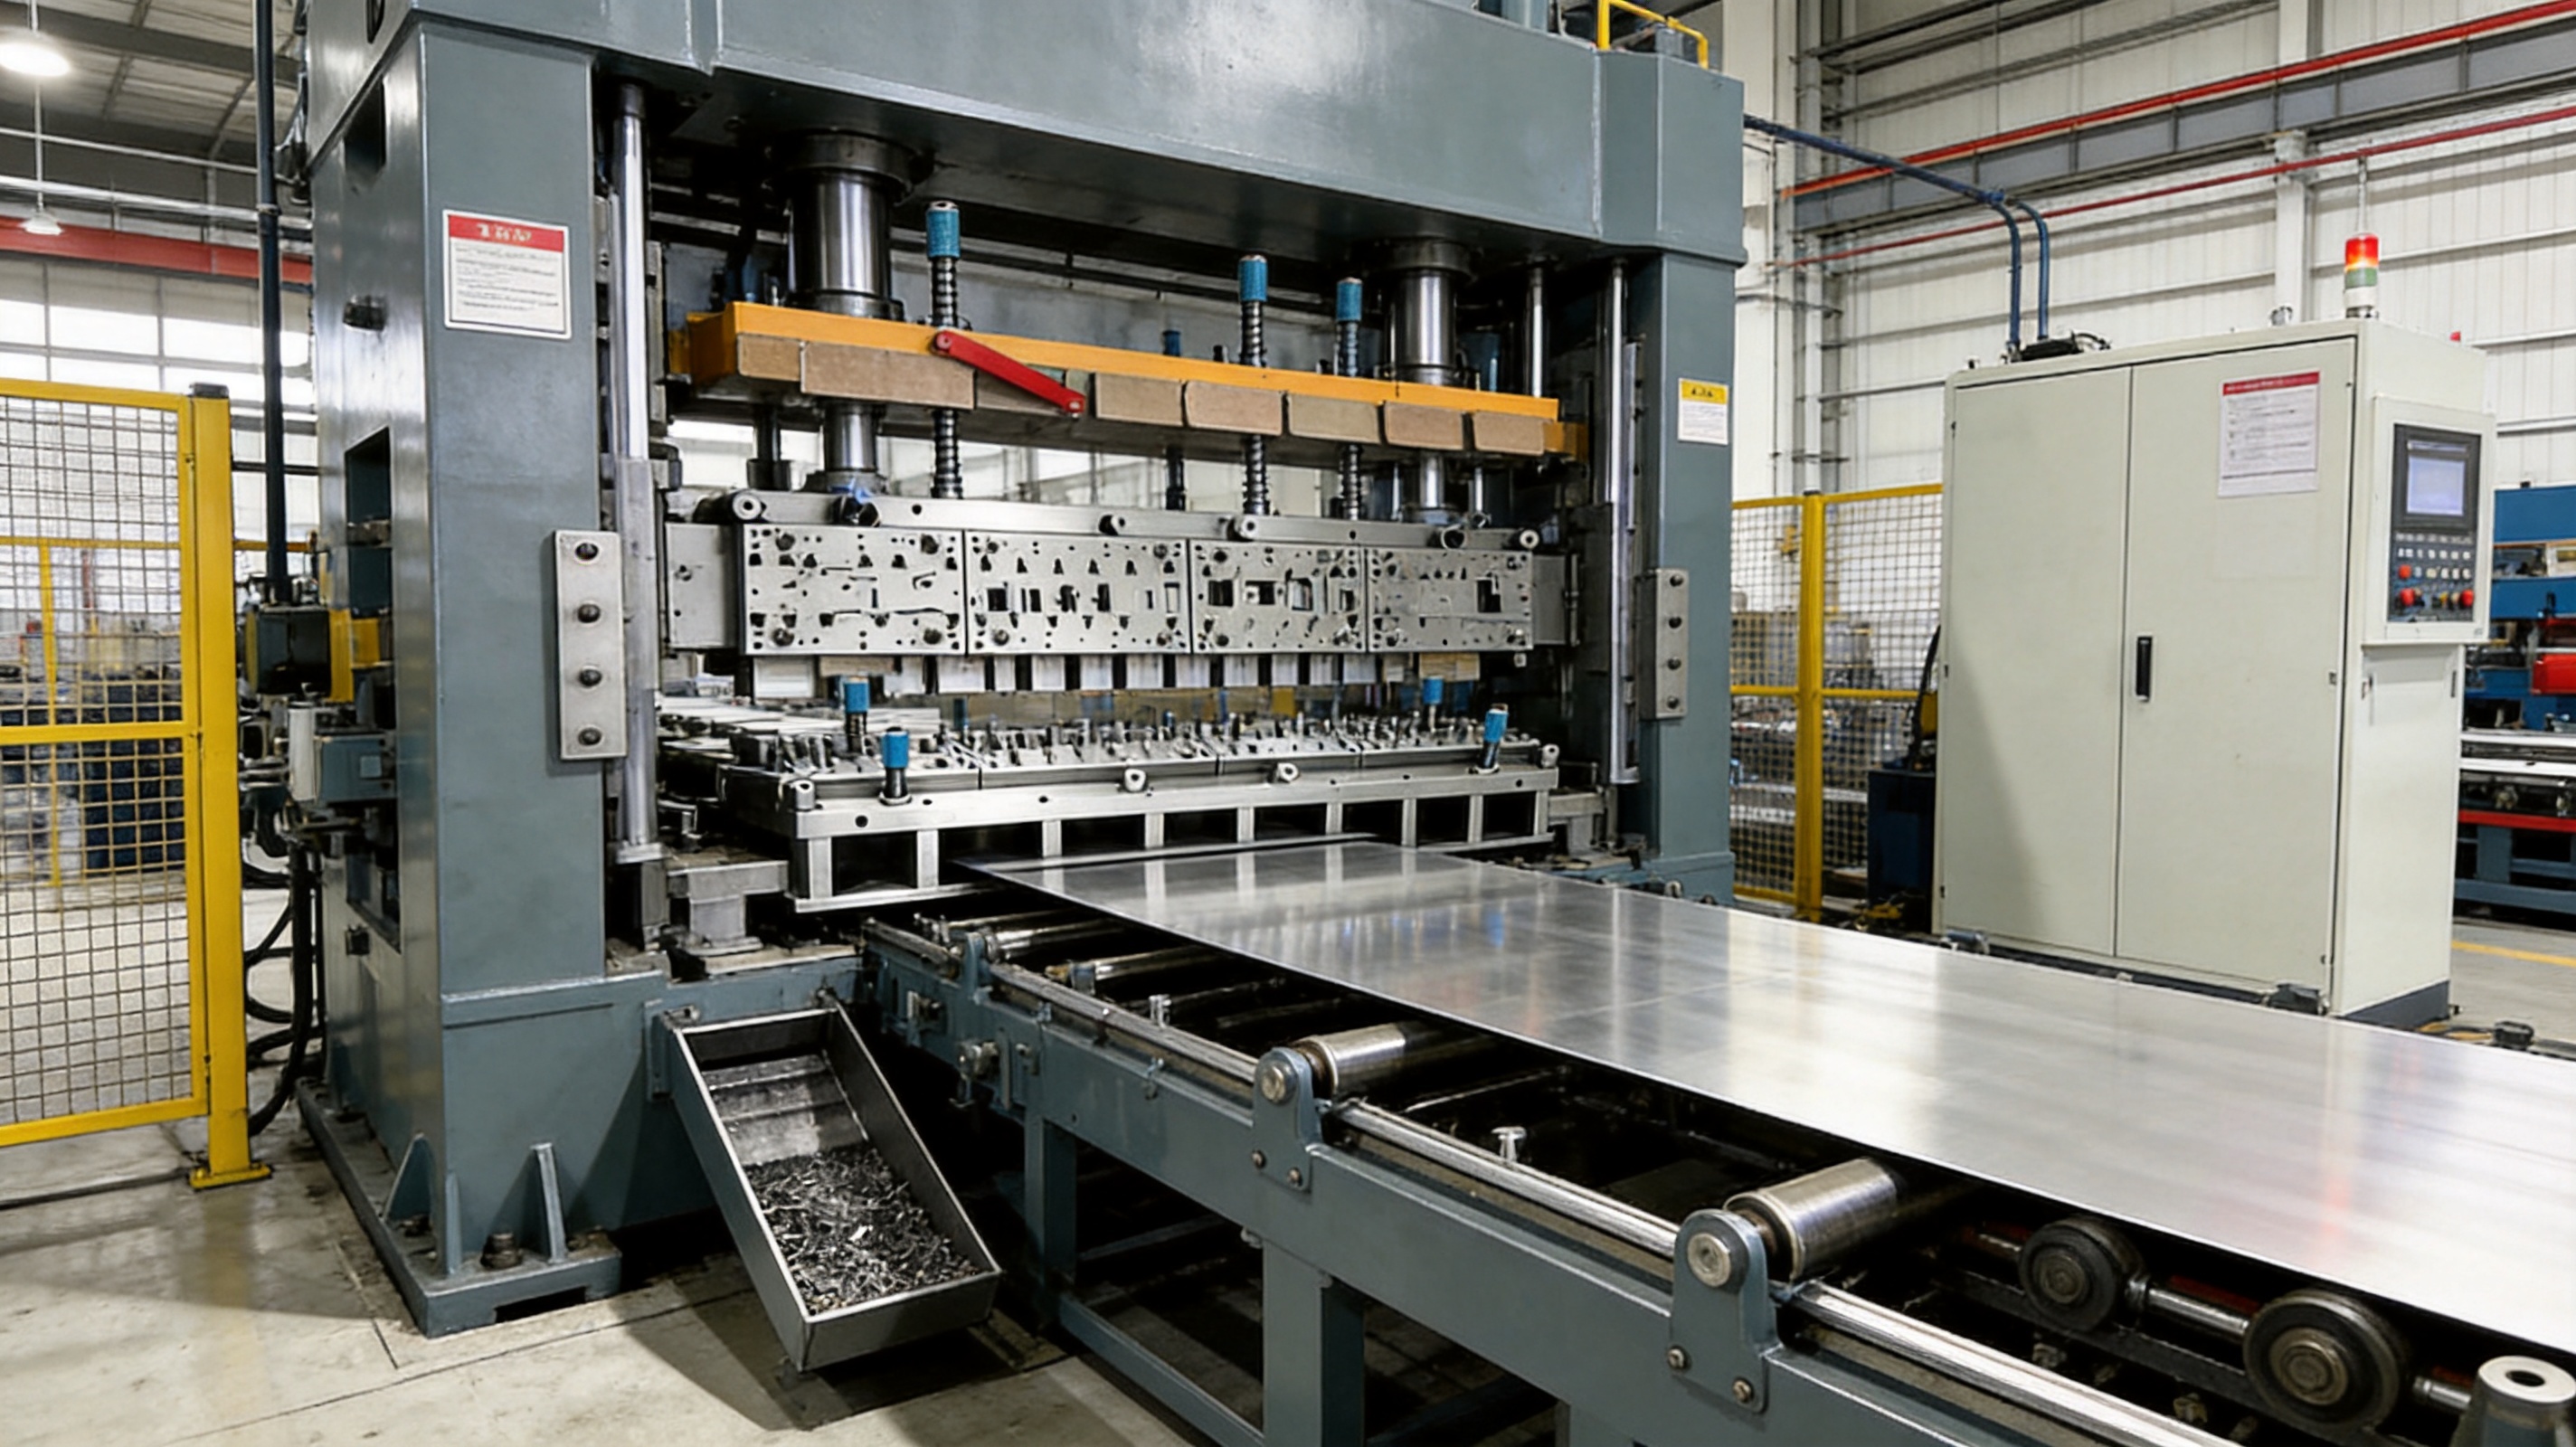
Long-Stroke Multi-Stage Progressive Dies for Complex Sheet Metal Forming
2026-10-16
Modern automotive, electric vehicle, electrical, and industrial products increasingly depend on sheet metal components with several bends, pierced holes, embossed surfaces, offsets, tabs, and three-dimensional profiles. Producing these parts efficiently requires more than a conventional blanking die or a short progressive tool. It requires a carefully engineered forming system that can control the strip from the first feed movement to the final part discharge.
The long-stroke multi-stage progressive die is designed for this purpose. It combines automatic coil feeding, multi-point strip guidance, sequential forming, precision piercing, controlled bending, springback compensation, final restriking, blanking, and automated part ejection in one integrated production solution. The result is a stable and repeatable process for manufacturing complex sheet metal hardware at high production volumes.
Unlike a short-stroke terminal die that generally focuses on one or a few operations, this long-travel progressive stamping tool uses an extended die body with multiple stations arranged along the strip direction. Each station performs a specific operation. As the strip advances by a fixed pitch, the workpiece gradually changes from a flat coil strip into a finished three-dimensional component.
This article explains the operating principle, structural advantages, manufacturing process, application range, quality controls, and customization capabilities of this type of progressive die. It also examines why an experienced integrated die and automation manufacturer can provide advantages over suppliers that only produce individual tooling components.
Content
- 1 What Is a Long-Stroke Multi-Stage Progressive Die?
- 2 Why Complex Sheet Metal Parts Need a Long Working Area
- 3 Operating Principle of the Automatic Strip-Feed System
- 4 Multi-Stage Forming for Complex Three-Dimensional Components
- 5 Springback Compensation and Dimensional Stability
- 6 Long-Strip Stability and Anti-Warping Design
- 7 Heavy-Duty Die Base and Multi-Point Guidance
- 8 Modular Forming Inserts and Maintenance Efficiency
- 9 Integrated Scrap Management and Part Ejection
- 10 Product Advantages Compared with Conventional Stamping Solutions
- 11 Manufacturing Process for the Progressive Die
- 12 Tryout, Debugging, and Validation
- 13 Manufacturing Capabilities and Integrated Technical Strengths
- 14 Application Areas
- 15 Key Technical Parameters to Define Before Ordering
- 16 Typical Process Structure
- 17 How to Select the Right Progressive Die Supplier
- 18 Maintenance and Production Support
- 19 Economic Value of the Long-Stroke Progressive Approach
- 20 Questions and Answers
- 20.1 What type of parts are suitable for this die?
- 20.2 How many stations can the die contain?
- 20.3 Can the die process high-strength steel?
- 20.4 Why are multiple pilot pins important?
- 20.5 How is springback controlled?
- 20.6 Can individual die stations be modified?
- 20.7 How are stamping slugs and scrap removed?
- 20.8 How is the finished part removed?
- 20.9 Can the die be integrated with stamping automation equipment?
- 20.10 What press capacity is required?
- 20.11 How does the tool improve production efficiency?
- 20.12 What information should be submitted for a quotation?
- 21 Conclusion
- 22 References
- 23 Product: Long-Stroke Multi-Stage Progressive Die Automatic Strip Feed Progressive Die Long Travel Follow on Stamping Tool for Sheet Metal Hardware Press Moulding
What Is a Long-Stroke Multi-Stage Progressive Die?
A long-stroke multi-stage progressive die is a precision stamping tool designed to complete numerous forming operations during a single continuous strip-feeding process. The die normally contains an extended sequence of stations, with the number of stations selected according to the part geometry, material, thickness, tolerance requirements, and production volume.
Typical stations may include coil entry, strip straightening, pilot positioning, piercing, notching, lancing, pre-bending, bending, forming, embossing, coining, restriking, trimming, separation, and final blanking. Some components require only eight or ten operations, while highly complex automotive or electrical parts may require more than thirty individual forming stages.
The strip is fed into the die at a controlled pitch. At every press stroke, the strip moves forward by one station interval. Several parts are therefore in the die simultaneously, with each part at a different stage of completion. One section of the strip may be receiving pilot holes, another may be undergoing a first bend, and another may be receiving final coining or separation.
This progressive arrangement allows many operations to be completed in a single automated cycle. It reduces manual handling and avoids transferring semi-finished parts between multiple independent dies. When the process is correctly designed, the final component leaves the tool ready for collection, inspection, assembly, or a limited secondary operation.
Why Complex Sheet Metal Parts Need a Long Working Area
Complex sheet metal parts cannot always be formed reliably in one or two heavy hits. A deep bend, a narrow flange, an offset, or a high-strength material may require gradual deformation. Attempting to produce all features simultaneously can lead to excessive forming force, distortion, cracking, unstable springback, and poor dimensional consistency.
An extended die layout provides the space needed to distribute forming operations across multiple stations. Instead of forcing the material to reach its final shape immediately, the tool introduces the geometry progressively. A typical sequence may begin with piercing and material separation, followed by a shallow pre-bend, a second bend, a controlled offset, an embossing step, a restrike operation, and final calibration.
This approach offers several technical benefits:
• Each forming operation can be optimized independently.
• Forming loads can be distributed across the press stroke.
• Material flow can be controlled more accurately.
• Springback can be corrected in later stations.
• Narrow flanges and small features can be formed without excessive interference.
• The strip remains supported during most of the production sequence.
• Finished parts can be produced without multiple manual transfers.
The long die body is particularly valuable when the component has several bends in different directions. It also supports the production of parts with complex relationships between holes, edges, ribs, and mounting surfaces. Because each feature is referenced to the strip and pilot system, positional accuracy can remain stable throughout the complete progression.
Operating Principle of the Automatic Strip-Feed System
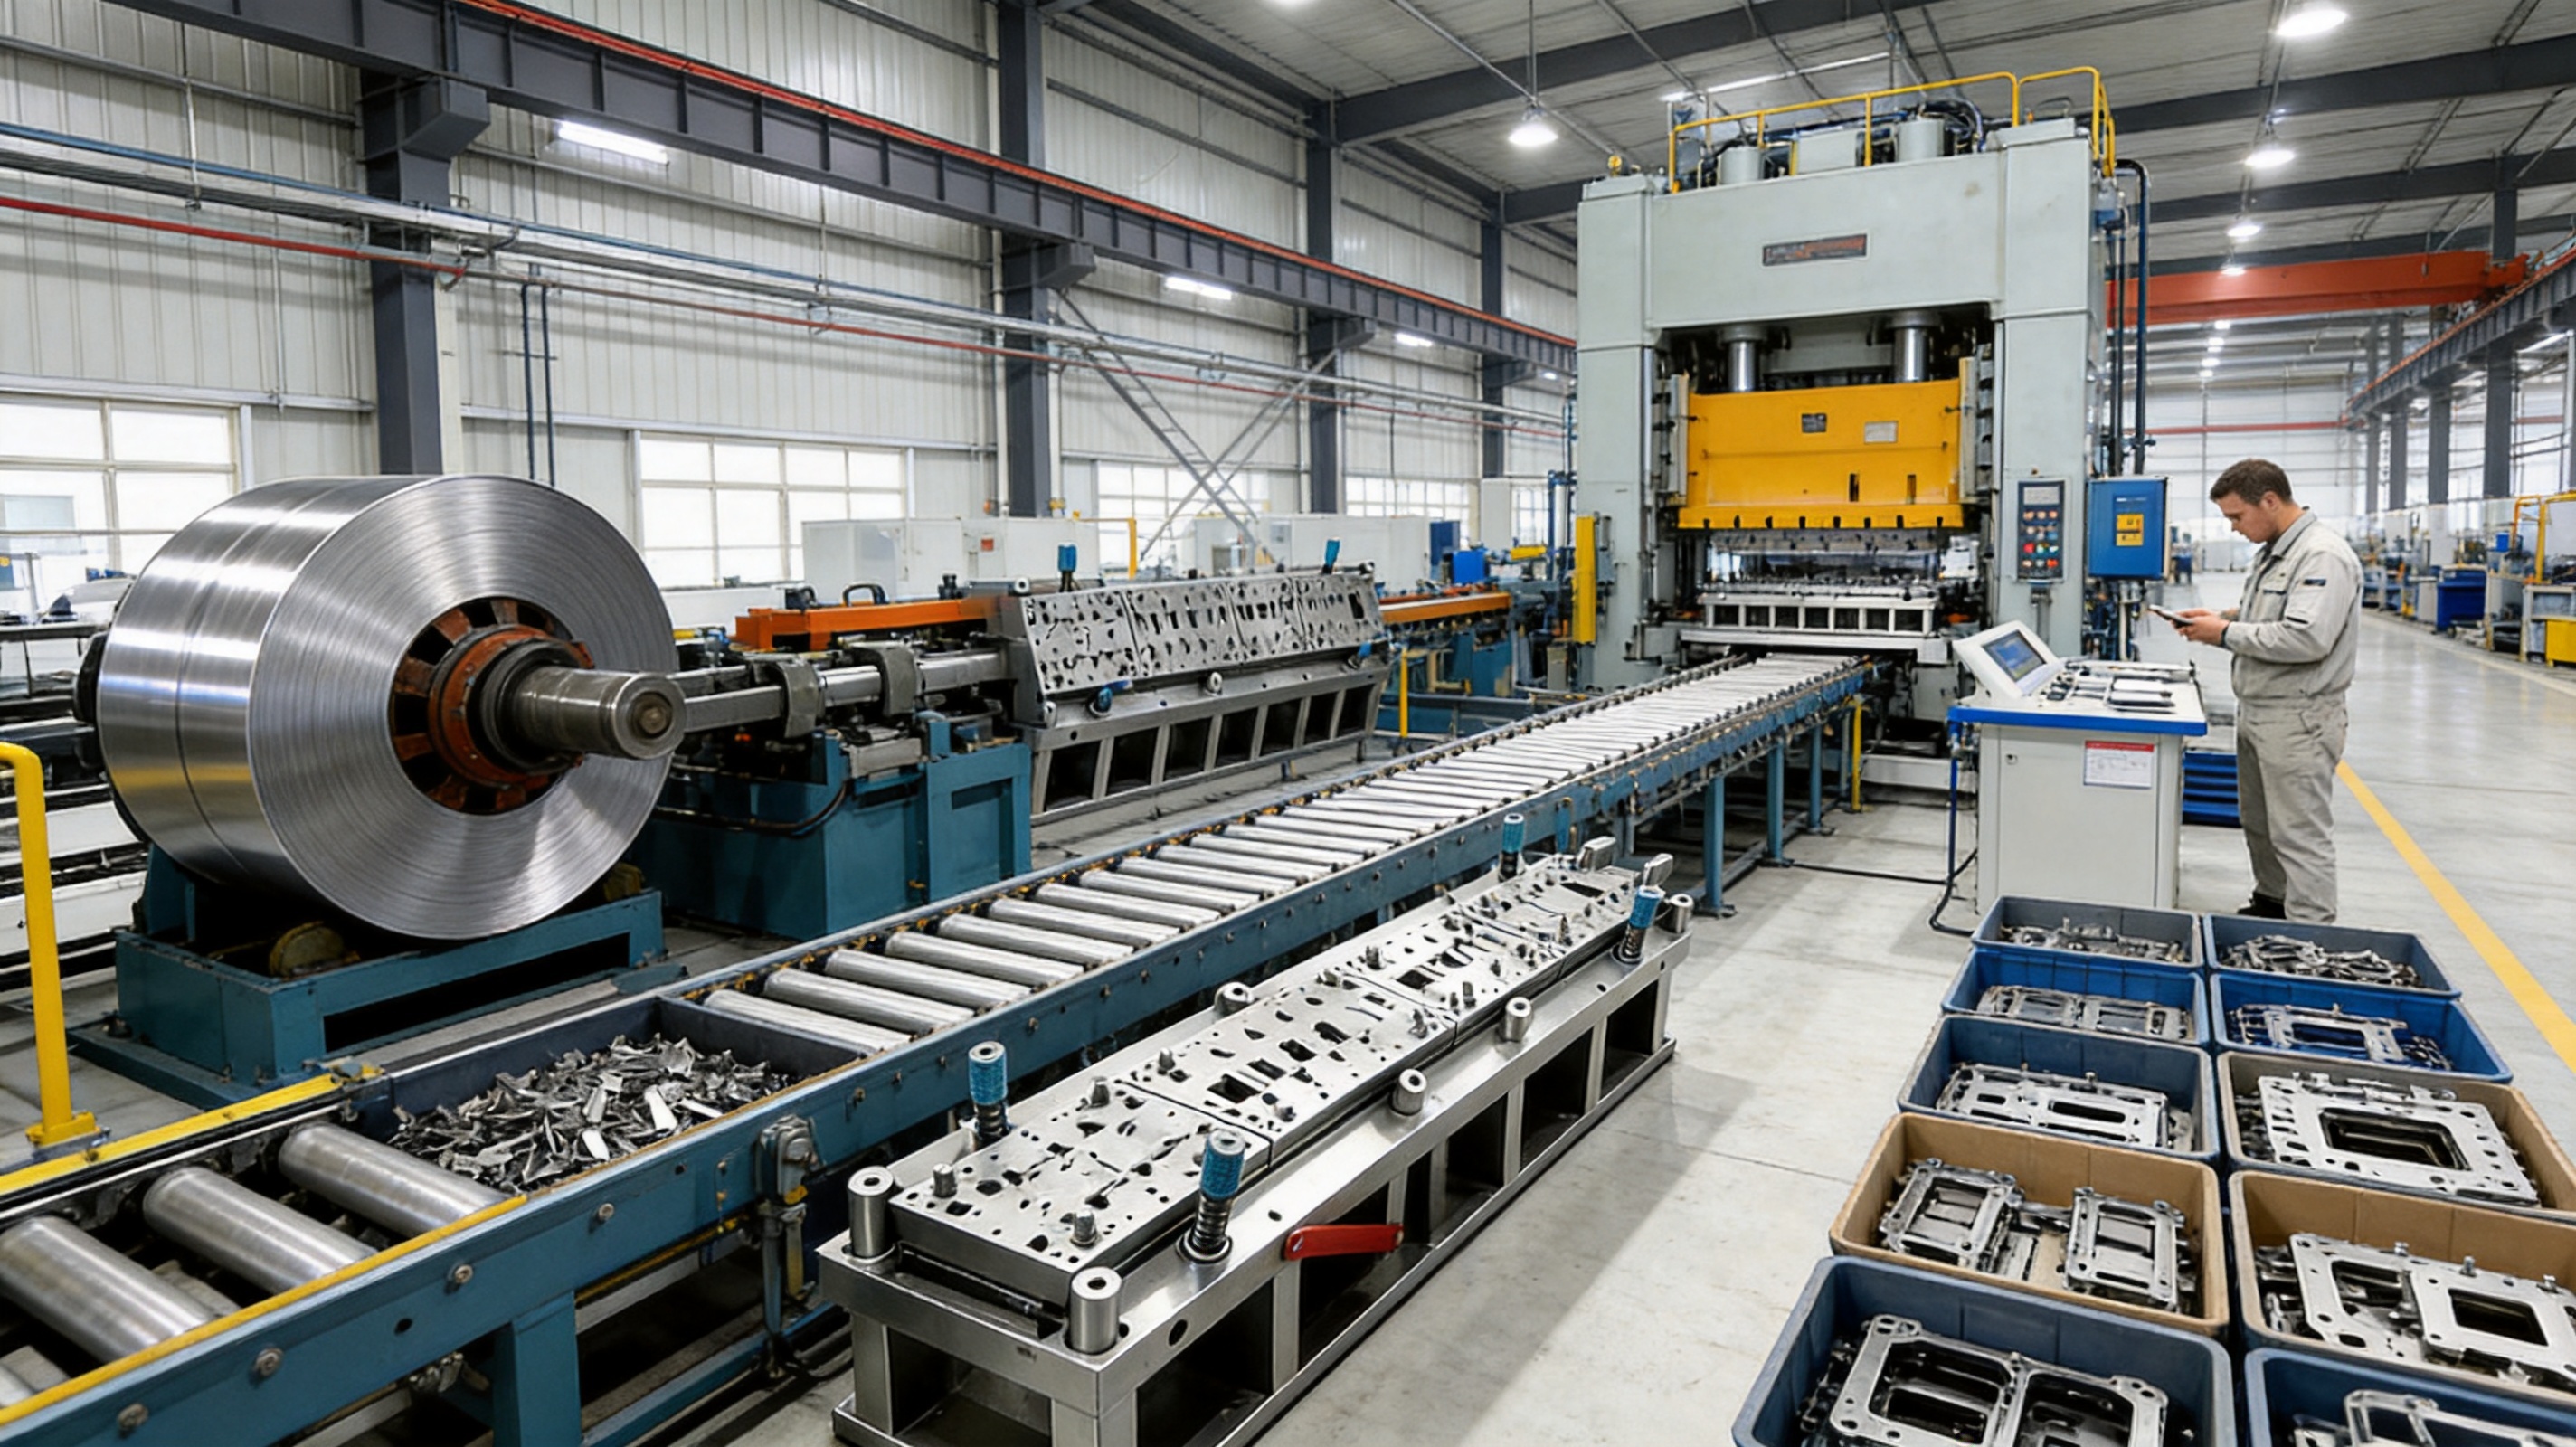
The production process begins with a coil of sheet metal. The coil is commonly processed through a decoiler, straightener, and automatic feeder before entering the progressive die. The feeder advances the strip at a defined pitch, while the die’s pilot pins and guide components establish the exact position required for each operation.
During the first press cycle, the strip enters the die and may receive initial holes, notches, or carrier features. On the next cycle, this partially processed section advances to the following station. At the same time, a new section enters the first station. This overlapping sequence continues until the first completed part reaches the final separation or blanking position.
The feed pitch is a critical parameter. If the pitch is incorrect, each station will act on the wrong location. This can cause hole misalignment, uneven flange width, incorrect embossing position, and interference between the strip and forming components. For this reason, the feed system is designed together with the die rather than treated as an unrelated accessory.
Pilot pins provide fine registration after the strip has been advanced. Strip lifters raise the material during return movement and help prevent unwanted contact with the die surface. Pressure pads hold the strip down during piercing and forming. Guide rails and supporting surfaces prevent lateral movement, twisting, or local deformation.
In long progressive tools, these functions must be repeated or distributed along the die body. A short die may be adequately controlled by guide rails at the entrance and exit. A long-stroke die needs additional support points because the strip may experience progressive deformation over a considerable distance. Multiple pilot locations and carefully designed carriers help maintain registration even after numerous operations have been completed.
Long-Stroke Multi-Stage Progressive Die Automatic Strip Feed Progressive Die Long Travel Follow on Stamping Tool for Sheet Metal Hardware Press Moulding
Multi-Stage Forming for Complex Three-Dimensional Components
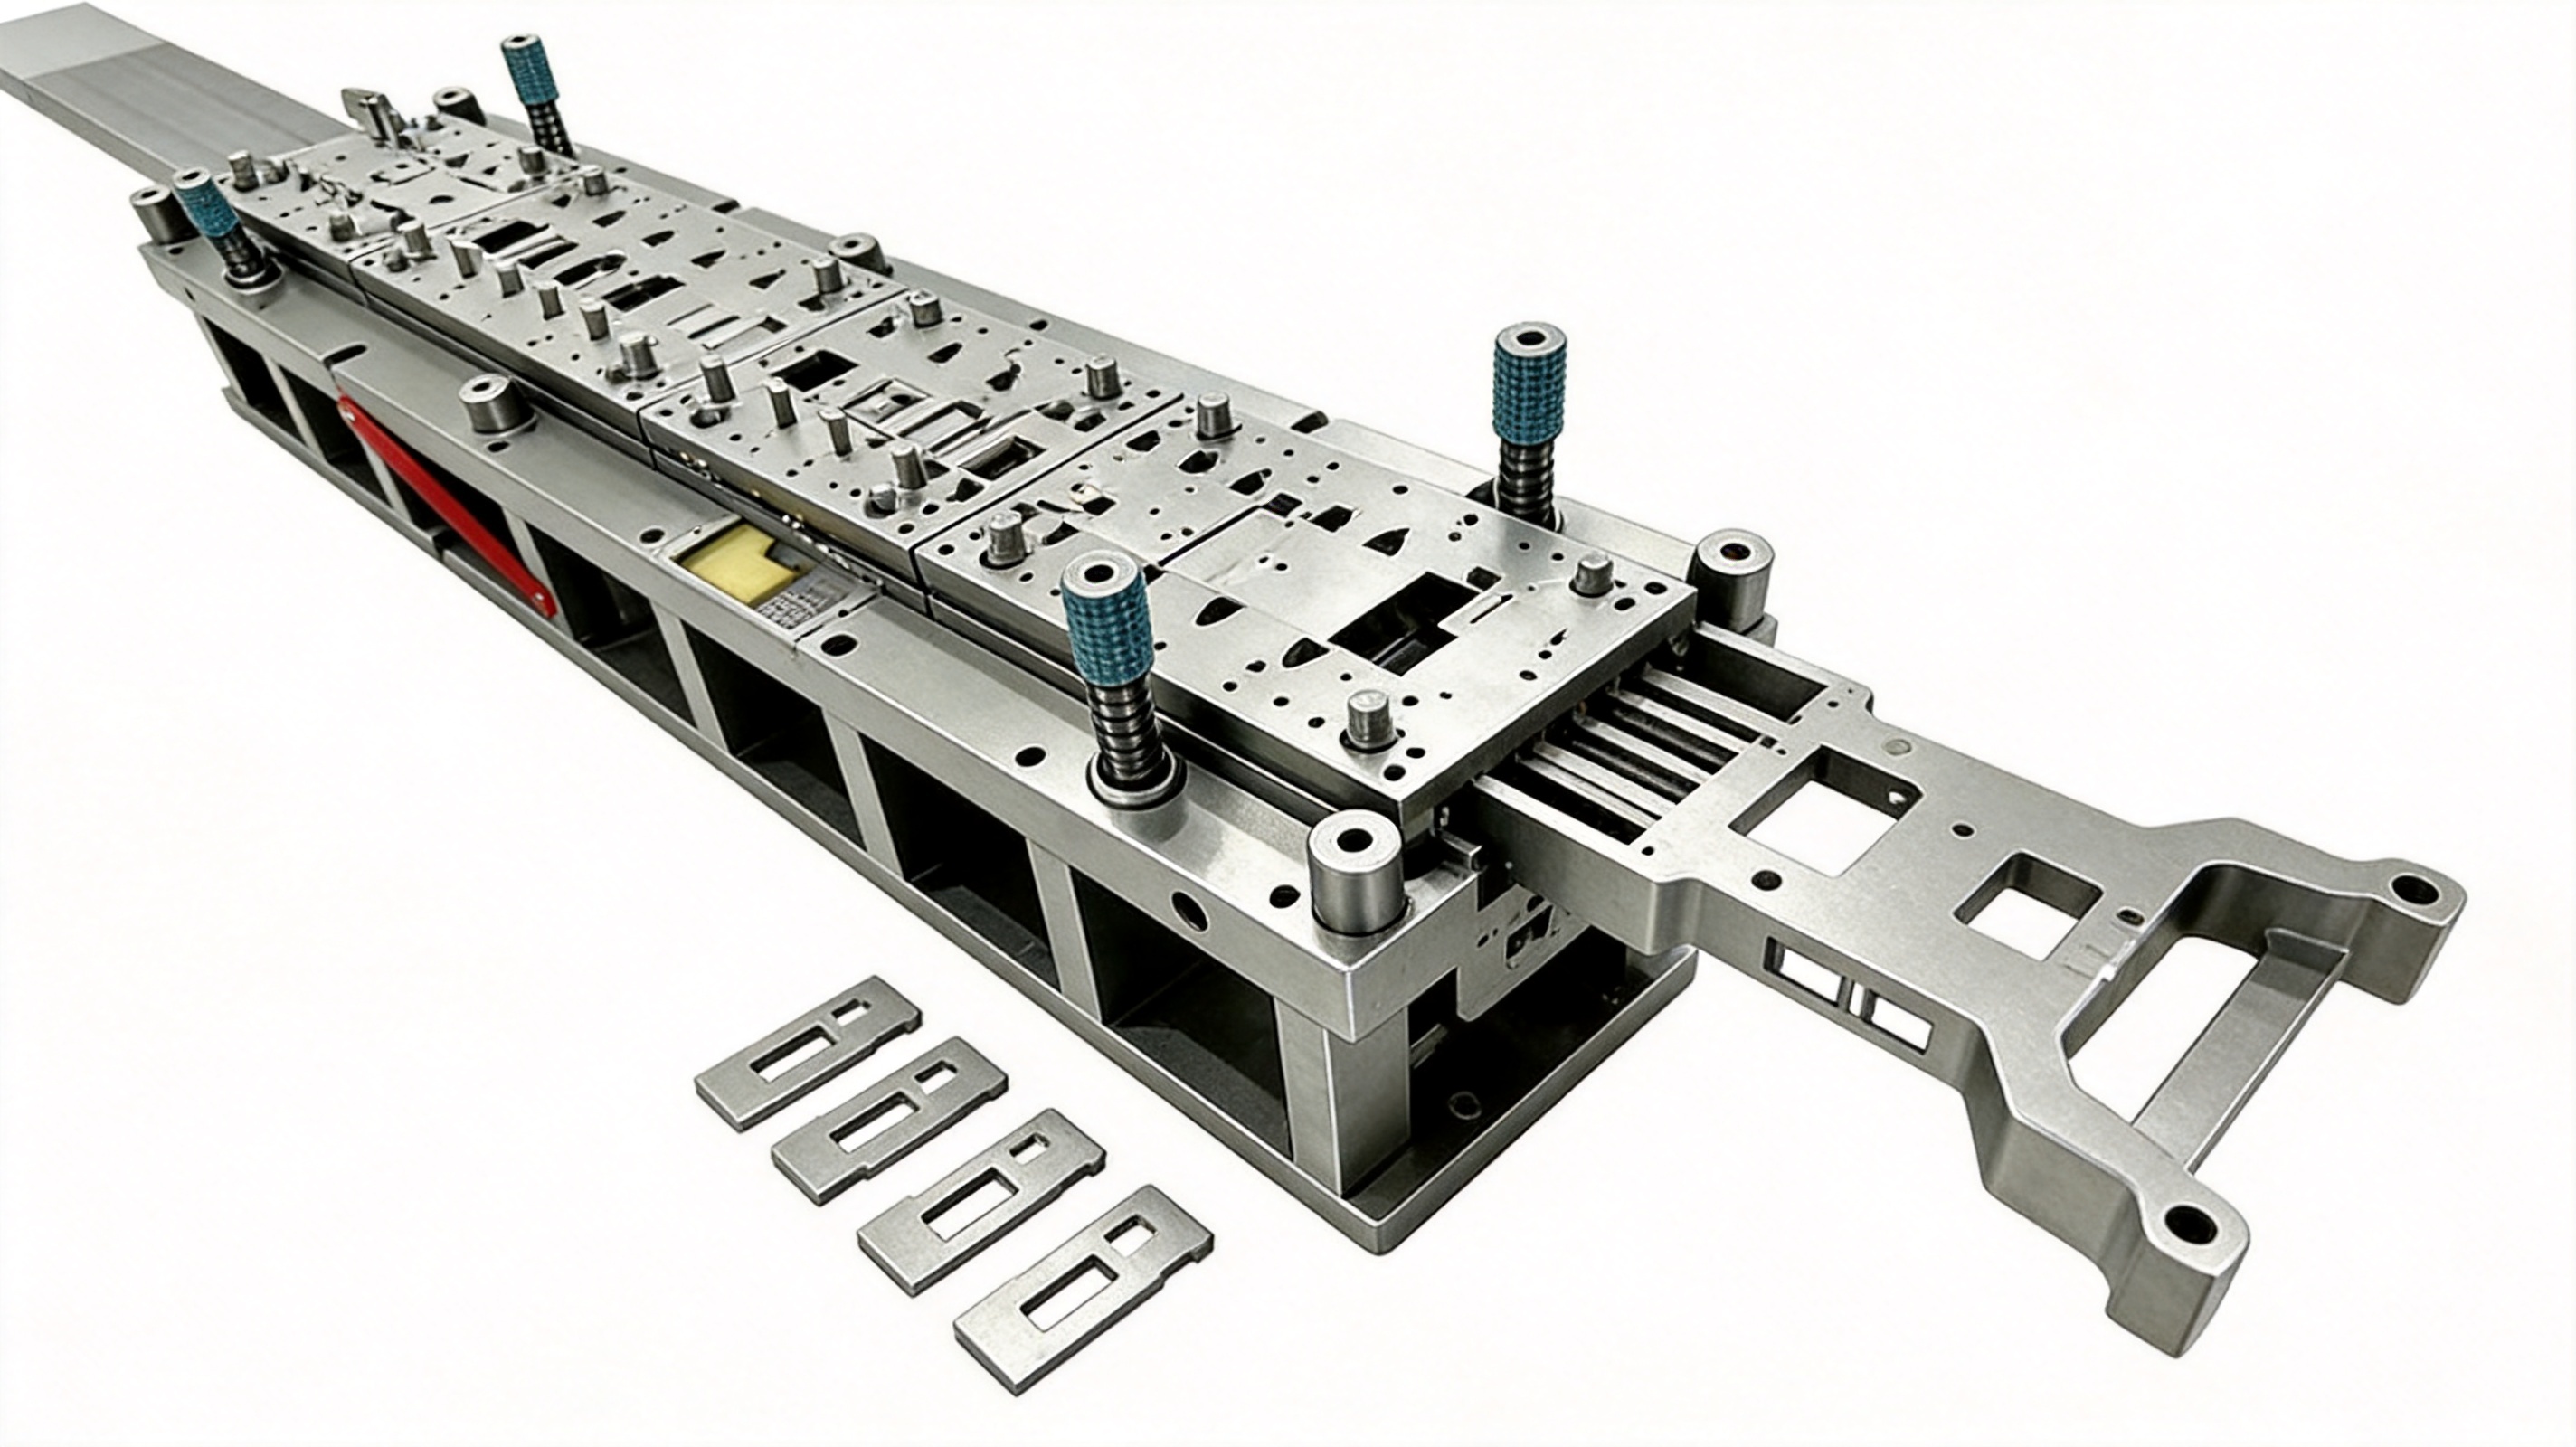
The central advantage of this die concept is its ability to transform a flat strip into a complex three-dimensional component through a controlled sequence. The process can include both cutting and forming actions, allowing holes, slots, tabs, beads, ribs, bends, and final contours to be created in one automated progression.
Piercing and Initial Material Preparation
Piercing is often carried out during the early part of the sequence. Holes used for assembly, positioning, or later pilot registration can be produced before the strip undergoes major deformation. Notching and lancing may also be used to create reliefs, tabs, or local openings.
The timing of each cut must be coordinated with the future forming operations. A hole positioned too close to a bend may deform during later forming. A notch that removes too much material may weaken the carrier. By analyzing material flow and feature interactions during die design, the manufacturing process can preserve part strength and dimensional accuracy.
Pre-Bending
Pre-bending introduces a controlled initial angle without requiring the material to reach its final position immediately. This reduces the shock associated with a large single-stage bend and helps guide the flange or wall into the correct path.
Pre-bending is especially useful for high-strength steel, stainless steel, thick-gauge materials, and components with narrow or elongated flanges. The first bending station may create a modest angle, while later stations gradually increase the angle and establish the final profile.
Final Bending and Restriking
Final bending stations bring the feature closer to its required angle and position. Restriking stations then apply a controlled finishing load to stabilize the geometry. In many cases, the restrike operation also improves the flatness of mating surfaces and reduces variation caused by material memory.
For parts that must fit into an assembly, the final restriking operation can be essential. It allows the die to compensate for predictable springback and helps maintain a repeatable relationship between mounting holes, flanges, and formed walls.
Embossing, Coining, and Local Calibration
Embosses and ribs can add stiffness without significantly increasing material weight. Coining may sharpen an edge, define a local radius, flatten a surface, or create a controlled indentation. These operations require accurate alignment between the punch and die insert.
When such features are placed too early in the sequence, later bending may distort them. When placed too late, access or material movement may become difficult. A multi-stage layout gives the tool designer flexibility to position these features at the most appropriate point in the process.
Trimming and Final Separation
At the end of the sequence, excess carrier material and unwanted edges can be trimmed. The final blanking station separates the completed part from the strip. Depending on the component design, the carrier may be removed by a complete perimeter cut, a partial cut followed by a controlled break, or a dedicated separation operation.
Final separation must be designed to prevent deformation of the completed component. A poorly timed or unsupported blanking cut can twist a flange or mark a finished surface. The final station therefore combines cutting clearance, support, ejection, and discharge considerations.
Springback Compensation and Dimensional Stability
Springback is one of the most important challenges in sheet metal forming. After the forming load is released, the material attempts to return partially toward its original shape. The amount of springback depends on material strength, thickness, grain direction, bend radius, forming angle, tooling condition, and process history.
High-strength steels and stainless steels often produce more pronounced springback than mild steel. As automotive and electric vehicle manufacturers use stronger and lighter materials, springback control becomes increasingly important. A die that produces acceptable results with low-carbon steel may require significant adjustment for advanced high-strength steel.
The long-stroke multi-stage design addresses springback through several methods:
• Dividing a large bend into pre-bending and final-bending operations.
• Using restrike stations to stabilize critical angles.
• Applying local coining where appropriate.
• Adjusting bend radii according to material behavior.
• Supporting the strip during and after each forming step.
• Compensating the die geometry based on measured trial results.
• Separating cutting and forming loads to reduce unwanted distortion.
Incremental forming makes the process more predictable. Rather than relying on one severe deformation, the tool manages the material in stages. This also makes troubleshooting more efficient. If a bend angle is incorrect, the relevant station can be studied and adjusted instead of modifying an entire multi-operation hit.
Modular forming inserts further support springback compensation. If material lots change or a customer updates the target angle, the affected insert can be revised or replaced without rebuilding the complete die. This reduces modification time and protects the value of the original tooling investment.
Long-Strip Stability and Anti-Warping Design
Strip control becomes more difficult as the die length increases. Every piercing, bending, and forming operation changes the stiffness and balance of the strip. A long carrier may become uneven, twist near an open feature, or lift during feeding if it is not properly supported.
The die addresses these risks through a combination of precision pilots, lifters, pressure pads, guide rails, and carrier design. Pilot pins are positioned at suitable intervals to establish accurate registration. Strip lifters support the material during die opening and help it move without dragging across the working surfaces. Pressure pads hold the strip in position during cutting and forming.
Guide rails maintain lateral control, while local support surfaces prevent unsupported sections from vibrating or bending. The arrangement must be carefully coordinated with scrap windows, forming punches, and moving inserts. Excessive support can interfere with the part, while insufficient support can reduce stability.
The carrier layout is equally important. A carrier that is too narrow may not withstand the forming loads. A carrier that is too wide may waste material or obstruct forming access. The design must balance strip utilization, rigidity, part release, and safe scrap removal.
Long-strip stability directly affects hole position, bend angle, part flatness, and overall production reliability. When the strip remains flat and accurately registered, each station can perform its intended operation with fewer unexpected variations.
Heavy-Duty Die Base and Multi-Point Guidance
A long die body must remain rigid under repeated press loads. Even minor deflection can produce changes in cutting clearance, bend depth, and parallelism between the upper and lower sections. Over millions of cycles, these errors can result in burrs, uneven forming, premature wear, or inconsistent product dimensions.
The die is built on a stress-relieved and precision-ground base. Stress relief helps reduce the risk of dimensional movement after machining. Precision grinding establishes flat reference surfaces and supports accurate assembly of plates, inserts, guide systems, and die components.
Instead of relying only on guide pillars at the four corners, a long-stroke design can use multiple guide pillar sets distributed along the die length. This multi-point guidance supports the entire working area and helps maintain parallel movement between the upper and lower die sections.
This approach reduces the risk of a “banana effect,” in which the central area of a long die deflects differently from the ends. It also helps maintain more consistent clearance across multiple cutting stations. Consistent clearance is essential for controlling burr height, tool life, and cut-edge quality.
Heavy-duty construction is particularly important when the die processes thick-gauge material or includes substantial forming operations. The frame, plates, fasteners, guide components, and inserts must work as a unified structure. A die that is strong in one area but flexible in another may still produce unstable results.
Modular Forming Inserts and Maintenance Efficiency
Progressive dies operate continuously and may produce hundreds of thousands or millions of parts. Wear is therefore inevitable in cutting edges, forming surfaces, pilots, springs, guide components, and ejectors. Maintenance planning must be considered during the initial design rather than after the tool enters production.
Modular inserts allow individual working areas to be removed, inspected, sharpened, adjusted, or replaced. If one piercing punch wears faster than another, it can be serviced independently. If a bend angle requires adjustment, the relevant forming insert can be modified without dismantling the entire die.
This modular architecture offers several advantages:
• Faster replacement of worn components.
• Reduced maintenance downtime.
• Lower modification cost.
• Easier spare-part management.
• Simplified troubleshooting during tryout.
• Better flexibility when part designs change.
• Improved protection of the main die base.
Insert materials and heat-treatment requirements are selected according to the operation. High-wear cutting areas may require hardened tool steel or specialized surface treatment. Forming inserts may be selected for toughness, resistance to galling, and dimensional stability. The correct balance depends on the material being stamped and the expected production volume.
Because each station can be inspected separately, maintenance personnel can identify the source of dimensional drift more quickly. This is especially valuable in a long die, where a defect observed at the final part may originate from a station many positions earlier in the sequence.
Integrated Scrap Management and Part Ejection
Progressive stamping produces scrap at many points in the process. Pierced slugs, notched pieces, trimmed edges, and carrier remnants must be removed continuously. If scrap accumulates inside the die, it may interfere with moving components, damage the working surfaces, or cause an unplanned press stoppage.
Internal scrap chutes guide slugs toward designated discharge points. The chute design must account for gravity, press orientation, slug size, material shape, and potential nesting. Some scraps fall directly through openings, while others require channels, air assistance, or mechanical removal.
Scrap management is not merely a housekeeping issue. It is part of the die’s safety and reliability system. A small slug trapped beneath a forming insert can change the die height and damage both the tool and the part. Proper scrap routing reduces this risk and makes production easier to monitor.
At the final station, the finished part may be discharged by an air blow, mechanical kicker, stripper, ejector pin, or conveyor interface. The selected method depends on part weight, orientation, surface sensitivity, and downstream handling requirements.
Automated ejection eliminates the need for an operator to retrieve parts from the press area. It supports continuous operation and can be connected to conveyors, collection bins, inspection systems, or robotic transfer equipment. For parts with delicate flanges or visible surfaces, the discharge system can be designed to minimize impact and scratching.
Product Advantages Compared with Conventional Stamping Solutions
One Integrated Process Instead of Several Separate Dies
A conventional production route may require separate dies for piercing, bending, embossing, trimming, and final calibration. Each transfer between dies introduces handling time, alignment variation, labor cost, and work-in-process inventory.
The long-stroke progressive die combines these operations into one automated sequence. This reduces the number of separate machines and simplifies production management. It can also reduce the risk of accumulating dimensional errors during manual transfers.
Higher Automation and Lower Labor Dependence
Automatic strip feeding, pilot registration, progressive forming, scrap removal, and part ejection reduce manual intervention. Operators can focus on material loading, process monitoring, quality checks, and scheduled maintenance rather than transferring individual parts between operations.
Lower labor dependence is especially valuable in high-volume production, where stable cycle times and consistent handling are essential. Automation also improves workplace safety by reducing the need for operators to work close to moving press components.
Better Repeatability for Complex Geometry
Every station is designed to reference the strip and the die’s registration system. This creates a controlled relationship between features. A hole, bend, and embossed detail can be positioned relative to one another more consistently than when they are produced in separate operations with manual repositioning.
Repeatability is important for automotive brackets, electrical connectors, battery supports, shielding components, and other parts that must fit into assemblies with limited adjustment allowance.
Controlled Forming Loads
Dividing the work across many stations reduces the demand placed on any one operation. The press still requires adequate capacity, but the force is distributed more intelligently. This can help reduce deformation of the die base, improve tool life, and permit the use of more controlled forming sequences.
Faster Product Design Changes
Modular inserts and station-based construction allow targeted modifications. A design update affecting one hole, bend, flange, or emboss can often be handled at the relevant station. This is more efficient than redesigning several independent dies or changing an entire one-hit tool.
Improved Long-Run Production Stability
The combination of multi-point guidance, strip support, modular wear parts, internal scrap routing, and controlled ejection supports stable long-term operation. This makes the die suitable for parts that must be produced repeatedly over extended production programs.
Manufacturing Process for the Progressive Die
The quality of the final stamping die depends heavily on the quality of its design and manufacturing process. A professional die manufacturer typically uses a structured workflow that connects product analysis, process planning, machining, assembly, tryout, measurement, and customer validation.
Part and Material Review
The process begins with a review of the customer’s component drawings, three-dimensional models, material grade, thickness, tolerance requirements, annual volume, press specifications, and downstream assembly conditions.
Engineers evaluate bend directions, narrow features, hole-to-edge distances, material flow, carrier options, scrap ratios, and likely springback. If a feature cannot be produced reliably in the proposed sequence, the die concept can be revised before detailed design begins.
Process Planning and Station Layout
The next stage is to develop the operation sequence. Engineers determine which features should be cut first, where pre-bending should begin, how many forming stages are required, and where restriking or coining should be placed.
The station layout must balance several factors: forming feasibility, strip stability, tool strength, press capacity, material utilization, maintenance access, scrap discharge, and finished-part ejection. A longer tool is not automatically better; the length must provide a technical purpose and remain compatible with the customer’s press line.
Three-Dimensional Die Design
After the process sequence is approved, the die components are developed in three-dimensional CAD. This includes the die base, upper and lower plates, punches, dies, pilots, pressure pads, lifters, inserts, guide rails, scrap channels, sensors, and ejection components.
Clearance, interference, stroke, shut height, forming depth, and maintenance access are reviewed digitally. Critical stations can be evaluated for material movement and potential collision before steel is cut.
Precision Machining
Die plates and inserts are produced using CNC machining centers, wire cutting equipment, grinding machines, drilling systems, and other precision machine tools. Fine profiles and narrow slots may require wire electrical discharge machining. Surfaces that control accuracy or wear are finished through grinding and careful fitting.
Machining quality directly affects assembly accuracy. A small deviation in a reference plate or insert location can influence several downstream stations. For this reason, manufacturing must be managed through controlled datum structures and inspection procedures.
Heat Treatment and Surface Preparation
Selected tool components receive heat treatment appropriate to their function. Cutting punches and high-wear inserts generally require high hardness and dimensional stability, while some structural elements require a balance between strength and toughness.
After heat treatment, components may require grinding or finishing to restore critical dimensions. Surface treatments can also be considered for reducing friction, galling, or adhesive wear when compatible with the stamped material and production conditions.
Assembly and Manual Fitting
Precision components are assembled into the die set and checked for smooth movement, correct alignment, suitable clearances, and proper return action. Skilled toolmakers fit critical surfaces and verify that pilots, lifters, pressure pads, and inserts operate without interference.
Manual fitting remains important even in a highly mechanized manufacturing environment. It helps resolve the small interactions between components that may not be fully represented by digital models, particularly in complex forming areas.
Tryout, Debugging, and Validation
Before delivery, the die undergoes tryout on a suitable press. Initial trials verify whether the strip feeds correctly, whether the die closes smoothly, whether the forming sequence is stable, and whether the part exits without damage.
Trial parts are inspected for burr height, hole position, bend angle, flatness, flange width, embossing depth, surface marks, cracks, wrinkles, and overall geometry. If a dimension is outside the required range, engineers identify whether the cause is related to feed accuracy, material behavior, forming depth, clearance, insert position, or springback.
Debugging is performed station by station. Adjustments may include changing a forming insert, modifying a restrike surface, correcting a pilot position, improving strip support, changing a lifter height, or optimizing the scrap path. The objective is not merely to obtain one acceptable sample but to establish a stable production window.
Experienced debugging personnel are particularly valuable for long progressive dies because defects can be cumulative. A small deviation at an early station may become a significant issue by the final station. Systematic inspection allows the root cause to be addressed rather than compensating for symptoms at the end of the process.
Validation may include dimensional inspection, capability studies, repeatability checks, cycle testing, material-lot comparisons, and continuous production trials. The final acceptance criteria should be agreed with the customer according to the product’s function and applicable quality requirements.
Manufacturing Capabilities and Integrated Technical Strengths
A manufacturer with integrated die-making and stamping automation capabilities can support the project beyond the fabrication of steel components. This is valuable because the die, feeder, press interface, part discharge, and production controls must function as one system.
The manufacturing organization described in the supplied company information has approximately 60 technical staff, 25 punch presses ranging from 80 to 400 tons, imported wire cutting machines, CNC machining centers, and more than ten grinding machines of different sizes. These resources support the production of precision tooling as well as trial stamping and process verification.
The available press range allows tools to be tested under different capacity conditions. Press selection depends on material thickness, part size, forming requirements, die dimensions, stroke, shut height, and production speed. Trialing the tool on an appropriate machine helps confirm that the design is suitable for the customer’s intended press environment.
Fifteen years of experience in the mold industry provides practical knowledge of stamping materials, progressive die construction, tool maintenance, and production troubleshooting. The company’s technical team has supplied molds and stamped products for servo drives, compressors, and new energy vehicle applications, where dimensional stability and production reliability are important.
The organization also established a related intelligent technology company focused on stamping automation equipment. This supports the development of turnkey solutions that may include progressive dies, automatic feeding systems, conveying equipment, collection systems, and other production-line components.
Integrated capability can reduce communication gaps between separate suppliers. When one technical team understands the die, feeder, press, and discharge requirements, it can coordinate interfaces more effectively. It can also help the customer evaluate the complete production investment instead of assessing the die as an isolated item.
Application Areas
Automotive and Electric Vehicle Components
The die is suitable for seat brackets, door panel clips, hinge components, brake line clips, sensor mounting brackets, connector housings, reinforcement plates, and structural hardware. Electric vehicle applications may include battery module brackets, busbar support frames, cooling-system clips, charging connector parts, and motor-related sheet metal components.
These applications often require high repeatability, controlled springback, accurate hole location, and reliable production over long runs. The progressive process can support both structural and functional components where multiple bends and pierced features are integrated into one part.
Electrical and Electronic Hardware
Relay frames, terminal blocks, switch housings, connector shells, EMI shielding cans, PCB mounting clips, and electrical support brackets can benefit from precise progressive forming. These parts may contain narrow tabs, fine slots, small bends, and close positional relationships.
Controlled feeding and accurate pilot positioning are especially important for connector and terminal applications. The tool must maintain consistent feature location while preventing burrs or deformation that could affect electrical assembly.
Telecommunications and Data Center Equipment
Server chassis brackets, cable management clips, rack hardware, shielding frames, heat sink mounting parts, and equipment support components can be produced using a multi-stage progressive process. These parts frequently combine mounting holes, offsets, stiffening beads, and return flanges.
Home Appliances
Washer and dryer brackets, compressor mounting plates, hinge components, control panel frames, and motor support structures are examples of appliance hardware that may require repeated bends and cut features. Long-run production and stable cycle time are often important for these products.
Industrial Automation
Sensor brackets, actuator clips, conveyor components, relay sockets, terminal strip housings, and machine mounting hardware can be produced with a progressive die when the part geometry and annual volume justify the tooling investment.
Aerospace-Related Sheet Metal Components
Lightweight bracket preforms, clip fasteners, and structural sheet metal components may also be considered, provided that the material, documentation, inspection, traceability, and quality requirements are defined appropriately. Projects for regulated industries require customer-specific compliance and validation procedures.
Key Technical Parameters to Define Before Ordering
Successful die development begins with complete technical information. Customers should provide the latest part drawing or three-dimensional model, material grade, thickness range, dimensional tolerances, surface requirements, annual quantity, target cycle rate, and intended press information.
Other important details include coil width, feed direction, grain direction, permissible burr orientation, acceptable scrap ratio, packaging method, part discharge direction, and whether the final part may require washing, deburring, plating, or secondary assembly.
The press specification should include nominal tonnage, stroke length, strokes per minute, shut height, bolster dimensions, slide dimensions, die mounting arrangement, feed-line height, and available automation interfaces. A die designed without accurate press data may require avoidable modification later.
It is also useful to identify the most critical product dimensions. Not every feature has the same functional importance. A mounting hole, assembly flange, or electrical contact surface may require tighter control than a nonfunctional exterior edge. This information helps engineers prioritize restriking, calibration, inspection, and process capability efforts.
Typical Process Structure
| Process Stage | Typical Function | Primary Quality Objective |
|---|---|---|
| Coil preparation | Uncoiling, straightening, and strip alignment | Stable material entry and flatness |
| Initial piercing | Creating holes, slots, and reference features | Accurate feature position and clean edges |
| Notching or lancing | Preparing reliefs, tabs, and carrier geometry | Controlled material flow and carrier strength |
| Pre-bending | Introducing gradual angular deformation | Reduced forming shock and controlled springback |
| Intermediate forming | Creating offsets, walls, ribs, and local contours | Stable three-dimensional geometry |
| Final bending | Bringing flanges and walls to target position | Correct angle and dimensional relationship |
| Restriking or coining | Calibrating critical features and surfaces | Improved repeatability and fit |
| Trimming | Removing excess material and refining edges | Correct contour and burr control |
| Final blanking | Separating the finished component | Clean separation without deformation |
| Ejection | Transferring the part to a conveyor or container | Damage-free and uninterrupted discharge |
How to Select the Right Progressive Die Supplier
A suitable supplier should demonstrate more than the ability to machine individual die components. The supplier should understand the complete stamping process, including material behavior, press compatibility, strip layout, automation, maintenance, and production validation.
Relevant questions include whether the supplier can perform process analysis before design, whether it has in-house machining and grinding capability, whether it can conduct press tryout, whether it can support automation integration, and whether replacement inserts and technical assistance will be available after delivery.
Experience with similar materials and part families is also important. A supplier that has produced tools for automotive, electrical, compressor, servo drive, or new energy applications may be better prepared to address the dimensional and production challenges associated with these sectors.
Quality control should cover incoming material, machining dimensions, heat treatment, component hardness, assembly accuracy, trial parts, and final documentation. Clear inspection records help customers understand the tool’s condition and provide a baseline for future maintenance.
Communication is another critical factor. Long progressive dies involve many technical decisions. A supplier that communicates clearly about station layout, expected tolerances, press requirements, risks, and modification plans can help prevent misunderstandings and reduce development delays.
Maintenance and Production Support
Even a well-designed progressive die requires regular maintenance. Cutting edges should be inspected for wear, pilots should be checked for damage, springs and lifters should be monitored, and scrap channels should be cleaned. Lubrication points must be maintained according to the tool design and stamped material.
Operators should record burr changes, feed errors, abnormal noise, part deformation, and increasing press load. These signs may indicate wear or misalignment before a major failure occurs. Preventive maintenance is generally less expensive than emergency repair after a punch breaks or an insert is damaged.
Replacement parts should be identified and stored according to a practical spare-parts plan. Modular inserts make it easier to keep critical components available without purchasing a complete duplicate die. Maintenance records can also reveal which stations experience the highest wear and whether process improvements are justified.
Technical support after delivery is valuable when the customer introduces a new material lot, changes the press speed, or modifies a part drawing. Because the die may produce several operations in one cycle, troubleshooting should consider the complete process rather than only the final station.
Economic Value of the Long-Stroke Progressive Approach
The initial investment in a complex progressive die can be higher than the cost of a simple single-operation tool. However, the correct comparison must include the full production system. Labor, handling equipment, floor space, secondary operations, work-in-process inventory, quality inspection, and cycle time all influence the total cost per part.
For high-volume components, an integrated progressive die can reduce recurring costs by completing several operations automatically. It can also decrease the number of operators, simplify material flow, and reduce the time between coil entry and finished-part collection.
Higher repeatability may reduce scrap and rework. Automated feeding and ejection can improve production consistency. Modular maintenance can reduce downtime. These benefits become increasingly significant over the life of a long production program.
The design is most economical when the part has sufficient volume and enough complexity to justify a multi-stage process. For very low-volume parts or simple flat blanks, a simpler die may be more appropriate. A professional supplier should evaluate the application honestly and recommend the process that best matches the customer’s production objectives.
Questions and Answers
What type of parts are suitable for this die?
The die is suitable for complex sheet metal parts with multiple bends, pierced holes, offsets, embosses, tabs, ribs, and three-dimensional features. Typical examples include automotive brackets, electric vehicle battery hardware, electrical connector housings, shielding parts, appliance brackets, and industrial clips.
How many stations can the die contain?
The supplied product concept supports an extended layout of approximately eight to more than thirty forming stations, depending on the component geometry and process requirements. The exact number is determined through engineering analysis rather than selected as a fixed standard.
Can the die process high-strength steel?
It can be designed for high-strength steel, stainless steel, and other challenging sheet materials when the material grade, thickness, forming limits, press capacity, and required tolerances are properly defined. Multi-stage bending and restriking help control springback and reduce excessive deformation.
Why are multiple pilot pins important?
Multiple pilot locations maintain strip registration along the extended die body. They help prevent cumulative feed error, twisting, and lateral movement, especially after the strip has undergone several cutting and forming operations.
How is springback controlled?
Springback is managed through staged bending, suitable bend radii, controlled material support, restriking, coining where appropriate, and geometry compensation based on trial results. The exact method depends on material properties and part requirements.
Can individual die stations be modified?
Yes. Modular forming and cutting inserts allow the affected station to be adjusted or replaced in many cases. This is useful for design changes, material-lot variation, wear correction, and springback compensation.
How are stamping slugs and scrap removed?
Internal scrap chutes and designated discharge paths guide pierced slugs and trimmed material away from the working area. The design may also use gravity, air assistance, or mechanical discharge, depending on scrap geometry and die orientation.
How is the finished part removed?
The finished component can be discharged by air blow, mechanical kicker, ejector, or conveyor transfer. The appropriate method depends on the part’s size, orientation, weight, surface condition, and downstream handling requirements.
Can the die be integrated with stamping automation equipment?
Yes. An integrated die and automation supplier can coordinate the progressive tool with coil handling, straightening, feeding, scrap collection, part conveyors, and other press-line equipment. This helps create a complete production solution instead of an isolated die.
What press capacity is required?
The required capacity depends on material thickness, tensile strength, part size, cutting perimeter, forming loads, station layout, and production speed. The company’s stated equipment range includes presses from 80 to 400 tons for manufacturing and trial purposes, but the appropriate press must be selected for each project.
How does the tool improve production efficiency?
It combines multiple operations into one automated progression, reducing manual transfer, secondary bending, work-in-process handling, and the number of separate dies required. It also supports stable cycle times and continuous part discharge.
What information should be submitted for a quotation?
Customers should provide the latest part drawing or model, material and thickness, annual production volume, tolerance requirements, surface specifications, press information, target cycle rate, coil details, and any special requirements for inspection, packaging, automation, or downstream assembly.
Conclusion
The long-stroke multi-stage progressive die is an advanced solution for manufacturers that need to produce complex sheet metal components accurately, continuously, and economically. Its extended station layout allows piercing, bending, forming, embossing, coining, trimming, blanking, and ejection to be coordinated within one automatic strip-fed process.
Its main advantages include controlled multi-stage forming, springback compensation, long-strip stability, multi-point guidance, modular inserts, integrated scrap removal, and automated finished-part discharge. These features make it more capable than short-stroke tools intended mainly for simple blanking or limited forming.
The performance of the die depends not only on its physical design but also on the supplier’s engineering process. Part analysis, process planning, precision machining, grinding, heat treatment, assembly, tryout, debugging, and automation integration must be managed as connected activities.
With approximately 15 years of mold-industry experience, a technical team of around 60 staff, CNC machining centers, imported wire cutting equipment, multiple grinding machines, and punch presses ranging from 80 to 400 tons, Suzhou Shuangqisi Mold Equipment Co., Ltd. can support custom stamping die development and production validation. Its related automation capability also enables turnkey solutions for stamping molds and production equipment.
For automotive, electric vehicle, electrical, appliance, industrial, telecom, and other high-volume applications, this integrated approach can help improve dimensional consistency, reduce labor dependence, shorten production flow, and create a more reliable manufacturing process for complex three-dimensional sheet metal hardware.
References
1. Product information supplied for the long-stroke multi-stage progressive die and automatic strip-feed stamping tool.
2. Company information supplied for Suzhou Shuangqisi Mold Equipment Co., Ltd., including manufacturing equipment, technical personnel, press capacity, and automation capabilities.
3. ASM Handbook, Volume 14B: Metalworking—Sheet Forming.
4. Metal Stamping Design Guidelines, general principles for progressive die layout, clearance, strip development, and forming sequence planning.
5. Technical literature on springback control, staged bending, restriking, and forming of high-strength sheet materials.
6. General industrial practices for progressive die maintenance, tool wear monitoring, scrap management, and automated press-line integration.
Product: Long-Stroke Multi-Stage Progressive Die Automatic Strip Feed Progressive Die Long Travel Follow on Stamping Tool for Sheet Metal Hardware Press Moulding
Previous Post
Progressive Stamping Dies for High-Speed Connector, Terminal, and Automotive Metal Parts
Next Post
Gas Tank End Stamping Parts: Precision-Formed Components for Reliable Automotive Fuel Tanks
Our Products.
Start Your Business with an OEM Manufacturer Right Here!

Provide global customers with complete turn-key solutions
through
innovation!
QUICK LINKS
CONTACT INFO.
-
 +86-139 1308 8972
-

-
 No. 118 Yexin Road, Wujiang Economic Development Zone, Suzhou, China
Copyright © Suzhou Shuangqisi Mold Equipment Co., Ltd. All Rights Reserved. Custom Stamping Die Metal Stamping Die Manufacturers
