 English
 Español
 Deutsch
-

Progressive Stamping Die for Connector & Terminal Parts High Speed Progressive Stamping Die Precision Metal Hardware Stamping Tool mold for Connector Terminal Parts Automotive Components
Progressive Stamping Die for Connector & Termi...
-
High Precision Stamping Die Multi Station Hardware Progressive Mold Tooling
Precision Metal Stamping Tool for Automotive &...
-
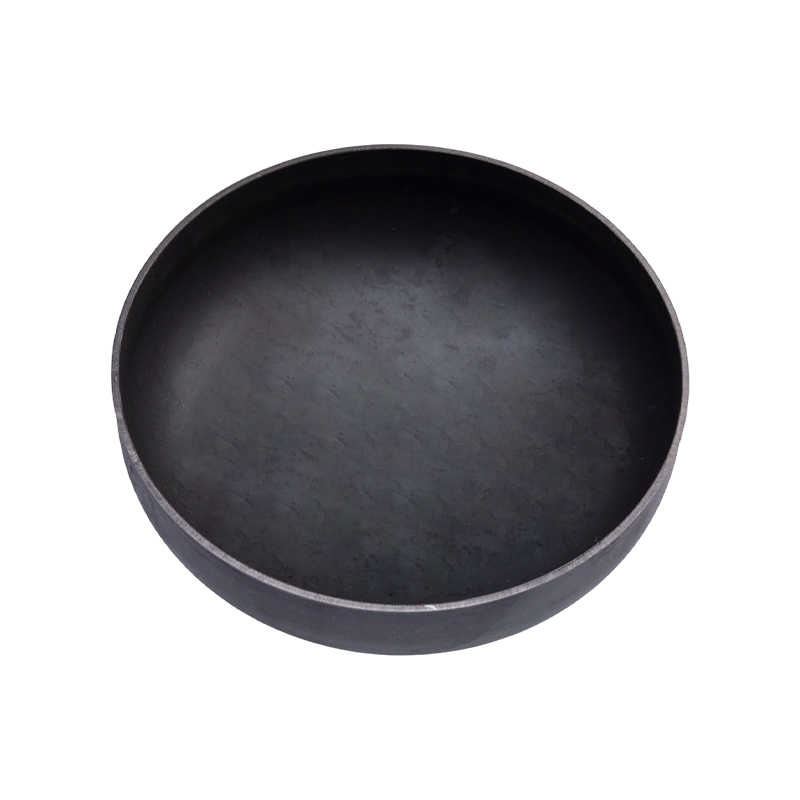
Gas tank end stamping parts
Gas tank end stamping parts are core structural co...
-

Long-Stroke Multi-Stage Progressive Die Automatic Strip Feed Progressive Die Long Travel Follow on Stamping Tool for Sheet Metal Hardware Press Moulding
Long-Stroke Multi-Stage Progressive DieOur custom ...
-
Multi-Station Progressive Stamping Die with Carbide Inserts Custom Multi Station Progressive Stamping Die Carbide Insert Metal Stamping Mold Tool for Equipment Appliances Device Hardware
High Speed Metal Stamping Tool for Precise Equipme...
- E-mail us: [email protected]
- Call us: +86-139 1308 8972

Zhou Mengjie – Technical Sales Specialist
Home / Author / Zhou Mengjie – Technical Sales Specialist / Gas Tank End Stamping Parts: Precision-Formed Components for Reliable Automotive Fuel Tanks
Gas Tank End Stamping Parts: Precision-Formed Components for Reliable Automotive Fuel Tanks
2026-10-12
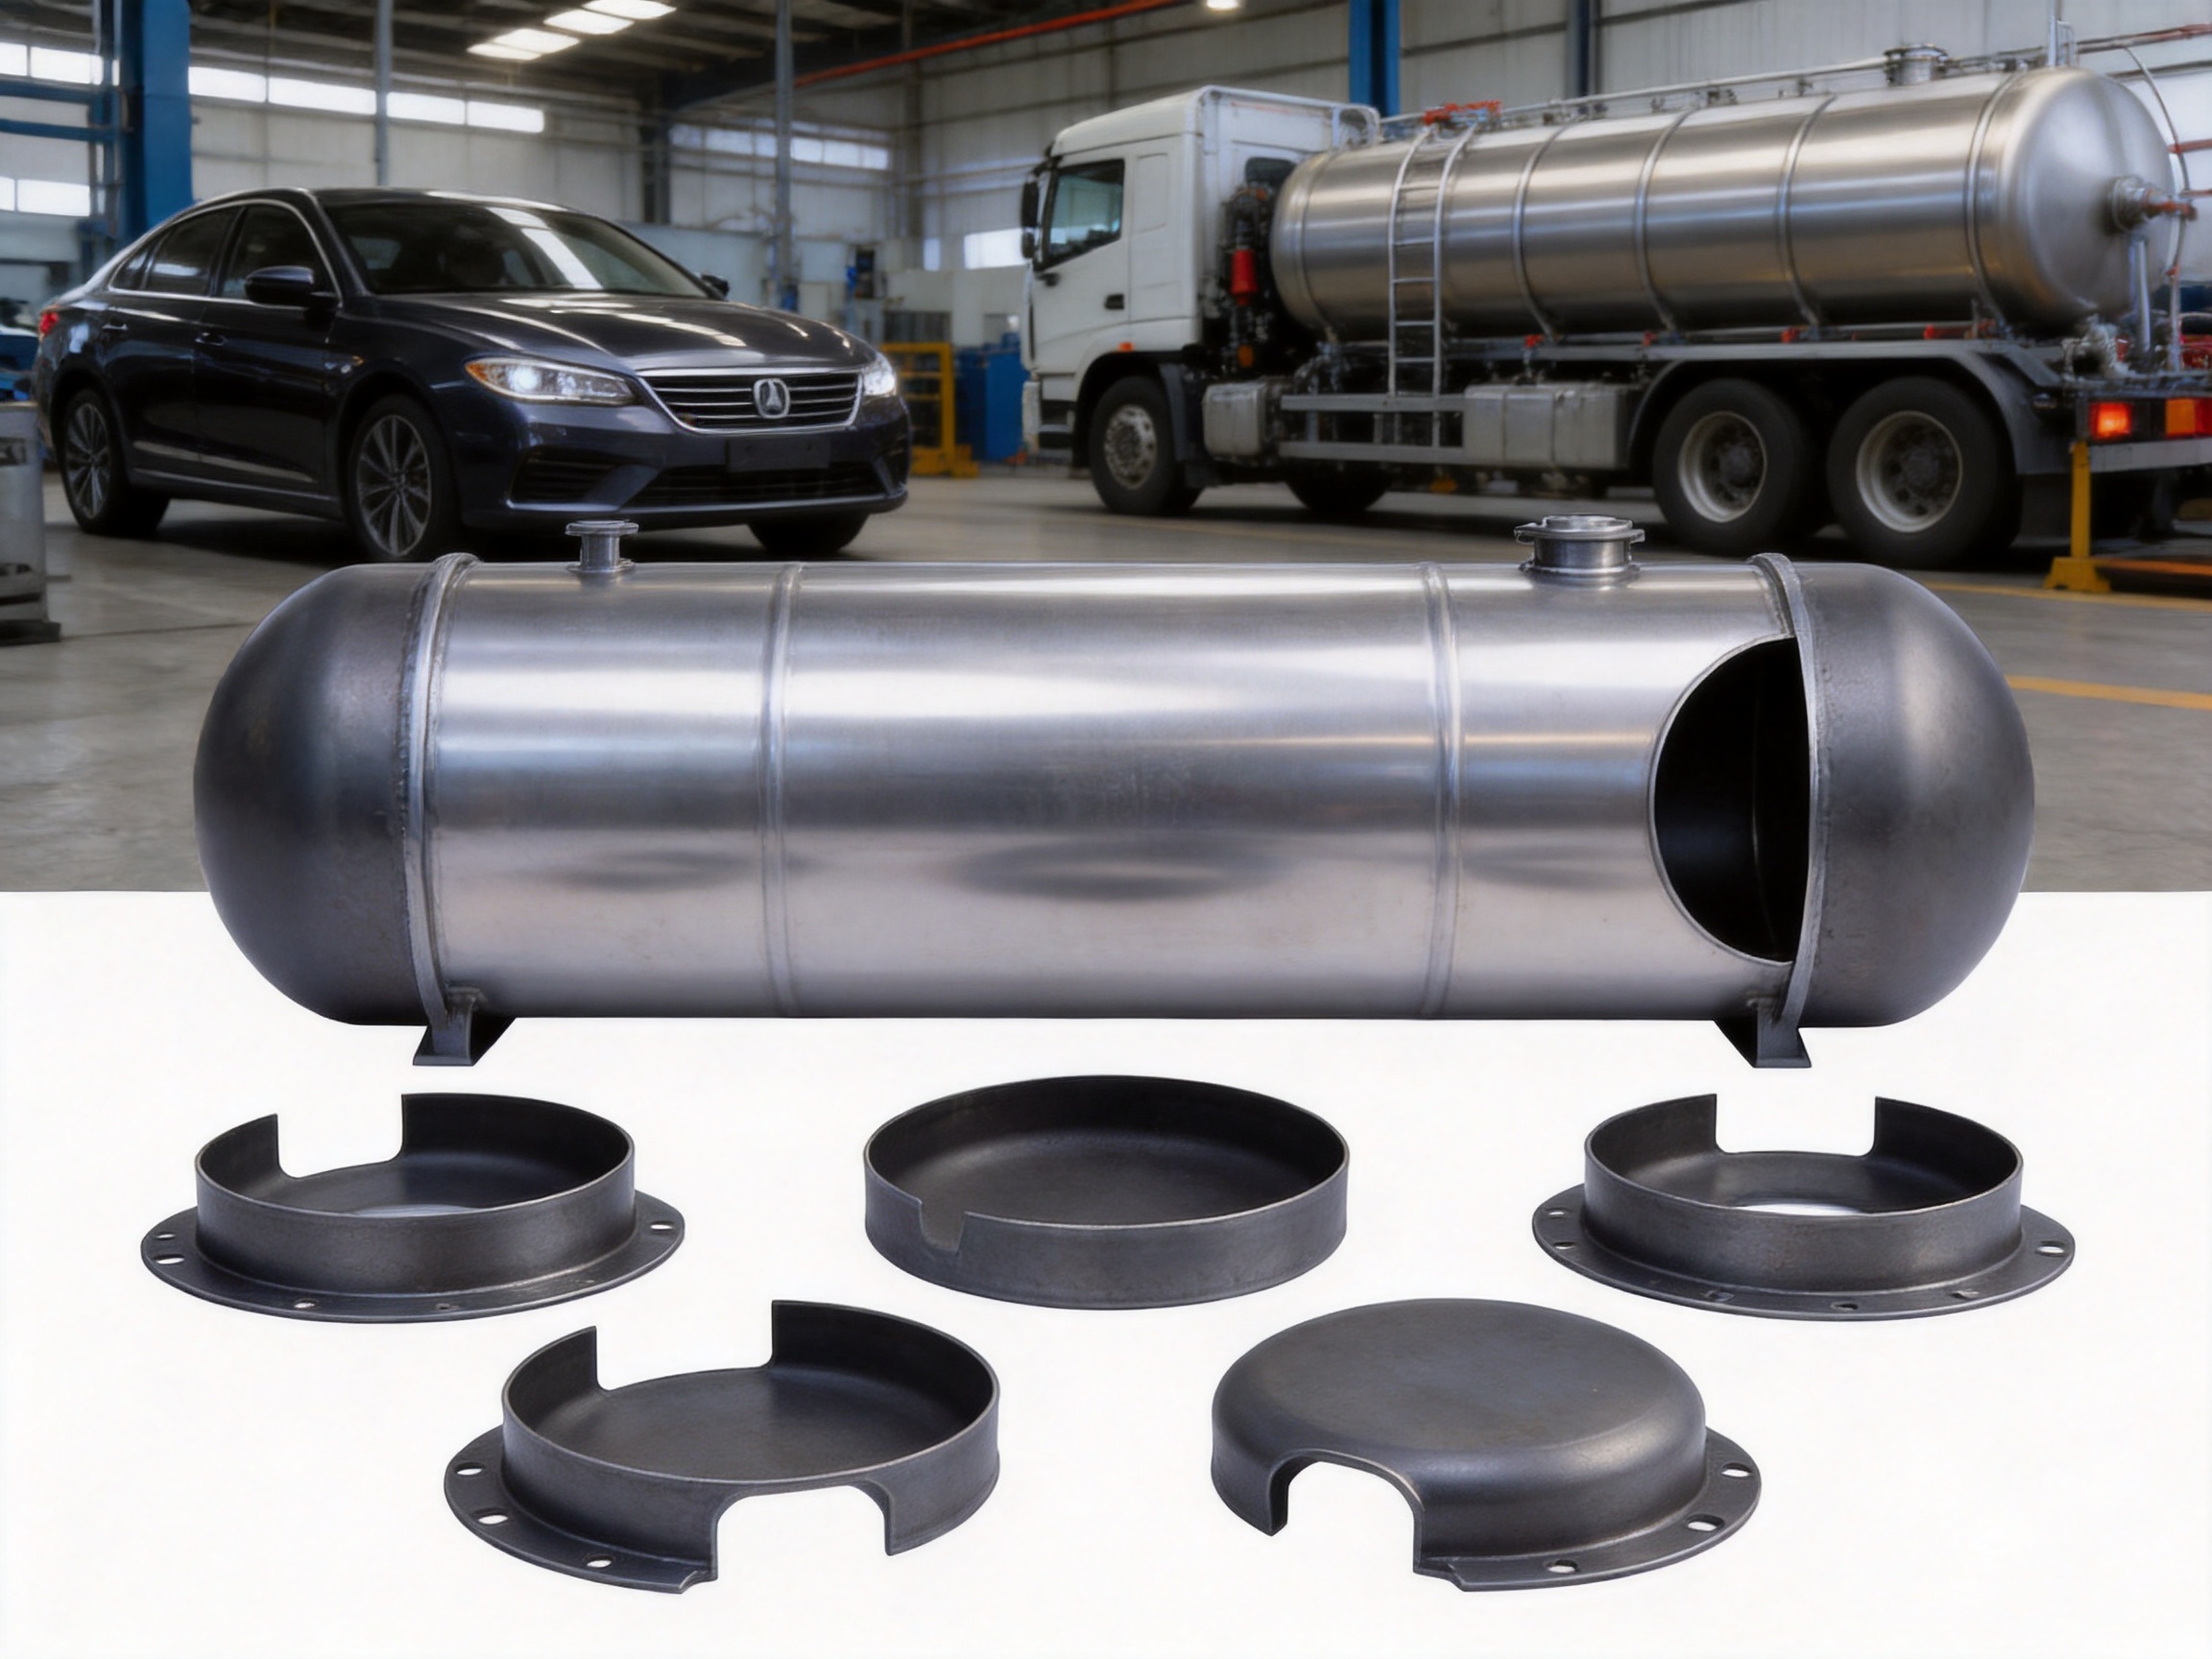
Gas tank end stamping parts are essential structural and sealing components used in automotive fuel tank assemblies. Although their shape may appear simple, these formed metal parts perform several demanding functions at the same time. They close the ends of a cylindrical or specially shaped fuel tank, help maintain the tank’s structural integrity, support reliable joining with the tank body, and contribute to long-term resistance against fuel leakage, vibration, pressure fluctuation, corrosion, and temperature changes.
For automotive manufacturers, fuel tank suppliers, and vehicle maintenance organizations, the quality of end components directly affects the performance and service life of the complete tank assembly. An end part with inaccurate dimensions, uneven thickness, surface cracking, insufficient forming depth, or poor compatibility with the tank body can create assembly difficulties and increase the risk of leakage or premature failure. For this reason, high-precision stamping is widely used to manufacture these components in a controlled, repeatable, and cost-effective manner.
Suzhou Shuangqisi Mold Equipment Co., Ltd. manufactures metal stamping dies, stamping parts, and stamping automation equipment for industrial customers. Its capabilities combine die design, precision mold manufacturing, stamping production, process debugging, and automation integration. This integrated approach supports the production of gas tank end stamping parts with consistent dimensions, controlled forming quality, and reliable production efficiency.
The company’s manufacturing resources include imported wire cutting machines, CNC machining centers, more than ten grinding machines of different sizes, and 25 punch presses ranging from 80 tons to 400 tons. Supported by technical personnel, experienced operators, and debugging specialists, the production system is designed to serve a range of metal-forming requirements for automotive, new energy, compressor, servo-drive, and other industrial applications.
Gas tank end stamping parts
Content
- 1 What Are Gas Tank End Stamping Parts?
- 2 Why End Components Matter in Fuel Tank Construction
- 3 Key Product Advantages
- 4 Recommended Materials and Their Characteristics
- 5 Manufacturing Process for Gas Tank End Stamping Parts
- 5.1 1. Technical Review and Product Feasibility Analysis
- 5.2 2. Die Structure and Process Planning
- 5.3 3. Precision Die Manufacturing
- 5.4 4. Blanking and Material Preparation
- 5.5 5. Drawing and Forming
- 5.6 6. Trimming, Piercing, and Flanging
- 5.7 7. Restraining, Calibration, and Debugging
- 5.8 8. Inspection and Quality Verification
- 6 Integrated Tooling and Automation Capability
- 7 Production Equipment and Technical Resources
- 8 Quality Risks and How They Are Controlled
- 9 Advantages Compared with Less Specialized Suppliers
- 10 Applications in Passenger and Commercial Vehicles
- 11 Customer-Specific Customization
- 12 Production Efficiency and Cost Control
- 13 Packaging, Storage, and Delivery Considerations
- 14 Why Choose a Specialized Stamping Die and Part Manufacturer?
- 15 Inspection Questions Customers Should Ask
- 16 Q&A: Gas Tank End Stamping Parts
- 16.1 What is the primary function of a gas tank end stamping part?
- 16.2 Which materials can be used?
- 16.3 Can the parts be customized for different vehicle models?
- 16.4 Why is die precision important?
- 16.5 How are cracks and wrinkles controlled?
- 16.6 What press capacity is required?
- 16.7 Are aluminum alloy end parts possible?
- 16.8 Can the supplier provide tooling and finished parts?
- 16.9 Can automation be included in the project?
- 16.10 What quality problems should be checked before shipment?
- 16.11 How does an integrated supplier reduce project risk?
- 16.12 What information should be provided for a quotation?
- 17 Conclusion
- 18 References
- 19 Product: Gas tank end stamping parts
What Are Gas Tank End Stamping Parts?
Gas tank end stamping parts are formed metal components installed at one or both ends of an automotive fuel tank. Depending on the tank design, the parts may be circular, oval, domed, stepped, flanged, or shaped with additional contours that correspond to the geometry of the tank body. Their primary purpose is to close and reinforce the tank while providing a suitable interface for welding, assembly, inspection, and installation of related accessories.
These components are generally manufactured from cold-rolled steel, coated steel, stainless steel, or aluminum alloy, depending on vehicle design, fuel compatibility, corrosion requirements, weight targets, and production standards. Material selection is important because the part must retain sufficient strength after forming while also resisting cracking, springback, corrosion, and distortion.
In many applications, the end stamping part is produced through a sequence that may include blanking, drawing, forming, trimming, piercing, flanging, restriking, and inspection. The specific sequence is determined by the part’s geometry and the customer’s technical requirements. A carefully designed process reduces material waste, limits forming defects, and improves compatibility with the tank body and other fuel-system components.
Why End Components Matter in Fuel Tank Construction
A fuel tank is exposed to changing internal and external conditions throughout the vehicle’s service life. Fuel volume changes as the tank is filled and emptied. Temperature variations cause fuel and vapor expansion. Road vibration produces repeated mechanical loading. Moisture, salt, mud, and other environmental factors can accelerate corrosion if the material or surface treatment is inadequate.
The end components help distribute these loads around the tank structure. Their formed geometry can improve stiffness compared with a flat plate, allowing the tank to resist deformation without requiring excessive material thickness. Properly shaped ends also allow the tank body to be sealed more effectively and provide controlled contact areas for welding or other joining operations.
Dimensional accuracy is equally important. The outside profile of an end component must correspond closely with the tank body. A mismatch can result in gaps, local stress concentration, irregular weld penetration, or difficulty positioning the part during assembly. Consistent production therefore supports not only the component itself but also the efficiency and repeatability of the customer’s downstream tank manufacturing process.
Key Product Advantages
Precision Forming and Dimensional Consistency
Precision stamping enables gas tank end parts to be produced with repeatable dimensions and controlled geometry. Properly engineered dies guide the sheet material through a stable forming path, reducing variation between individual parts. This consistency is valuable when components must be assembled with cylindrical tank bodies, brackets, valves, sensors, fuel lines, and other accessories.
Compared with manually formed or irregularly fabricated parts, precision-stamped components provide a more predictable fit. They can also support automated or semi-automated assembly because their dimensions and orientation are more uniform. For original equipment manufacturers and high-volume suppliers, this reduces adjustment work and helps maintain stable production takt times.
Reliable Sealing Performance
Fuel tank end parts must contribute to a sealed enclosure. Smooth forming transitions, accurate edge profiles, and controlled flange dimensions help create a reliable joining surface. When the part is properly matched with the tank body, welding or other approved joining methods can be performed more consistently.
The component itself does not replace the complete sealing system, because final performance depends on material compatibility, welding parameters, coating conditions, inspection, and tank design. However, a well-manufactured end stamping part provides the dimensional foundation needed for a secure and repeatable joint.
Resistance to Pressure and Structural Loading
Internal fuel vapor pressure and external mechanical forces place continuous demands on the tank structure. Curved and formed end geometries can provide improved rigidity compared with flat sheet metal. The design distributes loads across the end surface and into the surrounding tank wall, helping reduce localized deformation.
Material thickness, draw depth, corner radius, and forming direction all influence the final strength of the part. A suitable stamping process preserves the intended geometry while minimizing thinning, wrinkling, and residual stress. These factors are especially important for vehicles operating in environments with large temperature changes or severe road vibration.
Smooth Surface Quality
Automotive fuel tank parts must have a clean and uniform surface. Cracks, deep scratches, folds, excessive tool marks, and sharp irregularities may affect corrosion resistance, assembly, appearance, or functional performance. Controlled die surfaces, appropriate lubrication, suitable forming speed, and effective process monitoring help produce smooth components with a stable visual and functional finish.
A uniform surface also supports subsequent operations such as cleaning, coating, welding, leak testing, and dimensional inspection. When the surface condition is stable, downstream processes are less likely to experience contamination, inconsistent contact, or localized quality problems.
Material Efficiency and Production Economy
Stamping is well suited to medium- and high-volume production because a properly developed die can form many parts with consistent cycle times. Compared with labor-intensive machining or fabrication from multiple pieces, stamping can reduce secondary processing and material waste.
Production economy depends on more than press speed. It also relies on efficient nesting, suitable blank design, durable tooling, controlled scrap management, stable die maintenance, and reduced rework. An integrated mold and stamping supplier can optimize these elements together rather than treating die production and part production as separate activities.
Compatibility with Different Vehicle Applications
Gas tank end stamping parts can be designed for different passenger car and commercial vehicle fuel tank configurations. The appropriate design may vary according to tank capacity, body space, fuel-system layout, material selection, mounting structure, and connection requirements.
Custom tooling allows the component to follow the customer’s drawings and technical specifications. It also permits the development of different end profiles, flange arrangements, holes, beads, reinforcing features, and assembly interfaces. This flexibility is useful for vehicle platforms that require model-specific tank dimensions.
Recommended Materials and Their Characteristics
Material selection must be based on the complete operating environment rather than on cost alone. The sheet must withstand forming without excessive cracking or wrinkling, retain strength after processing, and remain compatible with fuel, vapor, coatings, welding methods, and corrosion-protection systems.
| Material Type | Main Characteristics | Potential Applications | Important Manufacturing Considerations |
|---|---|---|---|
| Cold-rolled steel | Good formability, strength, availability, and cost efficiency | General automotive tank structures and formed end components | Control draw depth, corner radius, lubrication, and surface protection |
| Coated steel | Improved corrosion resistance through a protective surface layer | Fuel tank applications requiring enhanced environmental durability | Protect the coating during forming and control joining conditions |
| Stainless steel | High corrosion resistance and stable mechanical performance | Specialized or demanding fuel-system environments | Use suitable tooling, forming parameters, and surface protection practices |
| Aluminum alloy | Low density, good corrosion resistance, and weight-reduction potential | Lightweight vehicle designs and selected tank structures | Manage springback, galling, surface marks, and alloy-specific formability |
Cold-rolled steel is commonly selected when a balance of formability, mechanical strength, and cost is required. Aluminum alloy may be preferred when reducing vehicle weight is a priority. However, aluminum requires careful control of springback and tool contact because its forming behavior differs from that of steel. The correct material must therefore be evaluated together with the die design and production method.
Manufacturing Process for Gas Tank End Stamping Parts
1. Technical Review and Product Feasibility Analysis
Manufacturing begins with a review of the customer’s drawings, material specifications, dimensional tolerances, functional requirements, and intended joining method. Engineers assess the part geometry, forming direction, available press capacity, blank size, draw ratio, flange design, and likely deformation behavior.
At this stage, potential risks such as corner cracking, excessive thinning, wrinkling, springback, difficult trimming, and tool interference are identified. Early feasibility analysis helps prevent costly changes after tooling has already been manufactured. It also allows the supplier to recommend practical modifications that improve production stability without compromising the customer’s functional requirements.
2. Die Structure and Process Planning
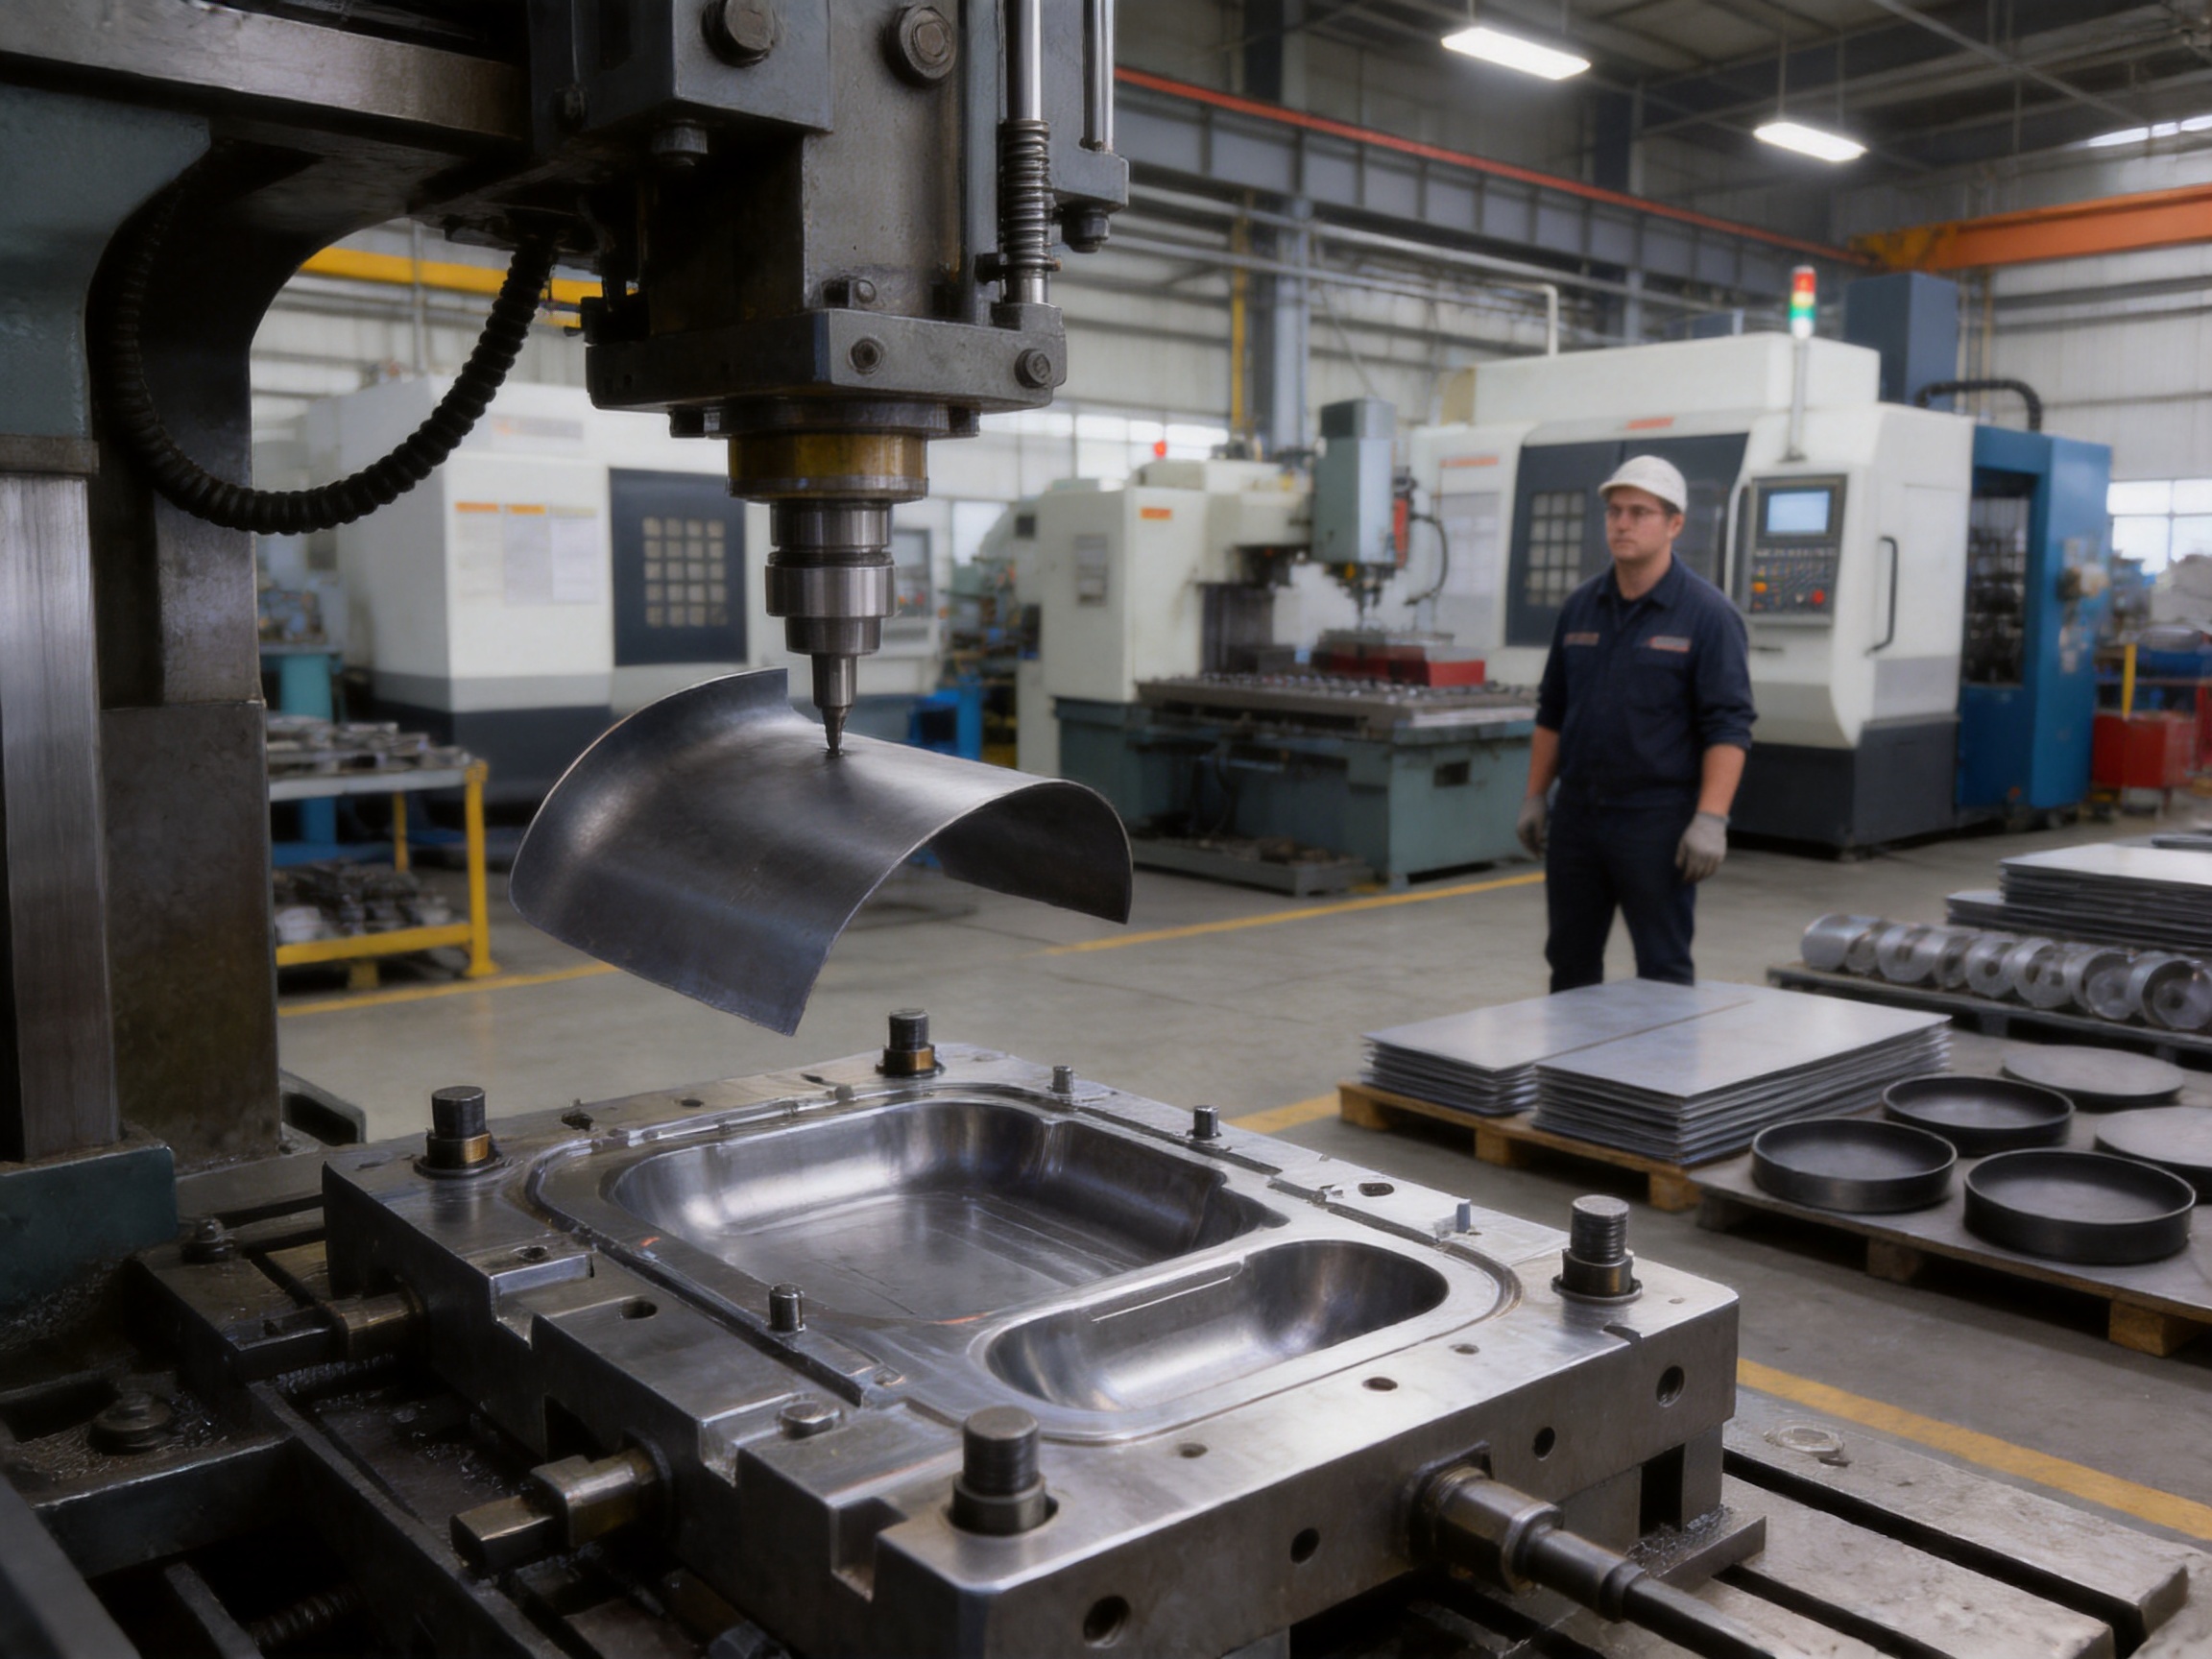
Die design is one of the most important factors affecting final part quality. The tool must guide the sheet through each forming stage while controlling material flow and maintaining the intended geometry. Depending on the component, the tooling may include blanking dies, drawing dies, trimming dies, piercing dies, flanging dies, restriking tools, or progressive and transfer arrangements.
The process plan is developed around the part’s shape, material, volume, and tolerance requirements. A simple component may be completed in a small number of operations, while a deep or highly contoured end component may need several stages. Proper sequencing reduces stress concentration and distributes deformation more evenly across the material.
3. Precision Die Manufacturing
After design approval, die components are machined and finished using precision equipment. CNC machining centers are used to create complex cavities, inserts, plates, and locating features. Wire cutting machines support the production of accurate profiles and intricate die details. Grinding machines are used to achieve controlled dimensions and appropriate surface conditions on critical components.
Tool accuracy affects more than the first sample. It influences long-term repeatability, maintenance requirements, part interchangeability, and the overall cost of production. A die manufactured with accurate working surfaces and robust guidance can maintain stable performance over extended production periods when operated and maintained correctly.
4. Blanking and Material Preparation
The sheet is first prepared into a blank with the required outline. Blank shape has a direct effect on material flow during drawing and forming. An inefficient blank may create unnecessary scrap or cause uneven deformation, while a properly developed blank can improve utilization and reduce the risk of defects.
Blanking quality is also important. Excessive burrs, distortion, or edge damage may interfere with later forming. The blanking operation must therefore be matched to the material thickness, die clearance, press condition, and required edge quality.
5. Drawing and Forming
In the drawing stage, the flat blank is transformed into the three-dimensional end shape. The die cavity, punch, blank holder, draw beads, and lubrication system work together to control material flow. If material enters the cavity too freely, wrinkling may occur. If it is restrained excessively, tearing or excessive thinning may result.
Drawing depth, corner radius, blank-holder force, press speed, and lubrication must be controlled according to the material and geometry. For complex components, multiple drawing or forming stages may be used instead of attempting to create the final shape in a single operation.
6. Trimming, Piercing, and Flanging
After the primary shape is formed, excess material may be trimmed to establish the final perimeter. Piercing operations create holes or openings required for assembly, brackets, valves, sensors, or other components. Flanging may then be used to create a joining edge, reinforcing lip, or controlled interface with the tank body.
These operations must preserve the dimensional relationship between the formed surface and the reference features. Poor alignment between trimming and forming can cause uneven flanges or inconsistent joining conditions. Precision die construction and accurate part positioning help maintain these relationships.
7. Restraining, Calibration, and Debugging
Some formed parts require restriking or calibration to correct springback and achieve the final dimensional profile. This is particularly relevant for aluminum alloys or geometries with large curved surfaces. A restriking operation applies controlled pressure to stabilize the shape without creating additional damage.
Die debugging is performed by experienced technical personnel who evaluate sample parts and adjust process parameters. Typical adjustments may involve die clearance, guide alignment, blank-holder force, material positioning, draw bead height, lubrication, press stroke, or operation sequence. Effective debugging converts the theoretical die design into a stable production process.
8. Inspection and Quality Verification
Quality control begins with incoming material verification and continues through die trials, first-article inspection, in-process checks, and final inspection. Dimensional checks confirm that the part meets the drawing requirements. Surface inspection identifies cracks, wrinkles, folds, scratches, dents, and other visible defects. Functional checks may include fit verification, flange inspection, and leak-related evaluation as required by the customer’s quality plan.
Inspection methods may include gauges, calipers, height gauges, profile templates, coordinate measurement, visual examination, and process-specific testing. The inspection system should be adapted to the component’s tolerance level and intended application. For fuel tank end parts, special attention is usually given to the sealing region, formed corners, joining flange, and any areas exposed to high stress.
Integrated Tooling and Automation Capability
One of the principal advantages of working with an integrated stamping supplier is the connection between die engineering, part production, and automation development. A tooling issue can be evaluated alongside the actual production process rather than being treated as an isolated design problem. This shortens communication cycles and supports faster correction when samples reveal a forming or assembly concern.
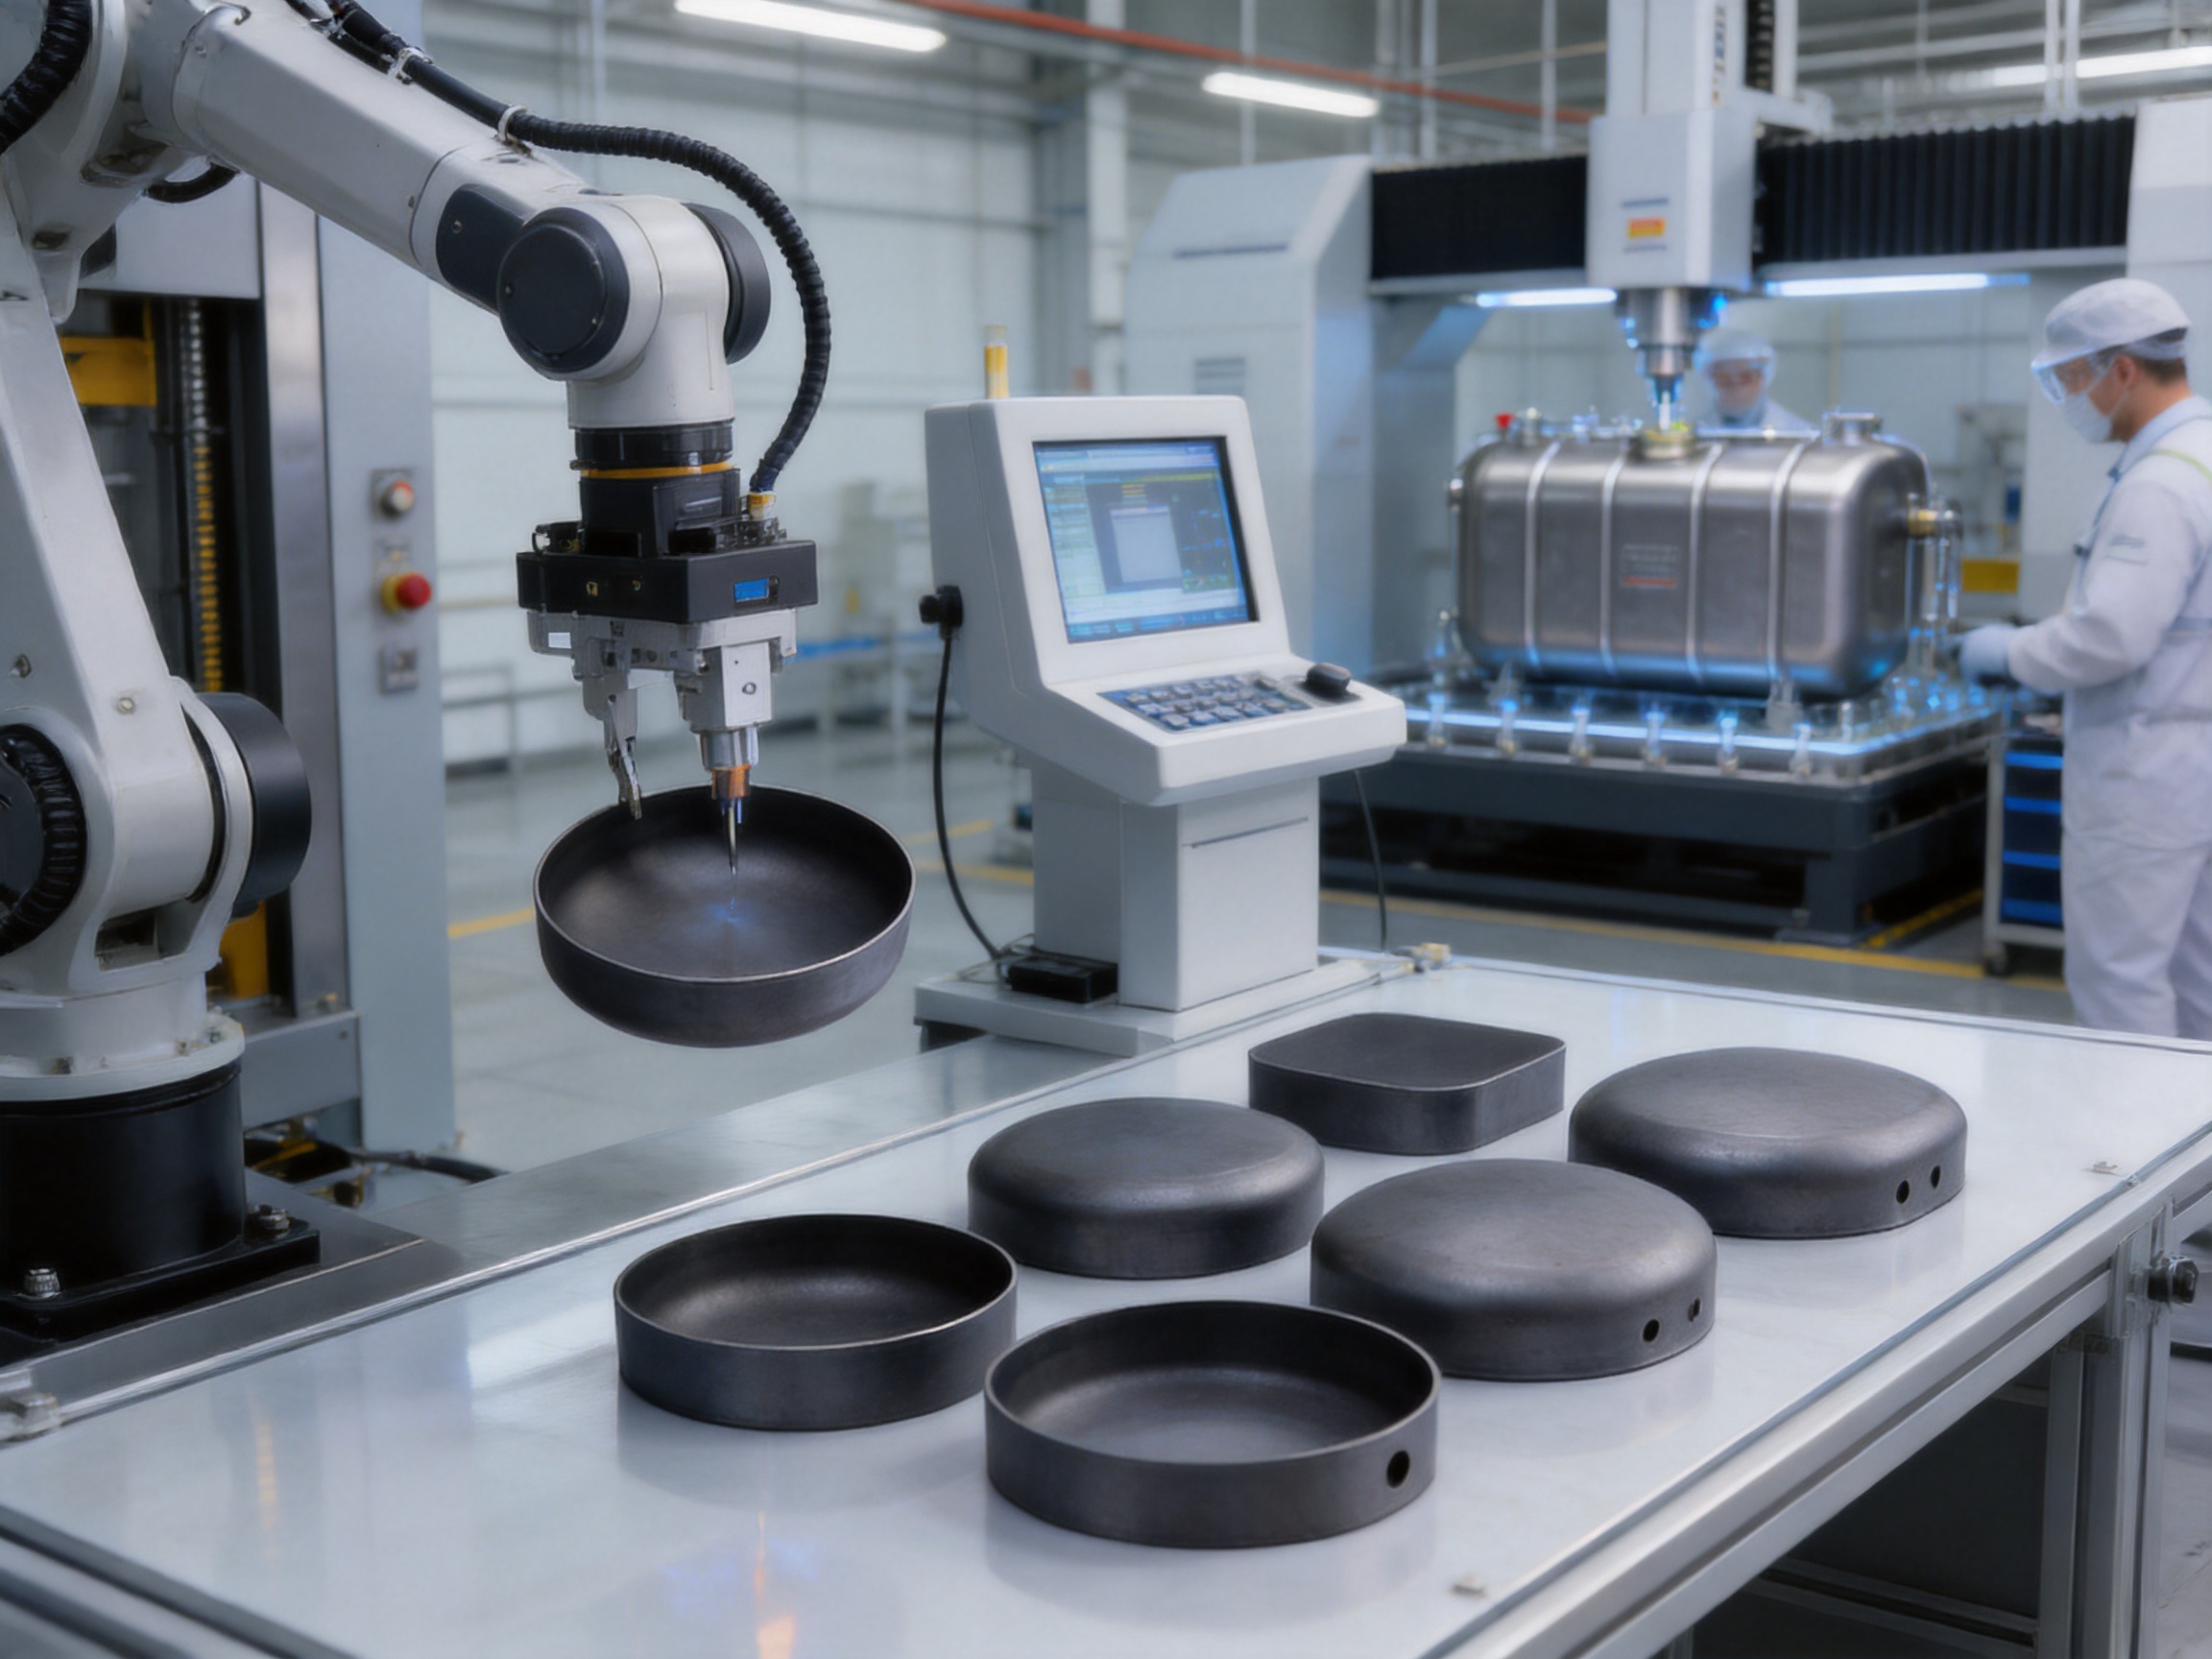
Suzhou Shuangqisi Mold Equipment Co., Ltd. provides stamping dies and stamping automation equipment in addition to stamping parts. Through its investment in Suzhou Keshuang Intelligent Technology Co., Ltd., the company also supports automation-related manufacturing capabilities. This allows customers to discuss tooling, press operation, material transfer, and production-line efficiency within a connected technical framework.
Automation can improve consistency by controlling loading, positioning, transfer, unloading, and inspection steps. It can also reduce manual handling and help protect formed surfaces from accidental damage. For higher-volume production, automated transfer or handling systems may improve cycle stability and support better process traceability.
A turnkey approach can be particularly valuable for customers establishing a new stamping line or expanding an existing one. Instead of sourcing dies, parts, automation, and debugging support from unrelated suppliers, the customer can coordinate these elements through a more unified project structure. This may reduce interface problems and make responsibility for process performance clearer.
Production Equipment and Technical Resources
Manufacturing equipment directly influences the range of components a supplier can produce. With 25 punch presses from 80 tons to 400 tons, the company has press capacity suitable for different part sizes, material thicknesses, forming requirements, and production volumes. The availability of multiple press capacities allows production planning to select equipment that matches the actual forming load rather than forcing every part onto a single machine type.
Imported wire cutting machines support accurate machining of die profiles and components. CNC machining centers are used for complex precision work, while grinding equipment helps achieve accurate dimensions and surface conditions on critical tooling elements. A combination of machining methods is often necessary because different die components require different levels of precision, surface finish, and geometric complexity.
Equipment alone does not guarantee quality. The technical team must understand how to apply the machines, verify results, maintain accuracy, and coordinate each operation with the wider process. Senior operators and experienced debugging personnel are therefore important resources in the development and production of automotive stamping parts.
Quality Risks and How They Are Controlled
Cracking and Tearing
Cracking may occur when the material is stretched beyond its forming capability, especially at corners, deep-draw regions, or pierced edges. Risk reduction methods include selecting suitable material, increasing forming radii where permitted, using multiple forming stages, adjusting lubrication, and controlling blank-holder force.
Tool surface damage or misalignment can also create localized stress. Regular die inspection and maintenance help identify worn or damaged areas before they affect a large number of parts.
Wrinkling
Wrinkling generally occurs when compressive stresses cause the sheet to buckle during forming. It may be controlled through blank-holder force, draw bead design, material flow adjustment, improved die guidance, or changes to the blank shape. Excessive restraint should be avoided because it can replace wrinkling with tearing.
Springback
Springback is the tendency of formed sheet metal to partially return toward its original shape after unloading. It can influence the end profile, flange position, and fit with the tank body. Calibration, restriking, compensation in the die design, and process parameter adjustment are common approaches to controlling springback.
Surface Marks
Surface marks may result from rough tooling, embedded particles, poor lubrication, improper handling, or excessive sliding friction. Keeping working surfaces clean and properly finished is essential. Operators should also use suitable handling practices to prevent dents and scratches after forming.
Dimensional Variation
Dimensional variation can be caused by material thickness differences, press instability, die wear, incorrect setup, temperature changes, or inconsistent positioning. A controlled inspection plan, stable tooling, correct press settings, and regular maintenance reduce these risks.
Corrosion Concerns
Corrosion resistance depends on the base material, coating, surface condition, storage environment, joining process, and final tank design. Forming should not unnecessarily damage protective coatings. After stamping, parts should be stored and handled in a way that limits moisture exposure, contamination, and mechanical damage.
Advantages Compared with Less Specialized Suppliers
Customers comparing suppliers should evaluate more than unit price. A low initial quotation may become expensive if the die requires repeated revisions, if part dimensions vary during production, or if the supplier cannot support automation and process debugging. The total cost includes tooling development, sampling, rework, scrap, logistics, maintenance, assembly disruption, and long-term quality performance.
An integrated manufacturer can offer several practical advantages:
First, die design and part production are connected. The people responsible for manufacturing the tool understand how it behaves during actual stamping and can respond more effectively to production feedback.
Second, the supplier can support both custom tooling and finished stamping parts. This provides continuity from initial design through mass production and reduces the risk of technical information being lost between separate vendors.
Third, a broader equipment base supports different press requirements. The availability of 80-ton to 400-ton presses gives production planners more flexibility when selecting an appropriate machine.
Fourth, automation capability can help customers improve line efficiency, repeatability, and labor utilization. This is increasingly important as automotive manufacturers seek more stable and traceable production systems.
Fifth, experience across automotive and industrial sectors can support cross-application problem solving. Experience with servo drives, compressors, new energy vehicles, and other formed products may help engineers recognize common issues related to material flow, tooling life, precision, and production organization.
Applications in Passenger and Commercial Vehicles
Gas tank end stamping parts are applicable to many fuel tank structures used in passenger cars, light commercial vehicles, trucks, and other road vehicles. The exact part configuration depends on tank capacity, available installation space, vehicle platform, fuel-system layout, and regulatory or customer requirements.
Passenger vehicle applications may prioritize compact packaging, low weight, corrosion resistance, and compatibility with complex tank shapes. Commercial vehicle applications may place greater emphasis on capacity, durability, vibration resistance, and long operating cycles. In both cases, dimensional compatibility and sealing reliability remain central requirements.
The parts may also be customized with openings, mounting features, reinforcement beads, or formed regions needed for tank accessories. A supplier that can develop the stamping die around the customer’s complete assembly requirements is better positioned to deliver a practical component rather than a generic formed shell.
Customer-Specific Customization
Customization begins with the customer’s technical documents. These may include two-dimensional drawings, three-dimensional models, material specifications, tolerance requirements, inspection standards, packaging instructions, and target production volumes. The supplier reviews the information and confirms whether the proposed geometry can be manufactured using the intended material and press capacity.
Where appropriate, the supplier may recommend changes to improve formability, reduce scrap, simplify die construction, or stabilize assembly. Any recommended change should be evaluated against the customer’s functional requirements. The objective is not to alter the product unnecessarily but to create a robust production method that satisfies the application.
Customization may involve the part outline, depth, curvature, flange dimensions, hole locations, bead features, material thickness, surface treatment, and packaging method. For customers with multiple vehicle models, common tooling concepts or modular die elements may also be considered where the designs share similar features.
Production Efficiency and Cost Control
Cost-effective stamping is achieved through coordinated decisions made before and during production. The blank layout influences scrap. The number of operations influences cycle time and tooling investment. The choice of press influences energy consumption, production capacity, and tool loading. The die material and heat treatment influence service life and maintenance frequency.
Process debugging also has a major effect on cost. A stable process reduces rejected parts, manual correction, unplanned downtime, and customer complaints. Clear inspection standards help operators identify deviations early instead of allowing a problem to continue through a full production batch.
Automation may further reduce handling time and improve part positioning. For large-volume orders, the resulting productivity improvement can be significant. For lower-volume or frequently changing products, flexible automation and well-organized manual processes may be more appropriate. The optimal solution depends on order quantity, product variety, labor conditions, and the customer’s investment plan.
Packaging, Storage, and Delivery Considerations
Even a precisely stamped component can be damaged after production if packaging is inadequate. Gas tank end parts should be arranged to prevent edge collision, surface scratching, deformation, and contamination. Protective separators, suitable containers, and stable stacking methods may be required depending on the part shape and surface condition.
Storage areas should be dry, clean, and organized. Components should be protected from excessive humidity and contact with corrosive substances. If the parts include a protective coating, handling procedures should limit abrasion and preserve the coating during transportation.
Packaging quantities should support efficient customer receiving and line-side handling. Labels or identification records can help connect each shipment to the relevant part number, material specification, production batch, and inspection information. Clear organization reduces the risk of mixing similar components.
Why Choose a Specialized Stamping Die and Part Manufacturer?
Gas tank end stamping parts require a combination of material knowledge, forming expertise, die precision, press capability, and quality discipline. A supplier that focuses on stamping dies and formed metal parts can invest in the equipment, personnel, and process experience needed to manage these requirements.
Suzhou Shuangqisi Mold Equipment Co., Ltd. has approximately 15 years of experience in the mold industry and a technical team of around 60 personnel. Its production capability covers die design, tool manufacturing, stamping, equipment integration, and service support. This structure allows the company to participate in projects from early concept review through production delivery.
The company also serves customers in multiple industrial fields, including servo drives, compressors, and new energy vehicles. This diversified experience provides a foundation for managing different materials, geometries, production volumes, and precision requirements. Its stated business approach emphasizes quality control, cost control, technical reliability, and customer value.
For customers seeking gas tank end stamping parts, these capabilities can provide a more complete sourcing option. Instead of purchasing a component without visibility into the tool behind it, customers can work with a supplier that understands how die construction and production performance are connected.
Inspection Questions Customers Should Ask
Before placing an order, customers should clarify the material grade, thickness, dimensional tolerance, surface requirements, required production capacity, inspection method, and joining process. They should also confirm whether the supplier can provide samples, dimensional reports, process documentation, and technical communication during die development.
It is useful to ask how the supplier controls forming defects, how die maintenance is managed, what press range is available, and whether automation can be incorporated if production volume increases. Customers may also ask about packaging, delivery schedules, spare die components, and support after the tooling enters production.
A clear technical discussion at the beginning helps prevent misunderstandings later. It also enables the supplier to evaluate the project using realistic manufacturing conditions rather than relying only on a theoretical drawing review.
Q&A: Gas Tank End Stamping Parts
What is the primary function of a gas tank end stamping part?
Its primary functions are to close the end of a fuel tank, contribute to sealing, reinforce the tank structure, and provide a dimensionally controlled interface for joining with the tank body and related components.
Which materials can be used?
Common choices include cold-rolled steel, coated steel, stainless steel, and aluminum alloy. The final selection depends on formability, strength, corrosion resistance, fuel-system compatibility, weight targets, and the customer’s technical standard.
Can the parts be customized for different vehicle models?
Yes. The shape, diameter, depth, flange, openings, reinforcing features, material, and tolerance can be developed according to the customer’s drawings and tank assembly requirements.
Why is die precision important?
Die precision affects the part’s dimensions, surface quality, repeatability, and fit with the tank body. Accurate tooling also helps reduce defects, rework, scrap, and problems during downstream welding or assembly.
How are cracks and wrinkles controlled?
Control methods include suitable material selection, correct blank design, appropriate corner radii, stable lubrication, balanced blank-holder force, proper draw bead design, multiple forming stages, and careful die debugging.
What press capacity is required?
The required capacity depends on material type, thickness, part size, forming depth, draw force, and process design. A supplier with presses ranging from 80 tons to 400 tons can evaluate different component requirements and select suitable equipment.
Are aluminum alloy end parts possible?
Yes. Aluminum alloy can be used when low weight and corrosion resistance are important. However, the process must account for springback, surface sensitivity, friction, and alloy-specific forming behavior.
Can the supplier provide tooling and finished parts?
Yes. An integrated stamping supplier can design and manufacture the die, debug the process, and produce the finished stamping parts. This approach helps maintain technical continuity between tooling and production.
Can automation be included in the project?
Automation may be incorporated for loading, transfer, positioning, unloading, inspection, or other production steps. The appropriate level of automation depends on volume, product variety, press layout, labor conditions, and the customer’s investment objectives.
What quality problems should be checked before shipment?
Customers should check dimensions, flange geometry, surface condition, cracks, wrinkles, folds, burrs, holes, deformation, material identification, and packaging condition. Additional functional or leak-related checks may be specified according to the complete tank assembly requirements.
How does an integrated supplier reduce project risk?
When die engineering, stamping production, debugging, and automation are handled within a connected organization, technical communication is more direct. This can reduce interface errors, accelerate problem resolution, and support a more stable transition from sample production to mass production.
What information should be provided for a quotation?
Useful information includes product drawings or three-dimensional data, material and thickness, annual or monthly volume, required tolerance, surface requirements, intended press or line conditions, packaging expectations, inspection standards, and target delivery schedule.
Conclusion
Gas tank end stamping parts are small compared with a complete vehicle, but they perform an important structural and sealing role within the fuel tank assembly. Their performance depends on accurate geometry, suitable material, controlled forming, high-quality tooling, stable production, and careful inspection. Uniform thickness, smooth surfaces, resistance to cracking and deformation, and reliable compatibility with the tank body are essential requirements.
Precision stamping offers an effective way to manufacture these components at consistent quality and competitive production cost. When supported by advanced die-making equipment, suitable punch presses, experienced operators, and systematic debugging, the process can serve a wide range of passenger car and commercial vehicle applications.
Suzhou Shuangqisi Mold Equipment Co., Ltd. combines stamping die design and manufacturing with stamping part production and automation equipment capabilities. Its CNC machining centers, wire cutting machines, grinding equipment, press capacity from 80 tons to 400 tons, technical personnel, and industrial experience support the development of customized automotive stamping solutions. The company’s integrated approach is intended to help customers control quality, improve efficiency, manage costs, and obtain practical tooling and production support from one technical source.
For automotive parts manufacturers and maintenance-related supply organizations, selecting the right supplier is a strategic decision. A reliable supplier should be able to understand the complete application, design a suitable forming process, manufacture accurate tooling, control production quality, and provide responsive technical support. With these capabilities in place, gas tank end stamping parts can contribute to safer, more durable, and more efficient fuel tank assemblies.
References
1. Automotive sheet-metal forming principles, including blank development, drawing, trimming, flanging, and springback control.
2. General engineering practices for cold-rolled steel and aluminum alloy stamping applications.
3. Automotive fuel tank structural design and sealing considerations.
4. Metal forming die design methods for deep drawing and three-dimensional sheet components.
5. Quality inspection practices for stamped automotive components.
6. Manufacturing process planning for stamping dies, press operations, and automated material handling.
7. General corrosion-control principles for automotive fuel-system components.
Product: Gas tank end stamping parts
Previous Post
Long-Stroke Multi-Stage Progressive Dies for Complex Sheet Metal Forming
Next Post
Car Seat Stamping Parts: Precision Metal Components for Safe, Stable, and Efficient Automotive Seat Manufacturing
Our Products.
Start Your Business with an OEM Manufacturer Right Here!

Provide global customers with complete turn-key solutions
through
innovation!
QUICK LINKS
CONTACT INFO.
-
 +86-139 1308 8972
-

-
 No. 118 Yexin Road, Wujiang Economic Development Zone, Suzhou, China
Copyright © Suzhou Shuangqisi Mold Equipment Co., Ltd. All Rights Reserved. Custom Stamping Die Metal Stamping Die Manufacturers
