 English
 Español
 Deutsch
-

Progressive Stamping Die for Connector & Terminal Parts High Speed Progressive Stamping Die Precision Metal Hardware Stamping Tool mold for Connector Terminal Parts Automotive Components
Progressive Stamping Die for Connector & Termi...
-
High Precision Stamping Die Multi Station Hardware Progressive Mold Tooling
Precision Metal Stamping Tool for Automotive &...
-

Long-Stroke Multi-Stage Progressive Die Automatic Strip Feed Progressive Die Long Travel Follow on Stamping Tool for Sheet Metal Hardware Press Moulding
Long-Stroke Multi-Stage Progressive DieOur custom ...
-
Multi-Station Progressive Stamping Die with Carbide Inserts Custom Multi Station Progressive Stamping Die Carbide Insert Metal Stamping Mold Tool for Equipment Appliances Device Hardware
High Speed Metal Stamping Tool for Precise Equipme...
-
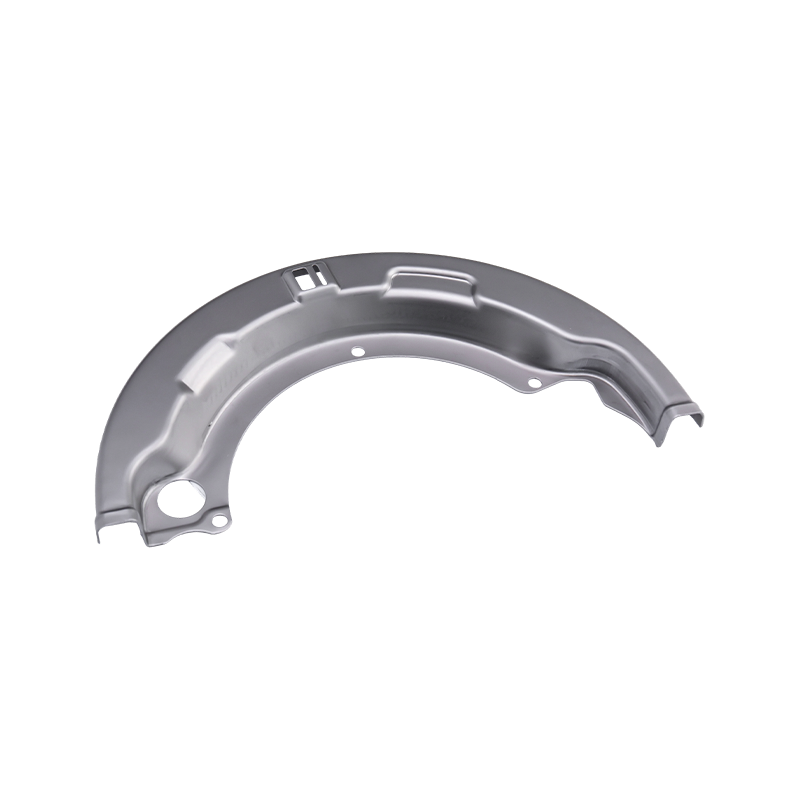
Heavy truck stamping parts
Our Heavy truck stamping parts are precision-manuf...
- E-mail us: [email protected]
- Call us: +86-139 1308 8972

Zhou Mengjie – Technical Sales Specialist
Home / Author / Zhou Mengjie – Technical Sales Specialist / Heavy Truck Stamping Parts: Precision Components for Reliable Commercial Vehicles
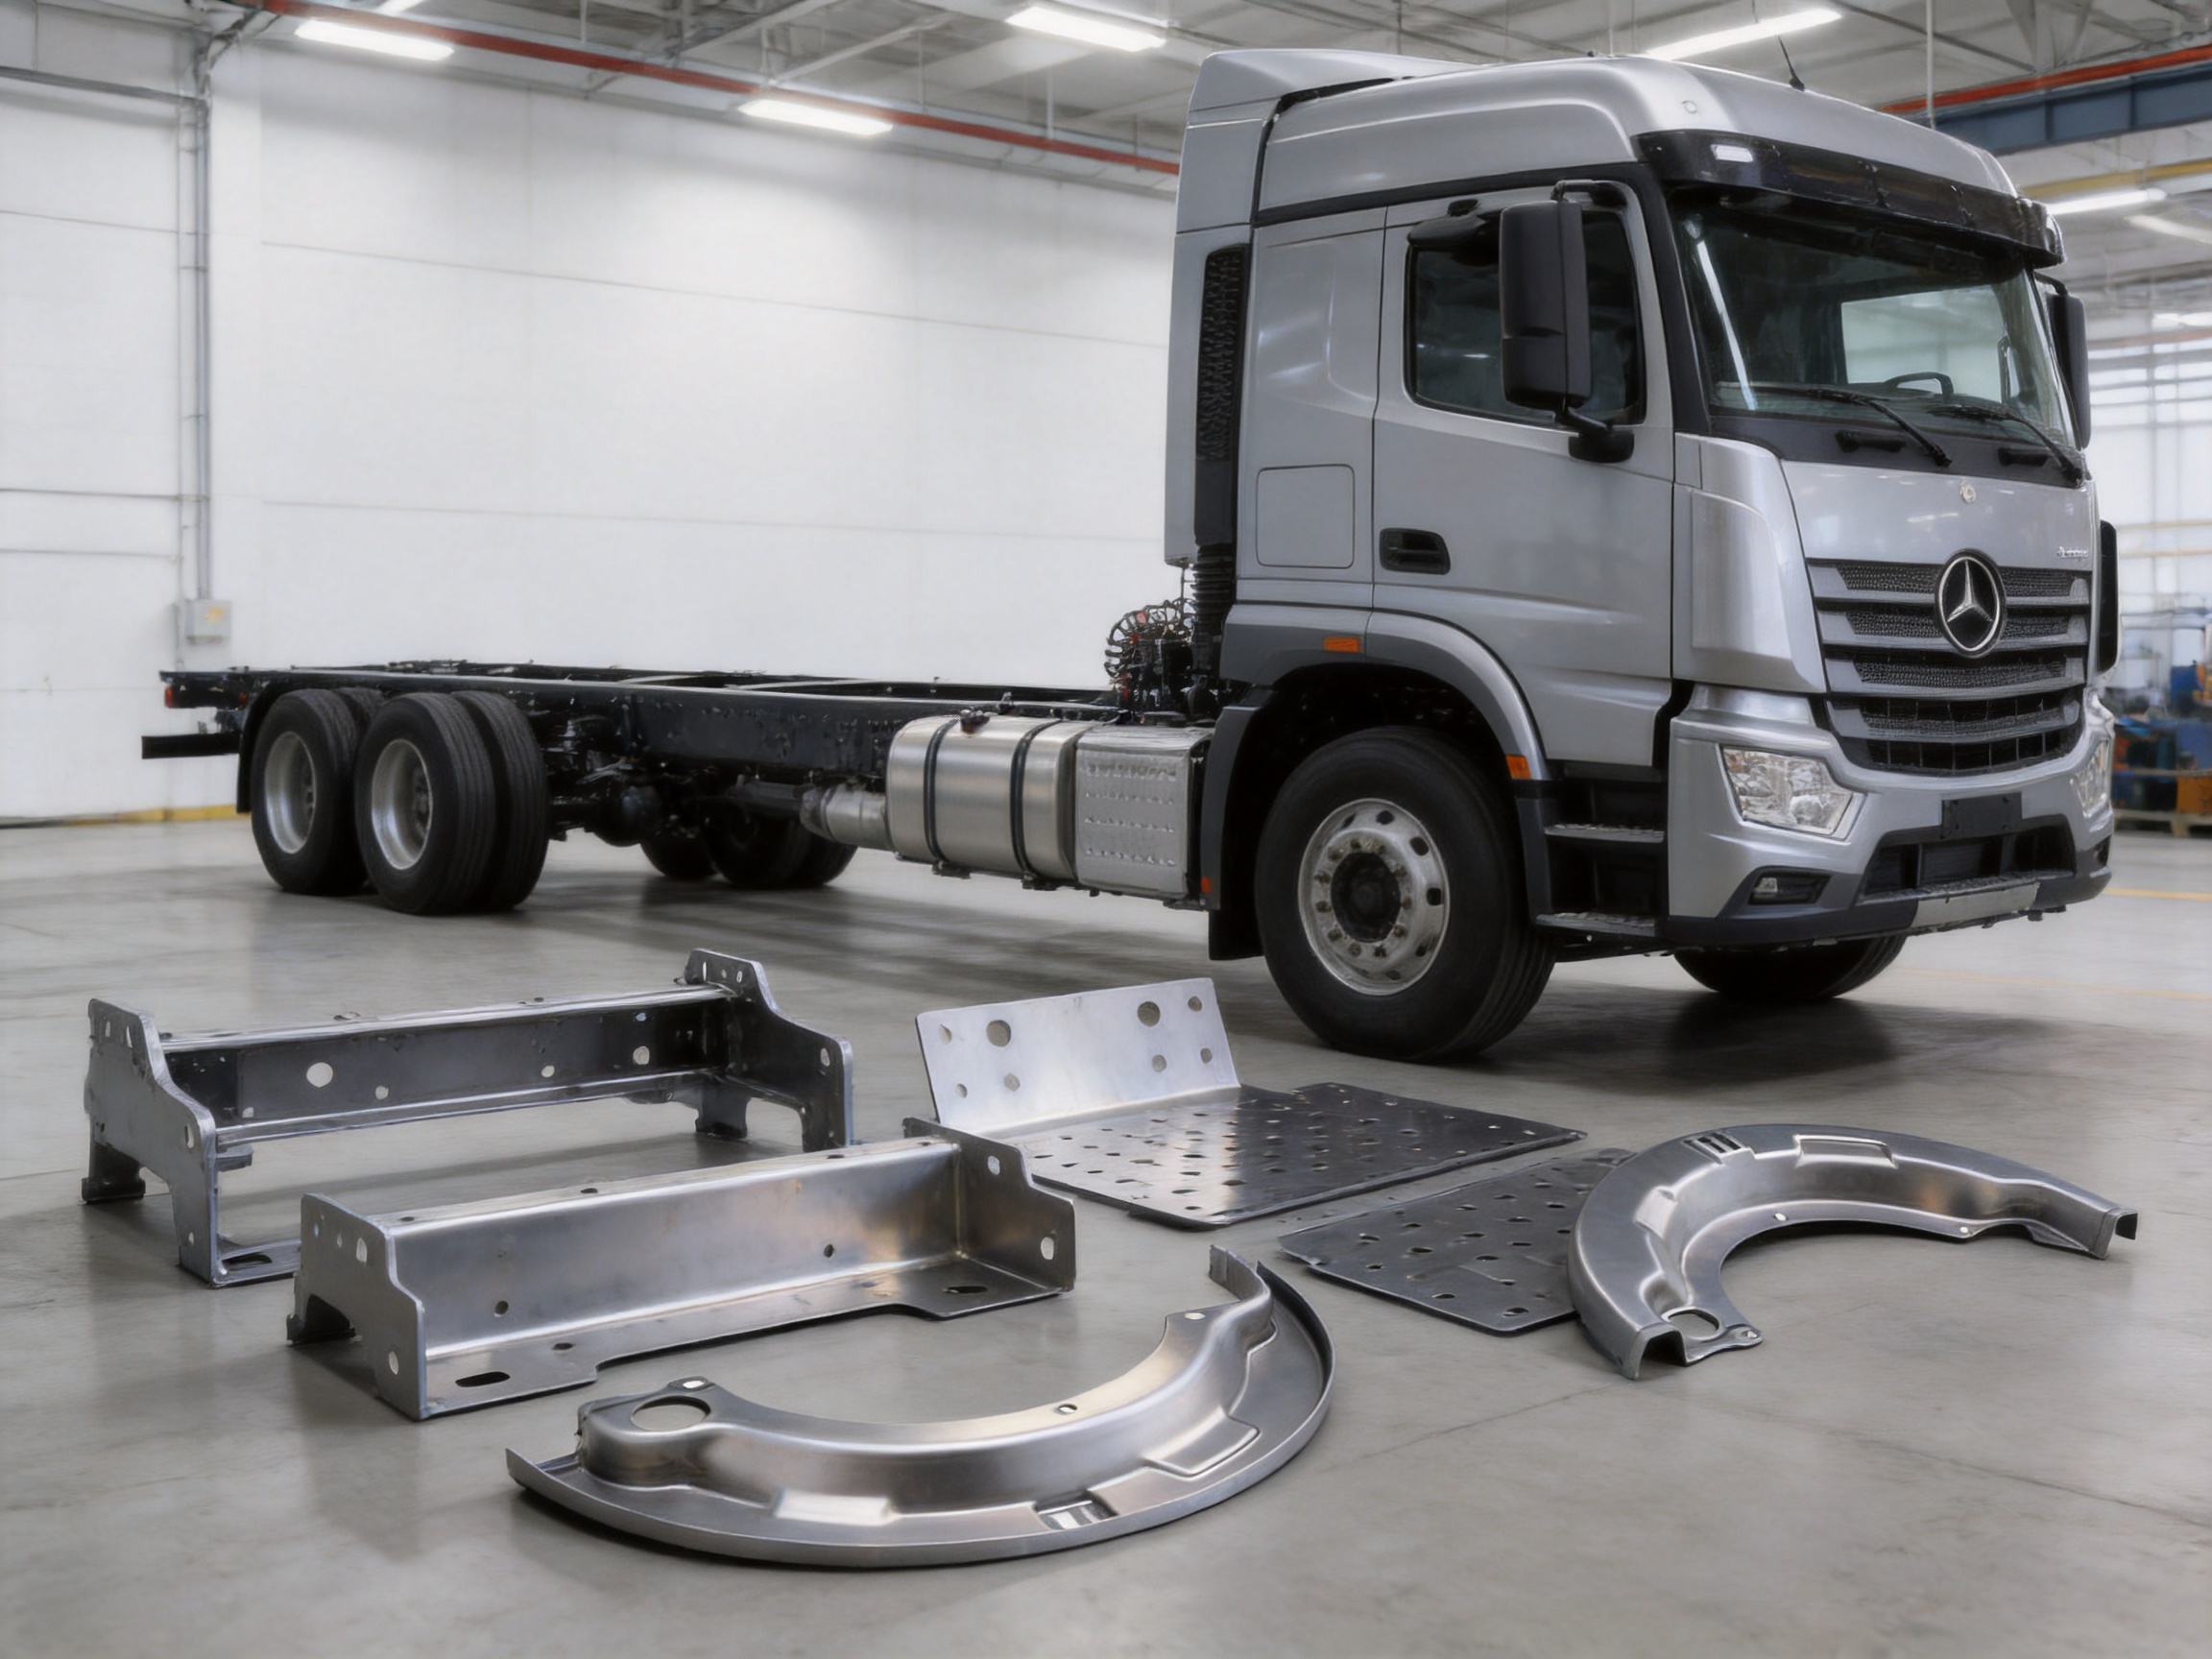
Heavy Truck Stamping Parts: Precision Components for Reliable Commercial Vehicles
2026-10-26
Heavy-duty trucks operate under demanding conditions that place exceptional stress on every structural and functional component. Long-distance transportation, construction work, mining logistics, agricultural distribution, and other commercial applications expose truck systems to heavy loads, continuous vibration, repeated impact, road debris, moisture, temperature fluctuations, and corrosion. Under these conditions, a stamping part is not simply a shaped piece of metal. It is a safety-related and performance-critical component that must maintain its geometry, strength, and connection reliability throughout the service life of the vehicle.
Heavy truck stamping parts are precision-manufactured metal components developed for commercial vehicles and their supporting systems. Typical products include frame brackets, suspension connecting plates, engine mounting supports, reinforcement plates, mounting panels, and other structural or semi-structural components. These parts are produced from high-strength steel plates through carefully controlled cold stamping processes. Their purpose is to provide dependable load transfer, accurate assembly, consistent dimensional performance, and long-term resistance to vibration and environmental exposure.
For truck manufacturers, tier suppliers, fleet operators, repair centers, and aftermarket distributors, the quality of stamped parts directly affects assembly efficiency, maintenance frequency, operating safety, and total ownership cost. A component with inconsistent thickness, poor forming accuracy, burrs, or inadequate corrosion protection can create alignment problems and accelerate wear in surrounding systems. By contrast, a precisely formed and properly inspected stamping part supports stable vehicle performance while simplifying production and maintenance.
Advanced manufacturing capabilities are therefore essential. A qualified supplier must combine product engineering, die design, precision machining, stamping, inspection, troubleshooting, and production support. Suzhou Shuangqisi Mold Equipment Co., Ltd. provides this integrated capability through its experience in stamping dies, hardware parts, and stamping automation equipment. Its production resources include imported wire-cutting machines, CNC machining centers, more than ten grinding machines of different sizes, and 25 punch presses ranging from 80 tons to 400 tons. This equipment base enables the company to develop and manufacture components for varied material thicknesses, geometries, and load requirements.
Heavy truck stamping parts
Content
- 1 What Are Heavy Truck Stamping Parts?
- 2 Core Product Applications
- 3 Key Advantages of Precision Heavy Truck Stamping Parts
- 4 Manufacturing Process for Heavy Truck Stamping Parts
- 5 Quality Control and Performance Verification
- 6 Comparison with Alternative Manufacturing Methods
- 7 Integrated Manufacturing Strengths
- 8 How Precision Engineering Reduces Total Cost
- 9 Customization and Project Development
- 10 Selection Guide for Buyers
- 11 Applications in Original Equipment and Aftermarket Supply
- 12 Maintenance Considerations for Stamped Components
- 13 Environmental and Operational Considerations
- 14 Frequently Asked Questions
- 14.1 Q1: What materials are commonly used for heavy truck stamping parts?
- 14.2 Q2: Which truck components can be manufactured by stamping?
- 14.3 Q3: Why is stamping suitable for heavy-duty vehicle parts?
- 14.4 Q4: Can stamped parts be customized for a specific truck model?
- 14.5 Q5: How does high-strength steel affect the stamping process?
- 14.6 Q6: What inspections are important for heavy truck stamping parts?
- 14.7 Q7: What press capacity is available for production?
- 14.8 Q8: Can the supplier provide stamping dies as well as finished parts?
- 14.9 Q9: Is stamping automation available?
- 14.10 Q10: How can a customer begin a heavy truck stamping project?
- 15 Conclusion
- 16 References
- 17 Product: Heavy truck stamping parts
What Are Heavy Truck Stamping Parts?
Heavy truck stamping parts are components formed from metal sheet or plate by applying controlled pressure through a stamping die. Depending on the design, the manufacturing process may include blanking, piercing, bending, forming, drawing, embossing, flanging, or a combination of several operations. The result is a repeatable three-dimensional part with a defined shape, accurate mounting points, and consistent structural characteristics.
Unlike general-purpose sheet-metal products, truck stamping parts must be engineered around the operating conditions of commercial vehicles. A frame bracket may need to transmit a substantial load between the chassis and an attached system. A suspension connecting plate must tolerate cyclic forces and repeated vibration. An engine mounting support must help maintain alignment while absorbing dynamic loads generated by the powertrain and road movement. Each application requires a suitable material grade, thickness, forming radius, hole arrangement, and surface treatment.
Cold stamping is particularly suitable for high-volume production because it can provide stable dimensions and efficient material utilization. Once the die and process parameters have been validated, the same geometry can be reproduced across large production runs with limited variation. This consistency is valuable for original equipment manufacturing, where each part must fit accurately into a defined assembly, as well as for aftermarket applications requiring compatibility with existing truck models.
High-strength steel is commonly selected for heavy-duty components because it offers a useful balance of strength, stiffness, durability, availability, and cost. The appropriate steel grade depends on the function of the part and the requirements of the vehicle system. Material selection must be coordinated with forming capability because higher-strength materials can require greater forming force, carefully designed radii, controlled springback compensation, and more precise process management.
Core Product Applications
Frame Brackets
Frame brackets connect or support components mounted to the truck chassis. They may be used around suspension assemblies, fuel systems, exhaust systems, cab structures, battery compartments, cross members, or other vehicle modules. Since the chassis is exposed to bending and torsional loads, brackets must maintain their shape and fastening accuracy under repeated stress.
Precision stamping helps produce uniform bracket walls, consistent mounting holes, and clean bends. Accurate geometry reduces the need for manual adjustment during vehicle assembly. It also helps prevent uneven load transfer, misalignment, and localized stress concentration. When the bracket is designed with suitable reinforcement features, stamped construction can provide high stiffness without requiring an unnecessarily heavy component.
Suspension Connecting Plates
Suspension connecting plates serve as load-transfer elements between suspension-related components. They are exposed to road shock, acceleration and braking forces, cornering loads, and continuous vibration. Their performance depends on material strength, hole position, flatness, edge condition, and resistance to fatigue-related deformation.
For these parts, dimensional accuracy is particularly important. Even a small deviation in a mounting location can influence the position of connected components and create assembly stress. A controlled stamping process ensures that the plate profile and fastening points remain consistent. Proper die design also helps minimize distortion around holes, corners, and formed sections where stress may be concentrated.
Engine Mounting Supports
Engine mounting supports must maintain the relative position of the engine and chassis while managing vibration and dynamic loads. They may include formed sections, reinforcing ribs, flanges, and precision mounting holes. The support must be strong enough for the engine mass and operating forces while also meeting the installation space and interface requirements of the vehicle.
Stamped construction allows engineers to incorporate bends and reinforcing features into a single component. This can reduce the number of separate pieces and fastening operations compared with a more complicated fabricated assembly. Consistent forming also supports repeatable engine installation and helps ensure that connected components remain within their intended alignment range.
Additional Structural and Hardware Components
Beyond the core product categories, heavy truck stamping programs may include reinforcement plates, support tabs, chassis covers, mounting panels, brackets, clamps, protective components, and customized hardware parts. The exact product range depends on customer drawings, vehicle platform requirements, production volume, and material specifications.
Because a stamping supplier with die-making capability can control both the forming tool and the production process, it can respond more effectively to customized components. Design changes, hole adjustments, flange revisions, and forming improvements can be coordinated within the same technical workflow rather than being divided between unrelated suppliers.
Key Advantages of Precision Heavy Truck Stamping Parts
High Structural Reliability
Heavy truck components must withstand demanding operating conditions over extended periods. Properly selected high-strength steel provides a strong foundation for load-bearing applications, while accurate forming preserves the intended geometry of the design. A well-manufactured stamping part distributes forces through its formed surfaces, flanges, ribs, and mounting areas in a predictable manner.
Structural reliability also depends on process stability. If one production batch contains variations in thickness, bend angle, or hole location, the resulting assembly may behave inconsistently. Controlled stamping parameters, suitable die clearance, and regular inspection help maintain repeatable results from the first part to the last part in a production run.
Consistent Dimensions and Interchangeability
Commercial vehicle production depends on the ability to install components efficiently and consistently. Heavy truck stamping parts are produced according to defined drawings, tolerances, and inspection requirements. Accurate dimensions support interchangeability between parts from the same production program and reduce the need for fitting, rework, or manual correction.
Consistency is also important for aftermarket service providers. Replacement parts need to match the mounting pattern and overall geometry of the original truck assembly. When the component is manufactured using a validated die, its shape can be reproduced more reliably than parts produced through uncontrolled manual fabrication.
Efficient Material Use
Stamping can use sheet and plate material efficiently when the blank layout and forming sequence are properly engineered. Efficient nesting and controlled blank dimensions help reduce scrap, especially in repeated production. Material utilization contributes to cost control and supports a more responsible manufacturing approach.
Material efficiency does not mean reducing thickness without considering performance. For heavy truck applications, the correct balance must be maintained between strength, stiffness, weight, manufacturability, and cost. An experienced manufacturer can evaluate the forming process and recommend practical solutions that preserve functional requirements while avoiding unnecessary material consumption.
Stable Production for Volume Orders
Once the die and process have been verified, stamping is suitable for repeat production. This is an advantage for vehicle manufacturers and parts distributors that require stable deliveries over a long program period. Repeatable production also makes it easier to establish inspection standards, packaging requirements, and batch traceability procedures.
The use of punch presses from 80 tons to 400 tons provides production flexibility for different part sizes and forming requirements. Smaller components may be processed on lower-capacity equipment, while larger or more demanding parts can be assigned to higher-capacity presses. Matching press capacity to part requirements supports production efficiency and reduces unnecessary equipment loading.
Clean Edges and Improved Assembly Quality
Edge condition is an important aspect of stamped parts. Excessive burrs, sharp edges, or incomplete piercing can interfere with assembly and create handling risks. Proper die maintenance and cutting clearance management help produce cleaner edges. Secondary deburring or finishing operations may be applied when the application requires an especially controlled edge condition.
Clean and consistent edges also support the performance of coatings and corrosion-protection treatments. Uneven edges can become vulnerable areas where coating coverage is reduced or where corrosion may begin more easily. For that reason, edge quality should be evaluated as part of the complete product performance rather than as a purely cosmetic characteristic.
Resistance to Vibration and Impact
Truck systems are exposed to continuous vibration and occasional impact. Stamped components must retain their shape under cyclic loading and should not develop premature cracks, loosened interfaces, or permanent deformation under normal operating conditions. Part geometry, steel grade, forming radius, and fastening design all influence this performance.
Reinforcing ribs, formed flanges, and carefully positioned bends can increase stiffness without requiring a solid block of material. The die must form these features accurately and avoid excessive thinning or damage at critical points. Inspection of formed areas is therefore essential, particularly for parts used in suspension and powertrain support systems.
Corrosion-Protection Potential
Heavy trucks may operate in rain, snow, mud, salt, dust, and industrial environments. Corrosion resistance is especially important for chassis components and parts located beneath the vehicle, where exposure to water and road contaminants is frequent. Stamped steel parts can be integrated into suitable cleaning, coating, plating, painting, or other anti-corrosion processes according to customer requirements.
A smooth and uniform surface supports more consistent treatment. Inspection may include visual checks, coating evaluation, and other customer-defined tests. The selected protection method should consider the truck’s operating environment, assembly contact points, expected service life, and maintenance practices.
Manufacturing Process for Heavy Truck Stamping Parts
1. Technical Review and Requirement Confirmation
Manufacturing begins with a review of the product drawing, three-dimensional model, material specification, annual demand, tolerance requirements, and intended application. Engineers examine the load-bearing function of the component, the position of holes and bends, the available installation space, and the potential forming risks.
At this stage, the supplier should clarify the steel grade, material thickness, surface requirements, critical dimensions, inspection standards, packaging method, and delivery schedule. Early communication helps identify design features that may complicate forming or increase the risk of cracking, springback, distortion, or tool wear.
For customized components, the engineering team may evaluate whether the existing design is suitable for stamping or whether a modified structure would improve manufacturability. The objective is not to change the functional intent of the part, but to develop a practical production route that supports quality, cost, and delivery requirements.
2. Stamping Die Design
The stamping die determines the final shape and much of the dimensional performance of the part. Die design must account for blank size, forming direction, material flow, punch and die clearance, bending sequence, springback, ejection, feeding, and operator safety.
Complex parts may require multiple operations. A typical sequence can include blanking the initial profile, piercing mounting holes, bending flanges, forming ribs, and calibrating critical surfaces. The order of operations must be selected carefully. If holes are pierced before excessive deformation occurs, their position may change during later forming. In other cases, pre-forming and final calibration may be necessary to achieve the required accuracy.
Die design also affects tool life. Excessive pressure, poor clearance, sharp transitions, and inadequate lubrication can accelerate wear or damage the material. A well-designed tool balances production speed, part quality, maintenance requirements, and operating safety.
3. Precision Die Manufacturing
After the design is approved, the die components are manufactured using precision equipment. Imported wire-cutting machines support the production of accurate profiles and intricate features. CNC machining centers are used for complex die blocks, bases, inserts, and other components requiring controlled geometry. Grinding machines help achieve precise flatness, surface finish, and dimensional accuracy on critical die surfaces.
The company’s equipment configuration includes more than ten grinding machines of various sizes. This range allows different die components to be processed according to their dimensions and accuracy requirements. The availability of multiple machine types also supports a more integrated production schedule and reduces dependence on external processing for key operations.
Die assembly is followed by dimensional verification and trial preparation. Proper alignment between punch, die, guide components, and forming surfaces is essential. Small errors in tool alignment can lead to burrs, uneven forming, accelerated wear, or inconsistent part dimensions.
4. Material Preparation
High-strength steel plates are prepared according to the approved material specification. Incoming material should be checked for grade, thickness, surface condition, flatness, and visible defects. Material identification helps prevent incorrect steel from entering production.
Flatness is important because significant coil or plate distortion can affect feeding, blank positioning, and forming accuracy. The blank size must also be controlled. An undersized blank may fail to fill the die cavity, while an oversized blank can increase waste or cause unwanted wrinkles and interference.
5. Trial Stamping and Process Debugging
Before regular production begins, the die is tested through trial stamping. Operators and debugging personnel examine the trial parts for shape, flatness, hole position, bend angle, edge quality, surface marks, and visible cracks. Process parameters are adjusted when necessary.
Debugging may involve changes to die clearance, blank-holder pressure, forming sequence, lubrication, feeding position, or calibration operations. Springback is a common consideration when forming high-strength steel. The die may need compensation features so that the released part reaches the specified final geometry.
Experienced operators are valuable during this stage because many quality issues are influenced by the interaction between material behavior, tool condition, machine operation, and process sequence. Practical experience helps identify the cause of a defect rather than merely correcting its appearance.
6. Production Stamping
After the trial process is approved, production stamping is carried out on a suitable punch press. The company operates 25 punch presses with capacities ranging from 80 tons to 400 tons. This press range supports a variety of truck stamping parts, from smaller brackets to larger and more demanding structural components.
During production, operators monitor feeding, die condition, lubrication, press behavior, and part appearance. Regular checks help detect burr growth, tool wear, material movement, or changes in forming quality before they affect a large quantity of parts. Process records can be maintained according to customer requirements.
7. Finishing and Surface Treatment
Depending on the specification, stamped parts may require deburring, cleaning, straightening, surface treatment, painting, plating, or another anti-corrosion process. The finishing route is selected according to the part’s application, assembly interface, and environmental exposure.
Flatness and edge condition are reviewed after forming and finishing. If a part includes large flat areas or thin sections, stress release during stamping may cause distortion. Controlled calibration or straightening can help meet final requirements, provided that the operation does not introduce additional damage or residual stress beyond acceptable limits.
8. Final Inspection and Packaging
Final inspection focuses on the characteristics most relevant to part performance. These may include hardness, flatness, dimensional accuracy, hole position, thickness, surface condition, edge quality, and anti-corrosion performance. Inspection methods are selected according to the product drawing and customer quality plan.
Packaging must protect the parts from impact, scratching, moisture, and deformation during storage and transportation. Heavy parts may require reinforced containers or separators. Smaller parts can be packed in counted batches to simplify receiving and production-line handling. Clear identification supports traceability and helps customers manage inventory efficiently.
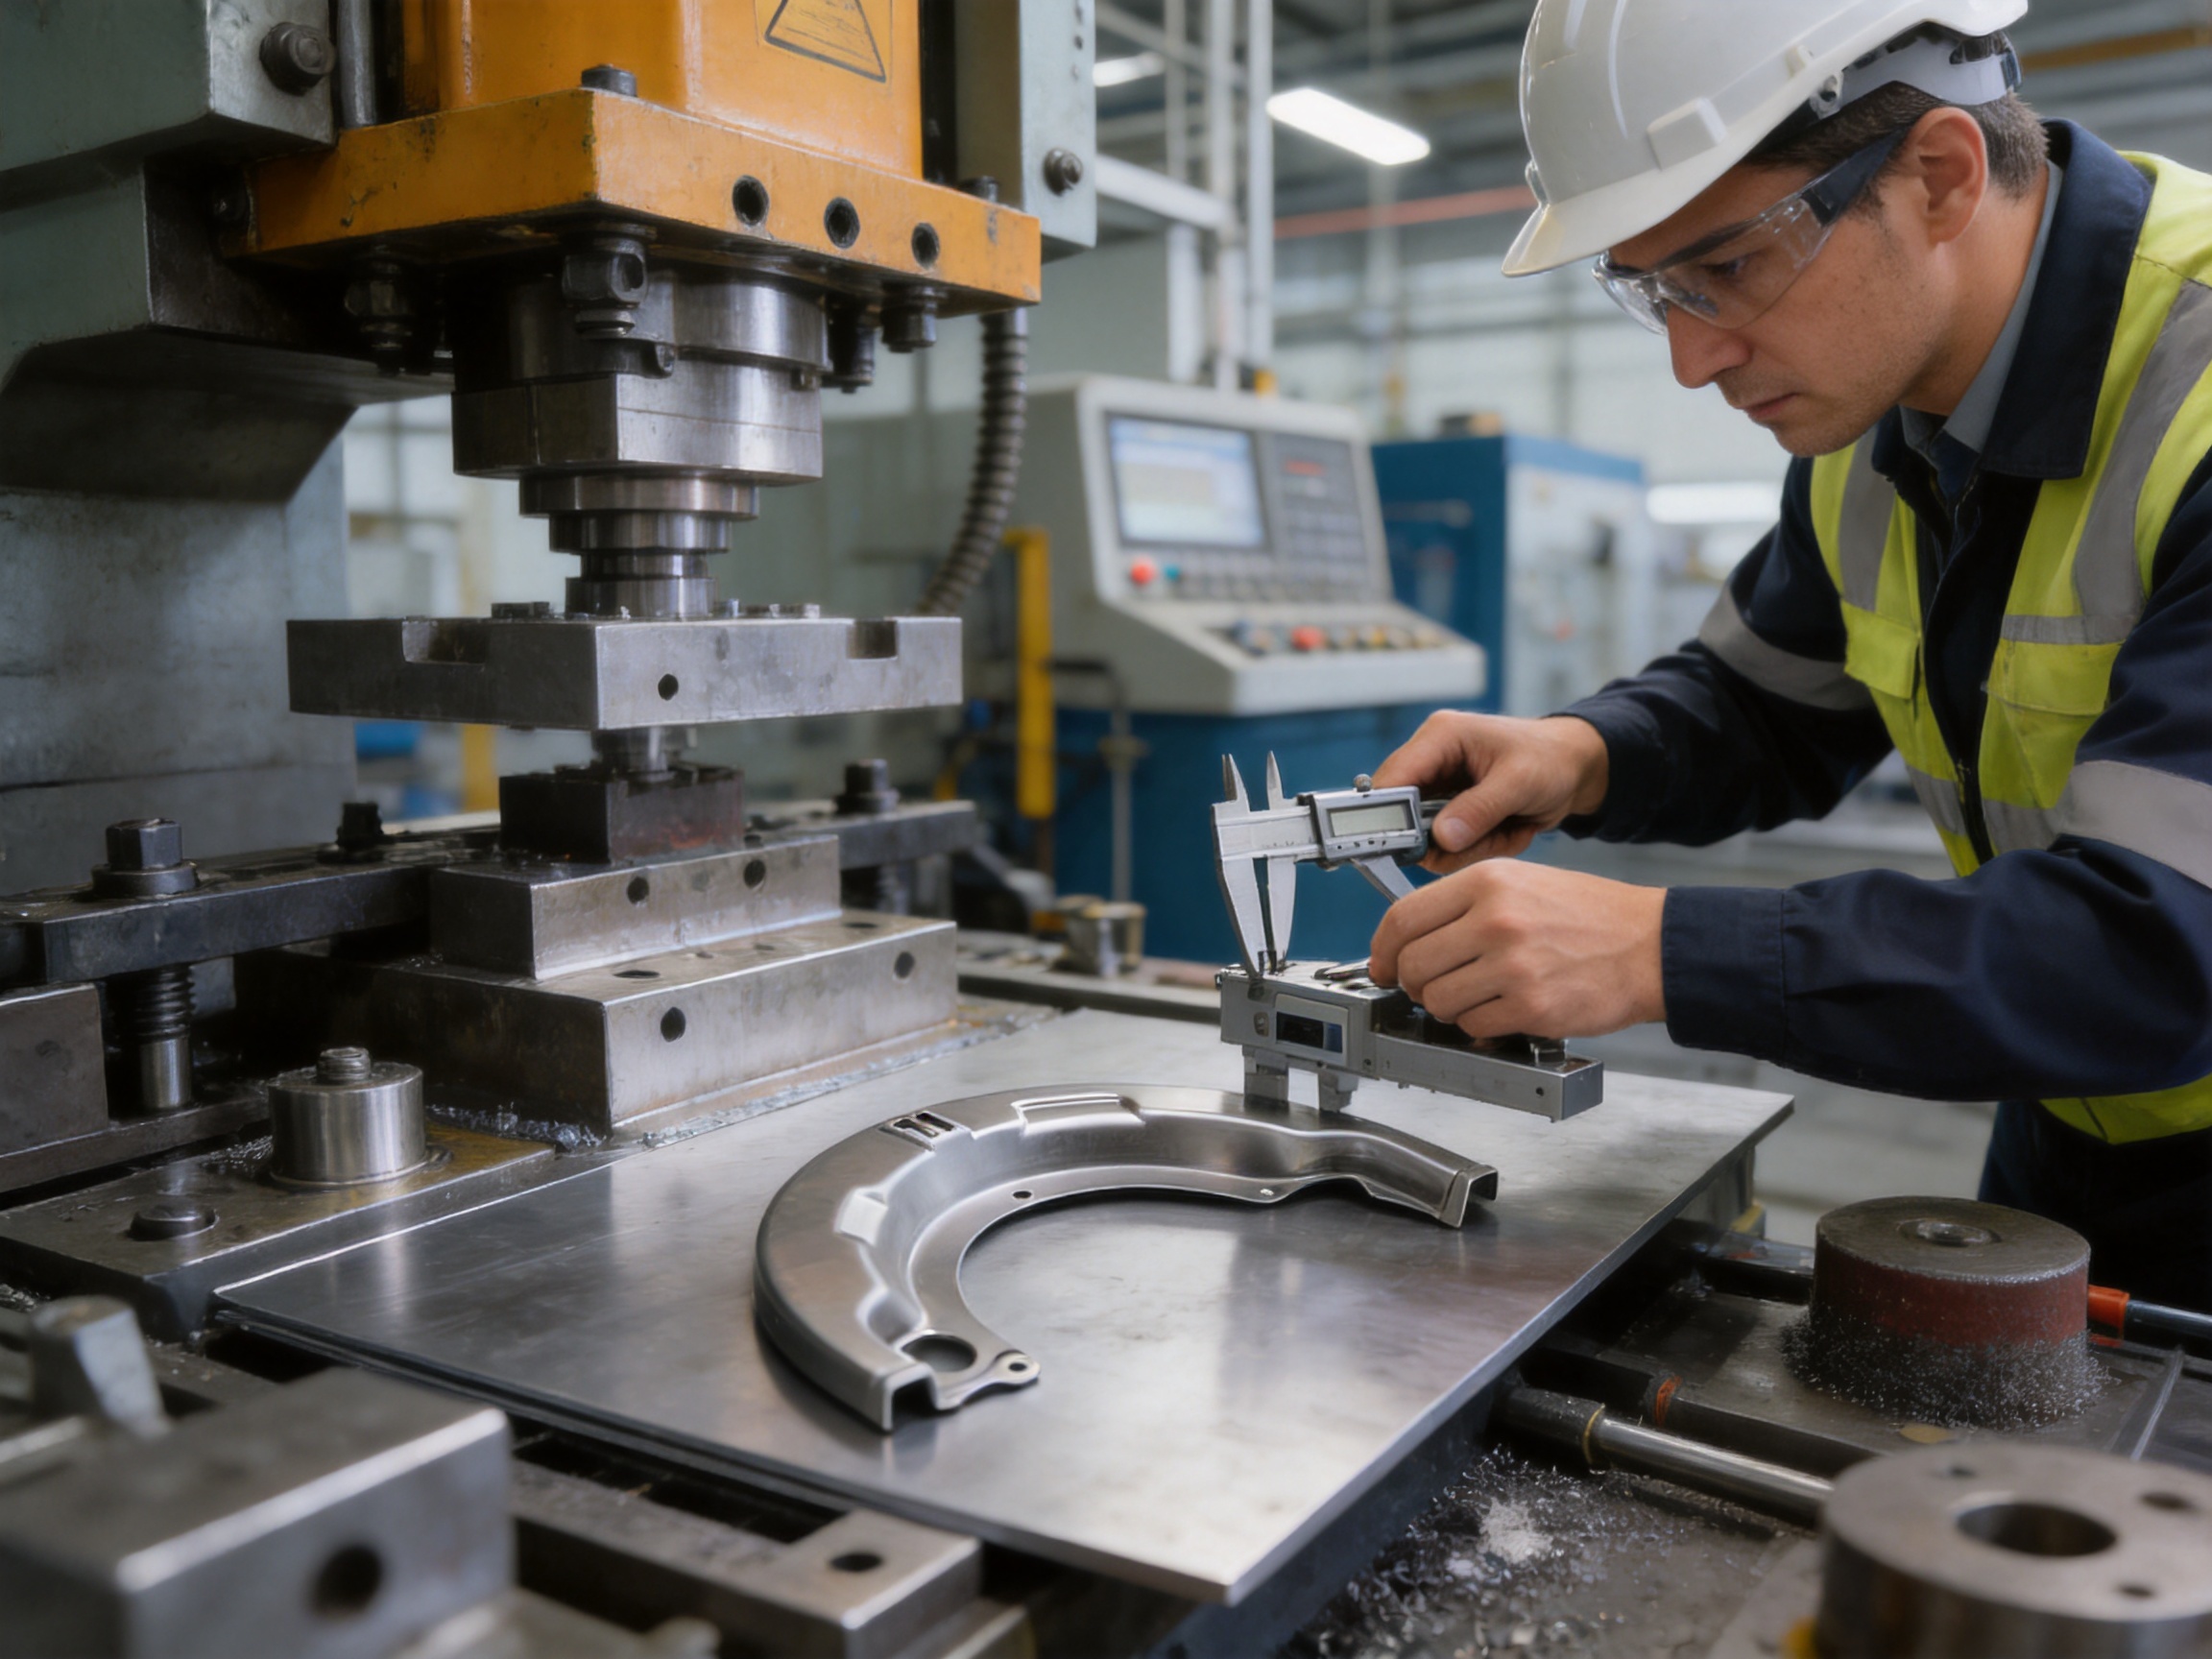
Quality Control and Performance Verification
Quality control for heavy truck stamping parts should begin before the first production stroke. It should continue through material receiving, die manufacturing, trial forming, mass production, finishing, inspection, and shipment. A complete quality system is more effective than relying solely on final inspection because many defects can be prevented through early process control.
Hardness and Material Verification
Hardness inspection provides information about material condition and consistency. It can help confirm that the supplied steel is within the intended range and that no unexpected variation has entered production. Hardness results should be interpreted according to the specified material standard and application requirements.
Flatness and Dimensional Accuracy
Flatness is important for mounting plates, brackets, and other parts that contact a chassis or adjacent assembly. Poor flatness can create gaps, uneven fastening pressure, or alignment problems. Dimensional inspection may include overall length and width, bend angles, hole diameter, hole-to-edge distance, center-to-center spacing, and critical formed profiles.
Inspection tools may include calipers, micrometers, height gauges, gauges, coordinate measurement equipment, and dedicated checking fixtures. The appropriate method depends on the tolerance and geometry of the part. A dedicated fixture can make repeated inspection faster and more consistent for high-volume components.
Surface and Edge Inspection
Visual inspection helps identify scratches, dents, cracks, wrinkles, die marks, incomplete forming, and excessive burrs. Critical formed areas should be examined closely because surface damage can become a starting point for fatigue or corrosion. Edge inspection is also important for assembly safety and coating consistency.
Anti-Corrosion Performance
For components used beneath a truck or in exposed environments, anti-corrosion performance must be considered during product development. The inspection plan may include coating thickness, adhesion, appearance, salt-spray testing, humidity exposure, or other customer-specified methods. The exact requirement should be established according to the part’s environment and intended service life.
Process Documentation
Process documentation provides a reference for repeat orders and supports communication between the manufacturer and customer. Useful documents may include material certificates, inspection reports, die-trial records, dimensional reports, process instructions, and nonconformance records. Clear documentation improves the ability to investigate issues and maintain consistent production over time.
Comparison with Alternative Manufacturing Methods
| Evaluation factor | Precision stamping | Manual fabrication | Machined solid component | Cast component |
|---|---|---|---|---|
| Production consistency | High after die validation | Dependent on operator skill | Generally high but process time may be longer | Dependent on mold and casting control |
| Suitability for sheet or plate parts | Excellent | Good for prototypes and low volume | Usually less efficient | Limited by casting design |
| High-volume efficiency | Very strong | Low to moderate | Moderate to low for large quantities | Moderate to strong after tooling investment |
| Dimensional repeatability | High with a stable die and process | Variable | High | Moderate to high depending on process |
| Material utilization | Efficient when blank layout is optimized | Variable | Lower when machining from solid stock | Potentially efficient but dependent on casting design |
| Part weight optimization | Good through formed ribs and flanges | Good but may require multiple pieces | Often limited by starting stock | Good design flexibility |
| Typical application | Brackets, plates, supports, and repeat-production hardware | Prototype work, repair, and low-volume customization | Complex solid or highly precise components | Selected housings and large shaped components |
Manual fabrication can be useful during prototyping, repair, and low-volume production. However, welded or manually bent parts may show greater variation in dimensions, heat-affected areas, and surface condition. They can also require more labor for trimming, drilling, fitting, and inspection.
Machining provides excellent precision for certain solid or complex components, but removing material from a larger block can be slower and less economical for thin plate brackets. It may also generate more material waste. Casting offers design flexibility for selected shapes, but it involves different tooling, material, and defect-control considerations. For high-volume sheet and plate components, stamping often provides a practical balance of strength, efficiency, repeatability, and cost.
Integrated Manufacturing Strengths
Die Design and Part Production Under One Technical System
One of the strongest advantages of an integrated supplier is the close relationship between die manufacturing and part production. The same organization can evaluate how a tool design affects the finished part, how a material behaves during trial stamping, and how a process adjustment influences production stability. This shortens technical communication and can make problem-solving more direct.
For customers, integrated manufacturing can reduce the risk of unclear responsibility between a die supplier and a stamping supplier. Tool modifications, process improvements, and production changes can be discussed through one coordinated channel. This is particularly valuable when a new heavy truck part requires multiple rounds of trial and refinement.
Broad Equipment Coverage
The combination of wire-cutting machines, CNC machining centers, grinding machines, and punch presses allows the company to manage many stages of the manufacturing process. Different equipment types support different technical needs, from the detailed machining of die components to the high-force forming of truck brackets and supports.
The 80-ton to 400-ton press range provides flexibility for part sizes and forming loads. Equipment selection can be matched to the part rather than forcing every project onto a single machine. Proper machine selection improves production stability and helps protect both the tooling and the material.
Experienced Technical and Production Personnel
Equipment alone does not guarantee a reliable product. Die designers, machinists, press operators, inspectors, and debugging personnel must understand how their work affects the next stage of production. The company has a technical team of approximately 60 staff members, supported by senior operators and experienced debugging personnel.
Practical knowledge is especially important for heavy truck components because these parts often combine structural requirements with tight assembly interfaces. Experienced staff can recognize early signs of springback, uneven material flow, tool wear, or developing burrs. Their input can help prevent small process issues from becoming large production problems.
Experience Across Industrial Applications
The company has approximately 15 years of experience in the mold industry and serves customers in areas including servo drives, compressors, and new energy vehicles. Experience across these sectors contributes to a broader understanding of precision stamping, functional hardware, production tooling, and quality control.
Although each heavy truck component has its own requirements, the engineering principles of accurate die design, stable material flow, controlled forming, and repeatable inspection apply across many industrial products. Cross-industry experience can therefore support the development of practical solutions for new truck stamping applications.
Stamping Automation Capability
In addition to stamping dies and hardware parts, the company is connected with stamping automation equipment through Suzhou Keshuang Intelligent Technology Co., Ltd., established in 2016. This capability supports customers that want to improve feeding, transfer, handling, production consistency, or labor efficiency in stamping operations.
Automation can be considered according to production volume, part geometry, press arrangement, safety requirements, and process sequence. For customers seeking a turnkey solution, the combination of die manufacturing and stamping automation knowledge can simplify the transition from tool development to production-line implementation.
How Precision Engineering Reduces Total Cost
The purchase price of a stamped part is only one element of its total cost. A low-priced component that requires rework, causes assembly delays, or fails prematurely may create greater expense over its service life. For heavy truck applications, total cost should include tooling, production, inspection, installation, maintenance, downtime, replacement, and warranty considerations.
Accurate stamped parts can reduce assembly labor because mounting holes and formed surfaces are more consistent. Stable dimensions also reduce sorting and adjustment work. Clean edges can minimize handling risks and additional finishing. Proper material selection and corrosion protection can extend service life and reduce replacement frequency.
Tool quality also has a long-term effect. A durable, accurately aligned die can support repeated production with predictable maintenance requirements. Although the initial die investment is important, it should be evaluated alongside expected production volume and the cost of inconsistent parts. For high-volume truck programs, a reliable tool often produces better economic results over the complete program lifecycle.
Customization and Project Development
Heavy truck manufacturers and aftermarket customers may require parts that differ in dimensions, material thickness, hole patterns, surface treatment, or packaging. Customization should begin with complete technical information, including drawings, samples, three-dimensional files, material requirements, annual demand, and target application.
A practical project workflow normally includes design review, manufacturability assessment, quotation, die design, tool manufacturing, trial stamping, sample approval, production planning, and delivery. The timing of each stage depends on part complexity, material availability, tool structure, inspection requirements, and customer approval procedures.
When customers provide an existing sample rather than a complete drawing, the supplier may need to inspect the sample, measure key features, and clarify the performance requirements before developing the tooling. Reverse engineering should be performed carefully because the visible geometry does not always reveal material grade, internal stress, load direction, or original forming sequence.
Design changes are easier to manage when communication is established early. A change to a hole location, flange height, bend radius, or material thickness may affect the entire die structure. Prompt confirmation helps avoid unnecessary tooling modifications and protects the project schedule.
Selection Guide for Buyers
When selecting a supplier for heavy truck stamping parts, buyers should evaluate more than equipment lists. The supplier should be able to explain how it controls material quality, die accuracy, trial production, dimensional inspection, surface protection, and delivery consistency.
Important questions include:
Can the supplier manufacture or manage the stamping die internally?
Does the press capacity match the size and forming force of the part?
Can the supplier work with high-strength steel and control springback?
Are hardness, flatness, dimensional accuracy, and anti-corrosion performance inspected?
Can the supplier support prototypes, small batches, and repeat production?
Are engineering changes handled through a documented approval process?
Does the supplier have experienced debugging and production personnel?
Can it provide automation or production-line support when required?
Is packaging designed to prevent deformation and corrosion during transportation?
A supplier that can answer these questions clearly is more likely to provide stable long-term support. Buyers should also request representative samples, inspection records, production references, and an explanation of the proposed manufacturing route for critical components.
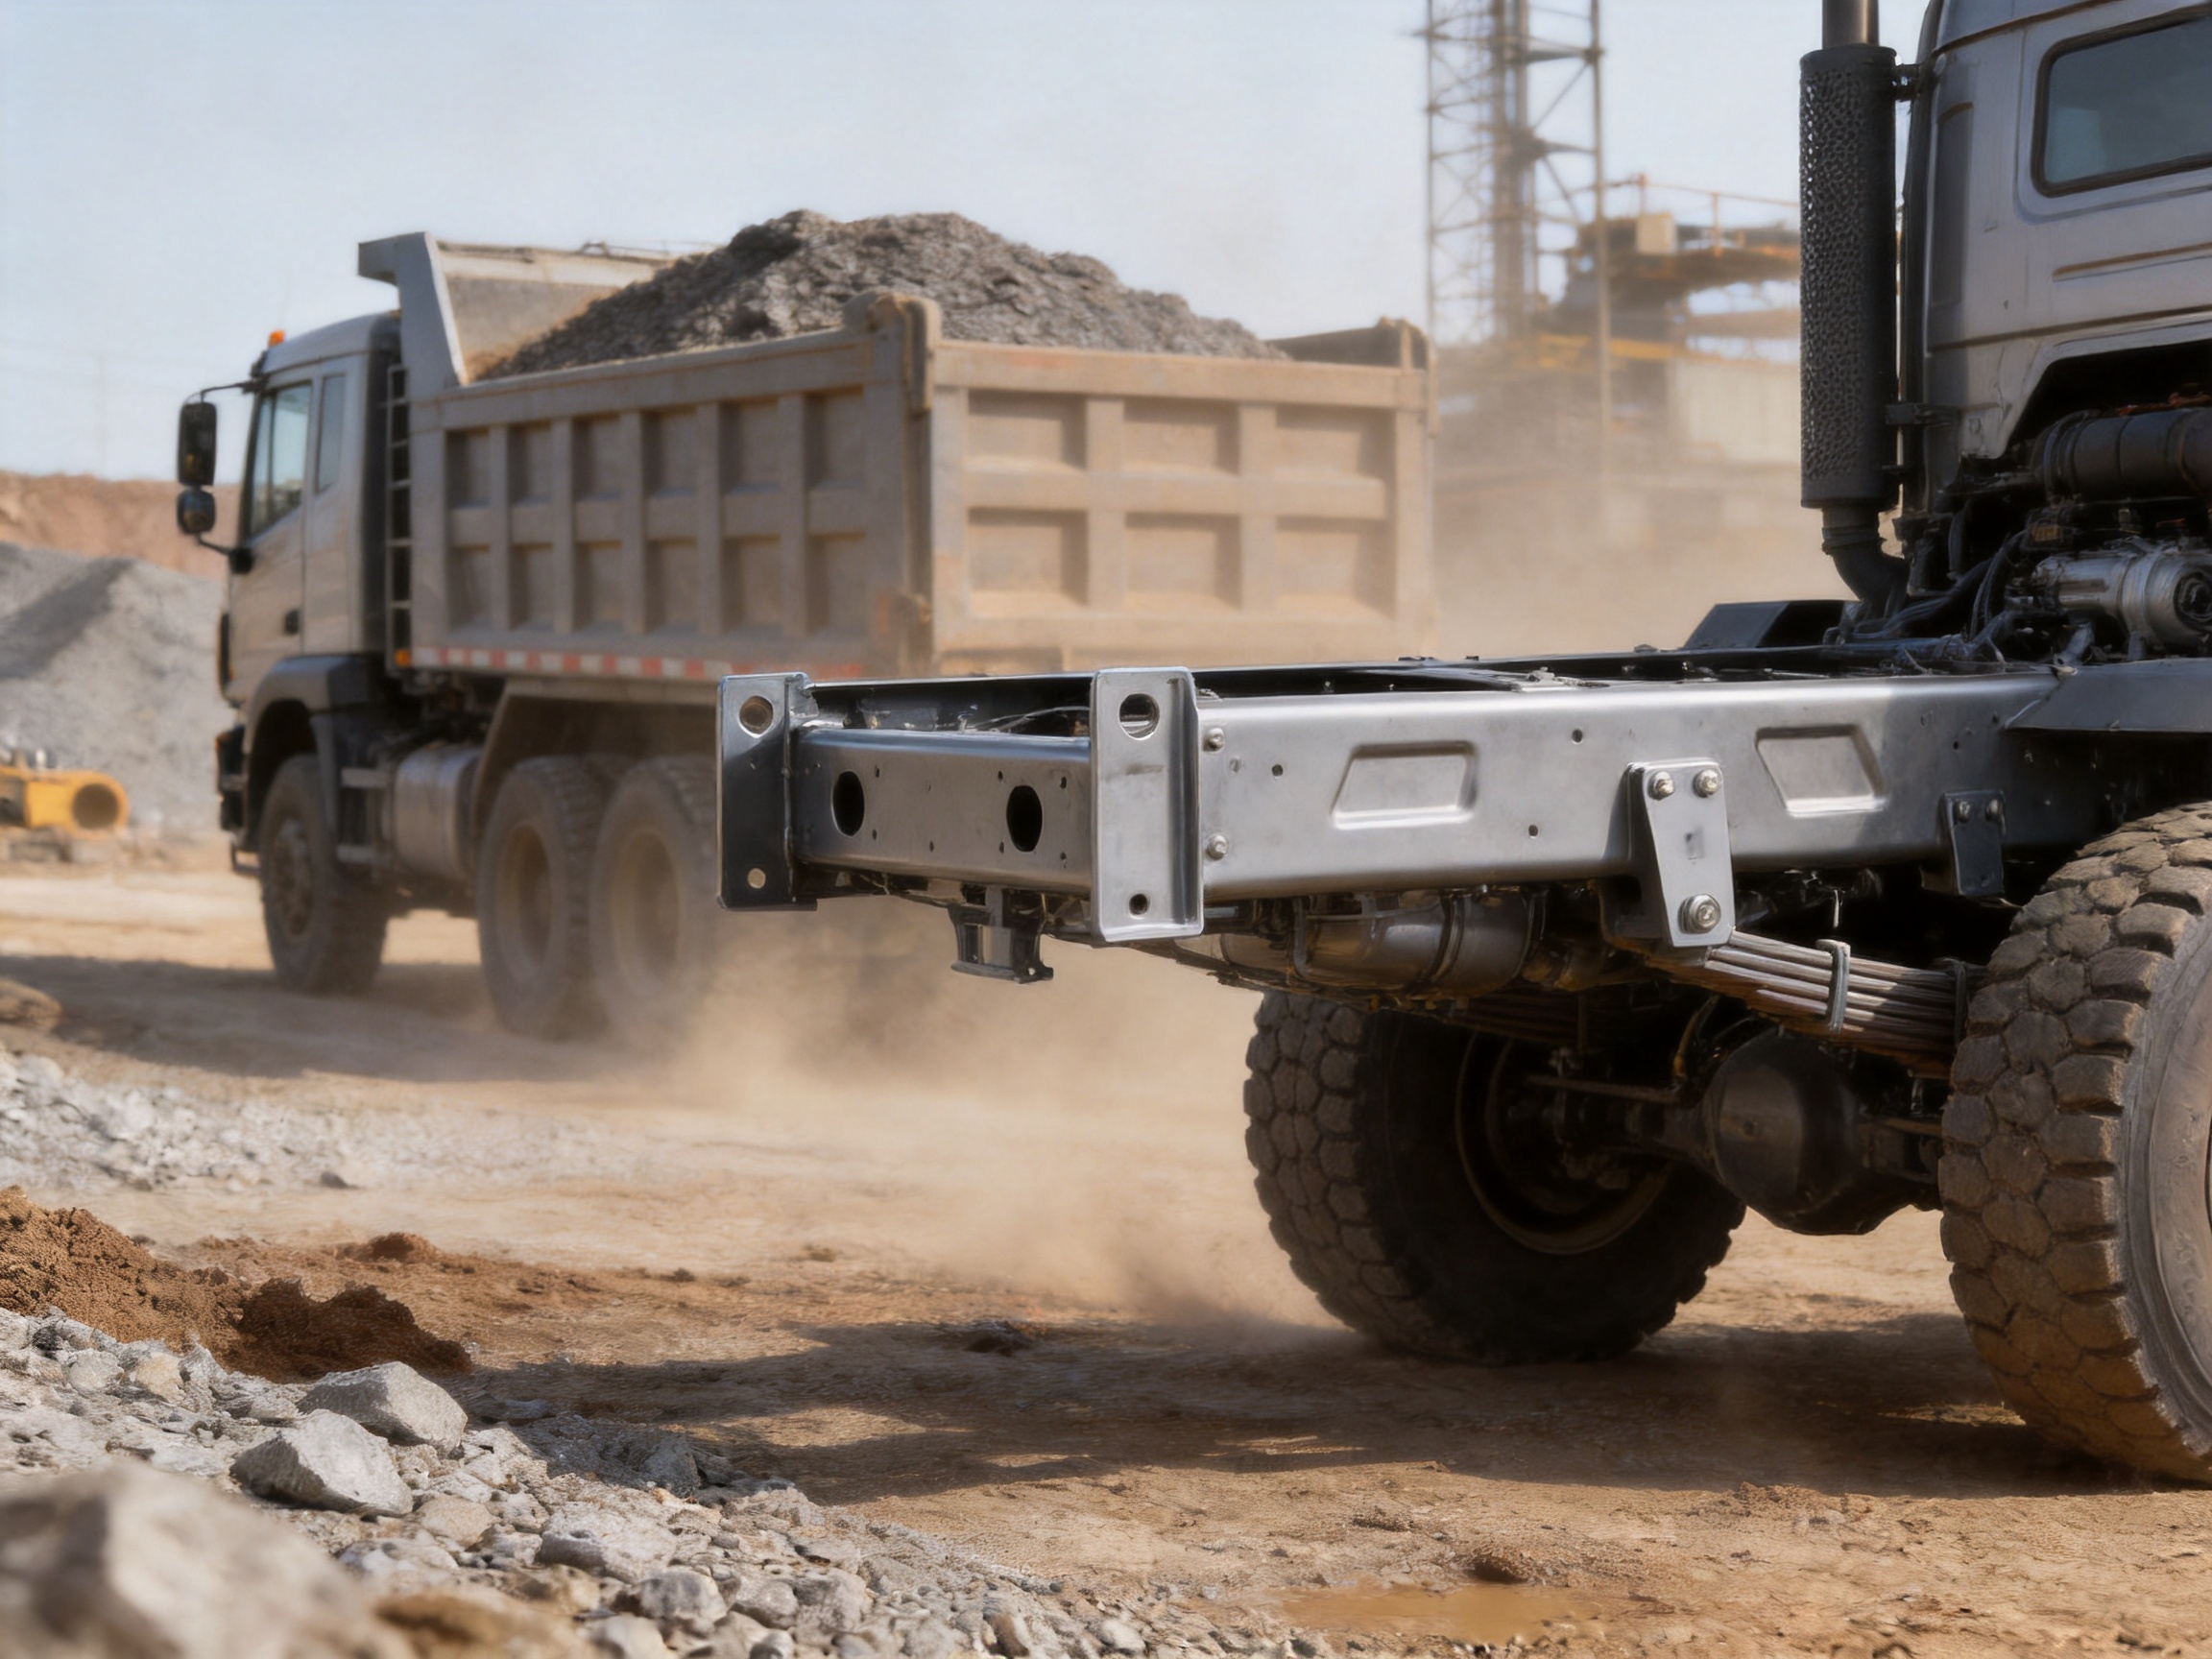
Applications in Original Equipment and Aftermarket Supply
For original equipment manufacturers, heavy truck stamping parts must be integrated into a carefully controlled vehicle platform. The supplier may need to follow strict drawing revisions, approval procedures, inspection plans, packaging specifications, and delivery schedules. Stable quality is essential because a component problem can affect an entire assembly line.
For aftermarket providers, compatibility and availability are often the main priorities. Replacement parts should match the original interface and provide dependable performance under comparable operating conditions. A manufacturer with die-making and production experience can reproduce repeat-use components more consistently than a workshop relying entirely on manual fabrication.
Fleet maintenance organizations may also benefit from reliable replacement components. Trucks that remain out of service create direct financial losses through delayed deliveries, missed construction schedules, or reduced fleet capacity. Durable brackets, supports, and connecting plates can help maintenance teams restore vehicles efficiently and reduce repeat repairs.
Maintenance Considerations for Stamped Components
Even a well-manufactured stamping part should be included in the truck’s inspection program. Maintenance personnel should check for cracks, permanent deformation, loose fasteners, corrosion, damaged coatings, elongated holes, and contact wear. Components exposed to road debris or chemical contamination may require more frequent inspection.
When a part shows deformation or cracking, the surrounding assembly should also be evaluated. Excessive stress may result from a damaged suspension component, improper loading, incorrect fastening torque, misalignment, or repeated operation beyond the vehicle’s intended capacity. Replacing the visible part without correcting the underlying cause may lead to another failure.
Proper installation is equally important. Mounting surfaces should be clean, fasteners should meet the specified grade and torque, and contact points should not be forced into alignment through excessive tightening. Correct installation allows the stamped part to carry loads as intended by the engineering design.
Environmental and Operational Considerations
Heavy truck stamping parts may operate in environments ranging from highways and ports to construction sites, mines, farms, and industrial facilities. Each environment presents different risks. Coastal and winter-road conditions may increase salt exposure. Construction sites may increase impact and dust. Mining operations may subject components to abrasive particles and severe vibration.
Product design and surface treatment should be matched to these conditions. Openings and edges should be designed to avoid unnecessary retention of water and contaminants where practical. Coatings should be selected according to exposure and assembly compatibility. Customers should communicate the intended application so that the supplier can recommend appropriate material and protection requirements.
Environmental responsibility can also be improved through efficient material utilization, durable tooling, reduced scrap, and longer component service life. A part that lasts longer and requires fewer replacements can reduce the material and energy associated with repeated manufacturing and maintenance.
Frequently Asked Questions
Q1: What materials are commonly used for heavy truck stamping parts?
High-strength steel plates are commonly used because they provide strength, stiffness, durability, and practical forming performance. The exact grade and thickness should be selected according to the part’s load, geometry, fatigue requirements, corrosion environment, and customer specification.
Q2: Which truck components can be manufactured by stamping?
Typical examples include frame brackets, suspension connecting plates, engine mounting supports, reinforcement plates, mounting panels, support brackets, and other structural or hardware components. The final product range depends on the customer’s drawing, material, production volume, and functional requirements.
Q3: Why is stamping suitable for heavy-duty vehicle parts?
Stamping provides repeatable geometry, efficient production for repeated orders, good material utilization, and the ability to form stiffening ribs, flanges, and bends into plate components. It is especially suitable when a part must be produced consistently in medium or high quantities.
Q4: Can stamped parts be customized for a specific truck model?
Yes. Parts can be developed according to customer drawings, samples, three-dimensional models, material specifications, hole patterns, surface requirements, and packaging instructions. The supplier should complete a technical review before designing the die and confirming the manufacturing route.
Q5: How does high-strength steel affect the stamping process?
High-strength steel may require greater forming force and more careful control of bend radii, die clearance, material flow, and springback. Tool design and trial debugging must be adjusted to prevent cracking, excessive thinning, distortion, and dimensional variation.
Q6: What inspections are important for heavy truck stamping parts?
Common inspections include material verification, hardness, thickness, flatness, dimensional accuracy, hole position, bend angle, surface condition, burr evaluation, and anti-corrosion performance. The exact inspection plan should be based on the product drawing and application risk.
Q7: What press capacity is available for production?
The available punch presses range from 80 tons to 400 tons. This range supports different component sizes and forming requirements. The appropriate press is selected according to the part geometry, material, thickness, die structure, and required forming force.
Q8: Can the supplier provide stamping dies as well as finished parts?
Yes. The company focuses on stamping dies and hardware parts and can integrate die design, die manufacturing, trial stamping, production, and service. This integrated approach helps coordinate tooling and finished-part requirements.
Q9: Is stamping automation available?
Stamping automation equipment and related technical support are available through the company’s associated automation business. Automation solutions may address feeding, transferring, handling, production efficiency, and process consistency according to the customer’s line configuration.
Q10: How can a customer begin a heavy truck stamping project?
The customer should provide drawings or samples, material and thickness requirements, annual quantity, critical tolerances, surface-treatment requirements, application information, and delivery expectations. The supplier can then review manufacturability, recommend a die and process route, and prepare a project quotation.
Conclusion
Heavy truck stamping parts are essential to the structural reliability, assembly accuracy, and service performance of commercial vehicles. Frame brackets, suspension connecting plates, engine mounting supports, and related hardware must withstand heavy loads, vibration, impact, moisture, and long operating cycles. Precision manufacturing is therefore necessary to achieve uniform thickness, smooth edges, accurate dimensions, suitable flatness, and dependable anti-corrosion performance.
Compared with uncontrolled manual fabrication, precision stamping offers stronger repeatability, efficient volume production, improved material utilization, and the ability to create reinforced forms from steel plate. Its success depends on more than the press operation. Accurate die design, precision machining, experienced debugging, appropriate material selection, stable process control, and complete inspection are all required.
Suzhou Shuangqisi Mold Equipment Co., Ltd. combines stamping die design and manufacturing with hardware-part production and stamping automation capabilities. Its technical team, machining resources, grinding equipment, wire-cutting technology, CNC machining centers, and 80-ton to 400-ton punch presses provide a practical foundation for customized and repeat-production projects. With approximately 15 years of mold-industry experience and a focus on integrated solutions, the company can support customers from initial design review through tooling, trial production, quality inspection, and delivery.
For truck manufacturers, aftermarket suppliers, and fleet-service providers, the right stamping partner can contribute to lower production risk, more efficient assembly, longer component service life, and better total operating value. By combining precision tooling with disciplined production and responsive technical service, heavy truck stamping parts can deliver the durability and consistency required for demanding commercial transportation.
References
1. Society of Automotive Engineers. Automotive Steel Material and Component Engineering Principles.
2. American Society for Testing and Materials. Standard Practices for Steel Sheet, Plate, Hardness, and Corrosion-Protection Evaluation.
3. European Committee for Standardization. General Principles for Metallic Product Dimensional and Geometrical Tolerances.
4. Manufacturing Engineering and Technology. Sheet-Metal Forming, Die Design, Springback Control, and Production Process Management.
5. Automotive Chassis Design. Structural Brackets, Suspension Load Paths, Engine Mounting Systems, and Fatigue Considerations.
6. Industrial Press Technology. Practical Guidelines for Punch Press Selection, Tool Maintenance, and Stamping Process Debugging.
Product: Heavy truck stamping parts
Previous Post
Long-Stroke Multi-Stage Progressive Dies for Complex Sheet Metal Forming
Next Post
Progressive Stamping Dies for High-Speed Connector, Terminal, and Automotive Metal Parts
Our Products.
Start Your Business with an OEM Manufacturer Right Here!

Provide global customers with complete turn-key solutions
through
innovation!
QUICK LINKS
CONTACT INFO.
-
 +86-139 1308 8972
-

-
 No. 118 Yexin Road, Wujiang Economic Development Zone, Suzhou, China
Copyright © Suzhou Shuangqisi Mold Equipment Co., Ltd. All Rights Reserved. Custom Stamping Die Metal Stamping Die Manufacturers
