 English
 Español
 Deutsch
-

Progressive Stamping Die for Connector & Terminal Parts High Speed Progressive Stamping Die Precision Metal Hardware Stamping Tool mold for Connector Terminal Parts Automotive Components
Progressive Stamping Die for Connector & Termi...
-
High Precision Stamping Die Multi Station Hardware Progressive Mold Tooling
Precision Metal Stamping Tool for Automotive &...
-
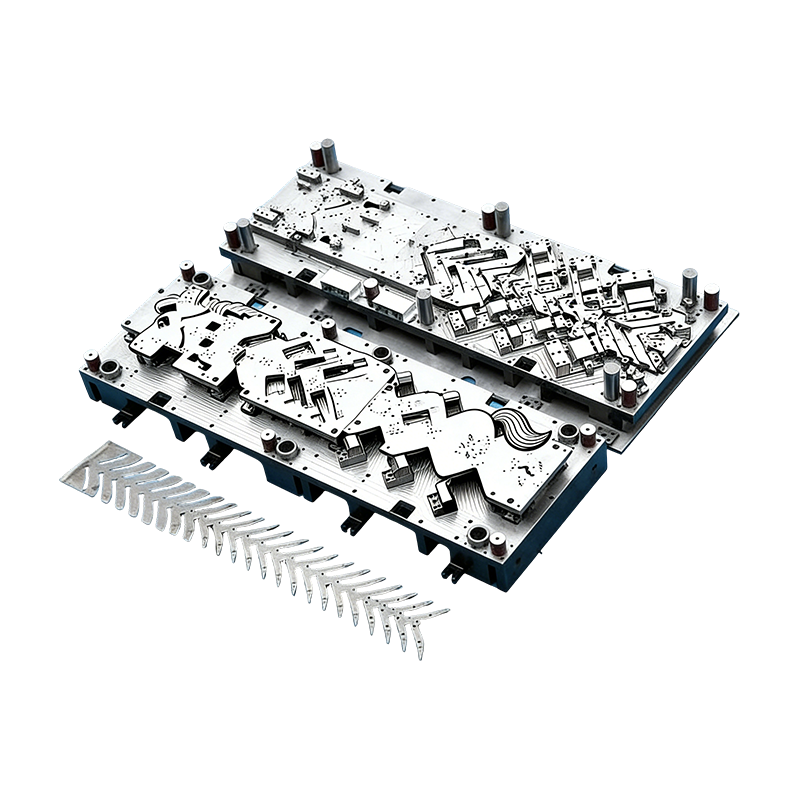
Progressive molds for automotive parts
This Continuous mold for automotive motor housing ...
-

Long-Stroke Multi-Stage Progressive Die Automatic Strip Feed Progressive Die Long Travel Follow on Stamping Tool for Sheet Metal Hardware Press Moulding
Long-Stroke Multi-Stage Progressive DieOur custom ...
-
Multi-Station Progressive Stamping Die with Carbide Inserts Custom Multi Station Progressive Stamping Die Carbide Insert Metal Stamping Mold Tool for Equipment Appliances Device Hardware
High Speed Metal Stamping Tool for Precise Equipme...
-
High Speed Progressive Stamping Die Sheet Metal Follow on Press Tool
Multi-operation Metal Stamping Tool for Continuous...
- E-mail us: [email protected]
- Call us: +86-139 1308 8972

Wang Xinyue – After-Sales Support Supervisor
Home / Author / Wang Xinyue – After-Sales Support Supervisor / Progressive Molds for Automotive Parts: Precision, Efficiency, and Integrated Stamping Solutions
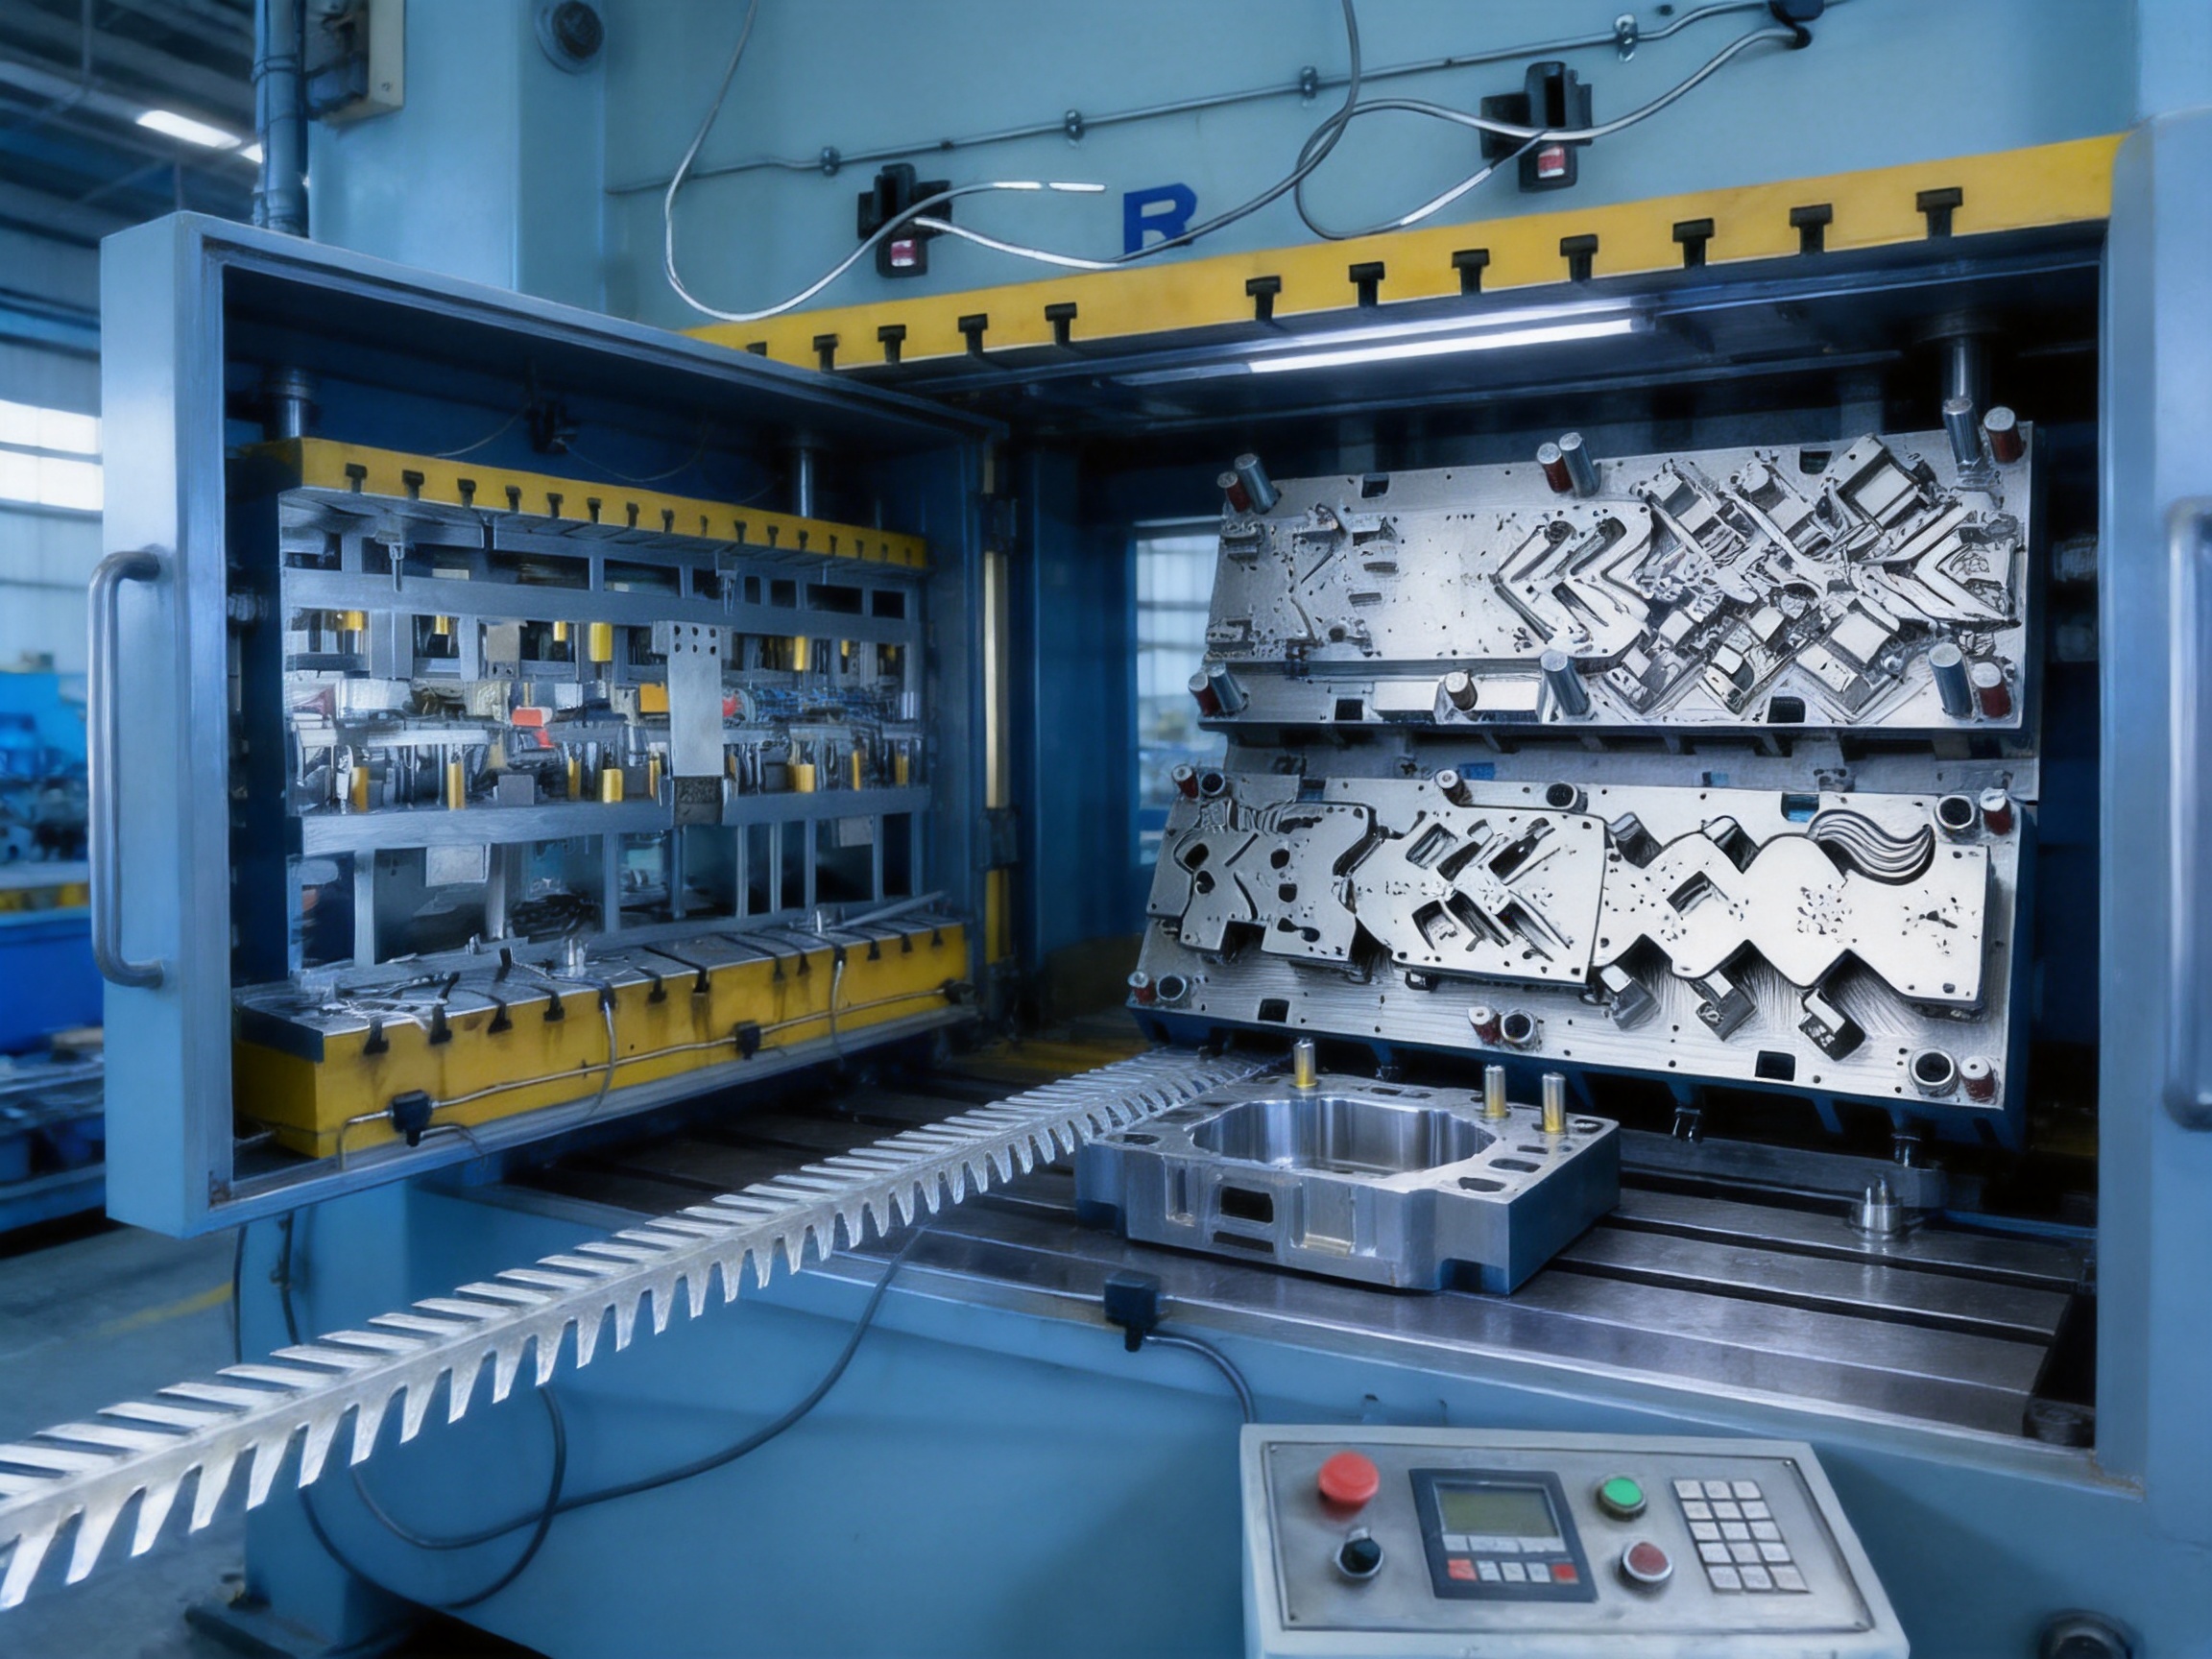
Progressive Molds for Automotive Parts: Precision, Efficiency, and Integrated Stamping Solutions
2026-10-22
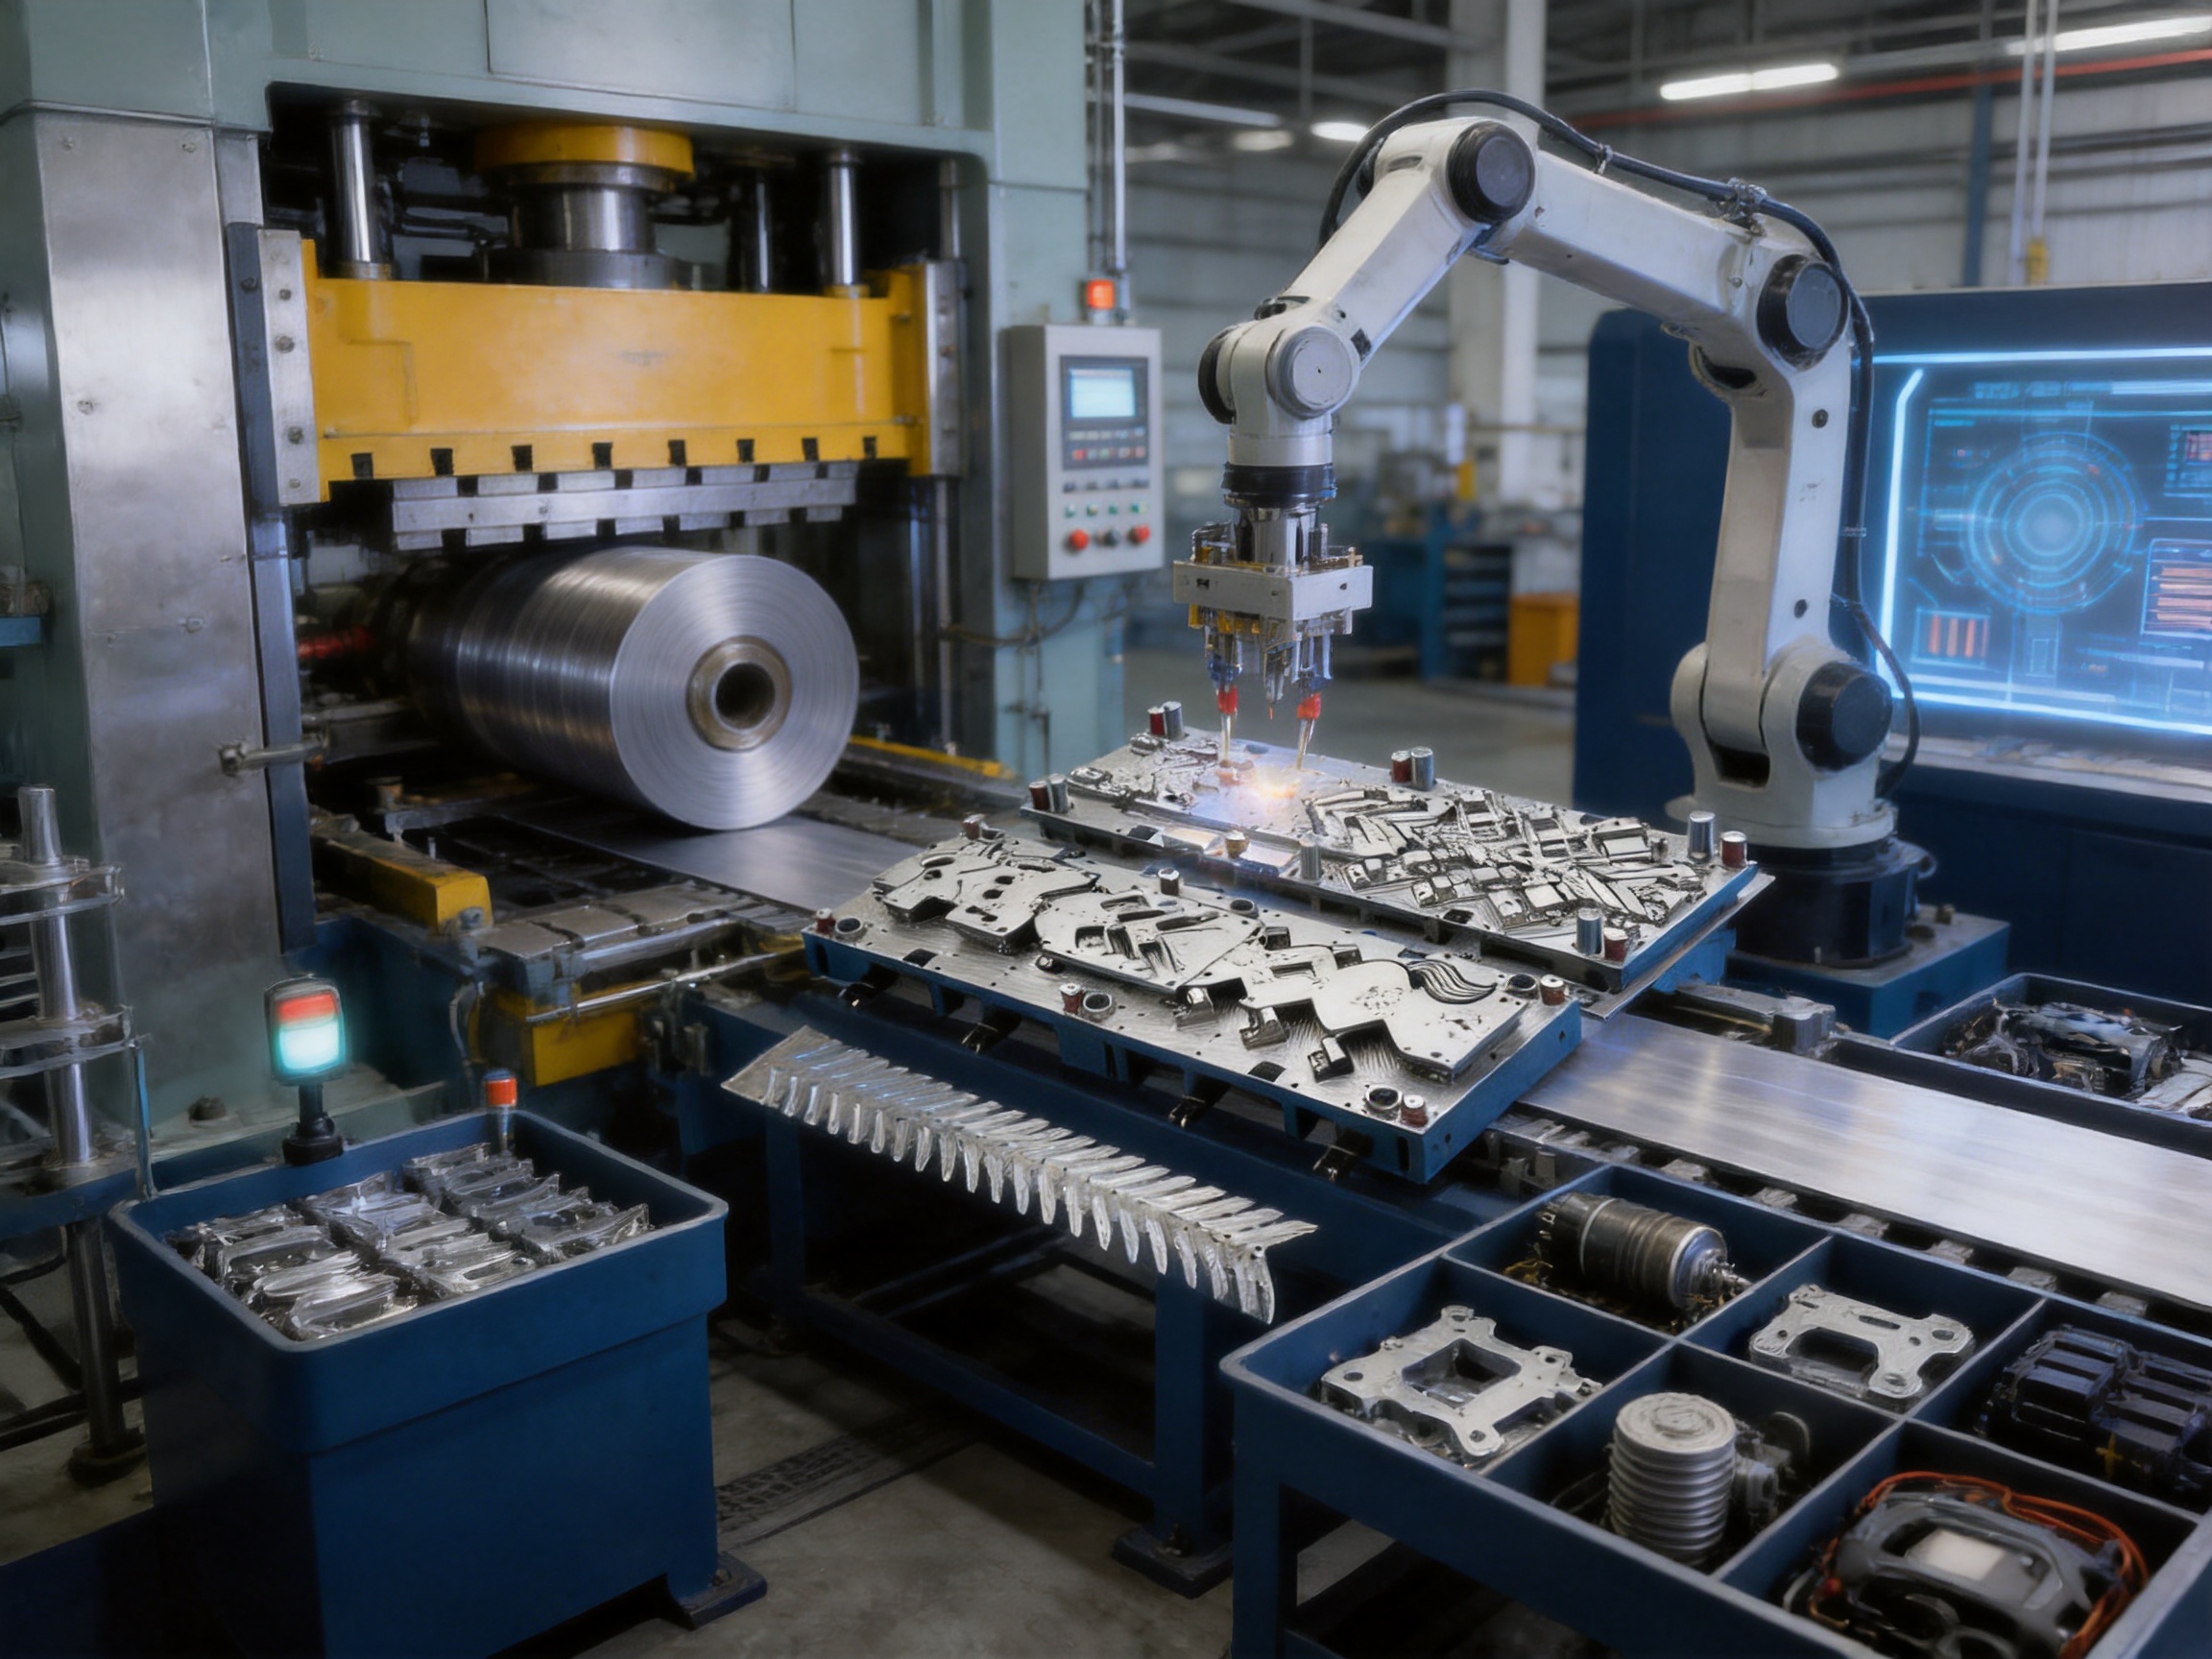
Modern automotive manufacturing depends on production systems that can deliver high accuracy, repeatability, and output while controlling the cost of every component. As vehicles become more compact, electrified, and technologically advanced, the requirements for stamped metal parts are becoming increasingly demanding. Components used in motor housings, powertrain assemblies, servo drives, compressors, and new energy vehicle systems must often combine tight dimensional tolerances with reliable mechanical performance and a consistent surface finish.
Progressive molds for automotive parts provide an effective solution for these production requirements. Also known as progressive stamping dies or continuous molds, these tools allow several forming operations to be completed in sequence as metal strip or sheet advances through the die. Cutting, piercing, drawing, bending, forming, and sizing operations can be integrated into one coordinated production process. This arrangement supports high-volume manufacturing while reducing handling, improving consistency, and shortening cycle times.
The progressive mold for automotive motor housings described in this article has been engineered for the continuous production of automotive motor housings and small-sized automotive parts. It combines stamping and forming operations in a streamlined process designed to support rapid, stable, and repeatable manufacturing. Its high-hardness alloy steel components, modular construction, maintenance-friendly structure, and compatibility with automotive production requirements make it a practical choice for manufacturers seeking a dependable long-term tooling solution.
Content
- 1 1. The Role of Progressive Molds in Automotive Manufacturing
- 2 2. Product Overview: Progressive Molds for Automotive Motor Housings
- 3 3. Key Advantages Over Conventional and Competing Tooling Approaches
- 4 4. Advanced Manufacturing Process
- 5 5. Manufacturing Capabilities of Suzhou Shuangqisi Mold Equipment Co., Ltd.
- 6 6. Integrated Mold and Stamping Automation Solutions
- 7 7. Quality Control Considerations
- 8 8. Application Benefits for Automotive and Electric Vehicle Production
- 9 9. Customer Project Workflow
- 10 10. Why Manufacturing Integration Matters
- 11 11. Frequently Asked Questions
- 11.1 11.1 What is a progressive mold for automotive parts?
- 11.2 11.2 What automotive parts can this mold produce?
- 11.3 11.3 How does the mold improve production efficiency?
- 11.4 11.4 Why are high-hardness alloy steel components used?
- 11.5 11.5 How does the modular structure help maintenance?
- 11.6 11.6 Can the mold support electric vehicle components?
- 11.7 11.7 What manufacturing equipment is available?
- 11.8 11.8 Does the company provide stamping automation?
- 11.9 11.9 What information should a customer provide for a quotation?
- 11.10 11.10 How should a progressive mold be maintained?
- 12 12. Conclusion
- 13 References
- 14 Product: Progressive molds for automotive parts
1. The Role of Progressive Molds in Automotive Manufacturing
Automotive parts are rarely produced through a single simple operation. Even a relatively small metal component may require blanking, piercing, drawing, flanging, bending, embossing, trimming, and calibration before it reaches its final form. Traditional production methods may perform these operations separately, requiring multiple dies, several presses, manual or robotic transfers, and additional inspection stages.
A progressive mold brings many of these operations together. The material moves through a series of stations inside one die. At each station, a specific operation is completed. The strip is indexed forward by a controlled distance, and the next station performs its assigned function. By the time the material leaves the final station, the finished or semi-finished part has been formed according to the required design.
This process has particular value in automotive manufacturing because production volumes are often high and delivery schedules are demanding. Once the progressive die has been correctly installed, adjusted, and validated, it can support repeated production with limited operator intervention. The result is a more stable process, fewer intermediate handling steps, and improved control over part-to-part variation.
For automotive motor housings and related small components, progressive tooling can also help maintain the relationship between critical features. When different operations are performed within the same die set, the part remains located according to a common tooling reference system. This can improve the alignment of holes, formed sections, fitting surfaces, and other functional features.
Progressive molds are not limited to one specific automotive application. They may be adapted for brackets, shields, covers, structural reinforcements, electrical connection components, sensor supports, motor-related parts, and other stamped metal products. Their effectiveness depends on proper engineering, accurate machining, suitable material selection, controlled press operation, and disciplined maintenance.
2. Product Overview: Progressive Molds for Automotive Motor Housings
The product covered here is a continuous mold developed for automotive motor housings and small-sized automotive parts. It is designed to integrate stamping and forming operations into a coordinated production sequence. The tooling concept emphasizes production speed, dimensional stability, wear resistance, and serviceability.
Automotive motor housings often require accurate external profiles, consistent wall thickness, correctly positioned openings, and reliable fitting surfaces. These characteristics are important because the housing may interface with bearings, shafts, covers, electrical components, fasteners, sealing elements, or other sections of a powertrain system. Even a small deviation in a critical area can affect assembly efficiency or create additional downstream correction work.
The mold is therefore designed around the principle of controlled, repeatable forming. Each station contributes to the final geometry while maintaining the position of the workpiece as it progresses through the die. Depending on the specific part design, the tooling may incorporate blanking, piercing, drawing, forming, bending, trimming, or sizing functions. The exact station layout can be customized according to material, thickness, geometry, press capacity, production volume, and tolerance requirements.
The integrated structure is especially useful for mass production. Instead of transferring partially completed pieces between several independent dies, the production line can use one progressive system to perform multiple operations in sequence. This can reduce handling time, minimize the possibility of orientation errors, and simplify the overall production arrangement.
| Product Attribute | Production Value |
|---|---|
| Progressive or continuous operation | Supports sequential stamping and forming within one coordinated die |
| Automotive application | Suitable for motor housings and small automotive components |
| High-hardness alloy steel components | Helps resist wear during extended production use |
| Modular construction | Facilitates maintenance and replacement of selected tooling sections |
| Precision-oriented design | Supports dimensional consistency, uniform wall thickness, and accurate fitting surfaces |
| High-volume capability | Helps manufacturers achieve stable output with reduced interruption |
| Custom engineering potential | Allows the die to be developed around part geometry and customer process requirements |
The value of the product is not limited to the physical die itself. A successful progressive mold is the result of coordinated design, material selection, machining, assembly, debugging, trial production, and process support. The manufacturer’s ability to manage these stages as an integrated project can have a direct effect on the final performance of the tooling.
Progressive molds for automotive parts
3. Key Advantages Over Conventional and Competing Tooling Approaches
3.1 Integrated Production Operations
One of the most important advantages of a progressive mold is the integration of multiple operations into one production system. In a conventional arrangement, separate dies may be used for blanking, drawing, piercing, bending, and finishing. Each additional die introduces another setup, another alignment reference, and another transfer stage.
With a progressive mold, the operations are arranged in a planned sequence. The strip or workpiece advances through the stations while the die maintains controlled positioning. This reduces the number of separate process changes and can make the production line more compact. For high-volume automotive programs, the reduction in handling can contribute to lower labor requirements and more predictable cycle times.
Integrated operation also supports process consistency. When the same die controls several related features, the relationship between those features can be managed more effectively than when the part is moved between independent tools. This is particularly important for housings with multiple openings, formed edges, and mating surfaces.
3.2 Stable High-Volume Output
Automotive suppliers commonly need to produce large quantities without sacrificing dimensional quality. A progressive mold is developed for repeated operation under defined press, material, and process conditions. After the tooling has been validated, the production team can operate it continuously with a consistent feeding and inspection routine.
The continuous design helps reduce idle time caused by repeated loading and unloading. It also allows the press to perform a sequence of operations during each stroke or indexed cycle. In a well-controlled application, this can increase productivity compared with separate manual or semi-automatic operations.
The product described here is intended specifically for mass production scenarios. Its design balances speed and stability so that manufacturers can pursue higher output while maintaining strict quality requirements. The actual production rate will depend on the component design, material characteristics, press configuration, feed system, station count, and approved operating parameters.
3.3 Improved Dimensional Repeatability
Repeatability is essential for automotive parts because components must fit into assemblies produced across multiple production lines and facilities. A die that produces acceptable parts only intermittently can create inspection delays, rework, and assembly problems. Progressive tooling addresses this challenge by using fixed station relationships, guided movement, and controlled forming conditions.
The mold for automotive motor housings is designed to support uniform wall thickness and precise fitting surfaces. These characteristics are important for parts that must interface with other powertrain or motor system components. Stable geometry can also reduce the need for corrective operations after stamping.
Repeatability does not result from die design alone. It also depends on material consistency, press condition, strip feeding accuracy, lubrication, operator training, preventive maintenance, and inspection control. The strength of this product is that its tooling design provides an appropriate foundation for managing these variables in a high-volume environment.
3.4 Wear Resistance for Extended Operation
Progressive dies are exposed to repeated mechanical loading, friction, impact, and contact with metal strip. High-production applications can place substantial demands on punches, inserts, guides, forming sections, and cutting edges. If these areas wear prematurely, dimensional accuracy may decline and maintenance frequency may increase.
The mold uses high-hardness alloy steel components to improve resistance to wear during long-term continuous operation. Properly selected and processed tool steel can help maintain the geometry of working surfaces over an extended production period. It can also improve the durability of high-load sections when combined with appropriate heat treatment, surface preparation, lubrication, and operating conditions.
Material hardness must be balanced with toughness and application requirements. Excessive hardness without adequate toughness may increase the risk of chipping or fracture in certain sections. For this reason, effective die manufacturing involves selecting materials according to the function of each component rather than applying one material choice indiscriminately across the entire tool.
3.5 Modular Maintenance and Faster Repair
Maintenance is a major consideration in automotive tooling. Even a well-designed die eventually requires inspection, adjustment, sharpening, replacement, or repair. If the complete die must be removed or rebuilt whenever one working section is damaged, production downtime can become expensive.
The modular design of this mold allows selected damaged or worn parts to be replaced more efficiently. Modular inserts and replaceable working components can make maintenance more targeted. This approach may reduce the time needed to restore the die and limit the effect of localized wear on the overall production schedule.
Modularity also supports future adaptation. If a customer needs to modify a hole position, forming radius, trimming section, or other localized feature, it may be possible to update a specific module instead of redesigning the complete die. The feasibility of such modifications depends on the original die structure and the extent of the requested change, but modular thinking provides a valuable foundation for long-term tooling service.
3.6 Reduced Production Interruption
Every production interruption can affect delivery schedules, machine utilization, labor planning, and customer commitments. A progressive mold can reduce certain sources of interruption by combining several operations, using durable working materials, and providing replaceable modules for maintenance.
The manufacturer’s experience in die debugging and production support is also important. A tooling project that includes practical commissioning assistance can reach stable production more efficiently than a project focused only on machining the die components. Careful trial stamping, dimensional verification, process adjustment, and operator guidance all contribute to reliable production startup.
3.7 Better Overall Process Economy
Tooling cost should not be evaluated only by the purchase price of the die. A more complete assessment includes production speed, material utilization, labor requirements, maintenance, scrap, downtime, inspection effort, and expected service life. A progressive mold may provide a higher level of initial engineering and manufacturing investment than a simple single-operation tool, but it can deliver greater value when production volume is high.
By combining operations and reducing manual transfers, the mold can help simplify the production route. Its wear-resistant components can support longer service intervals, while the modular structure can reduce the cost and duration of certain repairs. These advantages may improve the total cost of ownership over the life of an automotive program.
4. Advanced Manufacturing Process
The performance of a progressive mold depends on the quality of the manufacturing process used to create it. Automotive tooling requires more than accurate drawings. The die must be machined, assembled, adjusted, and tested so that each station works correctly in relation to the others.
4.1 Engineering Review and Process Planning
The manufacturing process begins with an examination of the part design and production objectives. The engineering team evaluates the part geometry, material type, thickness, forming depth, critical tolerances, feature locations, expected production volume, and press conditions. These factors influence the number and order of die stations.
Process planning may determine whether the part requires progressive blanking, piercing, drawing, bending, trimming, restriking, or other operations. The team must also consider strip layout, material utilization, carrier design, pilot locations, feed pitch, forming direction, and the prevention of deformation during transfer between stations.
A well-planned strip layout is particularly important. It should use material efficiently while providing enough support for stable feeding and accurate positioning. The layout must also account for the forces generated at each station and ensure that the strip remains sufficiently rigid throughout the process.
4.2 Die Structure and Component Selection
After the process sequence is established, the die structure is developed around the required working components. These may include punches, dies, inserts, guide pillars, guide bushes, stripper plates, pressure pads, lifters, pilots, cutting sections, forming blocks, and modular replacement units.
Each component has a specific role. Punches and die openings control cutting and forming features. Guides maintain alignment between the upper and lower sections. Strippers help separate the material from punches and control movement. Pilots help correct or maintain strip position before critical operations. Inserts can isolate high-wear areas and simplify replacement.
The structure must provide sufficient rigidity to prevent unwanted deflection during operation. It must also allow access for inspection, cleaning, lubrication, adjustment, and repair. A die that is difficult to maintain may create avoidable production delays even if its initial forming performance is satisfactory.
4.3 Precision Machining
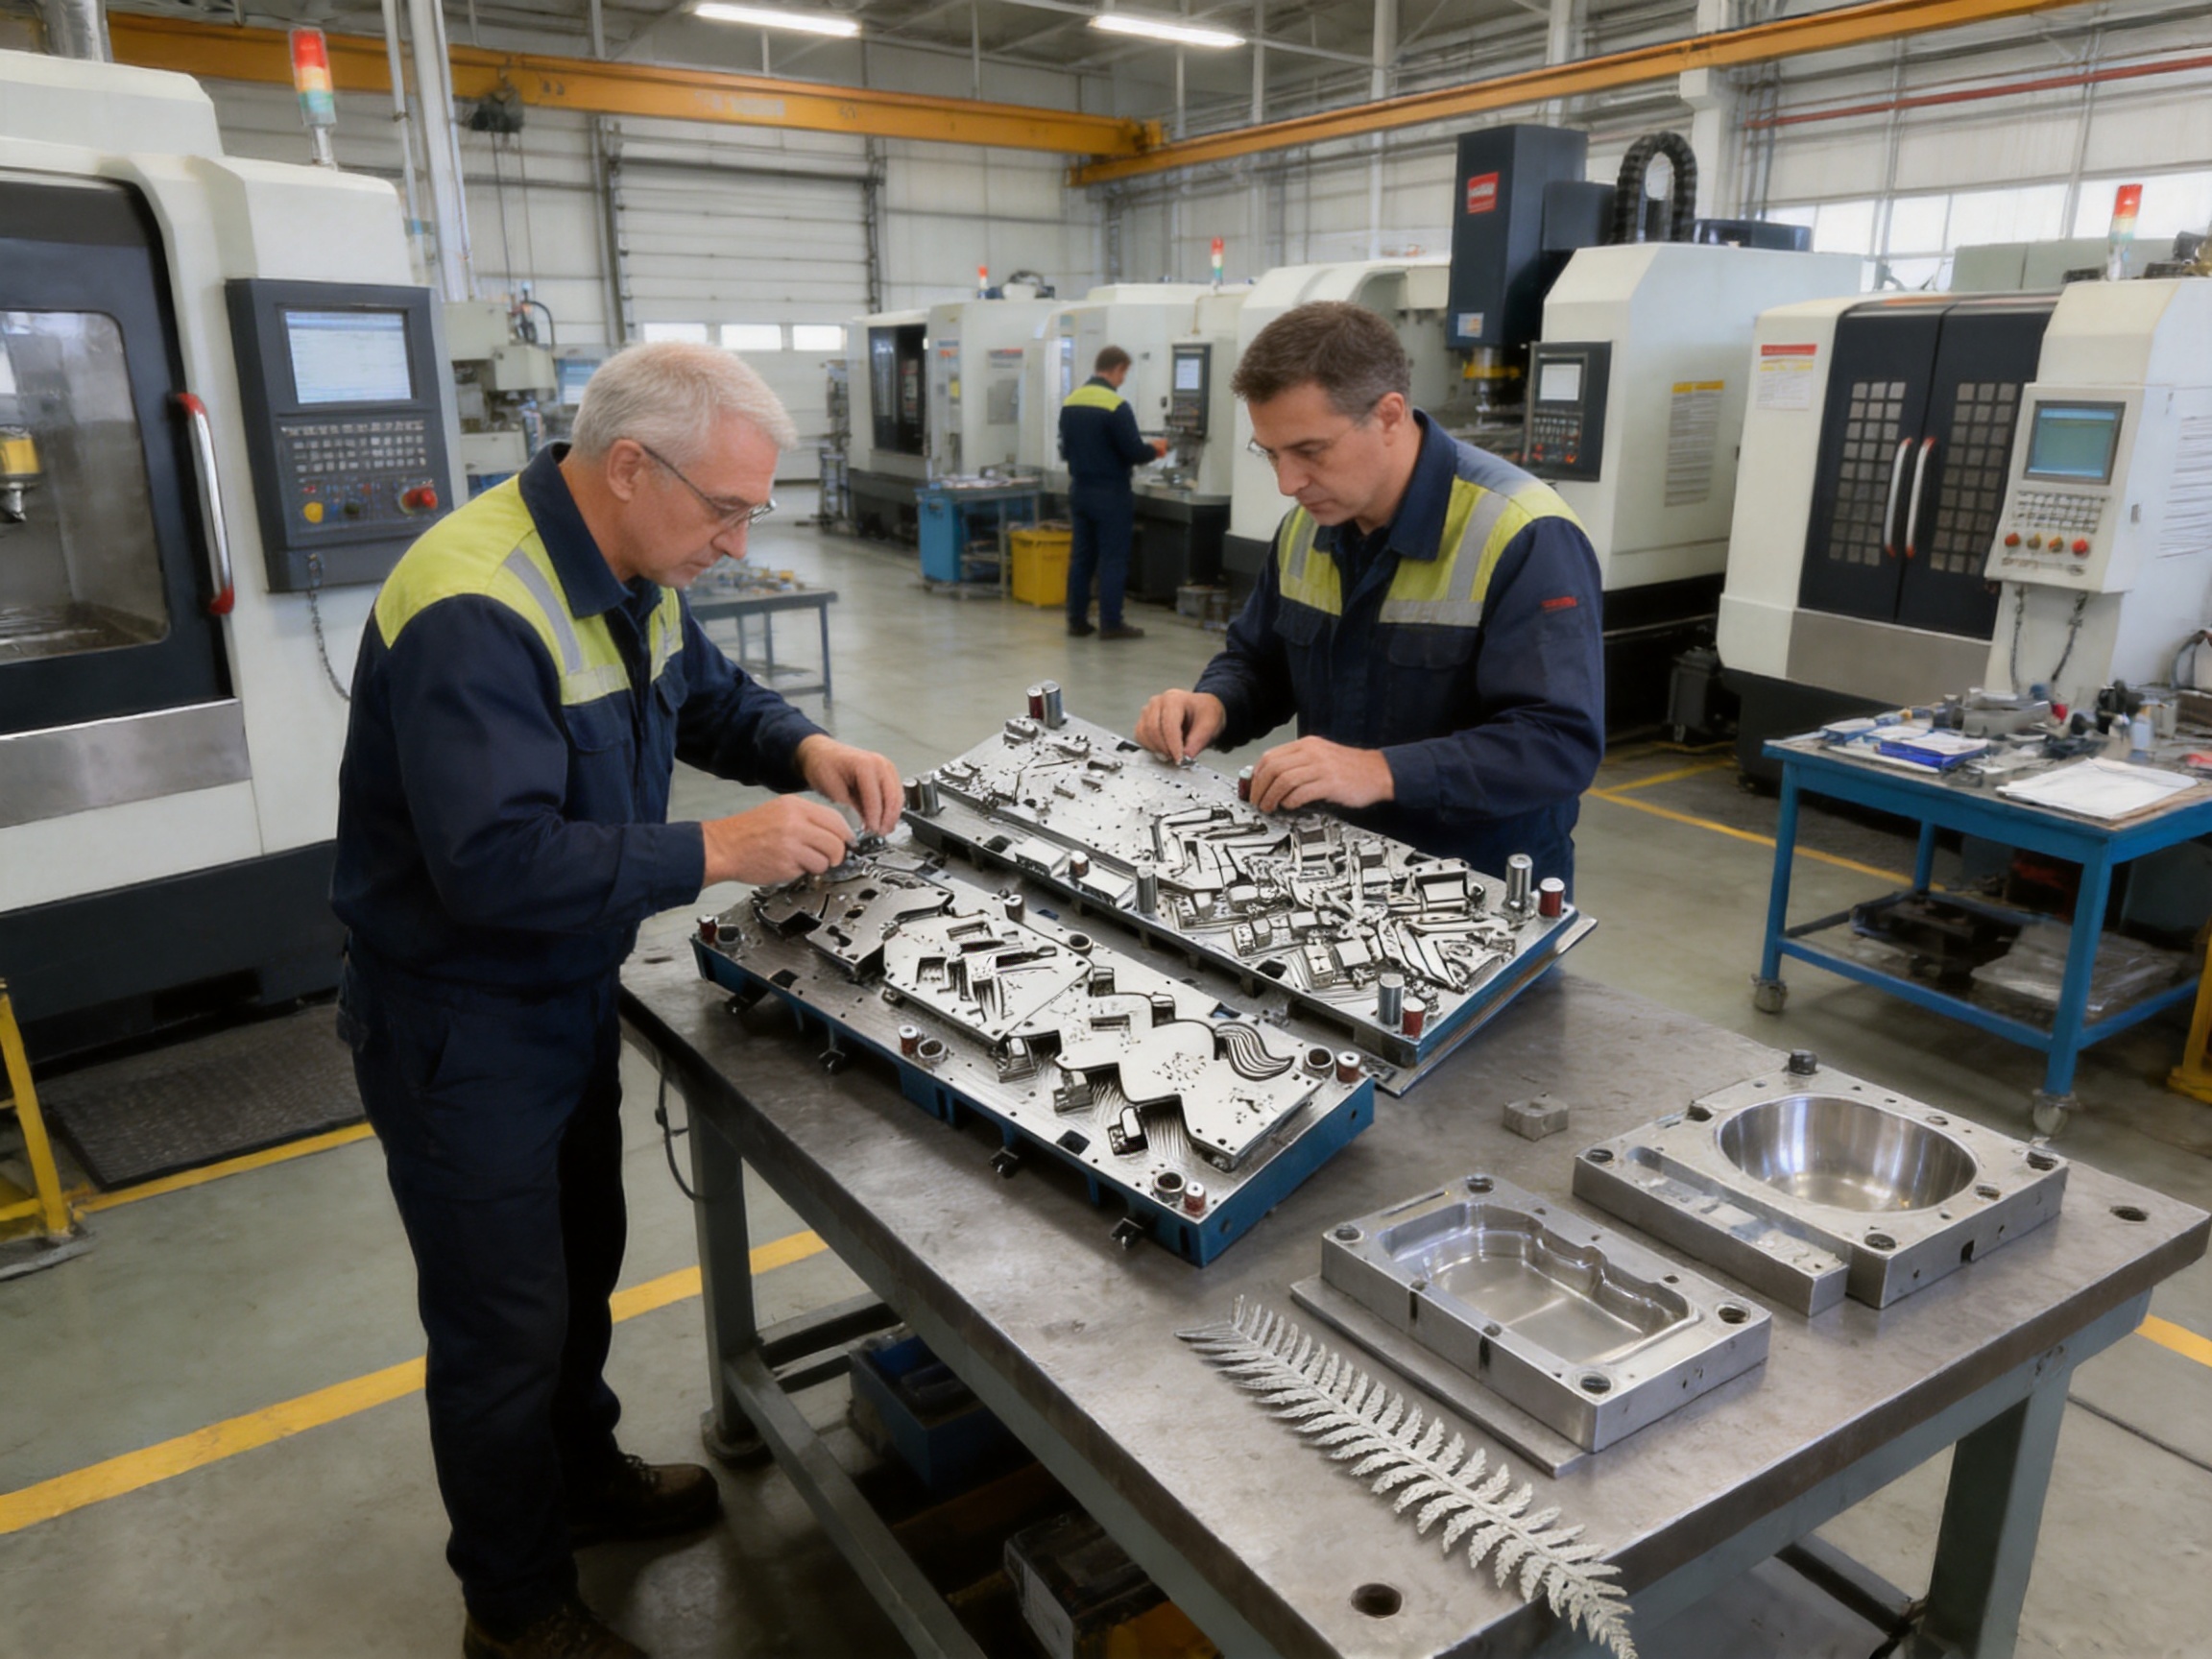
Suzhou Shuangqisi Mold Equipment Co., Ltd. is equipped with imported wire cutting machines, CNC machining centers, more than ten grinding machines of various sizes, and other precision machine tools. This equipment supports the production of die components requiring controlled geometry, accurate edges, close-fitting interfaces, and consistent surface quality.
Wire cutting is valuable for producing intricate profiles and precise openings in hardened or difficult-to-machine materials. CNC machining centers support the production of complex three-dimensional components, pockets, mounting surfaces, and modular inserts. Grinding operations help refine critical surfaces and achieve the dimensional accuracy required for proper die assembly and operation.
Precision machining must be supported by correct workholding, tool selection, cutting parameters, inspection practices, and process sequencing. A component may be accurately machined in isolation yet fail to perform correctly if its relationship to neighboring components is not controlled. For this reason, machining is coordinated with assembly references and the overall die structure.
4.4 Heat Treatment and Wear Management
High-hardness alloy steel components are selected for areas exposed to repeated contact and forming loads. Depending on the component and material specification, heat treatment may be used to achieve an appropriate balance of hardness, toughness, dimensional stability, and service performance.
Wear management also includes the design of replaceable inserts, the control of contact surfaces, proper clearance, suitable lubrication, and regular inspection. The goal is not simply to maximize hardness. The goal is to create a working system that preserves accuracy under real production conditions.
4.5 Assembly and Fitting
Die assembly requires careful fitting of machined components. Working sections must be aligned, clearances must be checked, and moving elements must operate smoothly without binding. The upper and lower die sections must maintain the intended relationship throughout the press stroke.
Experienced assembly personnel inspect the contact condition of components and confirm that replaceable modules can be installed and removed correctly. They also verify the operation of guide systems, strippers, lifters, pilots, and other moving parts. Proper assembly is critical because small errors can lead to burrs, material distortion, uneven forming, accelerated wear, or die damage.
4.6 Trial Stamping and Debugging
Before the die enters regular production, it must be tested under controlled conditions. Trial stamping allows the technical team to evaluate the forming sequence, material flow, feeding stability, part release, feature accuracy, and surface quality.
Debugging may involve adjusting clearances, forming heights, stripper pressure, pilot timing, feed position, lubrication, or other process parameters. Samples are inspected against the approved part requirements. If a feature does not meet the required condition, the team investigates whether the cause is related to die geometry, material behavior, press settings, feeding accuracy, or another factor.
The company has senior operators and experienced debugging personnel who support this stage of production. Their practical experience is valuable because some forming issues are best understood through direct observation of the press, strip movement, material response, and finished parts.
4.7 Final Verification and Production Handover
After debugging, the die undergoes final verification. The inspection process may include dimensional checks, visual examination, functional testing, sample production, and confirmation of stable operation. Documentation can include die drawings, maintenance guidance, component lists, process notes, and recommended inspection points.
A responsible handover helps the customer operate the tool correctly from the beginning. It also provides a reference for future maintenance and troubleshooting. The objective is to deliver not only a completed mold but a production-ready solution that can be integrated into the customer’s manufacturing system.
5. Manufacturing Capabilities of Suzhou Shuangqisi Mold Equipment Co., Ltd.
Suzhou Shuangqisi Mold Equipment Co., Ltd. is a professional manufacturer of stamping dies and hardware parts integrating design, manufacturing, and service. Located in Suzhou, China, the company has developed capabilities covering tooling engineering, precision machining, die assembly, debugging, stamping production support, and automation-related solutions.
The company has approximately 60 technical staff and operates a manufacturing facility equipped for a range of precision tooling activities. Its equipment includes imported wire cutting machines, CNC machining centers, more than ten grinding machines of different sizes, and 25 punch presses ranging from 80 tons to 400 tons. This combination supports both die manufacturing and practical stamping trials across a variety of component sizes and forming requirements.
The range of press capacities is important for tooling validation. A die must be tested under conditions that represent its intended production environment. Access to presses with different capacities can support process development for small hardware parts as well as more demanding automotive applications.
The company’s technical team includes senior operators and experienced debugging personnel. Their role extends beyond operating machinery. They contribute to process adjustment, tool verification, problem diagnosis, and production stabilization. This practical capability can help bridge the gap between computer-aided design and real-world stamping performance.
The company serves customers in fields including servo drives, compressors, and new energy vehicles. Its stated customer base includes Anter Group, Ousheng Electric, Dongbei Group, and Huichuan Technology. These industry areas require dependable metal components and tooling systems, particularly where precision, repeatability, and production continuity are important.
With 15 years of experience in the mold industry, the company has developed a foundation in stamping die design and manufacturing. Its focus is on creating value for customers through high-quality products, competitive pricing, technical support, and integrated production services.
6. Integrated Mold and Stamping Automation Solutions
A major strength of the company is its ability to connect mold manufacturing with stamping automation. In 2016, it invested in and established Suzhou Keshuang Intelligent Technology Co., Ltd., which mainly produces stamping automation equipment. This development expanded the company’s ability to offer customers more than standalone tooling.
Automation can include feeding equipment, transfer systems, material handling, part collection, inspection support, and coordinated press-line functions. When automation is designed together with the die, the complete process can be evaluated as one system. This may help improve synchronization, reduce manual handling, and support safer and more repeatable production.
For customers developing a new automotive component, the combination of die engineering and automation capability can simplify project coordination. Instead of managing unrelated suppliers for the die, feeding system, transfer equipment, and production integration, the customer may obtain a more complete solution from an experienced technical partner.
The company can provide turnkey solutions for stamping molds and stamping automation. It can also invest in related production equipment according to customer needs. This flexible approach may be valuable for companies that need to establish a new production line but want to control capital expenditure and technical risk.
An integrated project should begin with a clear understanding of the product, material, output target, production schedule, factory layout, press availability, quality standards, and future expansion plans. These factors influence the die structure, automation arrangement, inspection method, and maintenance strategy.
The combination of progressive molds and automation is especially suitable for high-volume automotive parts. The die performs the forming operations, while the automation system manages material movement and production flow. Together, they can create a more consistent and less labor-intensive manufacturing process.
7. Quality Control Considerations
Quality control for automotive progressive molds begins during design and continues through machining, assembly, trial production, and customer use. Each stage should be connected to the requirements of the finished part.
7.1 Dimensional Control
Critical die components must be inspected against their design requirements before assembly. The inspection process should focus on working profiles, guide relationships, hole positions, forming surfaces, insert locations, and other features that influence finished part accuracy.
During trial production, the molded parts should be checked for dimensions, wall thickness, hole position, surface condition, burrs, cracks, wrinkles, distortion, and fitting performance. The inspection method should reflect the function of the part rather than relying only on general appearance.
7.2 Material and Surface Quality
Tool steel selection, heat treatment, grinding quality, and surface preparation all affect die performance. Working surfaces should be free from defects that could damage the strip or create inconsistent forming conditions. Contact areas should be properly finished according to their function.
For automotive motor housings, surface quality can matter both visually and functionally. Scratches, galling, excessive burrs, or uneven edges may interfere with assembly or require additional finishing operations.
7.3 Process Stability
A die may produce an acceptable sample during a short trial but still require additional observation before being approved for continuous operation. Process stability should be assessed over a suitable production run. The team should monitor feeding, material flow, part release, press behavior, die temperature where relevant, lubrication, and changes in part dimensions.
Stable production is especially important when the mold is intended for high-volume use. The purpose of trial production is not simply to produce one good part; it is to confirm that the process can repeatedly produce conforming parts under defined conditions.
7.4 Maintenance Planning
Maintenance documentation should identify inspection points, lubrication requirements, wear components, recommended replacement intervals, and safe disassembly procedures. A modular design makes this planning more practical because individual parts or inserts can be tracked and replaced as needed.
Preventive maintenance is generally more effective than waiting for a failure. Regular cleaning and inspection can identify abnormal wear, loose fasteners, damaged guides, burr development, material buildup, or changes in forming performance before they lead to serious downtime.
8. Application Benefits for Automotive and Electric Vehicle Production
The automotive industry is undergoing significant changes as electric vehicles and advanced powertrain systems become more widespread. Although electric vehicles use different components from conventional vehicles, they still require many precision metal parts, including motor-related housings, shields, brackets, covers, supports, and electrical hardware.
Motor housings and similar components must often meet demanding requirements for shape, alignment, strength, and assembly compatibility. A progressive mold can support these requirements by integrating multiple forming stages and maintaining a consistent tooling reference throughout production.
The same principles apply to components used in servo drives, compressors, and other electromechanical systems. These products may require high production volumes and consistent quality because they are integrated into larger systems. A tooling supplier with experience across automotive, electrical, and new energy applications can apply knowledge from one sector to another while still customizing the die to the individual part.
The product is also suitable for small-sized automotive parts where the production quantity justifies dedicated tooling. In these applications, the speed advantage of a progressive die can be significant. The die can produce multiple features within a compact footprint, reducing the need for separate equipment and manual transfers.
For electric vehicle supply chains, production flexibility is increasingly valuable. Customers may need to develop new parts quickly, increase output in stages, or modify a component after initial testing. A modular tooling structure and an engineering team capable of supporting design changes can help manage these evolving requirements.
9. Customer Project Workflow
A successful tooling project benefits from a clear workflow. The following stages provide a practical framework for developing progressive molds for automotive parts.
9.1 Initial Requirement Review
The customer provides part drawings, three-dimensional data, material specifications, thickness information, tolerance requirements, target output, press details, and quality expectations. The manufacturer reviews the information and identifies any issues that may affect formability, die life, or production stability.
9.2 Feasibility and Process Proposal
The engineering team proposes a forming sequence, strip layout, station arrangement, die structure, and estimated production approach. Potential risks such as cracking, wrinkling, springback, excessive burrs, material waste, or difficult part release should be considered at this stage.
9.3 Design Approval
After technical discussion, the customer approves the proposed design or requests modifications. Clear approval of the die layout and critical features helps prevent misunderstandings later in the manufacturing process.
9.4 Machining and Component Production
Approved components are manufactured using CNC machining, wire cutting, grinding, and related processes. Critical parts are inspected before moving to assembly. Components requiring special hardness or surface characteristics are processed according to the agreed technical requirements.
9.5 Assembly and Trial Production
The die is assembled and tested on a suitable press. Trial samples are produced and evaluated. Adjustments are made to improve part quality, feeding stability, and overall operation.
9.6 Customer Validation
The customer reviews samples and confirms that the die meets the agreed requirements. Depending on the project, validation may include dimensional reports, production trials, capability studies, or assembly checks.
9.7 Delivery and After-Sales Support
After acceptance, the mold is prepared for delivery or installed within the customer’s production line. Technical guidance, maintenance recommendations, troubleshooting support, and replacement component planning can help maintain performance during long-term use.
10. Why Manufacturing Integration Matters
Many tooling problems occur when design, machining, testing, and production support are treated as isolated activities. A die designer may not fully understand press limitations. A machining supplier may not be familiar with forming behavior. A production operator may receive a tool without sufficient maintenance information. These gaps can delay commissioning and increase the total cost of the project.
An integrated manufacturer can reduce these communication barriers. When design engineers, machinists, assemblers, debugging personnel, and automation specialists work within a connected organization, technical information can move more efficiently between departments.
This integrated model is one of the principal strengths of Suzhou Shuangqisi Mold Equipment Co., Ltd. The company combines stamping die design and manufacturing with hardware parts production, press resources, experienced debugging, and stamping automation capability. As a result, its services can address not only the tooling itself but also the broader production process.
For customers, this may provide several practical benefits. Technical decisions can be made with a clearer understanding of manufacturing reality. Tooling and automation can be coordinated at an earlier stage. Production trials can be organized more efficiently. Problems can be traced to their source without requiring several independent suppliers to exchange information.
11. Frequently Asked Questions
11.1 What is a progressive mold for automotive parts?
A progressive mold is a stamping die that performs multiple operations in sequence as metal strip or sheet advances through the tooling. It may include blanking, piercing, drawing, bending, forming, trimming, and sizing stations. The finished or partially finished component exits after passing through the required operations.
11.2 What automotive parts can this mold produce?
The product described is intended for automotive motor housings and small-sized automotive parts. Depending on the approved design, progressive tooling may also be adapted for brackets, covers, shields, supports, electrical components, compressor parts, servo-drive components, and other stamped metal products.
11.3 How does the mold improve production efficiency?
It combines several operations into one coordinated process, reducing manual transfers and the need for multiple separate dies. The continuous structure supports faster cycle times, consistent positioning, and stable high-volume output when used with an appropriate press and feeding system.
11.4 Why are high-hardness alloy steel components used?
High-hardness alloy steel components help resist wear caused by repeated contact, cutting, and forming. This supports dimensional stability during extended production. The final material choice should also consider toughness, heat treatment, working load, and the specific function of each die component.
11.5 How does the modular structure help maintenance?
Modular construction allows selected inserts or working sections to be inspected, repaired, adjusted, or replaced without necessarily rebuilding the complete die. This can reduce maintenance time and help limit production interruptions caused by localized wear or damage.
11.6 Can the mold support electric vehicle components?
Yes. The mold is positioned for automotive and new energy vehicle applications, including motor-related parts and other small precision-stamped components. Each project must still be engineered according to the specific material, geometry, tolerance, and production volume of the component.
11.7 What manufacturing equipment is available?
The manufacturer has imported wire cutting machines, CNC machining centers, more than ten grinding machines of various sizes, and 25 punch presses with capacities from 80 tons to 400 tons. This equipment supports die machining, component production, trial stamping, and process validation.
11.8 Does the company provide stamping automation?
Yes. Through its related automation capability, the company can provide stamping automation equipment and turnkey solutions that combine molds with production equipment. The exact automation arrangement depends on the customer’s part, press, output, factory layout, and handling requirements.
11.9 What information should a customer provide for a quotation?
Useful information includes part drawings or three-dimensional files, material type, material thickness, annual or monthly volume, tolerance requirements, press specifications, feeding method, quality standards, delivery schedule, and any existing automation requirements. More complete information allows a more accurate technical and commercial evaluation.
11.10 How should a progressive mold be maintained?
Maintenance generally includes regular cleaning, lubrication, inspection of working edges and guides, checking of fasteners, monitoring of burrs and part dimensions, and timely replacement of worn components. A maintenance schedule should be adapted to the material, production volume, die design, and operating conditions.
12. Conclusion
Progressive molds for automotive parts are essential tools for manufacturers that need to combine precision, speed, and production stability. The continuous mold for automotive motor housings described in this article integrates stamping and forming operations into one coordinated system. Its high-hardness alloy steel components are intended to support wear resistance and long-term dimensional accuracy, while its modular construction makes maintenance and component replacement more practical.
Compared with separate single-operation tooling arrangements, the progressive design can reduce handling, improve feature alignment, simplify production flow, and support high-volume output. These advantages are particularly relevant to automotive motor housings, small automotive parts, servo-drive components, compressor parts, and new energy vehicle applications.
The value of the solution is strengthened by the manufacturing capabilities of Suzhou Shuangqisi Mold Equipment Co., Ltd. The company combines die design, precision machining, grinding, wire cutting, press resources, assembly, debugging, and technical support. Its team of approximately 60 technical staff, senior operators, and experienced debugging personnel provides a foundation for practical tooling development.
The company’s investment in stamping automation also extends its ability to provide integrated production solutions. By connecting molds with automation equipment and related production systems, it can help customers address the broader requirements of high-volume stamping rather than treating the die as an isolated product.
For manufacturers evaluating a progressive mold, the most important considerations include part geometry, material behavior, production volume, tolerance requirements, press capacity, maintenance strategy, automation compatibility, and supplier engineering capability. When these factors are addressed together, a progressive mold can become a long-term production asset that supports stable quality, improved efficiency, and controlled manufacturing costs.
For technical inquiries and project discussions, Suzhou Shuangqisi Mold Equipment Co., Ltd. can be contacted at +86-139 1308 8972 or [email protected]. Its facility is located at No. 118 Yexin Road, Wujiang Economic Development Zone, Suzhou, China.
References
1. Automotive Industry Action Group. Automotive Quality Core Tools and Production Part Approval Principles.
2. American Society of Mechanical Engineers. General Principles of Metal Forming and Manufacturing Process Design.
3. ASM International. Tool Materials and Surface Engineering for Metal Forming Applications.
4. Society of Manufacturing Engineers. Stamping Die Design, Pressworking, and Production Engineering Practices.
5. ISO 9001. Quality Management Systems—Requirements.
6. ISO 12100. Safety of Machinery—General Principles for Design and Risk Assessment.
7. Manufacturer-provided product information for progressive molds, stamping dies, hardware parts, and stamping automation equipment.
Product: Progressive molds for automotive parts
Previous Post
Advanced Stamping Automation Equipment for Efficient Metal Forming Production
Next Post
Long-Stroke Multi-Stage Progressive Dies for High-Precision Sheet Metal Forming
Our Products.
Start Your Business with an OEM Manufacturer Right Here!

Provide global customers with complete turn-key solutions
through
innovation!
QUICK LINKS
CONTACT INFO.
-
 +86-139 1308 8972
-

-
 No. 118 Yexin Road, Wujiang Economic Development Zone, Suzhou, China
Copyright © Suzhou Shuangqisi Mold Equipment Co., Ltd. All Rights Reserved. Custom Stamping Die Metal Stamping Die Manufacturers
