 English
 Español
 Deutsch
-

Long-Stroke Multi-Stage Progressive Die Automatic Strip Feed Progressive Die Long Travel Follow on Stamping Tool for Sheet Metal Hardware Press Moulding
Long-Stroke Multi-Stage Progressive DieOur custom ...
-

Progressive Stamping Die for Connector & Terminal Parts High Speed Progressive Stamping Die Precision Metal Hardware Stamping Tool mold for Connector Terminal Parts Automotive Components
Progressive Stamping Die for Connector & Termi...
-
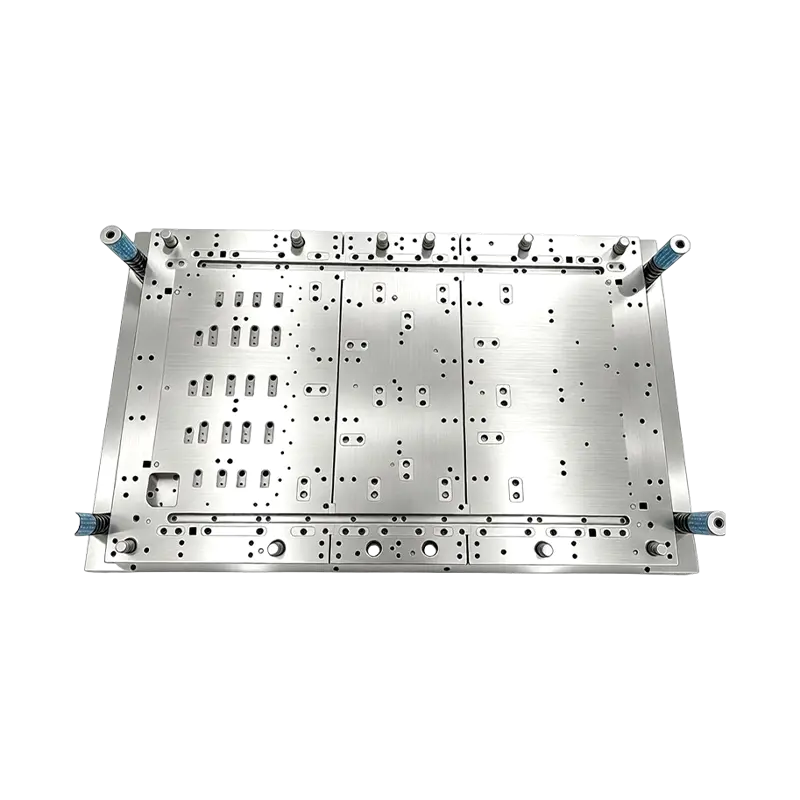
Multi-Station Progressive Stamping Die with Carbide Inserts Custom Multi Station Progressive Stamping Die Carbide Insert Metal Stamping Mold Tool for Equipment Appliances Device Hardware
High Speed Metal Stamping Tool for Precise Equipme...
-
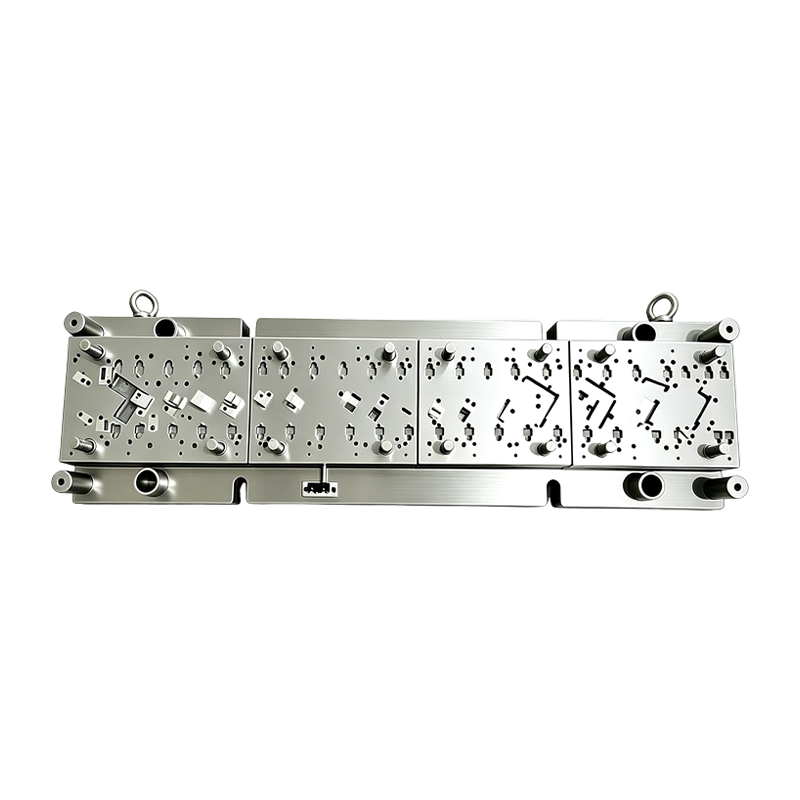
High Speed Progressive Stamping Die Sheet Metal Follow on Press Tool
Multi-operation Metal Stamping Tool for Continuous...
-
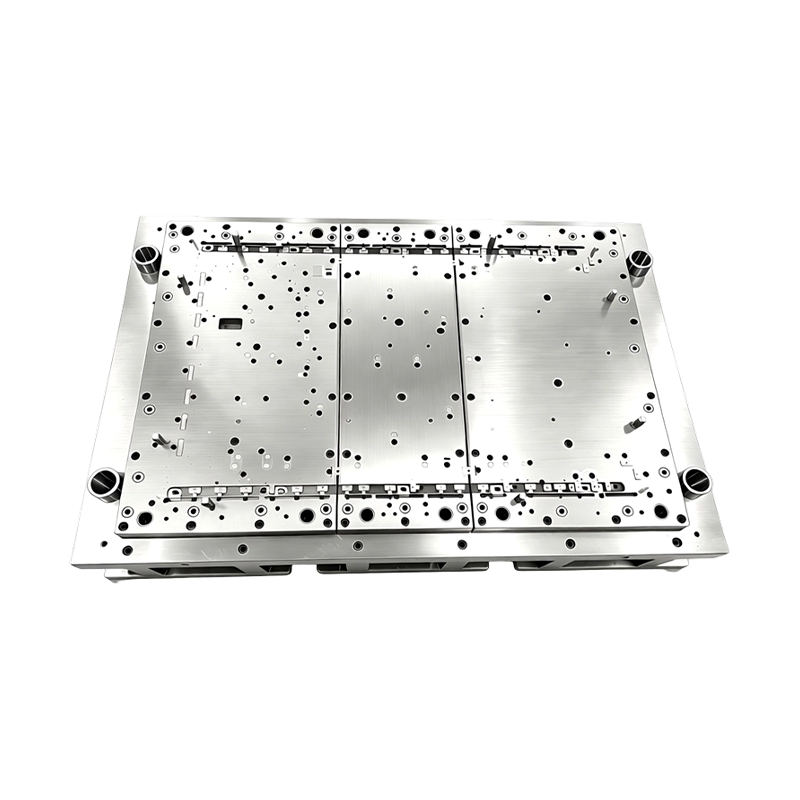
High Precision Stamping Die Multi Station Hardware Progressive Mold Tooling
Precision Metal Stamping Tool for Automotive &...
-
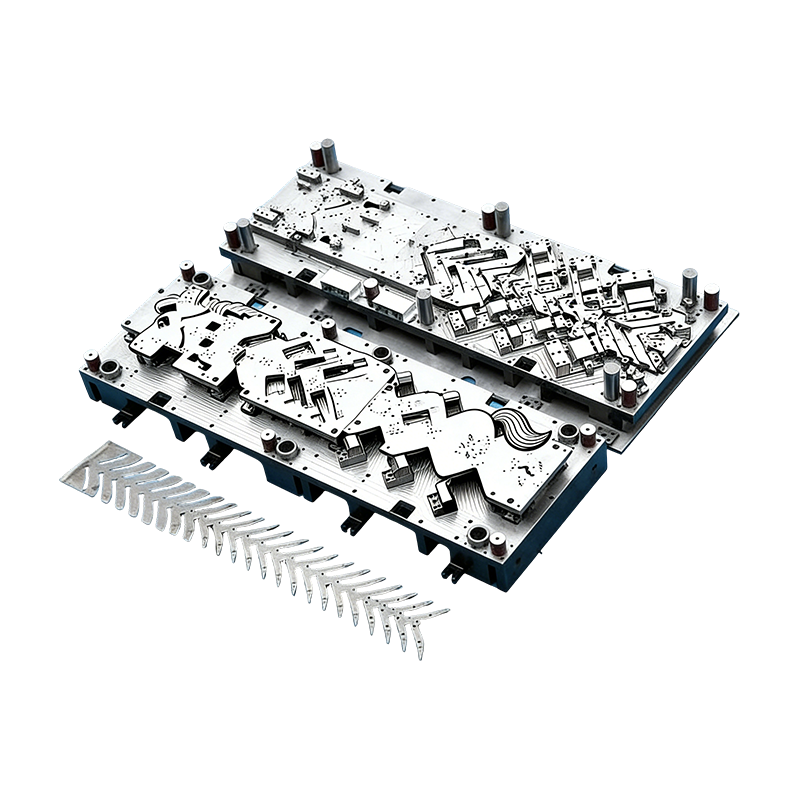
Progressive molds for automotive parts
This Continuous mold for automotive motor housing ...
- E-mail us: [email protected]
- Call us: +86-139 1308 8972

Wang Xinyue – After-Sales Support Supervisor
Home / Author / Wang Xinyue – After-Sales Support Supervisor / Long-Stroke Multi-Stage Progressive Dies for High-Precision Sheet Metal Forming
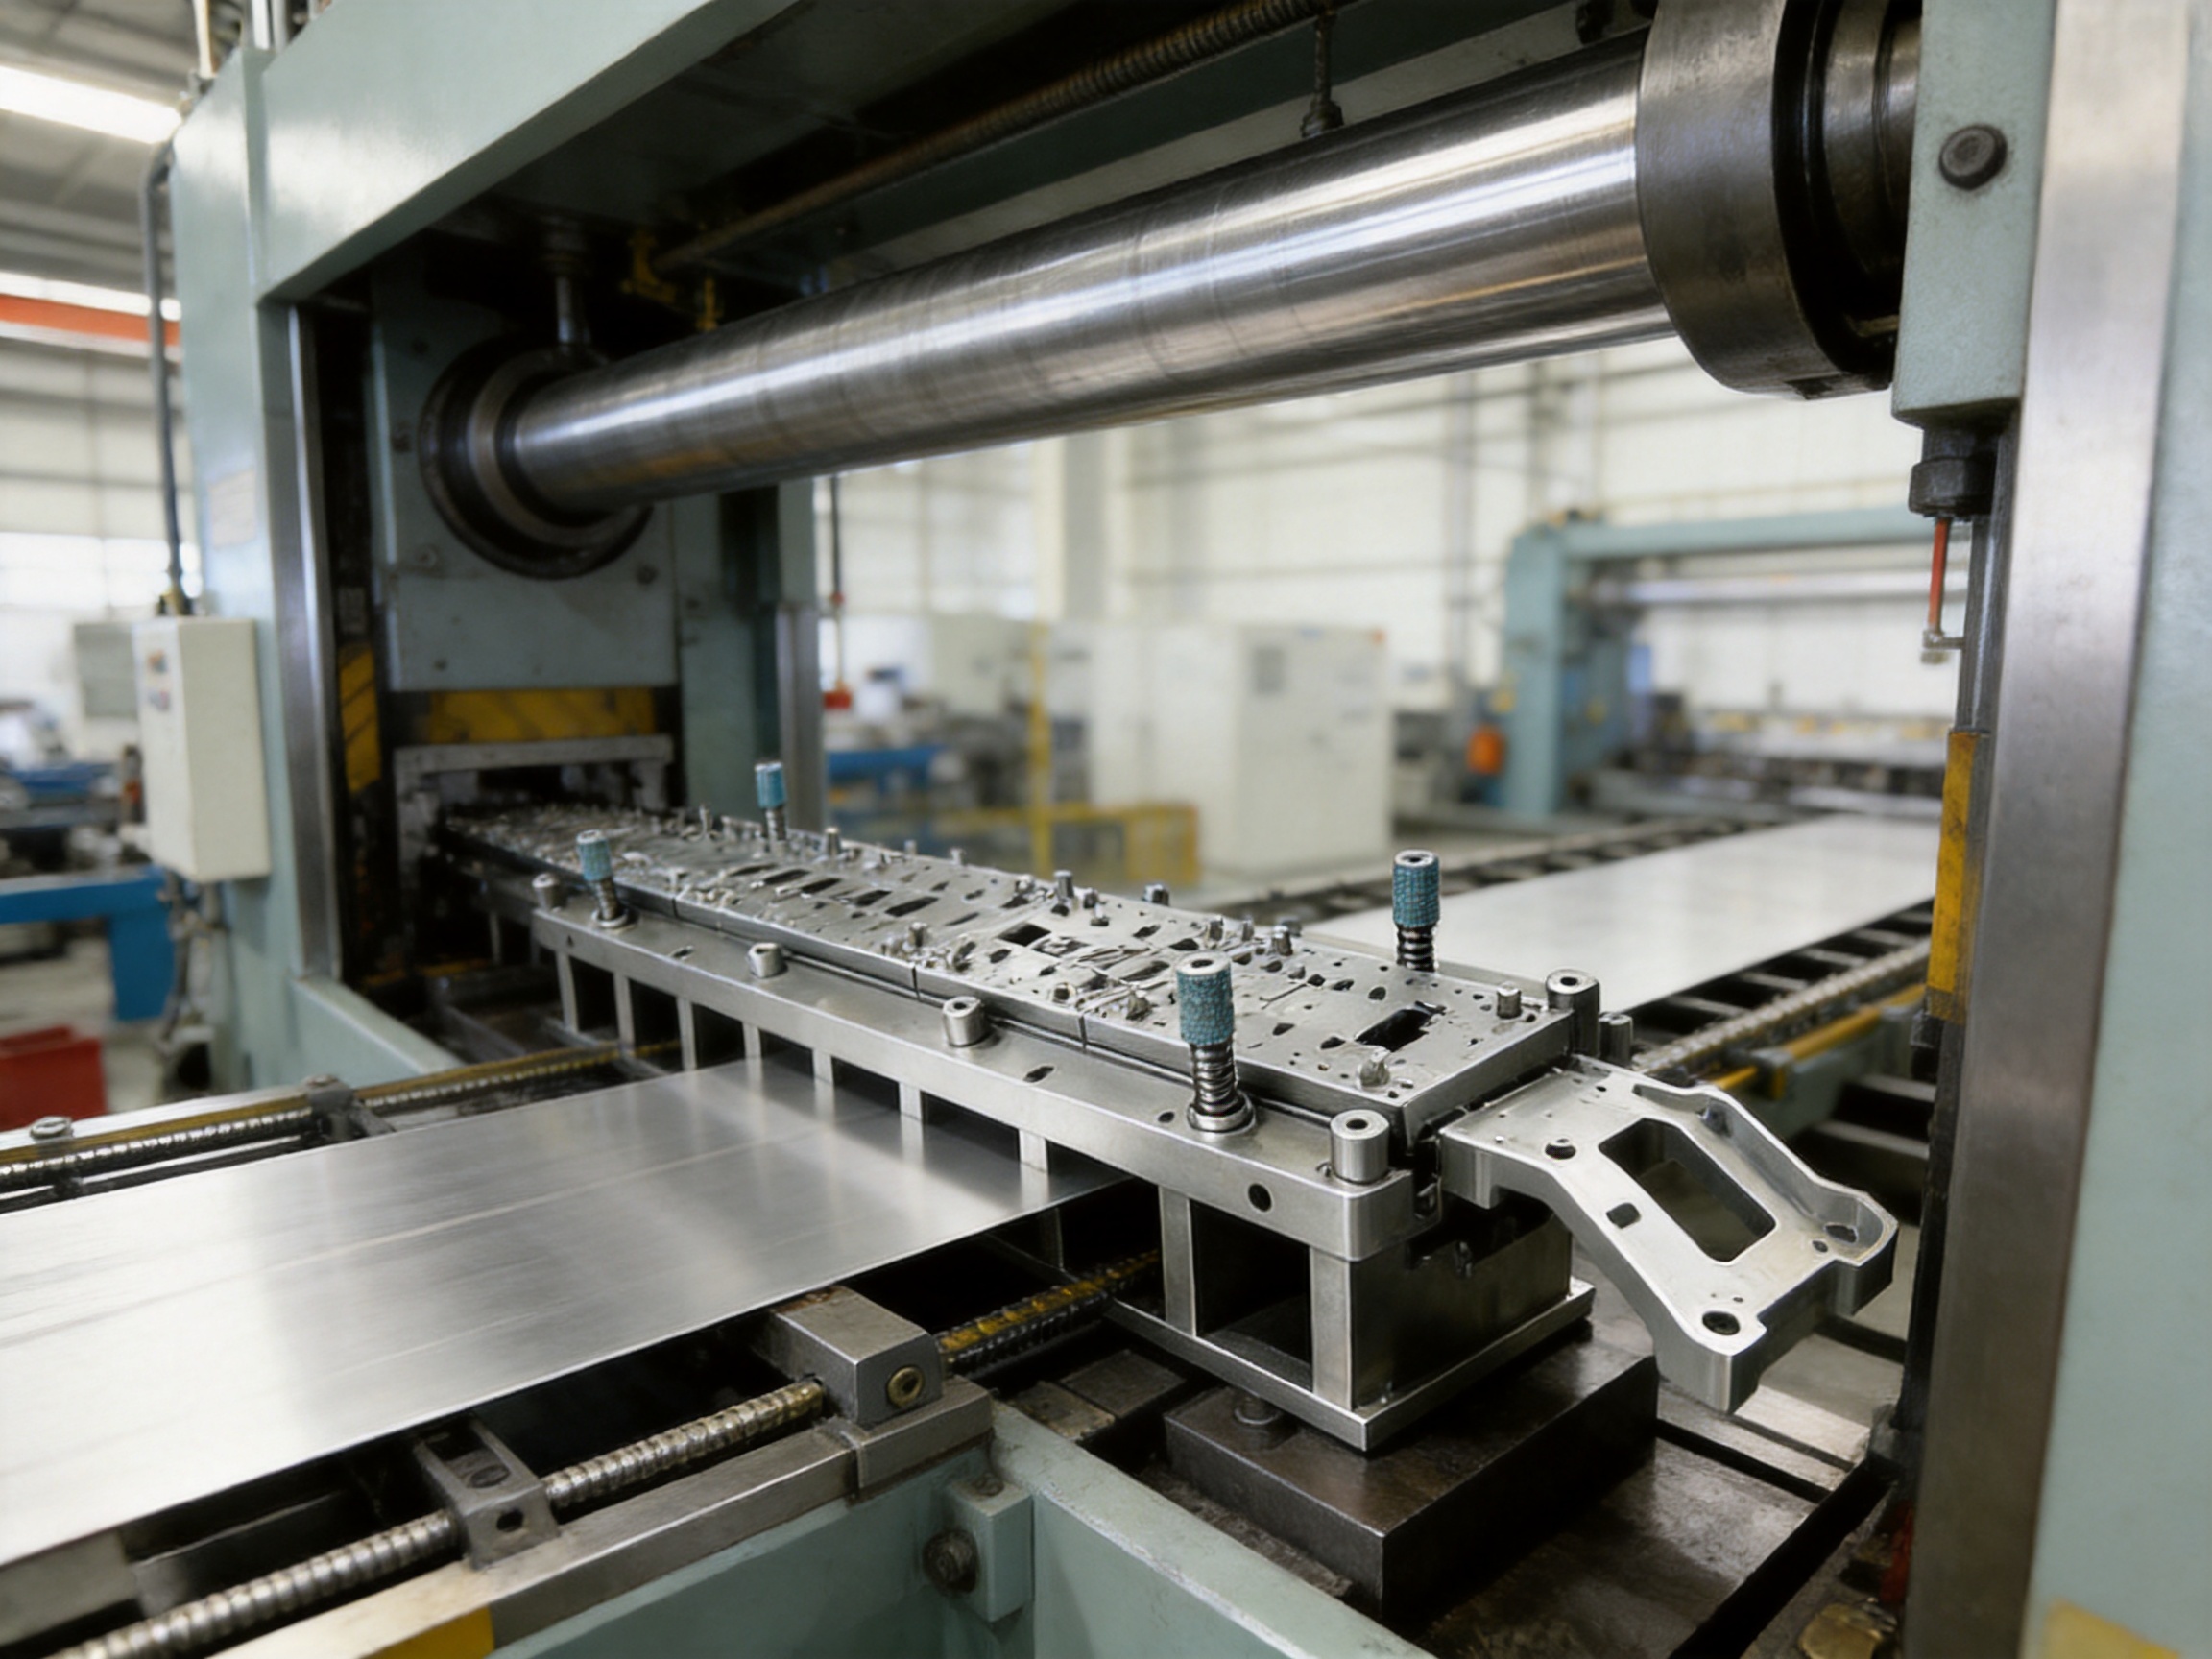
Long-Stroke Multi-Stage Progressive Dies for High-Precision Sheet Metal Forming
2026-10-06
Content
- 1 Introduction
- 2 What Is a Long-Stroke Multi-Stage Progressive Die?
- 3 Why Complex Sheet Metal Parts Require an Extended Die Layout
- 4 Core Product Advantages
- 5 Long-Strip Stability and Feed Accuracy
- 6 Heavy-Duty Die Construction
- 7 Modular Forming Inserts for Maintenance and Modification
- 8 Scrap Removal and Finished-Part Ejection
- 9 Application Areas
- 10 Engineering and Manufacturing Process
- 11 Manufacturing Strengths and Integrated Capability
- 12 Advantages Over Conventional and Competing Approaches
- 13 Quality, Cost, and Production Considerations
- 14 Recommended Customer Collaboration
- 15 Conclusion
- 16 Questions and Answers
- 16.1 What type of parts is suitable for a long-stroke multi-stage progressive die?
- 16.2 How many stations can the die include?
- 16.3 Why are pre-bending and final bending separated?
- 16.4 Can the die process high-strength steel or stainless steel?
- 16.5 How does the die prevent strip twisting and misalignment?
- 16.6 What happens if only one forming station needs adjustment?
- 16.7 How is stamping scrap removed?
- 16.8 How are finished parts removed from the die?
- 16.9 What manufacturing equipment supports the die production process?
- 16.10 Can the supplier provide stamping automation as well as the die?
- 16.11 What information should be supplied before requesting a quotation?
- 17 References
- 18 Product: Long-Stroke Multi-Stage Progressive Die Automatic Strip Feed Progressive Die Long Travel Follow on Stamping Tool for Sheet Metal Hardware Press Moulding
Introduction
Modern automotive, electric vehicle, electrical, and industrial products increasingly depend on sheet metal components with complicated three-dimensional geometries. A single part may require piercing, lancing, embossing, offset forming, multiple bends, coining, restriking, and final blanking. Producing these features with separate tools can increase handling, labor, floor space, and dimensional variation. A long-stroke multi-stage progressive die offers a more integrated solution by combining numerous forming operations into one continuous, automatic production process.
The long-stroke multi-stage progressive die described in this article is designed for complex sheet metal hardware that must be manufactured accurately and repeatedly at high production volumes. Its extended die layout provides sufficient space for multiple forming stations, while its strip-guiding, pilot-positioning, modular insert, and scrap-management systems help maintain stable operation throughout the entire progression.
Unlike a conventional short progressive die intended primarily for simple blanking or a limited number of bends, this type of tool is engineered around complex part development. The strip advances through a carefully planned sequence of operations. Each station performs a controlled task, allowing the final component to emerge with its required shape, holes, embosses, offsets, and bend angles in one automated run.
The result is a production system that can reduce secondary operations, improve consistency, shorten handling time, and support stable manufacturing for automotive brackets, electric vehicle hardware, electrical connectors, structural shields, appliance components, and other precision sheet metal parts.
Long-Stroke Multi-Stage Progressive Die Automatic Strip Feed Progressive Die Long Travel Follow on Stamping Tool for Sheet Metal Hardware Press Moulding
What Is a Long-Stroke Multi-Stage Progressive Die?
A progressive die is a stamping tool containing several workstations arranged along the direction of strip travel. A coil of sheet metal is fed into the die at a fixed pitch. At every press stroke, the strip moves forward by one pitch, and each station performs a specific operation on the portion of material positioned there. As the strip progresses, the partially formed features accumulate until the finished part is separated at the final station.
The term “long-stroke” refers to the extended working length and the ability to accommodate a large number of forming operations along the strip path. A long die body may include eight, fifteen, twenty, or more stations, depending on the part geometry, material, production volume, and required process sequence. The extended configuration is especially valuable when a component has several bends that cannot be formed reliably in a single hit.
Typical operations may include:
Pilot piercing for accurate strip registration.
Initial piercing and hole-making.
Lancing and partial separation.
Embossing and bead formation.
Pre-bending and staged bending.
Offset and step forming.
Restriking and coining.
Final sizing and calibration.
Blanking and part separation.
Instead of asking one station to complete a difficult bend or deep feature, the tool distributes the work across multiple stations. This controlled progression lowers forming shock, improves material flow, and gives the designer more opportunities to compensate for springback and dimensional variation.
Why Complex Sheet Metal Parts Require an Extended Die Layout
Simple flat brackets can often be made with a short progressive die or a single-operation stamping tool. However, complex components create several technical challenges. A part may include bends in different directions, narrow flanges, formed ribs, raised bosses, close-tolerance holes, and intersecting features. If too many operations are concentrated in one station, the material may wrinkle, crack, twist, or spring back beyond the required tolerance.
An extended layout creates room for a more gradual process. The strip can be pierced before forming, formed in small increments, stabilized with pressure pads, and calibrated near the end of the sequence. The distance between stations also makes it easier to manage material flow and prevent one operation from interfering with another.
The long-stroke design is particularly useful for components that must maintain a controlled relationship between holes and formed surfaces. For example, an automotive mounting bracket may require several piercings, two offset bends, an embossed reinforcement, and a final flange. If these features are produced without sufficient sequencing, the forming force can distort previously pierced holes or shift the reference position of the part. A longer process allows the design team to establish pilots and reference features early, then use them to control subsequent stations.
This approach also supports parts made from high-strength steel, stainless steel, copper alloys, and other materials with challenging forming behavior. Although material selection and process conditions remain critical, staged deformation provides greater control than a single aggressive forming operation.
Core Product Advantages
One Continuous Production Process
The most important advantage is process integration. Piercing, bending, forming, coining, and blanking can be completed inside one progressive tool. Once the die has been installed and the strip feeder has been set, the press can produce parts continuously with limited manual intervention.
Combining operations reduces the need to transfer parts between separate machines. It can also reduce the risks associated with manual repositioning, inconsistent secondary bending, and intermediate storage. For high-volume production, the reduction in handling can have a direct effect on labor cost, cycle stability, and overall equipment utilization.
Improved Dimensional Repeatability
Every station is designed around a defined operation and a controlled reference system. Multiple pilot pins, guide rails, pressure pads, and strip lifters help keep the material correctly positioned as it travels through the die. This is important because forming forces can cause a long strip to lift, twist, or move laterally if it is not properly supported.
Stable registration helps maintain the location of holes, bends, embosses, and cut edges from part to part. It also supports more consistent relationships between features, which is often more important than the dimensional accuracy of any single feature.
Controlled Springback Compensation
Springback is a major concern when forming high-strength or work-hardened materials. After the forming load is released, the metal attempts to return partially toward its original shape. The amount of springback depends on material properties, thickness, bend radius, grain direction, tooling condition, and forming history.
The multi-stage design addresses this issue by separating pre-bending, final bending, restriking, and coining into appropriate stations. A pre-bend can prepare the material without applying the entire deformation at once. A final bend can then bring the flange closer to the target angle, while a restrike or coining operation can improve repeatability and reduce residual variation.
This staged process is generally more predictable than making a sharp bend in one operation. It also provides flexibility during tryout because individual stations can be adjusted without redesigning the complete die.
Reduced Secondary Operations
Secondary operations increase production complexity. A stamped blank may need to be transferred to another press for bending, then manually inspected, cleaned, and packed. Each additional stage introduces setup time, handling cost, and the possibility of damage or variation.
A long-stroke progressive die can eliminate or reduce many of these follow-up activities. Depending on the part design, the finished product can leave the tool ready for inspection, assembly, or a limited downstream operation. This is especially valuable when a customer requires high output and stable delivery of formed components.
Efficient Use of Material and Equipment
Progressive stamping uses a continuous strip and a planned carrier layout. The strip can be designed to maximize material utilization while retaining enough carrier strength for reliable feeding. An experienced process engineering team can balance pitch, bridge width, part orientation, piercing sequence, and scrap separation.
Because multiple operations are performed in a single press cycle, the production line may require fewer machines than a collection of individual forming tools. This can reduce equipment footprint and simplify production planning. The actual economic benefit depends on part volume, material cost, tool complexity, press capacity, and cycle requirements, but the integrated concept is particularly attractive for repeat orders and long production runs.
Long-Strip Stability and Feed Accuracy
A long progressive die requires more than a longer base. The strip must remain stable over the complete working length, even after it has been pierced, bent, embossed, and partially separated. Poor strip support can lead to misfeeds, pilot damage, tool crashes, inconsistent bends, and part deformation.
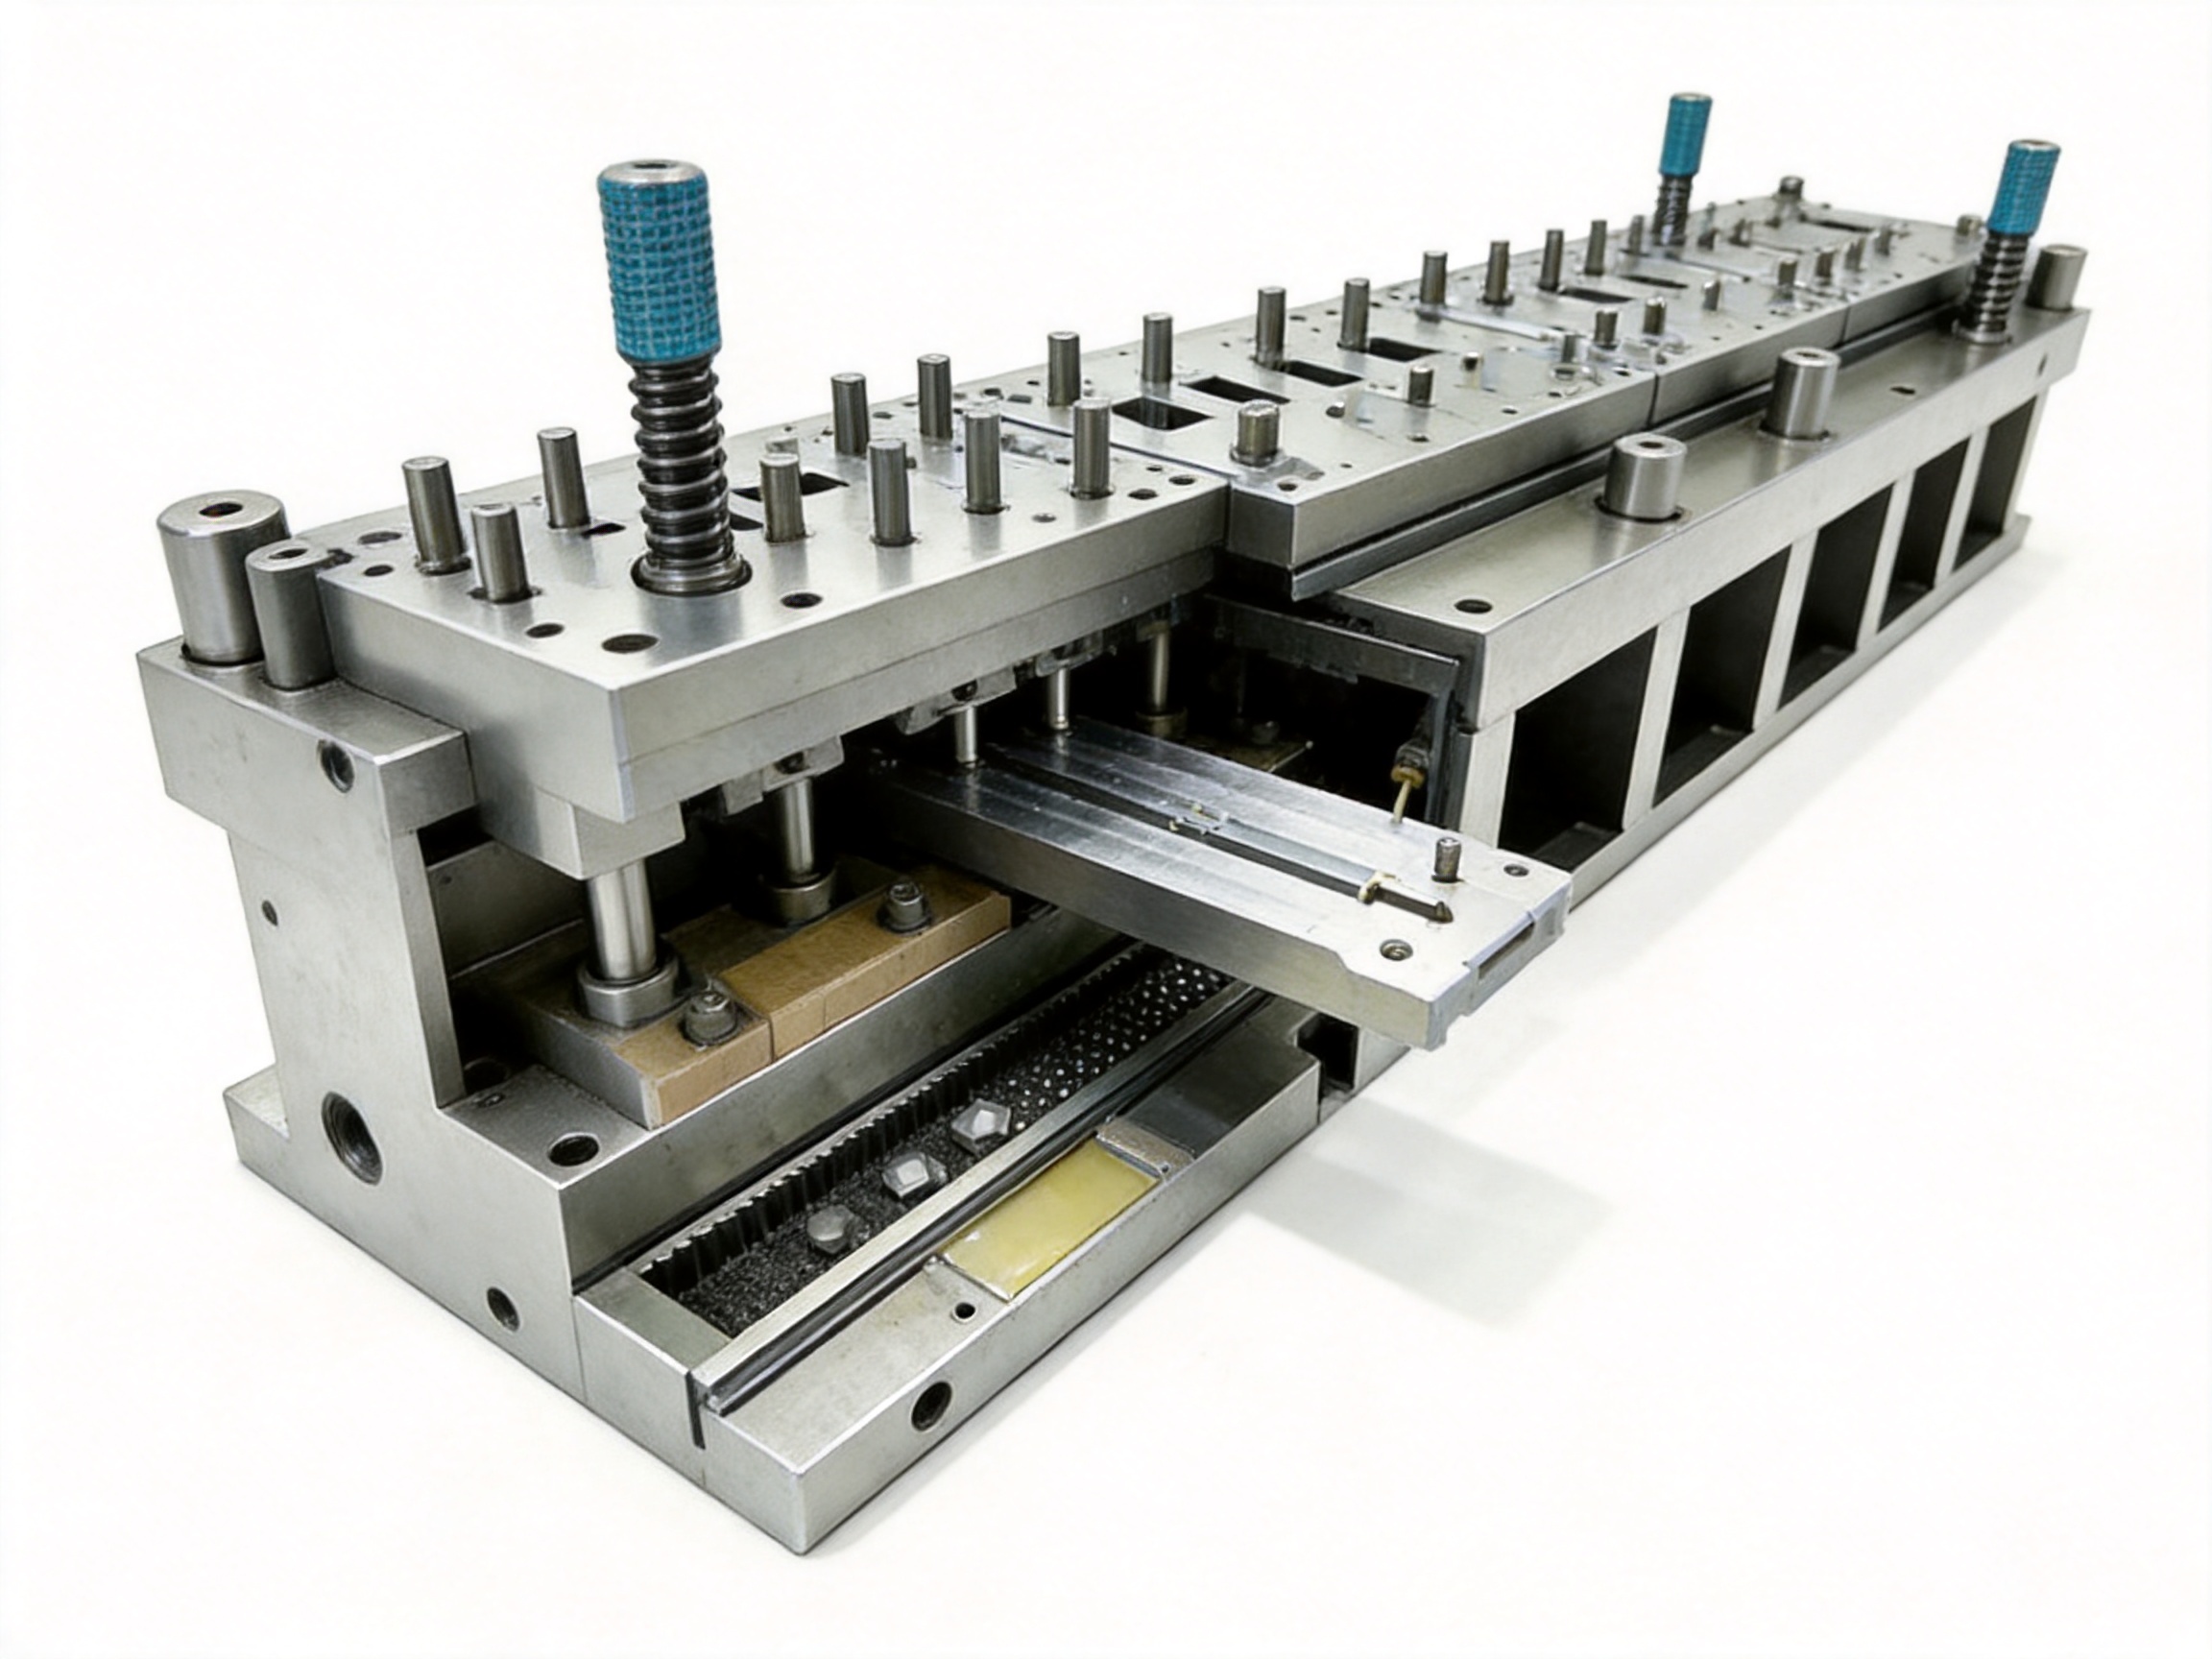
The described design uses multiple support and registration elements, including precision pilot pins, strip lifters, pressure pads, and guide rails. Pilot pins enter previously prepared holes to establish accurate positional references. Their locations can be distributed along the strip path so that registration is maintained at several points rather than relying only on one local reference.
Strip lifters help raise the material during die opening and support it during the feeding motion. Pressure pads control movement during forming and cutting. Guide rails help limit lateral movement and can be adapted to the material width and carrier design. Together, these features create a more controlled travel path through the extended die.
Long-strip support is especially important after the strip has undergone several forming operations. A carrier that was flat at the entry side may develop local curvature or torsion as features are formed. The die must therefore account for the changing shape of the strip rather than treating it as a simple flat band throughout the process.
Heavy-Duty Die Construction
An extended die body is exposed to repeated forming loads over a greater working length than a compact tool. If the base lacks rigidity or the guide system is insufficient, deflection can affect cutting clearance, bend depth, and alignment. The result may be premature wear or dimensional drift during long production runs.
The die is built around a stress-relieved and precision-ground base. Stress relief helps reduce the risk of movement caused by internal material stress after machining. Precision grinding establishes accurate reference surfaces for the die components and supports consistent assembly.
Multi-point guide pillar sets are distributed along the die length rather than being positioned only at the four corners. This arrangement helps maintain parallelism across the working area. It also reduces the risk of a “banana effect,” in which an extended die opens or deflects unevenly under load.
Uniform guidance is essential for maintaining the relationship between punches, dies, inserts, pressure pads, and pilots. When a tool is operating at high frequency, even a small alignment problem can create accelerated wear. A rigid structure with distributed guidance helps protect the tool and contributes to stable operation over millions of press cycles, provided that the tool is correctly installed, lubricated, maintained, and operated within its design limits.
Modular Forming Inserts for Maintenance and Modification
Complex progressive dies must often be adjusted during tryout. Material batches can differ slightly in strength or thickness, and customer design revisions may require a change to one bend, hole, flange, or emboss. A fully integrated, non-modular die can be expensive and time-consuming to modify in such situations.
Modular forming inserts provide a practical alternative. Each important bending or forming station can use an independently replaceable insert. If a bend angle needs correction, the affected insert can be reworked or replaced without disassembling and remanufacturing the entire die body.
This construction offers several advantages:
Faster adjustment during tool tryout.
Reduced maintenance downtime.
Lower cost when a localized component is damaged.
Easier implementation of engineering changes.
Improved access to wear-prone working components.
More convenient storage of replacement inserts.
Modularity also supports different production phases. A tool may initially use tryout inserts that allow rapid tuning, followed by hardened production inserts after the process has been validated. The specific insert materials and treatments should be selected according to the workpiece material, forming load, cutting condition, and expected production volume.
Scrap Removal and Finished-Part Ejection
Multi-stage progressive dies create scrap at several stations. Pierced slugs, trimmed sections, carrier remnants, and other waste must be removed continuously. If scrap accumulates inside the die, it can obstruct the strip, damage punches, interfere with sensors, or cause an unexpected stoppage.
Internal scrap chutes can direct slugs toward designated discharge points. Their design must consider the size and shape of the scrap, the direction of gravity, press speed, lubrication, and accessibility for cleaning. Where necessary, air assistance or other discharge methods can be incorporated to improve reliability.
At the final station, the completed three-dimensional part can be ejected using an air blow, mechanical kicker, or a combination of methods. The selected solution depends on the part’s shape, weight, orientation, surface sensitivity, and downstream handling system. A controlled ejection process helps prevent finished parts from remaining in the die or colliding with the next workpiece.
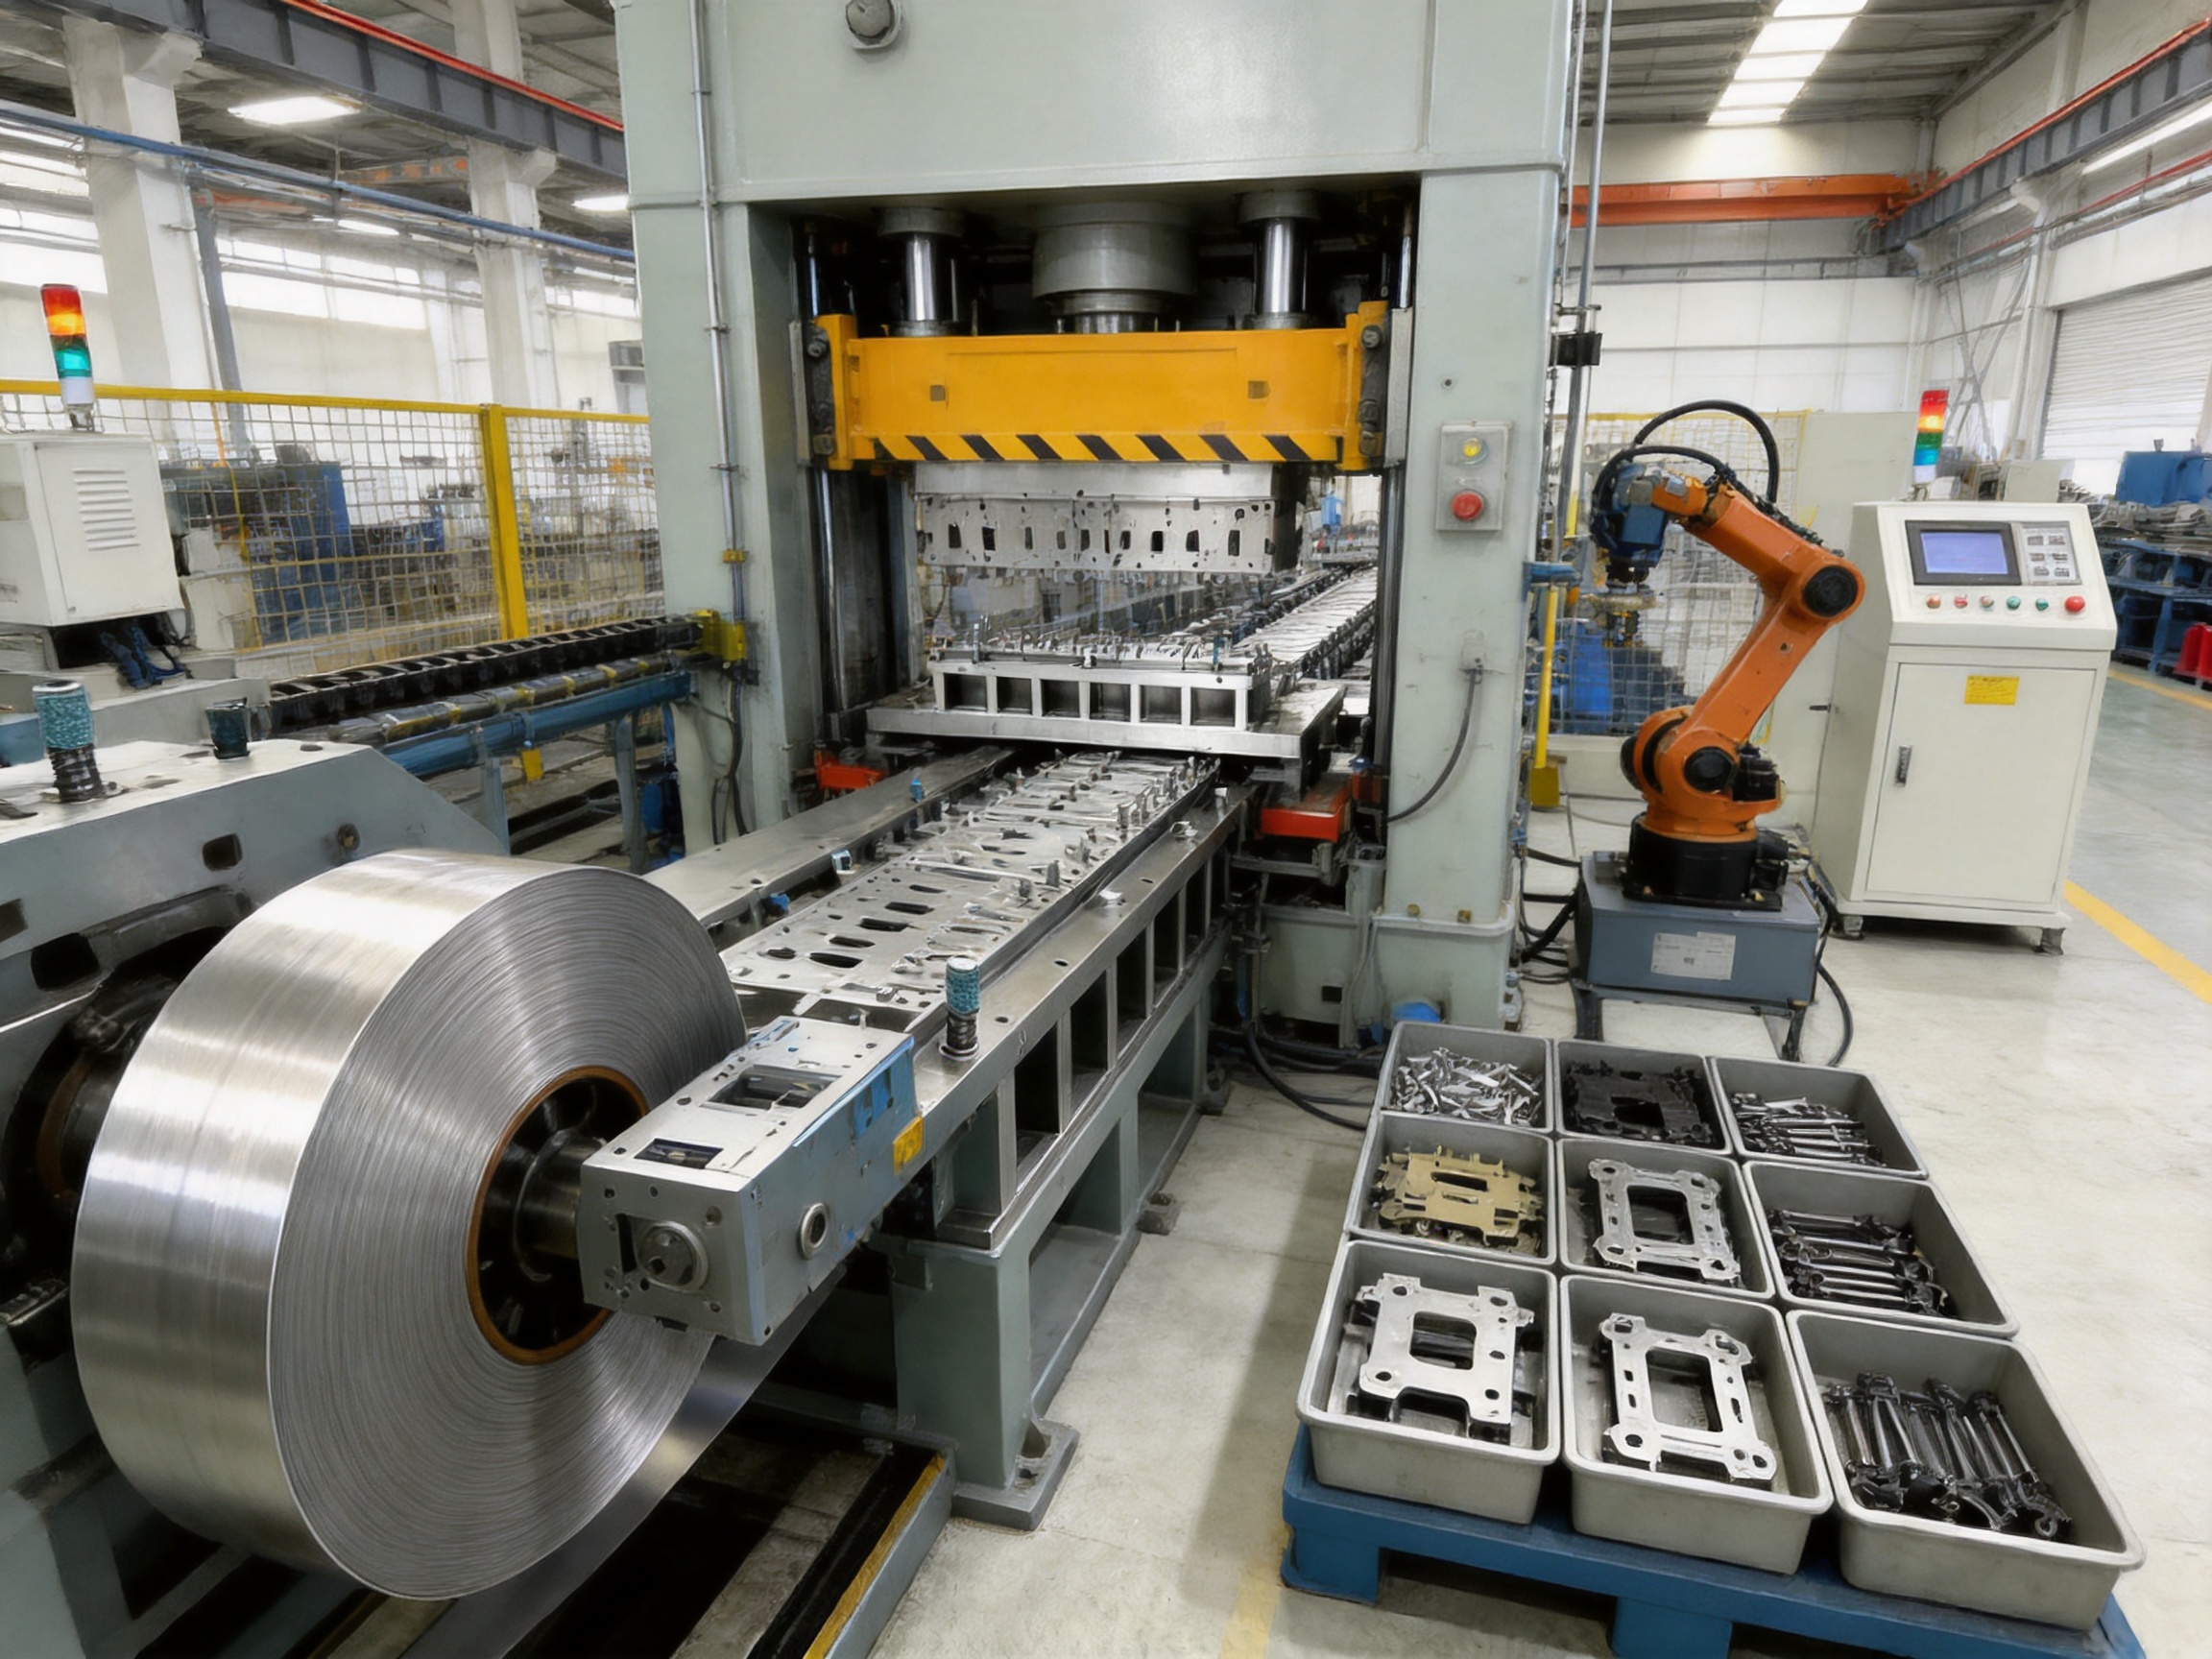
Finished parts may be transferred to a conveyor, collection container, inspection station, or automated assembly line. This creates a continuous production path from coil stock to formed component and supports the integration of stamping automation equipment.
| System Area | Typical Function | Production Benefit |
|---|---|---|
| Extended station layout | Distributes piercing, bending, forming, restriking, and blanking operations | Enables complex three-dimensional parts in one progressive process |
| Multiple pilot pins | Maintains strip registration at several locations | Improves feature-to-feature accuracy and feed stability |
| Strip lifters and guide rails | Supports and controls the strip during opening and feeding | Reduces lifting, twisting, and misalignment |
| Modular forming inserts | Allows individual stations to be adjusted or replaced | Shortens maintenance and engineering-change time |
| Restriking and coining stations | Calibrates formed surfaces and bend angles | Reduces springback variation |
| Scrap chutes | Routes slugs and waste away from working areas | Reduces jamming and unplanned stoppages |
| Air or mechanical ejection | Removes finished parts from the final station | Supports continuous automated collection |
Application Areas
Automotive Components
Automotive platforms use large quantities of formed sheet metal hardware. Seat brackets, door clips, hinge components, brake-line clips, sensor brackets, reinforcement plates, and connector housings often require several holes and bends in a compact part.
The progressive die can be configured to produce these features in a controlled order. Piercing may be completed before the main bends, while embosses or ribs can be introduced before final calibration. The result is a repeatable component suitable for high-volume vehicle production, subject to customer drawings, material specifications, and validation requirements.
Electric Vehicle and New Energy Hardware
Electric vehicles and energy systems require specialized brackets, clips, shields, busbar supports, battery module components, charging connector parts, and cooling-system hardware. These parts may need accurate mounting holes, electrical clearance features, formed edges, and controlled flatness.
A long-stroke tool can combine these features while maintaining a consistent strip reference. It can also be adapted for copper alloys, stainless steel, coated steel, and other materials commonly used in electrical and new energy applications. Proper attention must be given to burr direction, surface protection, conductivity, and cleanliness when the component is part of an electrical assembly.
Electrical and Electronic Products
Relay frames, terminal blocks, switch housings, connector shells, EMI shielding parts, and PCB mounting clips often contain small but complicated features. Their performance can depend on contact position, spring geometry, insertion force, and dimensional stability.
Progressive forming makes it possible to create these features in a repeatable sequence. Small lances, slots, tabs, and bends can be placed at dedicated stations, while final forming and sizing operations help control the finished geometry.
Telecommunications and Data Center Equipment
Server chassis brackets, rack hardware, cable management clips, shielding frames, and heat-sink mounting parts often require a combination of flatness, stiffness, and accurate mounting features. Progressive dies can support efficient production of these components and reduce the number of manual forming steps.
Home Appliances and Industrial Automation
Appliance brackets, compressor mounting plates, drum supports, hinge components, motor support structures, sensor brackets, actuator clips, and conveyor hardware are additional applications. Many of these parts are produced in substantial quantities and benefit from a dedicated tool that provides consistent geometry with minimal handling.
Aerospace-Related Sheet Metal Components
Lightweight bracket preforms, clip fasteners, and structural sheet metal components may also be produced using progressive technology when the part geometry and material are suitable. Aerospace-related production requires strict control of material traceability, process documentation, inspection, and customer-specific approvals. The die itself must be validated within the applicable quality system and part qualification process.
Engineering and Manufacturing Process
1. Product Drawing and Feasibility Review
Tool development begins with a review of the customer’s part drawing, three-dimensional data, material specification, thickness, tolerances, surface requirements, annual volume, and press limitations. The engineering team evaluates whether the part is suitable for progressive stamping and identifies difficult features such as narrow flanges, reverse bends, deep embosses, close-tolerance holes, and areas vulnerable to cracking.
At this stage, the team also considers the strip direction, carrier design, material utilization, feed pitch, press tonnage, die height, shut height, and coil-handling requirements. Early feasibility analysis helps prevent avoidable changes after machining has started.
2. Process Planning and Station Development
The part is divided into a logical series of operations. A typical sequence may begin with pilot holes and primary piercings, followed by lancing, embossing, pre-bending, intermediate forming, final bending, restriking, coining, trimming, and blanking.
The order is not universal. It must be selected according to material flow and the interaction between features. A hole may need to be pierced before a bend for positional accuracy, or after a bend if piercing it earlier would distort the hole. Similarly, a flange may require support from an adjacent feature before final sizing can be completed.
Simulation, engineering calculations, and practical experience are used to assess forming feasibility. The goal is to create a sequence that balances accuracy, tool life, press capacity, production speed, and ease of maintenance.
3. Die Design
The die design incorporates the complete station layout, guide system, pilot locations, pressure pads, lifters, punches, inserts, scrap routes, sensors, and ejection method. The extended base must be designed with adequate stiffness and access for assembly, inspection, cleaning, and maintenance.
Clearances are selected according to material type, thickness, operation, and required edge quality. Bend radii, forming radii, reliefs, and escape features are considered to prevent interference. Wear components are made accessible wherever possible, and replaceable inserts are used for stations likely to require adjustment.
4. Precision Machining
Manufacturing uses precision machining equipment appropriate for the required tolerances and surface quality. CNC machining centers produce die plates, holders, forming blocks, and structural components. Wire electrical discharge machining can be used for intricate profiles, narrow slots, complex punches, and close-tolerance cutting sections.
Grinding operations establish accurate working surfaces and improve the fit between mating components. The manufacturer’s equipment includes imported wire-cutting machines, CNC machining centers, more than ten grinding machines of different sizes, and punch presses ranging from 80 to 400 tons. This combination supports internal control over important manufacturing steps and allows the team to match the tool design to appropriate press capacity.
Machining quality is not limited to the visible working edge. Parallelism, flatness, perpendicularity, hole location, insert seating, and guide alignment all contribute to the final performance of the assembled die. Careful inspection between operations helps identify deviations before they affect later components.
5. Assembly and Tryout
After machining, the die components are cleaned, inspected, and assembled. Guide pillars, plates, punches, inserts, pressure pads, pilots, lifters, and scrap-management parts are installed according to the assembly drawings.
Tryout begins with controlled press testing. The team checks feeding, strip registration, station timing, cutting action, forming behavior, ejection, and scrap discharge. Initial samples are measured against the part drawing. If a bend angle, flange height, hole position, or formed profile needs correction, the relevant modular insert or station component can be adjusted.
Tryout is an important stage for complex long-stroke dies because the interaction of multiple operations can produce effects that are difficult to predict entirely from drawings. Experienced operators and debugging personnel can identify whether a problem originates from material flow, clearance, pressure, timing, strip support, or local forming geometry.
6. Validation and Production Preparation
Once the tool produces acceptable samples, the process is reviewed for repeatability. The team checks whether the strip feeds consistently, whether scrap exits properly, whether parts are ejected without damage, and whether the die can operate at the planned production conditions.
Documentation may include inspection records, sample approval information, maintenance recommendations, spare-part lists, press settings, lubrication requirements, and operating instructions. These documents help the customer establish a controlled production process and support future troubleshooting.
Manufacturing Strengths and Integrated Capability
Suzhou Shuangqisi Mold Equipment Co., Ltd. combines stamping die design, tool manufacturing, stamping production capability, and automation equipment development. This integrated structure is significant because a progressive die cannot be evaluated separately from the press, feeder, coil system, sensors, ejection equipment, and production method that will operate it.
The company has approximately 60 technical staff and more than 15 years of experience in the mold industry. Its equipment includes wire cutting machines, CNC machining centers, multiple grinding machines, and 25 punch presses with capacities from 80 to 400 tons. These resources support the development of tools for different part sizes, materials, and forming requirements.
The organization also established Suzhou Keshuang Intelligent Technology Co., Ltd. in 2016 to focus on stamping automation equipment. This enables the business to provide more than a standalone die. Depending on customer requirements, it can support a broader turnkey solution involving stamping molds, automatic feeding, part handling, production equipment, and related process integration.
Such integration can simplify communication during a project. The die designer can consider the actual press and feeder conditions, while the automation team can account for part orientation, ejection, collection, and downstream handling. This reduces the risk of designing a tool that performs well in isolation but is difficult to integrate into the customer’s production line.
The company serves customers in servo drives, compressors, new energy vehicles, electrical products, and other industrial sectors. Its stated customers include Anter Group, Ousheng Electric, Dongbei Group, and Huichuan Technology. Experience across these fields supports practical understanding of formed hardware, precision requirements, production stability, and cost control.
Advantages Over Conventional and Competing Approaches
Compared with Single-Operation Dies
A single-operation die may have a lower initial design complexity, but it requires more equipment and handling when several operations are needed. The long-stroke progressive solution consolidates the sequence into one automated tool. This can reduce transfers, improve feature alignment, and lower the amount of work-in-process inventory.
Compared with Short Progressive Dies
Short progressive dies are effective for flat washers, simple clips, basic terminals, and parts with limited forming requirements. They are less suitable when a part needs many bends, gradual forming, or repeated calibration. The extended layout of a long-stroke tool provides additional stations for pre-forming, springback control, restriking, and final sizing.
Compared with Manual Secondary Bending
Manual bending can be flexible for prototypes or very low-volume work, but it is more dependent on operator skill and can create variation in angle, position, and orientation. Integrating the bending operations into the progressive die improves repeatability and supports higher production volumes.
Compared with Non-Modular Tool Construction
A non-modular tool can be difficult to revise when one feature changes. Modular inserts isolate adjustments and wear areas. This can reduce downtime and make engineering changes more manageable throughout the product life cycle.
Compared with Basic Strip Feeding
Long-strip forming requires stronger control than simple feeding into a short blanking tool. Multiple pilots, lifters, pressure pads, and guide rails help maintain accuracy after the strip has experienced repeated deformation. This is a major performance advantage for extended dies with many stations.
Quality, Cost, and Production Considerations
The economic value of a progressive die depends on the complete production scenario rather than the purchase price of the tool alone. Important factors include annual volume, material utilization, press availability, labor cost, cycle rate, secondary operations, maintenance, scrap, and expected service life.
A long-stroke multi-stage die generally requires more engineering and a higher initial investment than a simple tool. However, the investment can be justified when the component is produced repeatedly and the integrated process eliminates multiple operations. The return becomes stronger when the part has a high annual demand and requires stable dimensional control.
Material utilization should be evaluated during strip-layout development. The carrier must be strong enough for feeding, but unnecessary carrier width increases scrap. Part orientation and pitch must be balanced against forming access, pilot-hole placement, and tool strength.
Maintenance planning is also essential. The tool should be cleaned regularly, scrap paths should remain open, and wear components should be inspected according to production volume. Lubrication must be compatible with the material and customer requirements. Punches, cutting edges, pilots, guide components, springs, and forming inserts should be monitored for wear or damage.
When the tool is designed with replaceable inserts and accessible working components, maintenance can often be performed more efficiently. Preventive replacement of selected wear parts may be preferable to waiting for a failure that causes a press stoppage or affects product quality.
Recommended Customer Collaboration
The best results are achieved when the customer and die manufacturer cooperate from the beginning. The customer should provide accurate part data, material information, production targets, press specifications, quality standards, and downstream handling requirements.
Important questions include:
What is the material grade, thickness, coating, and temper?
What are the annual volume and expected production speed?
Which dimensions and features are critical to function?
What press capacity, bed size, shut height, and stroke are available?
Will the part be oiled, cleaned, plated, welded, or assembled after stamping?
How should finished parts be oriented and collected?
Are there customer-specific inspection, traceability, or validation requirements?
Clear answers allow the engineering team to develop a practical strip layout and avoid unnecessary tool complexity. They also help determine whether air ejection, mechanical transfer, conveyor collection, sensors, or additional automation should be included.
Conclusion
The long-stroke multi-stage progressive die is a high-value solution for complex sheet metal components requiring many sequential operations. Its extended station layout allows piercing, lancing, embossing, pre-bending, final bending, coining, restriking, and blanking to be coordinated in one continuous process.
Its principal advantages include integrated production, improved dimensional repeatability, controlled springback compensation, reduced secondary operations, stable long-strip feeding, modular maintenance, and efficient scrap and part handling. Multi-point guidance and a rigid die base help protect alignment across the extended working area, while replaceable forming inserts simplify tryout and future modification.
The manufacturing strength behind the product is equally important. With experienced technical personnel, wire-cutting and CNC machining resources, multiple grinding machines, press capacities from 80 to 400 tons, and dedicated stamping automation capability, Suzhou Shuangqisi Mold Equipment Co., Ltd. can support projects from die design through manufacturing, debugging, and production integration.
For automotive, electric vehicle, electrical, appliance, industrial automation, telecommunications, and other high-volume applications, this combination of long-stroke progressive forming and integrated automation can provide a more stable and economical alternative to multiple separate dies and manual secondary operations.
Questions and Answers
What type of parts is suitable for a long-stroke multi-stage progressive die?
The tool is suitable for sheet metal parts with multiple holes, bends, offsets, embosses, lances, formed ribs, and final blanking requirements. Typical examples include automotive brackets, electrical clips, connector housings, battery hardware, shielding parts, appliance supports, and industrial mounting components.
How many stations can the die include?
The extended working area can accommodate approximately eight to more than thirty stations, depending on the part geometry, material, forming sequence, press limitations, and customer requirements. The exact number is determined during process planning.
Why are pre-bending and final bending separated?
Separating the operations allows the material to be formed gradually. This reduces forming shock, improves material flow, and provides better control over springback. A later restriking or coining station can further calibrate the finished bend.
Can the die process high-strength steel or stainless steel?
It can be designed for high-strength steel, stainless steel, and other demanding materials when the material thickness, tensile properties, bend radii, press capacity, and tooling materials are properly evaluated. Final suitability should be confirmed through engineering analysis and tryout.
How does the die prevent strip twisting and misalignment?
Multiple pilot pins, guide rails, strip lifters, and pressure pads support and register the strip along its travel path. Their combined function helps control the strip after it has been pierced and progressively deformed.
What happens if only one forming station needs adjustment?
With modular forming inserts, the affected insert can be modified or replaced without rebuilding the complete die. This reduces adjustment time and simplifies maintenance and engineering changes.
How is stamping scrap removed?
Internal scrap chutes route pierced slugs and other waste toward designated discharge points. The specific design may use gravity, air assistance, or other methods depending on the scrap shape and die configuration.
How are finished parts removed from the die?
Finished parts can be ejected using an air blow, mechanical kicker, or a combined system. They may then be delivered to a conveyor, collection container, inspection station, or automated assembly process.
What manufacturing equipment supports the die production process?
The manufacturer uses imported wire-cutting machines, CNC machining centers, more than ten grinding machines of different sizes, and 25 punch presses ranging from 80 to 400 tons. These resources support precision machining, assembly, tryout, and production verification.
Can the supplier provide stamping automation as well as the die?
Yes. Through its associated automation capability, the company can provide stamping automation equipment and turnkey solutions that connect the die with feeding, handling, ejection, and related production equipment according to customer needs.
What information should be supplied before requesting a quotation?
Customers should provide the part drawing or three-dimensional model, material grade and thickness, tolerance requirements, annual volume, target cycle rate, press specifications, coil information, surface requirements, and downstream handling expectations. This information supports accurate feasibility analysis and quotation preparation.
References
1. User-supplied product specification: Long-Stroke Multi-Stage Progressive Die, automatic strip-feed progressive stamping tool.
2. User-supplied company profile: Suzhou Shuangqisi Mold Equipment Co., Ltd., manufacturing capabilities, equipment resources, technical personnel, and automation services.
3. ASM International, ASM Handbook, Volume 14B: Metalworking—Sheet Forming.
4. American Society of Mechanical Engineers, principles of mechanical power press operation and tooling safety.
5. Society of Manufacturing Engineers, sheet metal stamping process planning and progressive die engineering references.
6. Automotive Industry Action Group, quality planning and production-part approval principles for automotive components.
7. General engineering practice for progressive die design, strip layout, springback compensation, tool maintenance, and automated part handling.
Product: Long-Stroke Multi-Stage Progressive Die Automatic Strip Feed Progressive Die Long Travel Follow on Stamping Tool for Sheet Metal Hardware Press Moulding
Previous Post
Progressive Molds for Automotive Parts: Precision, Efficiency, and Integrated Stamping Solutions
Next Post
High-Precision Car Seat Stamping Parts for Safe, Durable Automotive Seat Structures
Our Products.
Start Your Business with an OEM Manufacturer Right Here!

Provide global customers with complete turn-key solutions
through
innovation!
QUICK LINKS
CONTACT INFO.
-
 +86-139 1308 8972
-

-
 No. 118 Yexin Road, Wujiang Economic Development Zone, Suzhou, China
Copyright © Suzhou Shuangqisi Mold Equipment Co., Ltd. All Rights Reserved. Custom Stamping Die Metal Stamping Die Manufacturers
