 English
 Español
 Deutsch
-

Progressive Stamping Die for Connector & Terminal Parts High Speed Progressive Stamping Die Precision Metal Hardware Stamping Tool mold for Connector Terminal Parts Automotive Components
Progressive Stamping Die for Connector & Termi...
-
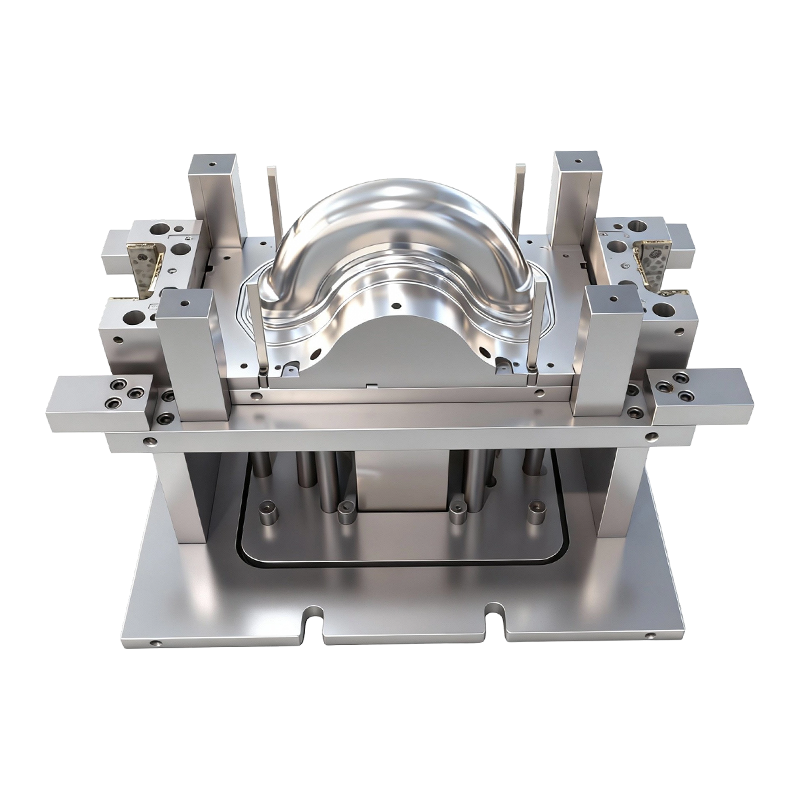
Deep drawing mold for front and rear wheels of two-wheeled electric vehicles
This Deep drawing mold for front and rear wheels o...
-
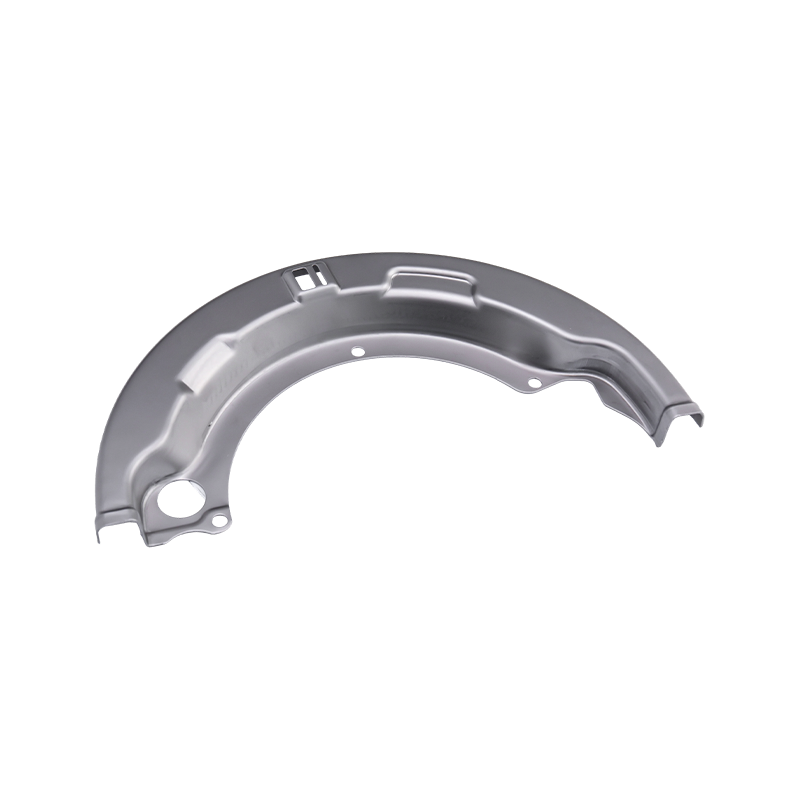
Heavy truck stamping parts
Our Heavy truck stamping parts are precision-manuf...
-

Long-Stroke Multi-Stage Progressive Die Automatic Strip Feed Progressive Die Long Travel Follow on Stamping Tool for Sheet Metal Hardware Press Moulding
Long-Stroke Multi-Stage Progressive DieOur custom ...
-
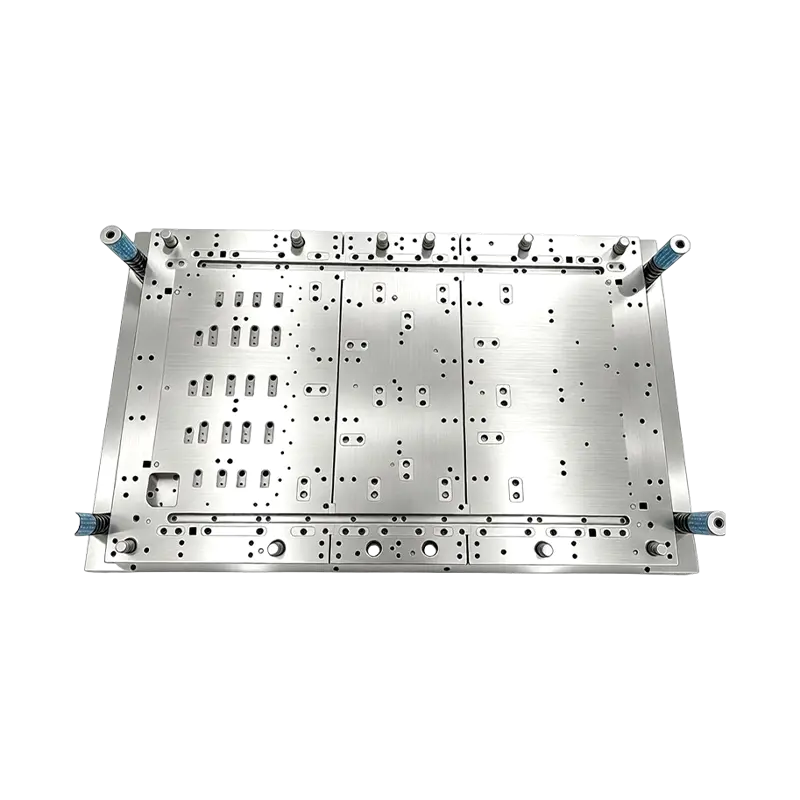
Multi-Station Progressive Stamping Die with Carbide Inserts Custom Multi Station Progressive Stamping Die Carbide Insert Metal Stamping Mold Tool for Equipment Appliances Device Hardware
High Speed Metal Stamping Tool for Precise Equipme...
- E-mail us: [email protected]
- Call us: +86-139 1308 8972

Liu Yanan – After-Sales Service Engineer
Home / Author / Liu Yanan – After-Sales Service Engineer / Heavy Truck Stamping Parts: Precision, Strength, and Reliable Manufacturing for Commercial Vehicles
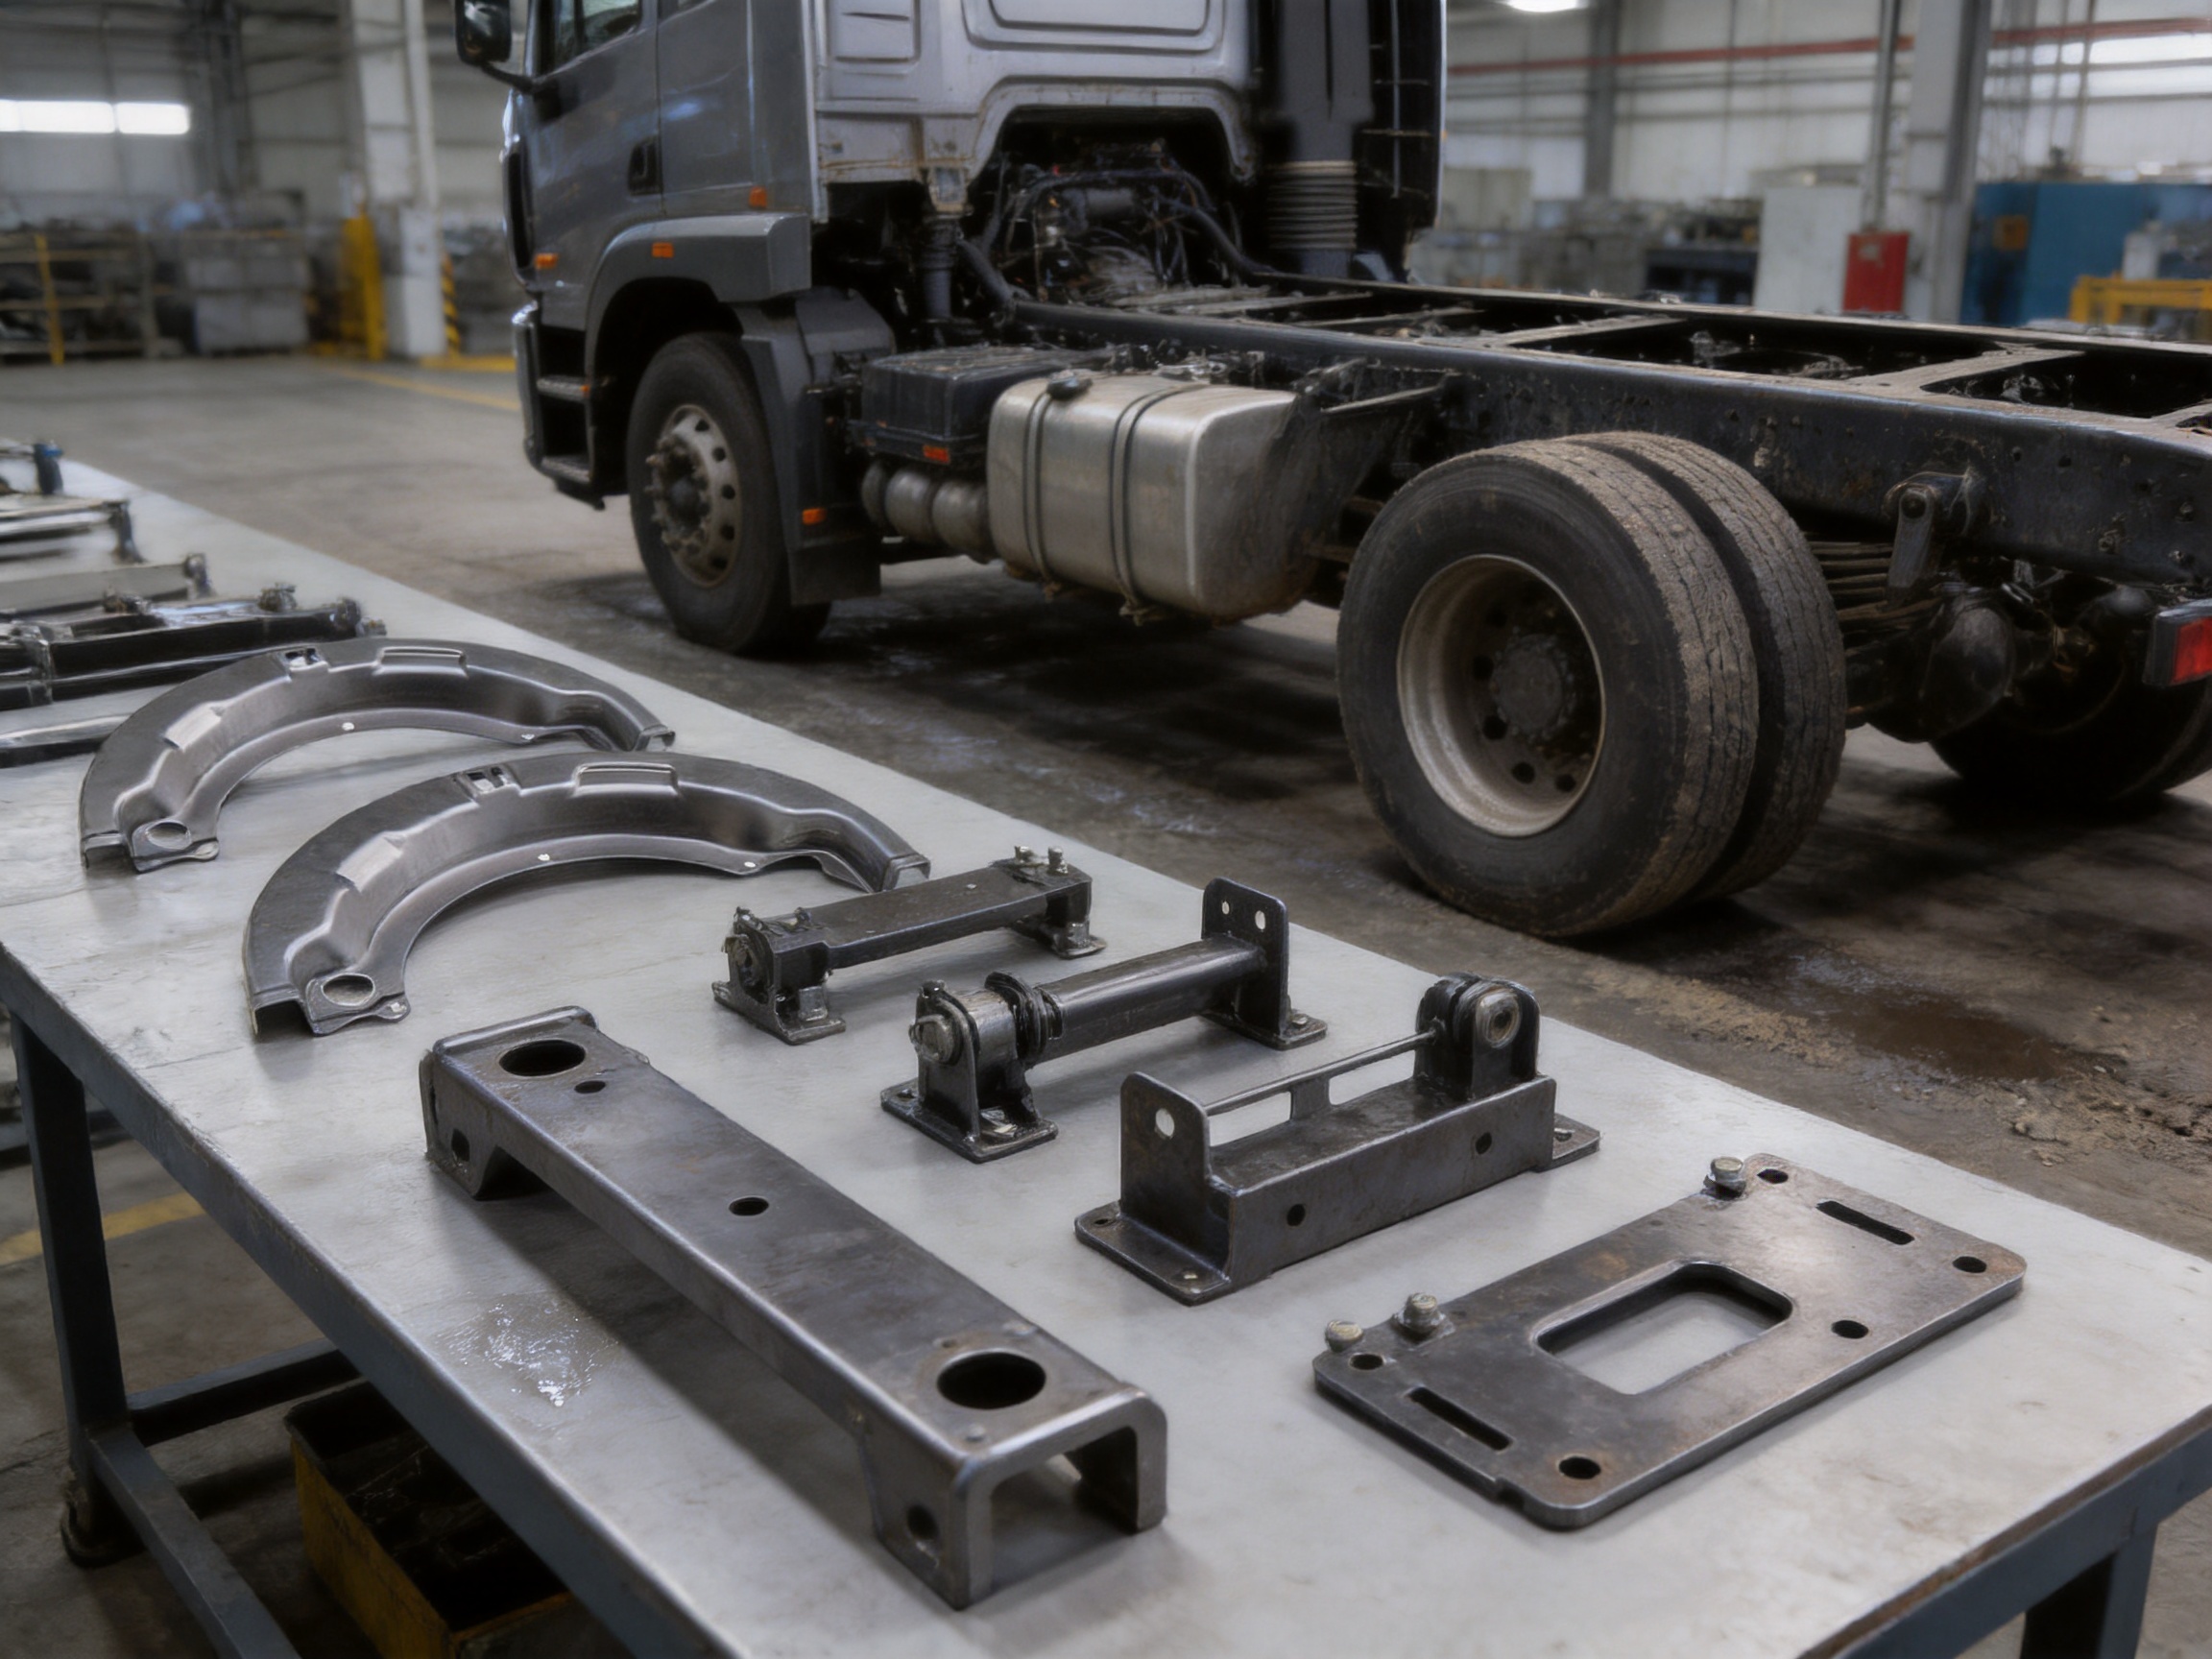
Heavy Truck Stamping Parts: Precision, Strength, and Reliable Manufacturing for Commercial Vehicles
2026-10-14
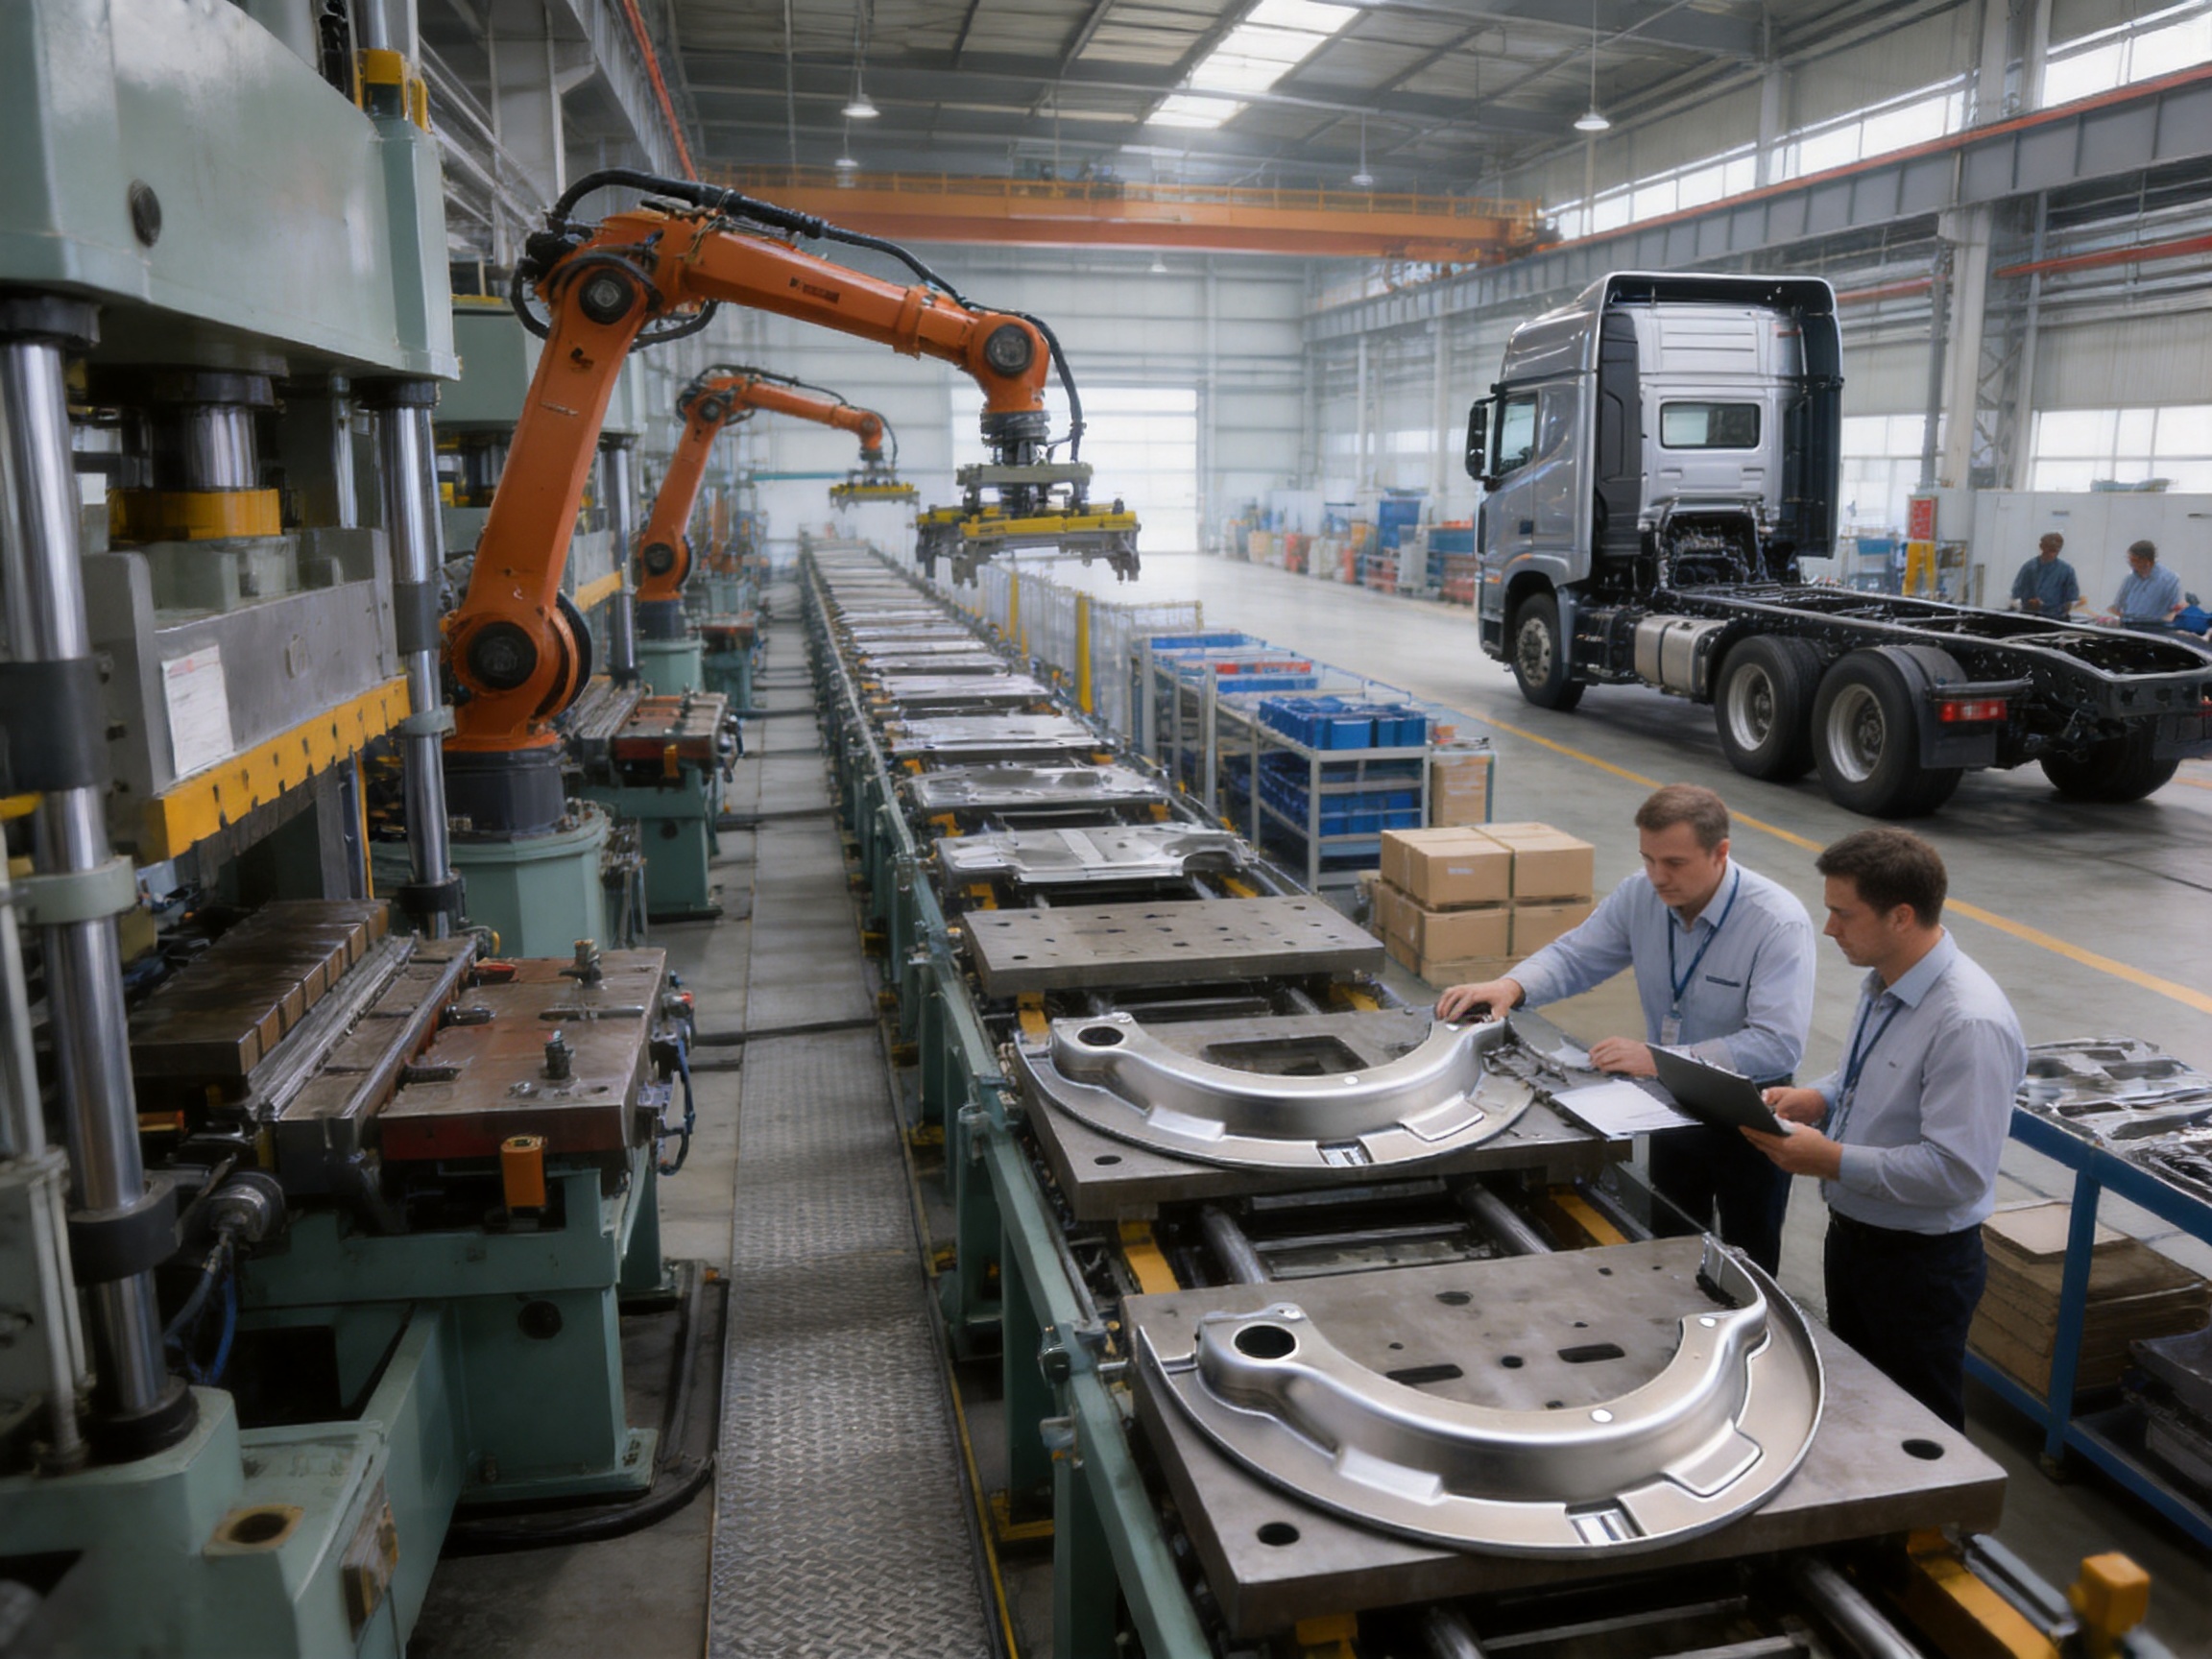
Content
- 1 Introduction to Heavy Truck Stamping Parts
- 2 Why Heavy Truck Stamping Parts Require Specialized Engineering
- 3 Product Scope and Typical Applications
- 4 Material Selection for Heavy-Duty Stamped Components
- 5 Advanced Cold Stamping Technology
- 6 Integrated Die Design and Manufacturing
- 7 Manufacturing Process from Design to Finished Part
- 7.1 1. Technical Review and Requirement Confirmation
- 7.2 2. Product and Process Engineering
- 7.3 3. Die Design and Component Machining
- 7.4 4. Die Assembly and Trial Stamping
- 7.5 5. Material Preparation and Production Stamping
- 7.6 6. Deburring, Calibration, and Secondary Operations
- 7.7 7. Inspection and Release
- 7.8 8. Packaging and Delivery
- 8 Quality Control for Commercial Vehicle Components
- 9 Advantages Compared with Less Integrated Suppliers
- 10 Manufacturing Capabilities and Company Strengths
- 11 Stamping Automation and Production Efficiency
- 12 Product Benefits for Truck Manufacturers and Aftermarket Providers
- 13 Recommended Customer Project Workflow
- 14 Comparison of Key Performance Factors
- 15 Applications in Long-Haul and Construction Vehicles
- 16 Maintenance and Service Considerations
- 17 Quality, Value, and Long-Term Partnership
- 18 Frequently Asked Questions
- 18.1 What are heavy truck stamping parts?
- 18.2 What materials are used for these components?
- 18.3 Why is die quality important?
- 18.4 Can the parts be customized?
- 18.5 What quality checks are performed?
- 18.6 What production equipment is available?
- 18.7 Does the supplier provide stamping automation?
- 18.8 How can stamping parts help reduce maintenance frequency?
- 18.9 Are these parts suitable for aftermarket service?
- 18.10 What information should be supplied for a quotation?
- 19 Conclusion
- 20 References
- 21 Product: Heavy truck stamping parts
Introduction to Heavy Truck Stamping Parts
Heavy-duty trucks operate in some of the most demanding transportation environments in the world. Long-haul vehicles may travel thousands of kilometers under high payloads, while construction, mining, logistics, and municipal trucks are repeatedly exposed to vibration, impact, dust, moisture, road salt, temperature changes, and uneven terrain. Every structural and mounting component must therefore provide dependable mechanical performance throughout the service life of the vehicle.
Heavy truck stamping parts are essential components in this system. They are formed from steel plate through controlled stamping operations to create brackets, connecting plates, support members, reinforcement pieces, and other parts used in truck frames, suspension systems, engine mounting assemblies, and related structures. Although many stamped parts are compact compared with a complete truck, their dimensional accuracy, material strength, and installation consistency can directly affect vehicle stability, component alignment, maintenance requirements, and operating safety.
Modern heavy truck manufacturers and aftermarket suppliers require more than simple pressed metal components. They need parts made with reliable dies, stable production processes, repeatable quality control, and efficient delivery capabilities. The manufacturing of heavy truck stamping parts must balance strength, weight, manufacturability, cost, surface protection, and compatibility with original vehicle assemblies.
Suzhou Shuangqisi Mold Equipment Co., Ltd. provides heavy truck stamping parts supported by integrated die design, mold manufacturing, stamping production, inspection, and technical service capabilities. The company’s experience in stamping dies and hardware components allows it to control the relationship between tooling accuracy and final-part quality. Its production capabilities include high-strength steel stamping, precision machining, grinding, wire cutting, press forming, process debugging, and quality inspection.
This integrated approach is particularly valuable for commercial vehicle components. Instead of treating the stamping die and stamped product as separate purchasing categories, customers can obtain coordinated support from product development through production implementation. The result is a more controlled manufacturing chain, improved dimensional consistency, and a practical foundation for long-term supply.
Why Heavy Truck Stamping Parts Require Specialized Engineering
Passenger vehicle stamping parts and heavy truck stamping parts may share some basic forming principles, but their engineering requirements are not identical. Heavy trucks carry higher loads, experience greater structural stress, and often operate for longer hours than ordinary passenger vehicles. Parts mounted near the frame, suspension, engine, or powertrain must tolerate repeated load cycles without excessive deformation or premature fatigue.
A frame bracket, for example, may be exposed to vertical loading, lateral forces, torsional movement, and vibration transmitted from the road. A suspension connecting plate must maintain the correct relationship between suspension components even when the vehicle is fully loaded. An engine mounting support must combine strength with accurate positioning so that the engine remains correctly aligned while vibration is controlled.
These working conditions create several key manufacturing requirements:
First, the selected steel must provide an appropriate combination of tensile strength, yield strength, formability, and fatigue resistance. A material that is too soft may deform under load, while a material that is too hard or poorly suited to the forming process may crack during stamping.
Second, the die must be designed to control material flow. Uneven material movement can produce wrinkles, splits, thinning, springback, or dimensional variation. These defects may not always be visible during a basic visual inspection, but they can affect assembly and long-term durability.
Third, critical dimensions must remain stable from one production batch to another. Heavy truck components are normally installed as part of a larger assembly. A small dimensional error in a mounting hole, bend angle, or reference surface may create installation difficulty or place additional stress on connected components.
Fourth, edges and formed surfaces require appropriate control. Sharp burrs can interfere with assembly, damage nearby parts, create safety risks during handling, or accelerate coating failure. Smooth edges and consistent radii help support both production efficiency and service reliability.
Finally, surface condition and corrosion resistance must be considered according to the truck’s application. Commercial vehicles frequently work in wet, dirty, or chemically aggressive environments. Proper material preparation, cleaning, protective treatment, and storage practices can help maintain the service performance of stamped components.
Product Scope and Typical Applications
The heavy truck stamping parts product line is designed for commercial heavy-duty vehicle applications. It covers structural and functional components manufactured from high-strength steel plates using advanced cold stamping technology. The parts can be developed for original equipment projects, replacement programs, aftermarket service, or customized vehicle assemblies.
Frame Brackets
Frame brackets provide connection and support functions within the truck chassis. They may be used to attach auxiliary structures, cross members, body components, cab systems, suspension-related parts, or other equipment to the main frame. Because the frame is exposed to dynamic loading, bracket geometry and hole positioning are particularly important.
Stamped frame brackets can be designed with flanges, ribs, mounting holes, relief features, and reinforcing sections to provide an effective balance between stiffness and weight. Proper forming reduces the need for excessive secondary operations while maintaining the geometry required for secure installation.
Suspension Connecting Plates
Suspension connecting plates help transfer loads and maintain the relationship between suspension elements. They must tolerate repeated movement and vibration while preserving dimensional stability. The position, diameter, and alignment of mounting holes are often critical because they influence bolt installation, joint loading, and suspension geometry.
High-strength steel and controlled stamping operations allow these plates to achieve the required structural performance without unnecessary material thickness. Accurate forming also helps reduce assembly adjustments and supports consistent performance across vehicles.
Engine Mounting Supports
Engine mounting supports connect the engine or powertrain assembly to the vehicle structure. These parts must carry static weight while managing vibration, torque reaction, and dynamic movement. Their design may include multiple bends, reinforcement features, mounting surfaces, and precisely located holes.
Accurate engine mounting supports help maintain the intended powertrain position. This can support proper alignment with transmission, exhaust, cooling, electrical, and driveline systems. Stable production is essential because variation in these components may lead to installation interference or excessive vibration.
Customized Structural and Hardware Components
In addition to standard product categories, heavy truck manufacturers and service providers may require customized brackets, reinforcement plates, support pieces, covers, connecting components, or other sheet-metal parts. These products can be developed according to customer drawings, samples, three-dimensional data, technical specifications, and application requirements.
Customization may involve material selection, thickness, bend radius, hole patterns, surface treatment, packaging, inspection plans, or production volume. A manufacturer with both die-making and stamping capabilities can evaluate the product and tooling together, improving the practicality of the final design.
Heavy truck stamping parts
Material Selection for Heavy-Duty Stamped Components
Material selection is one of the most important decisions in the production of heavy truck stamping parts. The appropriate steel grade depends on the part’s load requirements, geometry, forming depth, thickness, fatigue conditions, joining method, corrosion environment, and cost target.
High-strength steel plates are widely used for commercial vehicle components because they can provide increased load capacity while helping control component weight. Reducing unnecessary weight can contribute to payload efficiency, fuel economy, and overall vehicle performance. However, high-strength materials also require careful control during forming because their higher strength may increase springback and forming forces.
The material must therefore be matched to the stamping process. Engineers need to consider whether a part can be formed in one operation or requires multiple steps. They may also evaluate blank shape, grain direction, draw depth, flange design, bend radius, local reinforcement, and the sequence of forming operations.
Material consistency is equally important. Variations in thickness, mechanical properties, or surface quality can affect die performance and final-part dimensions. Reliable incoming inspection and controlled material storage help reduce these risks. Material identification should also be maintained through production records so that product traceability can be supported when required by the customer.
For parts exposed to moisture, road debris, or corrosive substances, the material and surface protection strategy should be considered together. Stamping quality alone cannot prevent corrosion if the product is stored improperly or left without suitable protection. Depending on the customer’s requirements, surface preparation, coating, oiling, painting, or other anti-corrosion measures may be incorporated into the manufacturing plan.
Advanced Cold Stamping Technology
Cold stamping forms steel plate at room temperature using a combination of dies, presses, punches, forming surfaces, and controlled force. The process can create complex shapes with high repeatability and efficient material utilization. For heavy truck applications, cold stamping is well suited to brackets, plates, supports, reinforcements, and other components that require strong, stable geometries.
A typical cold stamping project begins with product analysis. Engineers review the drawing or sample to understand the part’s functional surfaces, load-bearing zones, mounting points, bend areas, and potential forming risks. The design is then evaluated for manufacturability. Where necessary, the original geometry may be optimized to improve material flow, simplify tooling, reduce secondary work, or increase structural stiffness.
The next stage is process planning. Engineers determine the blank shape, forming sequence, piercing operations, trimming requirements, bending steps, and inspection points. A part may be produced using a progressive die, compound die, transfer process, or a series of single-operation dies, depending on its geometry, volume, and quality requirements.
Die design must account for clearance, punch and die alignment, forming radii, press capacity, material springback, wear, lubrication, and maintenance access. For heavy truck components, the die must also withstand repeated production forces without losing dimensional stability. Properly designed tooling contributes directly to consistent product quality and lower long-term production risk.
During stamping, the steel blank is positioned in the die and subjected to controlled pressure. Cutting, punching, bending, drawing, embossing, or forming may occur depending on the operation. The finished part is then removed, checked, and transferred to subsequent processes such as deburring, calibration, welding, surface treatment, or packaging.
Advanced cold stamping provides several benefits over less controlled fabrication methods. Compared with manual cutting and bending, stamping can deliver more consistent geometry, higher output, cleaner repeatability, and better suitability for medium- and high-volume production. Compared with some welded assemblies, a correctly formed stamped part may reduce the number of joints, simplify assembly, and offer a more uniform load path.
Integrated Die Design and Manufacturing
The quality of a stamped part depends heavily on the quality of its die. A die that is inaccurate, poorly balanced, or unsuitable for the selected material can create recurring defects and unstable production. For this reason, integrated die design and manufacturing is one of the major strengths behind reliable heavy truck stamping parts.
Suzhou Shuangqisi Mold Equipment Co., Ltd. operates as a professional manufacturer of stamping dies and hardware parts, integrating design, manufacturing, and service. This structure allows the company to evaluate tooling and product requirements as one technical system rather than as isolated activities.
The company has 60 technical staff and a production foundation that includes imported wire cutting machines, CNC machining centers, more than 10 grinding machines of various sizes, and 25 punch presses ranging from 80 tons to 400 tons. This equipment range supports the development and production of stamping dies and parts in different sizes and complexity levels.
Wire cutting equipment is useful for producing accurate profiles, inserts, and complex die components. CNC machining centers support precise milling of die bases, forming surfaces, pockets, locating features, and other structural elements. Grinding machines help achieve accurate flatness, surface quality, and dimensional control on critical die components.
Press capacity is another important consideration. The available range from 80 tons to 400 tons allows production planning to be matched to part size, material thickness, forming force, and die design. Selecting an appropriate press helps prevent overloading, reduces unnecessary equipment consumption, and supports stable forming conditions.
After machining, dies must be assembled, adjusted, tested, and debugged. Senior operators and experienced debugging personnel can identify practical issues that may not be fully visible in a design review. Trial stamping helps reveal material flow behavior, springback, burr formation, wrinkling, cracking, hole displacement, and other factors that require correction before mass production.
Tooling Accuracy and Part Consistency
Tooling accuracy influences the repeatability of every production cycle. If locating surfaces, cutting edges, or forming elements are not correctly aligned, the resulting parts may show variation in hole position, flange angle, flatness, or overall profile. Such differences can increase assembly time and create downstream quality problems.
Precision machining and grinding help establish the geometric foundation of the die. Careful assembly and trial adjustment then ensure that the tooling performs as intended under actual press conditions. This combination of equipment and human expertise supports the stable production of heavy-duty components.
Tooling Durability and Maintenance
Heavy truck stamping parts may be produced in repeated batches over an extended supply period. The die must therefore be durable and maintainable. Wear-prone areas should be designed for inspection and, where practical, replacement or repair. Regular maintenance can help preserve cutting clearance, forming accuracy, surface condition, and production efficiency.
A well-maintained die also reduces unexpected downtime. Planned inspection of punches, inserts, guide components, springs, locating elements, and forming surfaces can identify wear before it creates large quantities of defective parts.
Manufacturing Process from Design to Finished Part
A dependable heavy truck stamping part is the result of a controlled sequence rather than a single press operation. The following stages illustrate a typical production approach.
1. Technical Review and Requirement Confirmation
The process begins with a review of customer drawings, samples, three-dimensional data, material specifications, annual demand, inspection requirements, and intended application. Engineers confirm critical dimensions, functional surfaces, mounting locations, tolerance requirements, and expected production conditions.
If the customer provides only a sample or basic concept, the technical team may need to evaluate the component’s manufacturability and develop a practical process route. Any design risks should be discussed before tooling begins.
2. Product and Process Engineering
Engineers analyze the component’s geometry and determine how it can be formed efficiently. They consider blank development, cutting layout, bend sequence, draw direction, press tonnage, die structure, material utilization, and post-stamping operations.
At this stage, design improvements may be recommended. For example, an excessively sharp corner may be modified to reduce cracking risk, or an unnecessary feature may be simplified to improve production stability. Any proposed change should preserve the component’s functional requirements.
3. Die Design and Component Machining
After process approval, the die is designed and its components are manufactured. CNC machining, wire cutting, grinding, drilling, and other precision operations are used according to the component’s function. Critical dimensions and reference surfaces receive particular attention.
Machining accuracy must be supported by appropriate inspection. Die components are checked before assembly to confirm that they meet the intended design requirements. This helps prevent the transfer of errors into the final tooling system.
4. Die Assembly and Trial Stamping
Machined components are assembled into a complete die and installed for testing. Trial stamping is used to evaluate actual forming behavior. Engineers and operators inspect the trial parts for dimensional accuracy, surface quality, burrs, cracks, wrinkles, thinning, springback, and assembly compatibility.
Adjustments may include modifying forming surfaces, correcting clearances, refining guide elements, improving blank positioning, changing process sequence, or adjusting press conditions. Several trial cycles may be necessary before the die is ready for stable production.
5. Material Preparation and Production Stamping
Approved steel plate is prepared according to the production plan. Blanks are cut or otherwise prepared to the required dimensions and loaded into the stamping process. Operators verify die setup, press settings, lubrication conditions, material orientation, and safety requirements before production begins.
During production, parts are formed under controlled press conditions. Process parameters should remain consistent, and operators should monitor unusual noise, material movement, burr development, surface damage, or changes in press behavior.
6. Deburring, Calibration, and Secondary Operations
After stamping, parts may require deburring, edge treatment, calibration, straightening, tapping, welding, drilling, or other operations depending on the product design. The goal is to ensure that the finished component is safe to handle, compatible with its assembly, and consistent with customer requirements.
Calibration may be used when springback or forming variation must be further controlled. Secondary operations should be planned carefully because they can influence flatness, hole position, and surface condition.
7. Inspection and Release
Finished parts undergo inspection according to the approved quality plan. Inspection may include visual examination, dimensional measurement, hardness checks, flatness verification, edge inspection, and anti-corrosion performance evaluation where applicable.
Inspection records provide evidence that the batch has been reviewed. If a deviation is identified, the cause should be investigated rather than simply sorting the product without corrective action. This approach supports continuous improvement and helps protect future production stability.
8. Packaging and Delivery
Proper packaging prevents deformation, scratching, moisture exposure, and mixing of different part numbers during transportation. Heavy truck components may be packed using separators, protective materials, pallets, cartons, or customized containers according to their size and surface requirements.
Clear identification supports warehouse control and customer receiving. Part number, quantity, batch information, and handling instructions can be included according to the customer’s supply-chain requirements.
Quality Control for Commercial Vehicle Components
Quality control for heavy truck stamping parts should combine prevention, process monitoring, and final verification. Final inspection is important, but it cannot replace good die design, stable material control, and disciplined production procedures.
Dimensional Accuracy
Dimensional accuracy is essential for assembly compatibility. Critical dimensions may include overall length and width, bend angle, hole diameter, hole-to-hole distance, flange height, reference-plane position, and mounting-surface flatness.
Measurement methods should be selected according to the part’s geometry and tolerance. Simple gauges may be suitable for repetitive checks, while coordinate measurement or specialized fixtures may be used for more complex shapes. The objective is to verify the dimensions that affect function rather than measuring without a clear quality purpose.
Hardness and Material Condition
Hardness inspection can help verify material condition and identify abnormalities. It may also support the assessment of whether the part has experienced unexpected changes during processing. The inspection method and acceptance range should be determined according to the material and customer requirements.
Flatness and Form Stability
Flatness is important for parts that contact frames, brackets, engine mounts, or other structural components. Excessive distortion may cause gaps, uneven bolt loading, installation difficulty, or local stress concentration.
Form stability depends on material characteristics, die accuracy, forming sequence, cooling and handling conditions, and storage. Parts should be supported appropriately after stamping to reduce the risk of deformation before inspection and shipment.
Edge and Surface Quality
Edges should be free from harmful burrs, cracks, sharp projections, and excessive deformation. Surface inspection can identify scratches, dents, press marks, rust, oil contamination, and other conditions that may affect installation or protective treatment.
Corrosion Protection
Anti-corrosion performance is especially important for parts installed beneath or around commercial vehicles. The required protection method depends on the part’s location, exposure conditions, customer specification, and downstream assembly process.
Protection may involve appropriate material selection, cleaning, temporary rust prevention, coating, painting, or another approved treatment. Storage and transportation conditions must also be controlled because even a well-treated part can corrode if exposed to moisture for an extended period.
Advantages Compared with Less Integrated Suppliers
Customers sourcing heavy truck stamping parts often compare suppliers according to price, delivery time, tooling quality, technical support, and long-term reliability. A low initial quotation may not represent the lowest total cost if the supplier lacks process engineering capability or cannot maintain die accuracy.
One Technical Chain from Tooling to Product
An integrated supplier can connect die design, machining, trial production, stamping, inspection, and service. This reduces communication gaps between separate vendors. When a product issue occurs, the technical team can evaluate whether the cause relates to material, die geometry, press conditions, secondary operations, or inspection methods.
This unified responsibility can shorten problem-solving cycles and make engineering changes more manageable. It also helps customers avoid coordinating multiple suppliers for tooling correction and part production.
Suitable Equipment for Different Production Requirements
The combination of precision machining equipment, grinding capacity, wire cutting capability, and presses from 80 tons to 400 tons allows production planning to be adapted to different part sizes and forming demands. This flexibility is useful for both development projects and repeat production.
Practical Experience in Debugging
Computer-aided design is valuable, but real stamping performance also depends on practical trial adjustment. Experienced operators and debugging personnel understand how material behavior, press conditions, lubrication, and tooling alignment interact in actual production.
This practical knowledge can help resolve forming problems efficiently and support a smoother transition from prototype to production.
Cost and Quality Balance
Competitive pricing should be achieved through efficient process design, appropriate tooling, material utilization, stable production, and controlled rework rather than by reducing essential quality measures. An integrated manufacturing model can help lower hidden costs associated with repeated tooling changes, rejected parts, delayed deliveries, and assembly problems.
Experience Across Multiple Industrial Applications
The company has approximately 15 years of experience in the mold industry and has supplied molds and products for applications including servo drives, compressors, and new energy vehicles. Experience across these sectors can support broader understanding of precision stamping, structural requirements, repeat production, and customer-specific quality expectations.
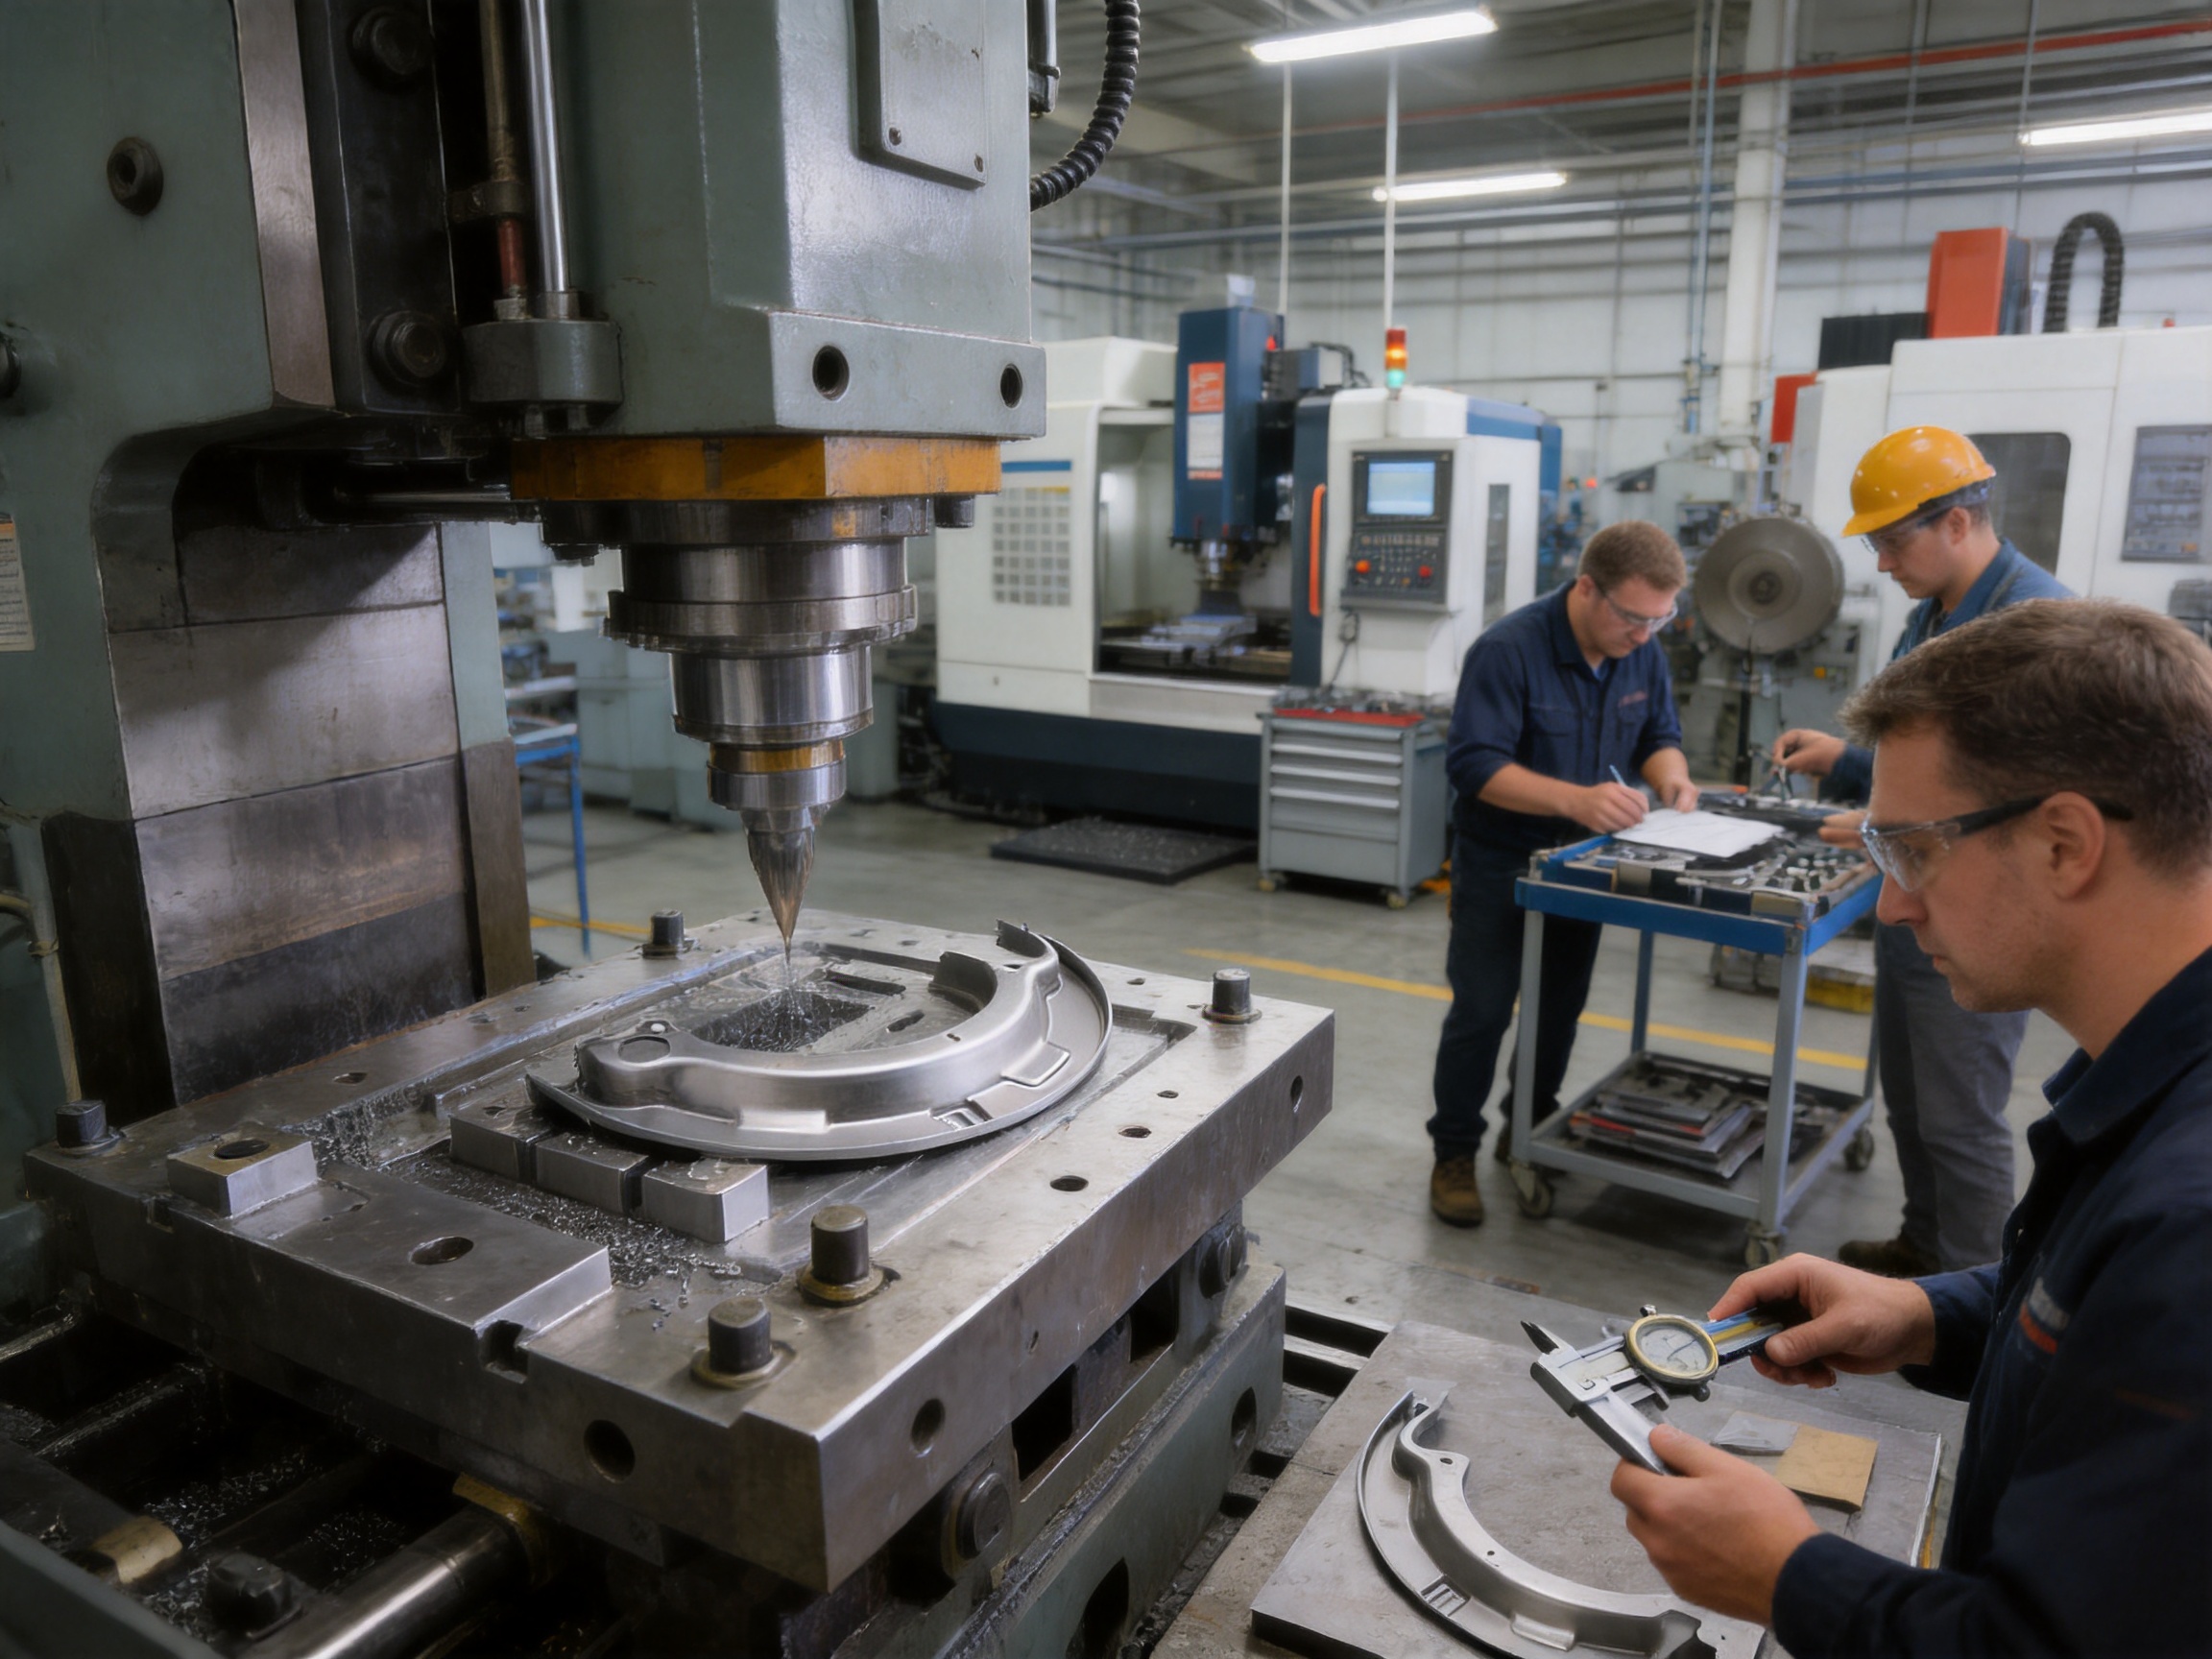
Manufacturing Capabilities and Company Strengths
Suzhou Shuangqisi Mold Equipment Co., Ltd. is located in the Wujiang Economic Development Zone of Suzhou, China. The company specializes in stamping dies and hardware parts and integrates design, manufacturing, and service within one organization.
The company’s 60 technical staff support product development, die engineering, machining, assembly, production debugging, and customer service. A technical team of this structure can be valuable for customized heavy truck components because commercial vehicle projects often require detailed communication and engineering coordination.
The company’s equipment includes imported wire cutting machines, CNC machining centers, more than 10 grinding machines of various sizes, and 25 punch presses with capacities ranging from 80 tons to 400 tons. These resources create a manufacturing foundation for both tooling and stamped products.
Senior operators and experienced debugging personnel contribute practical knowledge during trial production and process adjustment. Their role is particularly important when working with high-strength steel, complex bends, tight mounting dimensions, or components requiring careful control of springback.
In 2016, the company invested in and established Suzhou Keshuang Intelligent Technology Co., Ltd., which focuses mainly on stamping automation equipment. This development expanded the company’s ability to provide integrated solutions that combine stamping molds with automation equipment.
For customers planning a new production line, this capability may provide additional value. Instead of purchasing a die without considering the full production environment, the customer can discuss automation, handling, press integration, and production efficiency as part of a broader project. The company can also invest in related production equipment according to customer needs and provide cost-effective solutions.
Stamping Automation and Production Efficiency
Automation can improve the consistency, safety, and efficiency of stamping production. Depending on the product and press arrangement, automated systems may support material feeding, transfer between operations, part removal, stacking, inspection assistance, and production data collection.
Automation is particularly useful for repetitive heavy truck components produced in medium or large quantities. It can reduce manual handling, limit variation caused by inconsistent positioning, and help protect operators from repetitive or high-force tasks.
However, automation should be designed around the part, die, press, cycle time, and factory layout. A technically complex system is not automatically the best solution if it is difficult to maintain or poorly matched to production volume. Practical automation should provide a clear benefit in safety, quality, output, labor efficiency, or process stability.
Because the company has capabilities in both stamping dies and stamping automation equipment, customers can discuss these elements together. This may improve coordination between die design and automated handling requirements. Features such as part orientation, gripping points, transfer clearance, stacking direction, and access for inspection can be considered earlier in the project.
Product Benefits for Truck Manufacturers and Aftermarket Providers
Reliable Assembly Compatibility
Accurately manufactured mounting points, holes, and formed surfaces help the part fit with original truck assemblies. This reduces the need for manual modification and supports more efficient installation during vehicle production or repair.
Durability Under Severe Operating Conditions
High-strength steel and controlled forming provide a strong foundation for components that must resist vibration, impact, and repeated loading. Properly designed parts can help maintain structural performance during long-haul, construction, and other demanding operations.
Reduced Maintenance Risk
When brackets, supports, and connecting plates maintain their shape and attachment points, related assemblies can operate under more predictable conditions. This may help reduce premature loosening, misalignment, deformation, and unnecessary maintenance intervention.
Efficient Repeat Production
Stamping dies are suitable for producing repeated parts with stable geometry. Once tooling has been developed and validated, production can be organized for consistent output and predictable quality, especially when supported by appropriate automation.
Customized Supply Support
Customers may require parts with specific thicknesses, hole patterns, surface treatments, packaging methods, or inspection standards. An experienced manufacturer can adapt the product and process to project requirements rather than offering only a fixed standard item.
Recommended Customer Project Workflow
Customers can improve project efficiency by preparing complete technical information at the beginning of the inquiry. Useful information includes two-dimensional drawings, three-dimensional models, material grade, thickness, annual quantity, prototype quantity, critical tolerances, surface treatment requirements, application environment, inspection standards, and delivery expectations.
When drawings are not available, samples, photographs, measurements, and assembly information can help the engineering team understand the component. Information about load direction, adjacent parts, fastening methods, and service conditions is also valuable for evaluating the design.
The supplier should then provide feedback on manufacturability, tooling concept, process route, production capacity, quality control, and expected lead time. Clear agreement at this stage helps prevent later misunderstandings regarding materials, tolerances, secondary processes, and acceptance criteria.
Prototype or trial parts should be evaluated in the actual assembly whenever possible. A component may meet isolated dimensional requirements but still create interference when installed with neighboring parts. Assembly verification provides practical confirmation of fit, access, bolt alignment, clearance, and functional performance.
After approval, mass production should follow an agreed control plan. Any changes to material, die, process sequence, surface treatment, or packaging should be reviewed before implementation. This protects consistency throughout the product’s supply life.
Comparison of Key Performance Factors
| Performance Factor | Importance in Heavy Truck Applications | Manufacturing Response |
|---|---|---|
| Material strength | Supports load-bearing and fatigue resistance | Selection of suitable high-strength steel and incoming material control |
| Dimensional accuracy | Ensures compatibility with original assemblies | Precision die manufacturing, trial stamping, and dimensional inspection |
| Form stability | Reduces deformation and installation problems | Controlled forming sequence, calibration, and flatness verification |
| Edge quality | Improves handling safety and assembly reliability | Controlled cutting clearance, deburring, and edge inspection |
| Corrosion resistance | Protects components in moisture, salt, and road debris | Appropriate material preparation, protection, treatment, and storage |
| Tooling life | Supports repeat production and stable cost | Durable die construction, maintenance planning, and wear monitoring |
| Production efficiency | Helps meet volume and delivery requirements | Suitable press selection, process optimization, and stamping automation |
| Technical service | Reduces project risk and speeds problem resolution | Integrated design, manufacturing, debugging, inspection, and customer support |
Applications in Long-Haul and Construction Vehicles
Long-haul trucks operate continuously over highways and mixed road conditions. Their structural components experience repeated vibration and loading over extended distances. Heavy truck stamping parts used in these vehicles must therefore deliver consistent performance across long service intervals.
Construction trucks face additional challenges. They may travel on unpaved roads, carry heavy materials, operate near dust and mud, and experience frequent impact or shock loading. Brackets and supports in these vehicles should be designed and manufactured with adequate strength, secure mounting, and suitable protection against environmental exposure.
Other applications may include municipal service vehicles, logistics fleets, special-purpose trucks, trailers, vocational vehicles, and aftermarket replacement programs. Each application may have different requirements, but the underlying priorities remain similar: accurate fit, dependable strength, stable quality, and efficient supply.
Maintenance and Service Considerations
Although stamped parts are designed for durability, regular vehicle inspection remains important. Maintenance personnel should check mounting bolts, contact surfaces, cracks, deformation, corrosion, and unusual movement in the surrounding assembly. Damage to a connected component may place abnormal loads on the stamped part and should be addressed promptly.
When replacing a heavy truck stamping part, the replacement should match the required material, dimensions, mounting pattern, and surface protection. Improvised modification, uncontrolled drilling, excessive grinding, or unauthorized welding may weaken the component or alter load distribution.
Suppliers can support service providers by maintaining clear part identification and providing consistent replacement products. Stable production records and traceability can also help customers investigate field issues and select the correct replacement specification.
Quality, Value, and Long-Term Partnership
The value of a heavy truck stamping part should be evaluated over its entire service and supply cycle. Purchase price is important, but so are tooling stability, installation efficiency, field durability, delivery reliability, and technical responsiveness.
A supplier that can manufacture both dies and parts is positioned to understand the complete cost structure. The supplier can identify whether a design change will affect tooling investment, material utilization, cycle time, secondary work, inspection, or maintenance. This broader view helps customers make decisions based on total value rather than only unit price.
Long-term partnership also depends on communication. Heavy truck projects may evolve as vehicle platforms, production volumes, material specifications, or regulatory expectations change. A responsive technical team can help review new requirements, improve existing tooling, and adjust production methods while protecting quality and delivery commitments.
Suzhou Shuangqisi Mold Equipment Co., Ltd. emphasizes customer value, high-quality development, strict cost control, and reliable technical expertise. Its combined capabilities in mold making, stamping production, and automation equipment support a practical one-stop model for customers seeking heavy truck components and related manufacturing solutions.
Frequently Asked Questions
What are heavy truck stamping parts?
Heavy truck stamping parts are metal components formed from steel plate through stamping operations for use in commercial heavy-duty vehicles. Typical examples include frame brackets, suspension connecting plates, engine mounting supports, reinforcement plates, and other structural or hardware components.
What materials are used for these components?
High-strength steel plates are commonly used because they provide a suitable combination of strength, formability, durability, and weight efficiency. The exact material should be selected according to the component’s geometry, load requirements, forming process, surface treatment, and customer specification.
Why is die quality important?
The die controls the shape, hole position, bend angle, edge condition, and repeatability of the stamped part. An inaccurate or unstable die can create variation, burrs, cracks, springback, and assembly problems. Precision machining, grinding, assembly, and trial stamping help establish reliable tooling performance.
Can the parts be customized?
Yes. Heavy truck stamping parts can be customized according to drawings, samples, three-dimensional data, material requirements, thickness, hole patterns, surface treatment, packaging, and inspection standards. Custom development is especially useful for original equipment and specialized aftermarket applications.
What quality checks are performed?
Quality checks may include visual inspection, dimensional measurement, hardness testing, flatness verification, edge inspection, surface evaluation, and anti-corrosion performance assessment where required. The final inspection plan should be agreed according to the product’s critical characteristics and customer requirements.
What production equipment is available?
The manufacturing resources include imported wire cutting machines, CNC machining centers, more than 10 grinding machines of various sizes, and 25 punch presses with capacities ranging from 80 tons to 400 tons. This equipment supports stamping die manufacturing and the production of different heavy truck components.
Does the supplier provide stamping automation?
Yes. Through its investment in Suzhou Keshuang Intelligent Technology Co., Ltd., the company can provide stamping automation equipment in addition to dies and stamped parts. Customers can discuss integrated solutions for feeding, transfer, handling, stacking, and related production requirements.
How can stamping parts help reduce maintenance frequency?
Accurately formed and durable parts can help maintain proper alignment, secure mounting, and stable load transfer. This may reduce problems caused by deformation, poor fit, premature loosening, or excessive stress in connected assemblies. Actual maintenance results also depend on vehicle design, operating conditions, installation, and inspection practices.
Are these parts suitable for aftermarket service?
They can be suitable for aftermarket service when manufactured according to the required original dimensions, material specification, mounting configuration, and quality standard. Customers should provide accurate reference information so that replacement parts can be matched correctly to the intended vehicle assembly.
What information should be supplied for a quotation?
Useful information includes part drawings or samples, three-dimensional files, material grade, thickness, expected quantity, prototype needs, tolerance requirements, surface treatment, packaging, inspection standards, and delivery schedule. The more complete the technical information, the more accurately the tooling and production plan can be evaluated.
Conclusion
Heavy truck stamping parts play an important role in the safety, reliability, and service life of commercial vehicles. Frame brackets, suspension connecting plates, engine mounting supports, and related components must withstand vibration, impact, repeated loading, environmental exposure, and demanding operating schedules.
High-strength steel, advanced cold stamping, precise die construction, controlled forming, careful secondary processing, and strict inspection work together to produce dependable components. The most effective manufacturing approach is one that controls the complete chain from product engineering and tooling design to stamping, debugging, quality verification, packaging, and technical service.
Suzhou Shuangqisi Mold Equipment Co., Ltd. combines approximately 15 years of mold industry experience with a technical team, precision manufacturing equipment, 80-ton to 400-ton press capacity, stamping production resources, and stamping automation capabilities. This integrated foundation enables the company to support customized heavy truck components and broader die-and-automation projects.
For truck manufacturers, fleet service organizations, and aftermarket providers, the benefits extend beyond the individual metal part. A stable supplier can help improve assembly compatibility, production efficiency, component durability, maintenance planning, and total project value. Through coordinated engineering and manufacturing, heavy truck stamping parts can be developed to meet the demanding requirements of long-haul transportation, construction vehicles, and other heavy-duty applications.
References
1. General principles of sheet-metal forming and cold stamping process engineering.
2. Automotive engineering practices for chassis brackets, suspension components, and powertrain mounting structures.
3. Industrial guidance on high-strength steel selection, forming behavior, springback control, and fatigue performance.
4. Manufacturing quality-control practices for dimensional inspection, hardness verification, flatness evaluation, and surface protection.
5. Principles of stamping die design, precision machining, die maintenance, and production debugging.
6. Industrial practices for stamping automation, material handling, press-line integration, and operator safety.
7. Technical information supplied for the heavy truck stamping parts product line and associated manufacturing capabilities.
Product: Heavy truck stamping parts
Previous Post
Automatic Riveting Mold for Large Computer Machine Bases: Integrated Precision, Automation, and Reliable Production
Next Post
Deep Drawing Dies for Front and Rear Wheels of Two-Wheeled Electric Vehicles
Our Products.
Start Your Business with an OEM Manufacturer Right Here!

Provide global customers with complete turn-key solutions
through
innovation!
QUICK LINKS
CONTACT INFO.
-
 +86-139 1308 8972
-

-
 No. 118 Yexin Road, Wujiang Economic Development Zone, Suzhou, China
Copyright © Suzhou Shuangqisi Mold Equipment Co., Ltd. All Rights Reserved. Custom Stamping Die Metal Stamping Die Manufacturers
