 English
 Español
 Deutsch
-

Progressive Stamping Die for Connector & Terminal Parts High Speed Progressive Stamping Die Precision Metal Hardware Stamping Tool mold for Connector Terminal Parts Automotive Components
Progressive Stamping Die for Connector & Termi...
-
High Precision Stamping Die Multi Station Hardware Progressive Mold Tooling
Precision Metal Stamping Tool for Automotive &...
-
High Speed Progressive Stamping Die Sheet Metal Follow on Press Tool
Multi-operation Metal Stamping Tool for Continuous...
-
Progressive molds for automotive parts
This Continuous mold for automotive motor housing ...
-
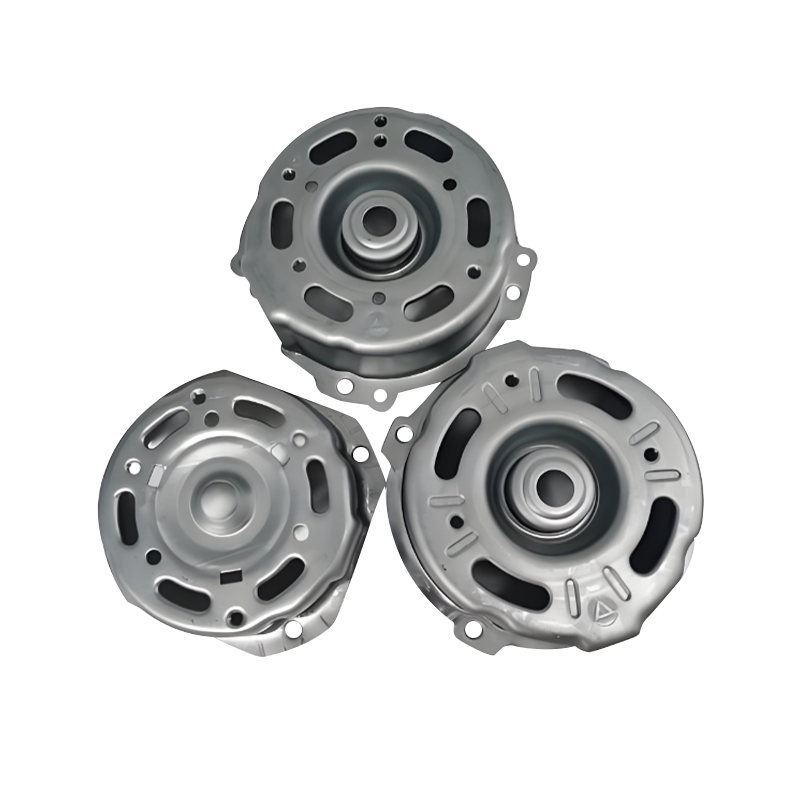
Automotive motor housing stamping parts
Automotive motor housing stamping parts are core c...
-

Long-Stroke Multi-Stage Progressive Die Automatic Strip Feed Progressive Die Long Travel Follow on Stamping Tool for Sheet Metal Hardware Press Moulding
Long-Stroke Multi-Stage Progressive DieOur custom ...
- E-mail us: [email protected]
- Call us: +86-139 1308 8972

Chen Siyi – Overseas Sales Manager
Home / Author / Chen Siyi – Overseas Sales Manager / Progressive Molds for Automotive Parts: Precision, Efficiency, and Reliable High-Volume Production
Progressive Molds for Automotive Parts: Precision, Efficiency, and Reliable High-Volume Production
2026-11-01
Progressive molds, also known as progressive stamping dies, are essential tools for the high-volume manufacture of automotive components. By combining several forming, piercing, drawing, bending, and trimming operations into one continuous production system, a progressive mold can transform metal strip or coil stock into accurately shaped parts with outstanding repeatability. For automotive motor housings and small-sized automotive parts, this manufacturing approach provides a practical balance of speed, dimensional control, material utilization, and long-term operating stability.
The progressive mold for automotive parts described in this article is engineered for continuous stamping and forming applications. It is particularly suitable for automotive motor housings and related components that require consistent wall thickness, accurate profiles, reliable fitting surfaces, and stable quality over extended production runs. The die is designed around the specific geometry and tolerance requirements of the finished component, allowing manufacturers to produce complex parts through a controlled sequence of operations.
In modern automotive manufacturing, the ability to produce large quantities of components without sacrificing quality is increasingly important. Vehicle manufacturers and suppliers must control production costs while meeting demanding requirements for safety, performance, assembly compatibility, and delivery speed. A well-designed progressive mold addresses these challenges by reducing manual intervention, shortening processing time, and integrating multiple manufacturing steps into a single coordinated tool.
Progressive molds for automotive parts
Content
- 1 What Is a Progressive Mold for Automotive Parts?
- 2 Application in Automotive Motor Housing Production
- 3 Integrated Stamping and Forming Process
- 4 Key Product Advantages
- 5 Advantages Compared with Conventional Multi-Stage Production
- 6 Engineering and Design Considerations
- 7 Advanced Manufacturing Capabilities
- 8 Modular Construction and Maintenance Benefits
- 9 Quality Control and Production Stability
- 10 Company Manufacturing Strengths
- 11 Stamping Automation and Production Integration
- 12 Economic Value Over the Tooling Life Cycle
- 13 Recommended Customer Development Process
- 14 Operating and Maintenance Recommendations
- 15 Comparison of Production Approaches
- 16 Why Choose an Integrated Tooling Supplier?
- 17 Applications Beyond Motor Housings
- 18 Environmental and Resource Considerations
- 19 Frequently Asked Questions
- 19.1 What type of parts is this progressive mold designed to produce?
- 19.2 What does “progressive” mean in stamping?
- 19.3 Can the mold perform deep drawing?
- 19.4 How does the mold maintain dimensional accuracy?
- 19.5 What materials are used to manufacture the die?
- 19.6 What is the benefit of modular construction?
- 19.7 Can the mold be used for high-volume production?
- 19.8 Does the supplier provide automation equipment?
- 19.9 What press capacity is available for testing or production?
- 19.10 How can customers reduce downtime?
- 19.11 Is the mold suitable for electric vehicle components?
- 19.12 What information is required for a quotation or technical evaluation?
- 20 Conclusion
- 21 References
- 22 Product: Progressive molds for automotive parts
What Is a Progressive Mold for Automotive Parts?
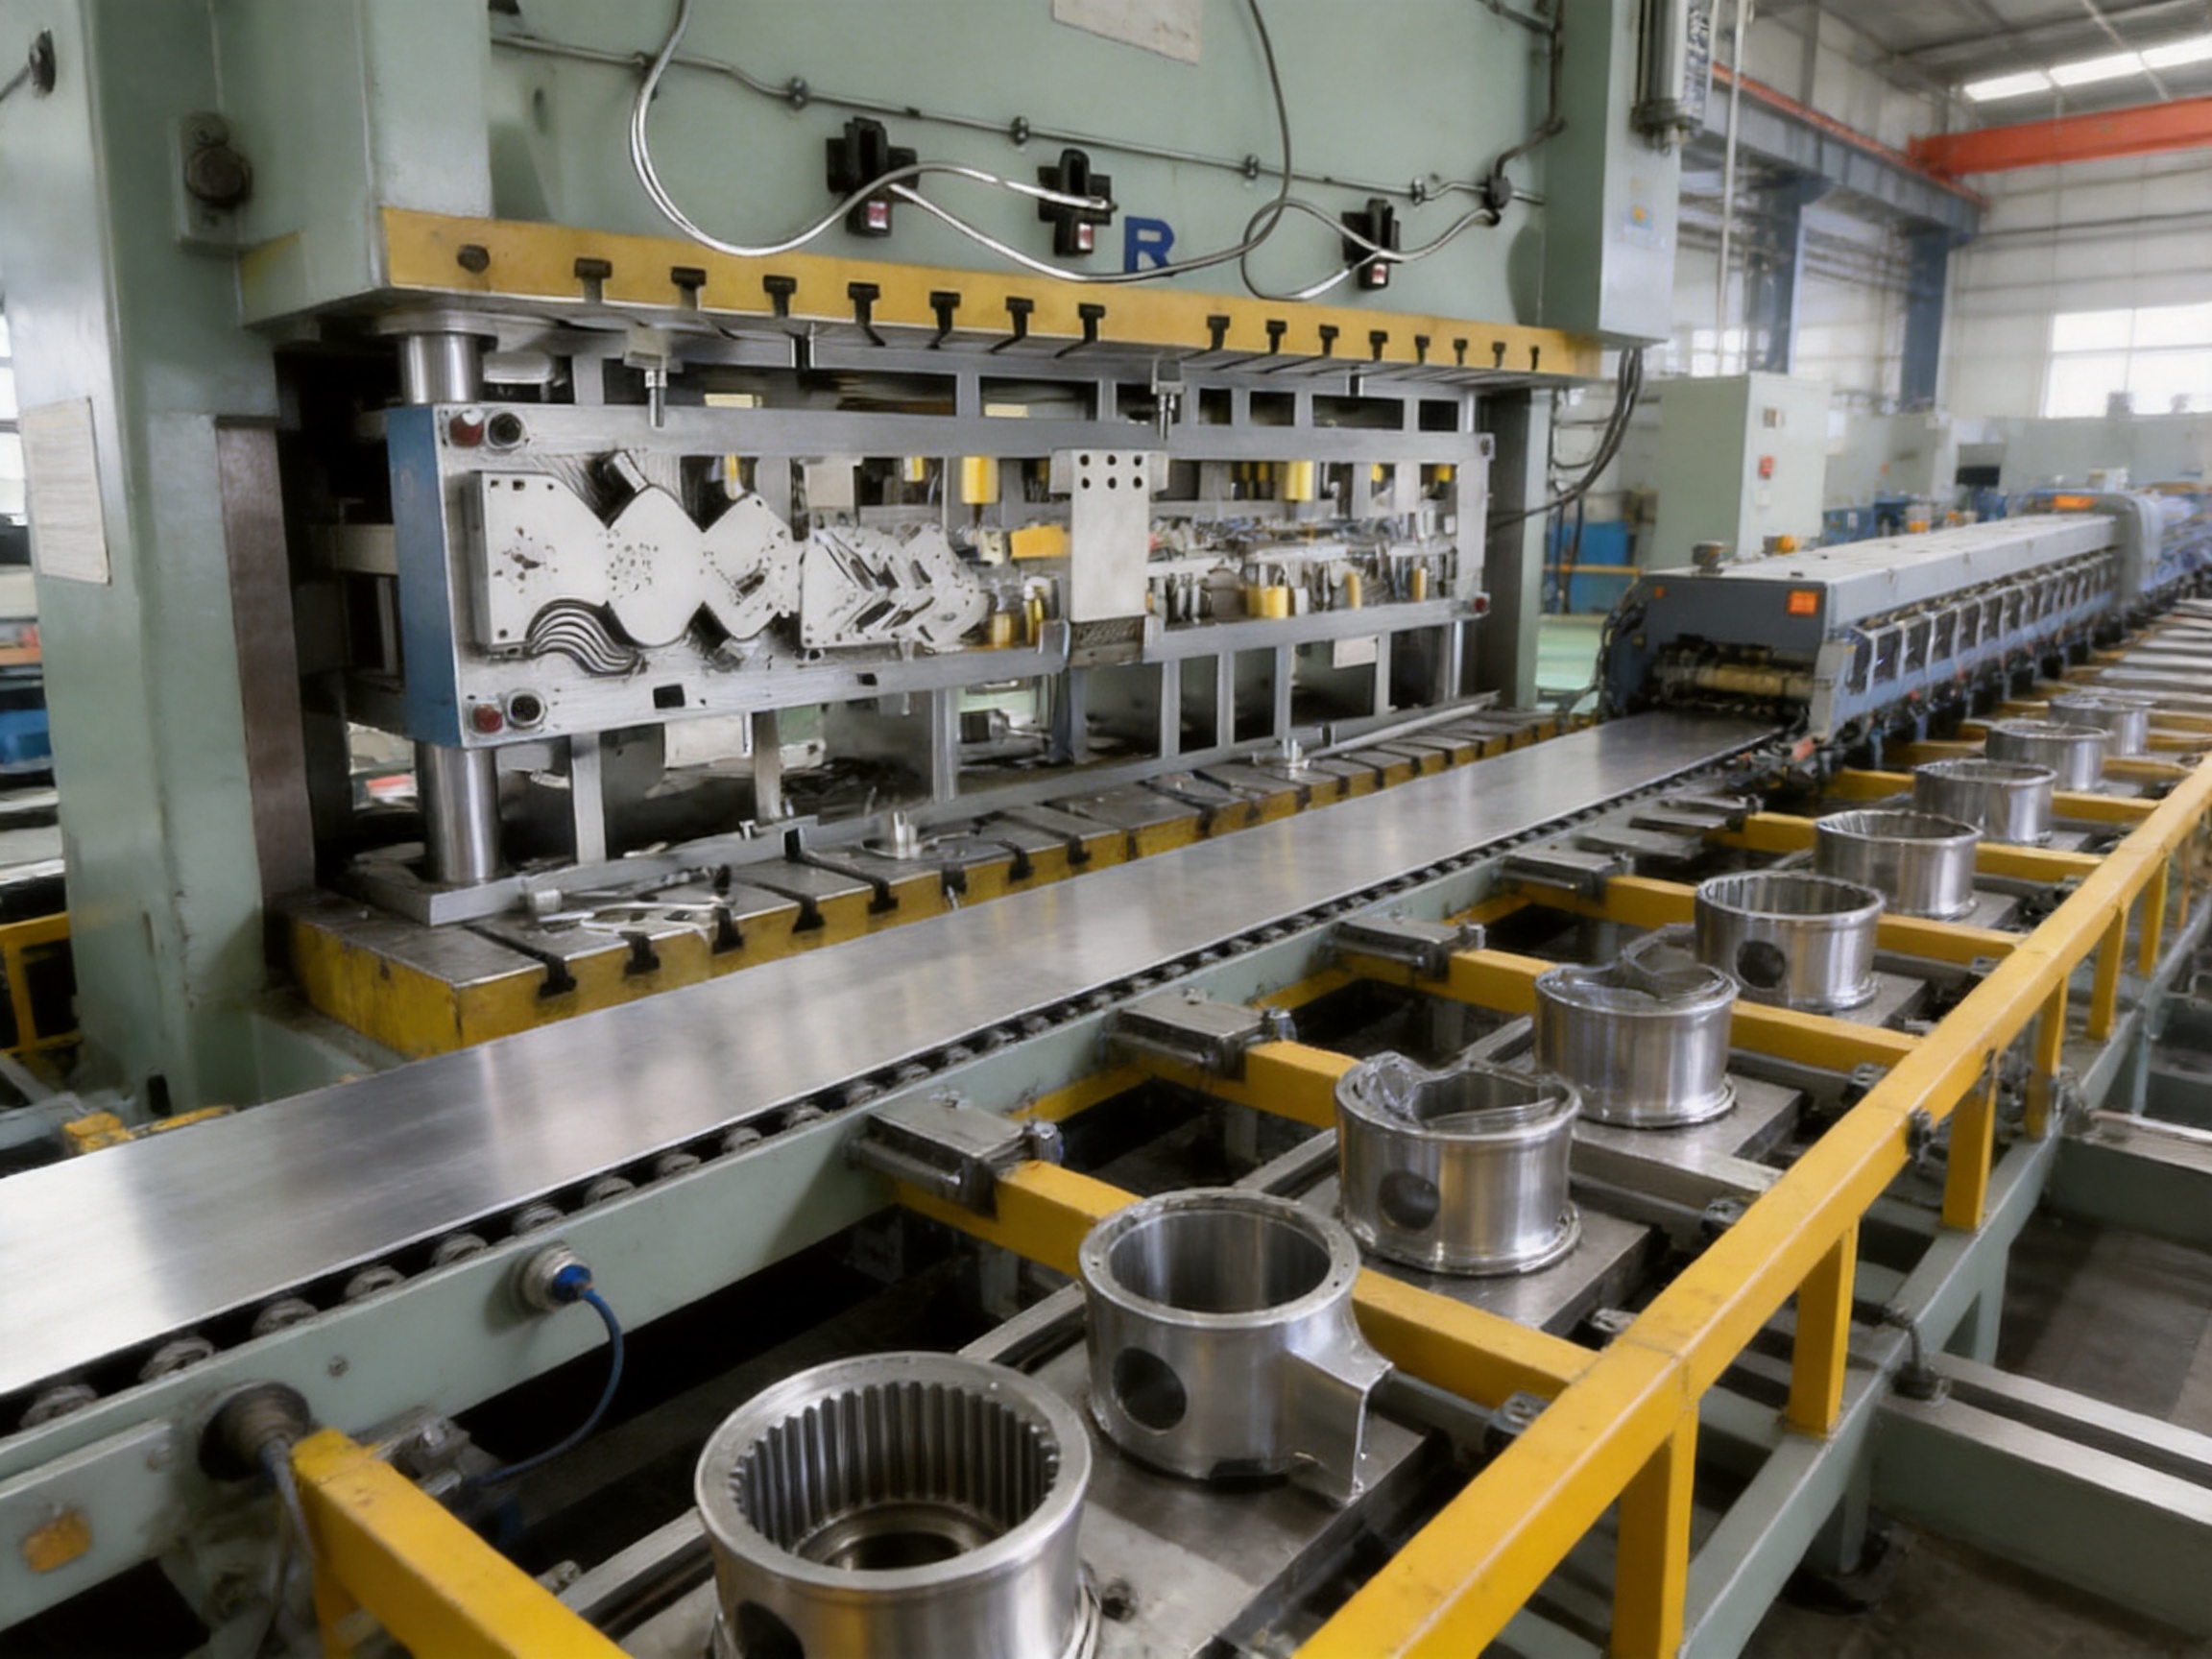
A progressive mold is a multi-station stamping die used with a mechanical or servo press. Metal strip is fed through the die in a controlled sequence. At each station, a particular operation is performed. These operations may include piercing, notching, blanking, drawing, embossing, bending, forming, restriking, and cutoff. As the strip advances from one station to the next, the partially formed component gradually reaches its final shape.
Unlike a single-operation die, which performs one primary manufacturing step at a time, a progressive mold integrates several operations into one production system. This arrangement allows the press to produce a finished or nearly finished component during every stroke after the strip has reached the final station. The result is a continuous production cycle with limited handling between operations.
For automotive motor housings, progressive tooling may be configured to create cylindrical, cup-shaped, flanged, or otherwise deep-formed components. The exact station layout depends on the material, part geometry, drawing depth, required radii, dimensional tolerances, and production volume. A carefully engineered layout ensures that deformation is distributed appropriately and that the material moves through the die without excessive stress or instability.
Progressive molds are especially valuable when the same component must be produced in large quantities with minimal variation. Once the die is installed, aligned, and properly adjusted, the production line can operate at a stable rhythm. This makes progressive stamping suitable for automotive powertrain components, motor housings, structural hardware, electrical parts, and other precision metal products.
Application in Automotive Motor Housing Production
Automotive motor housings must satisfy several functional requirements. They may need to protect internal components, provide accurate mounting surfaces, maintain a controlled internal diameter, and support proper assembly with other parts. Depending on the application, the housing may also need to meet requirements related to heat transfer, electromagnetic performance, vibration resistance, and structural stability.
These requirements place significant demands on the stamping die. The tooling must control the position of the workpiece throughout each operation, prevent unnecessary distortion, and maintain consistent forming conditions. If the drawing process is poorly designed, the material may develop wrinkles, cracks, uneven wall thickness, excessive thinning, or dimensional deviation. A high-quality progressive mold reduces these risks through coordinated station design and precise die construction.
The mold described for automotive motor housings is intended to support high-volume production of small and medium-sized automotive components. Its integrated stamping and forming process helps reduce production interruptions and allows the component to move through several operations in a predictable sequence. The resulting parts can be produced with uniform profiles and fitting surfaces that correspond to the assembly requirements of automotive powertrain systems.
For manufacturers of electric vehicles and hybrid vehicles, motor-related components are becoming increasingly important. Electric drive systems require housings and structural parts with accurate interfaces, stable dimensions, and dependable repeatability. Progressive stamping can help support these requirements by providing a controlled manufacturing process that is suitable for continuous operation and scalable production.
Integrated Stamping and Forming Process
The principal advantage of the progressive mold is its integrated production sequence. Instead of transferring workpieces manually between several separate dies, the material advances automatically through a series of stations. Each station is designed to perform a defined operation while preserving the reference position required by the following station.
A typical process may begin with strip feeding and pilot location. Initial stations may create pilot holes, notches, or preliminary contours. Subsequent stations can perform drawing or forming operations, gradually developing the height and shape of the housing. Additional stations may create openings, mounting features, flanges, grooves, or other functional details. The final stations can complete trimming, calibration, restriking, or cutoff.
This integrated approach offers several production benefits. It reduces the number of separate setups, limits handling damage, and improves process consistency. It also makes it easier to maintain a repeatable relationship between features because the component remains connected to the strip until the appropriate point in the sequence.
Progressive forming is particularly advantageous for parts that contain multiple features positioned relative to one another. When individual operations are carried out in separate tools, cumulative positioning errors can affect the finished component. With a progressive mold, the stations are designed as one coordinated system, helping maintain the relationship between holes, edges, drawn walls, flanges, and forming surfaces.
The integrated design also supports automation. Coil stock can be loaded into a feeder, straightened, lubricated where appropriate, and delivered to the press at a controlled pitch. Sensors can monitor strip position, material presence, die protection, and press operation. This enables stable production with reduced dependence on manual handling.
Key Product Advantages
High Production Efficiency
A progressive mold is designed for continuous operation. Once the press reaches the required operating condition, each stroke can produce a part or advance a component toward completion. This high-throughput approach is more efficient than manufacturing the same part through a series of independent operations with separate loading and unloading steps.
Higher productivity is especially valuable in automotive supply chains, where component demand can be substantial and delivery schedules are strict. The reduction in manual transfer and setup time allows manufacturers to use press capacity more effectively. It can also reduce labor requirements associated with repetitive part movement and intermediate inspection.
Consistent Dimensional Accuracy
Automotive components often require close control of critical dimensions. A motor housing may need to fit with bearings, shafts, covers, electrical assemblies, brackets, or other powertrain components. Small deviations in diameter, height, flange position, or mounting-hole location can create assembly problems or affect product performance.
The progressive mold supports dimensional consistency by using fixed station relationships, precision guide systems, controlled material feeding, and carefully prepared forming surfaces. When the die is correctly maintained and operated within its design parameters, it can produce parts with stable dimensions across long production runs.
Uniform Wall Thickness and Formed Profiles
Deep drawing and progressive forming require careful control of material flow. Excessive deformation at one station can lead to local thinning, tearing, or distortion. By distributing the forming work across several stages, the die can manage the material more gradually.
This staged approach is beneficial for motor housings and other deep-drawn components that require consistent wall sections. Uniform wall thickness can improve structural reliability, dimensional stability, and the fit of mating components. It may also support more predictable performance during subsequent machining, coating, assembly, or testing.
Reduced Production Downtime
The mold uses a modular construction concept that allows damaged or worn components to be replaced more efficiently. Instead of rebuilding an entire die when a localized component requires service, maintenance personnel can often remove and replace the relevant insert, punch, guide element, or forming component.
Modular maintenance reduces the time required for corrective work and supports faster return to production. This is important in high-volume manufacturing environments, where extended press downtime can affect delivery schedules and increase operating costs.
Long-Term Wear Resistance
The mold is constructed with high-hardness alloy steel components selected for demanding stamping conditions. Proper material selection is important because stamping dies are exposed to repeated mechanical loading, sliding contact, impact, friction, and, in some applications, abrasive material behavior.
High-hardness alloy steel can provide strong resistance to wear and deformation when it is correctly heat-treated, machined, finished, and maintained. Stable tooling surfaces help preserve the intended geometry of the die over time. This contributes to reliable part quality and reduces the frequency of major tooling corrections.
Suitability for Mass Production
The progressive mold is intended for high-volume manufacturing rather than occasional or low-output production. Its design emphasizes repeatability, automation compatibility, efficient material flow, and fast cycle operation. These characteristics make it appropriate for automotive component programs in which the same part must be produced consistently over an extended period.
For customers comparing tooling options, the ability to combine production speed with quality control is a major advantage. A low-cost die that produces inconsistent parts or requires frequent adjustment may create greater total expense than a precision die with a higher initial investment. The progressive mold is designed to provide value throughout the complete production lifecycle.
Advantages Compared with Conventional Multi-Stage Production
Conventional production may use multiple independent dies, with operators or transfer equipment moving workpieces from one process to the next. This approach can be appropriate for certain shapes, materials, or production volumes, but it often introduces additional handling, setup, inspection, and storage requirements.
A progressive mold reduces these intermediate steps. The strip remains under controlled guidance while it passes through the tool, reducing the risk of orientation errors and inconsistent positioning. The manufacturer can also reduce work-in-process inventory because components do not need to accumulate between separate operations.
Another advantage is process integration. When drawing, piercing, forming, and trimming operations are planned together, the die designer can consider their interactions from the beginning. This makes it possible to optimize the sequence for material flow, tool strength, production speed, and part quality.
Progressive stamping may also reduce the floor space required for production. Several operations that would otherwise require separate presses or workstations can be integrated into one press line. The resulting layout can support more efficient use of factory space and simplify production supervision.
Compared with manual or semi-manual forming, progressive production offers improved repeatability. Human operators remain important for setup, inspection, maintenance, and process control, but the repetitive positioning and transfer functions are performed by the tooling and feeding system. This can help reduce variation caused by fatigue or inconsistent handling.
Engineering and Design Considerations
Material Selection
The design of a progressive mold begins with the material to be stamped. Automotive components may be made from carbon steel, stainless steel, aluminum alloys, electrical steel, or other sheet materials. Each material has different strength, ductility, springback behavior, surface characteristics, and forming limits.
The die must be matched to the material thickness and mechanical properties. A design suitable for a thin, ductile sheet may not be appropriate for a high-strength material. Drawing clearances, punch radii, die radii, blank-holder conditions, and station spacing must be evaluated according to the material and part geometry.
Part Geometry and Forming Sequence
The geometry of the motor housing determines how the forming work should be divided among the stations. A deep or complex shape may require several drawing stages. Features such as beads, ribs, holes, flanges, and local embossments may need to be introduced at specific points in the sequence to avoid interference or distortion.
The forming sequence must also consider when the material remains connected to the carrier strip and when the finished part is separated. Cutting too early may reduce stability, while cutting too late may complicate part removal. The engineering team must balance accessibility, part support, material utilization, and production speed.
Strip Layout and Material Utilization
Strip layout has a direct effect on material cost. An efficient layout minimizes scrap while providing adequate carrier strength and sufficient space for each station. The layout must support reliable feeding and prevent the strip from twisting, buckling, or losing alignment.
For automotive parts produced in large quantities, even a small improvement in material utilization can generate substantial savings over the lifetime of the program. Progressive mold design therefore considers not only the die itself but also the relationship between part orientation, pitch, carrier design, and scrap management.
Guidance and Alignment
Accurate guidance is essential for progressive stamping. Guide posts, guide plates, pilots, pressure elements, and precision locating features work together to keep the die halves aligned and the strip positioned correctly. Alignment errors can cause uneven wear, poor cutting quality, dimensional deviation, and damage to punches or inserts.
The tooling must also maintain stable alignment under press load. This requires appropriate structural support and careful machining of the die components. Proper alignment improves the service life of the tool and supports repeatable part quality.
Press Compatibility
A progressive mold must be matched to a suitable press. Important factors include rated tonnage, available stroke, shut height, bed dimensions, press speed, feeder capacity, and control system compatibility. The press must provide sufficient force for the most demanding station while maintaining stable operation across the complete cycle.
The manufacturer’s available equipment includes punch presses ranging from 80 tons to 400 tons. This range supports a variety of stamping applications and allows tooling projects to be evaluated according to part size, material, forming requirements, and production volume.
Advanced Manufacturing Capabilities
High-quality stamping dies depend on the accuracy of the manufacturing process used to produce them. Even a well-developed design can fail to deliver reliable performance if the die components are poorly machined, inadequately finished, or incorrectly assembled. For this reason, the manufacturing capabilities of the tooling supplier are as important as the initial concept.
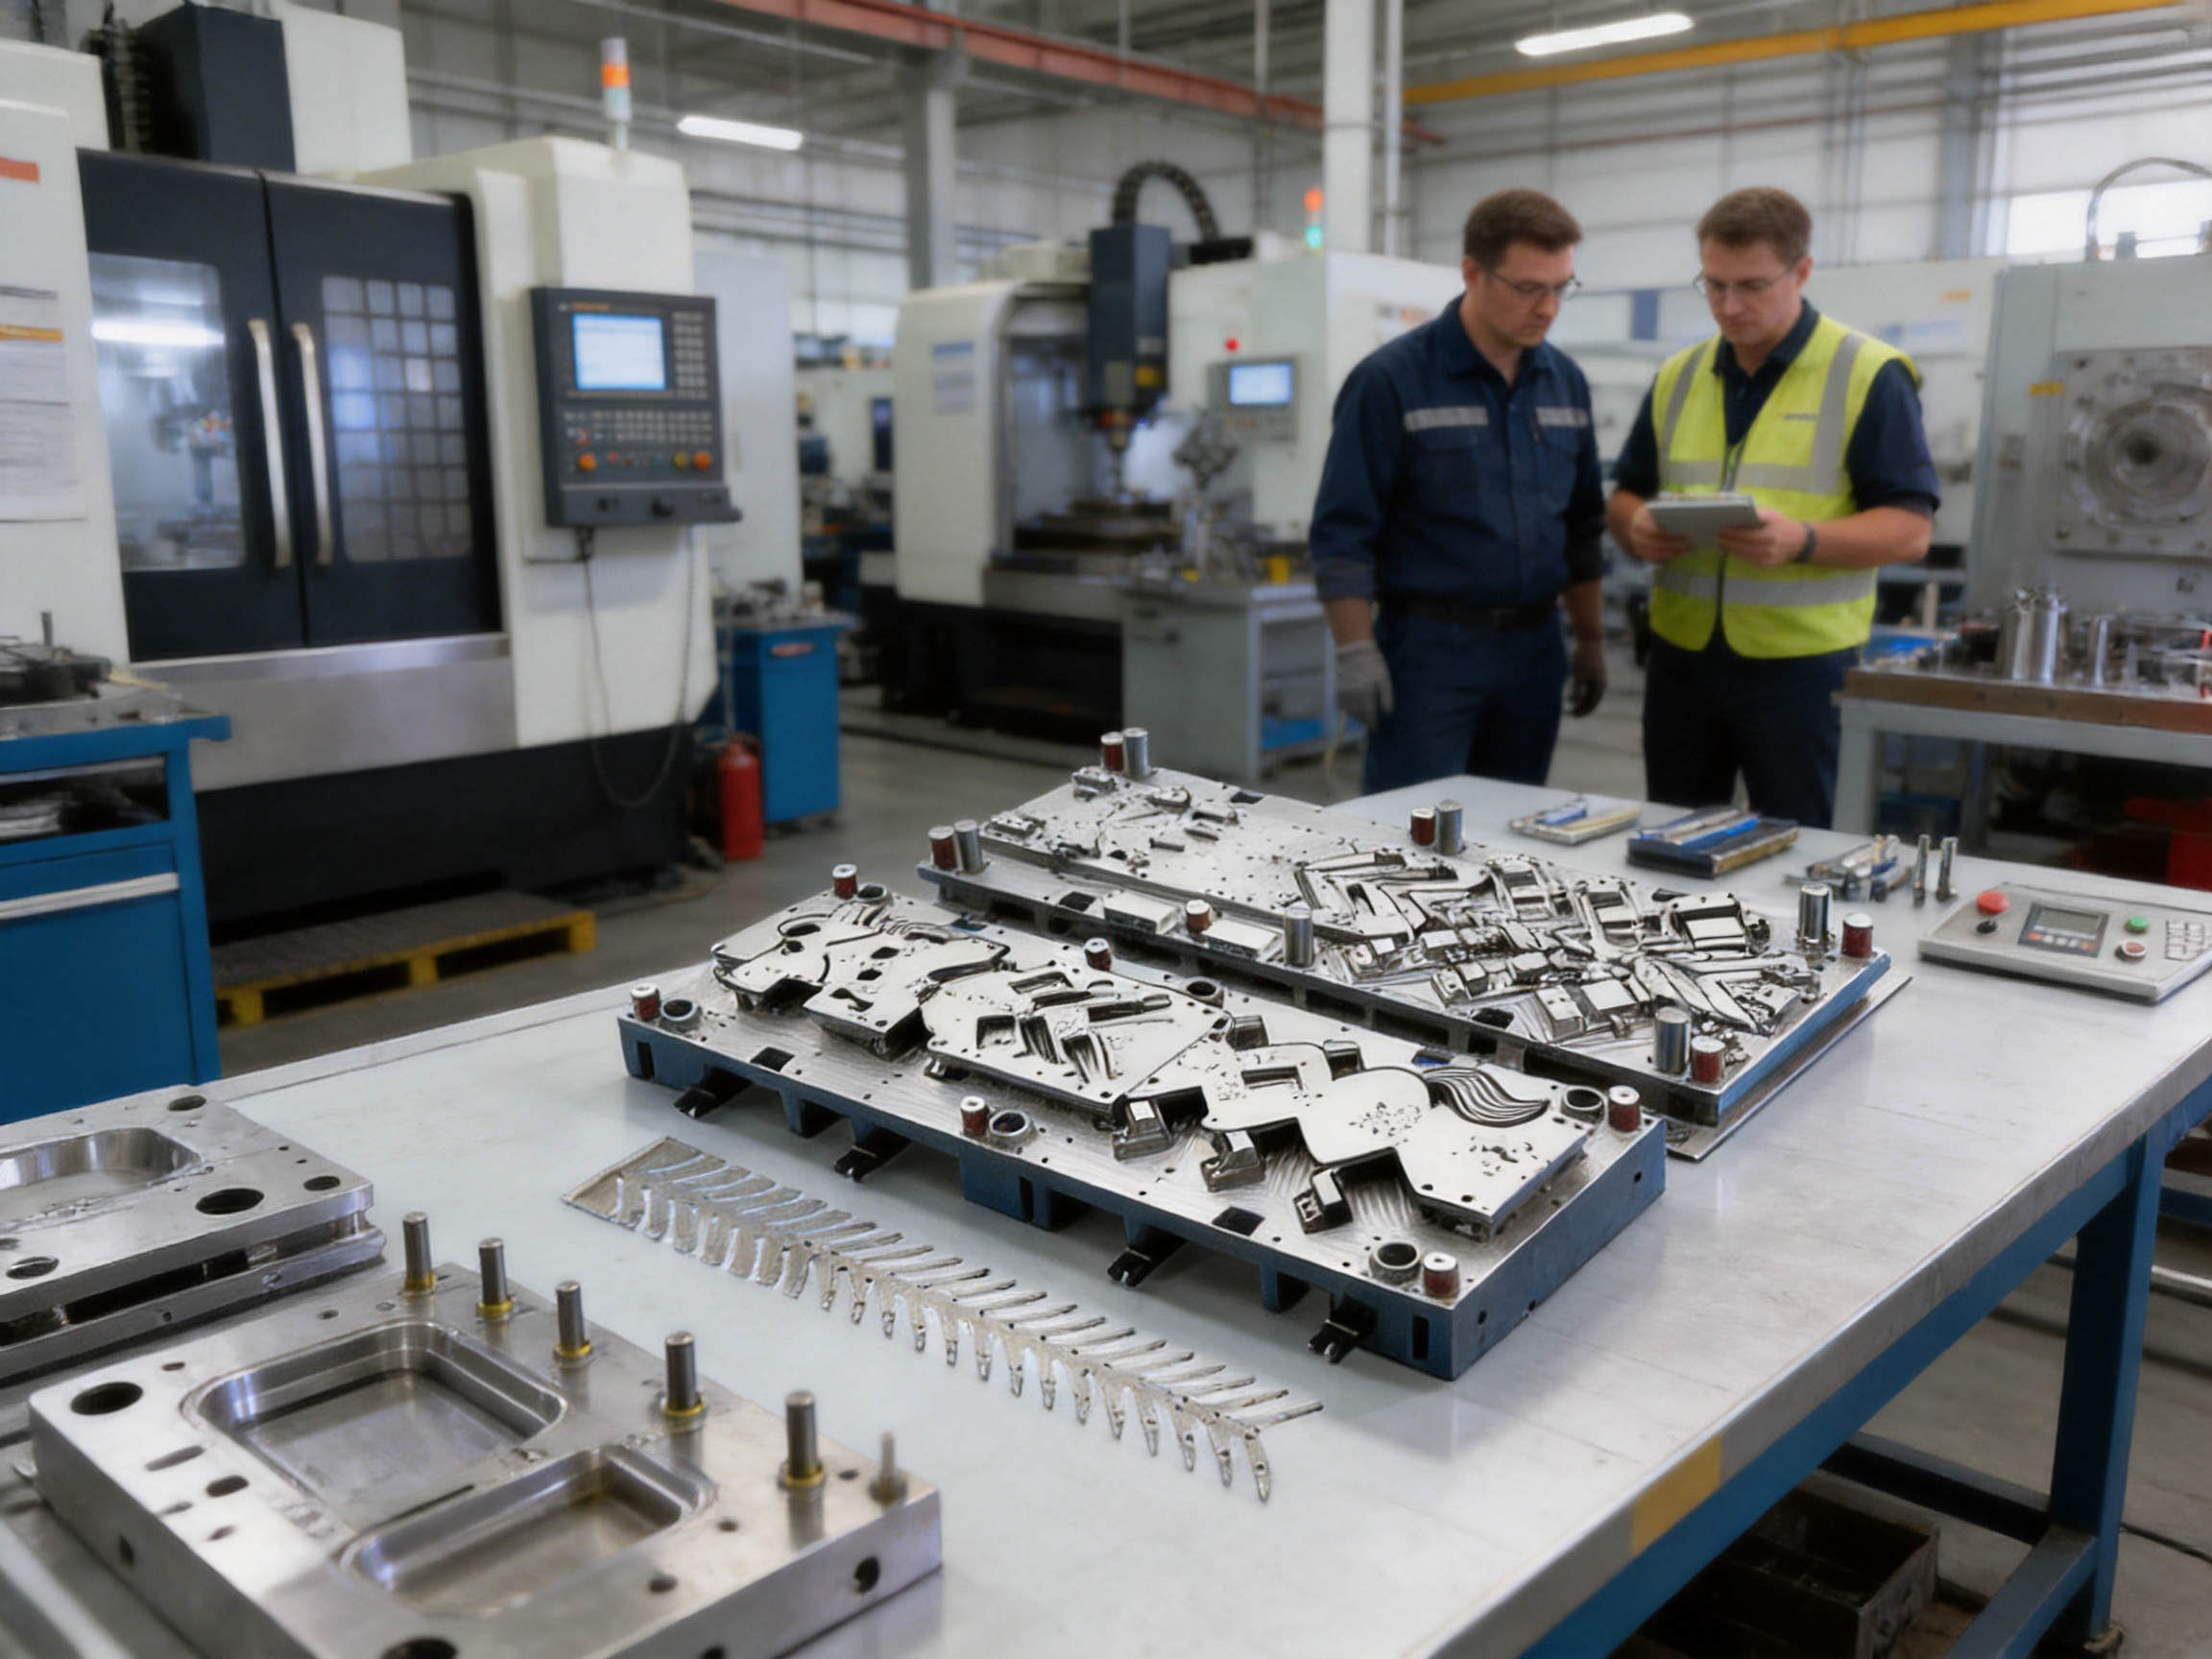
Suzhou Shuangqisi Mold Equipment Co., Ltd. integrates die design, machining, assembly, debugging, and service. Its production resources include imported wire-cutting machines, CNC machining centers, more than ten grinding machines of different sizes, and a range of punch presses. These capabilities support the manufacture and testing of precision stamping dies for automotive, electrical, compressor, servo-drive, and new-energy applications.
Wire cutting is useful for producing accurate profiles and fine features in hardened or difficult-to-machine materials. CNC machining centers provide controlled milling for die plates, inserts, holders, cavities, and complex three-dimensional surfaces. Grinding equipment supports the finishing of critical planes, guide surfaces, cutting edges, and forming elements.
The combination of these processes helps the manufacturer control the relationship between design data and finished tooling. Precision machining is followed by fitting, assembly, inspection, and debugging. This integrated workflow can reduce communication gaps between separate suppliers and make it easier to resolve design or production issues during development.
Design and Process Planning
Successful progressive tooling begins with a detailed understanding of the part and its production requirements. Engineers must review the component drawing, material specification, tolerance requirements, target output, press information, feeding method, and quality expectations.
Based on this information, the tooling team can develop the strip layout and station sequence. The design process may include analysis of drawing ratios, forming limits, cutting clearances, material flow, carrier strength, scrap separation, and maintenance access. Each decision affects the performance of the completed die.
A practical design must also consider production realities. It should allow operators to inspect the tool, replace wear components, remove scrap, adjust sensors, and perform routine lubrication. A die that is theoretically capable of producing a part but difficult to maintain may not deliver the best value in a real factory environment.
Precision Machining
Machining accuracy influences the fit and function of every die component. CNC equipment can be used to produce complex surfaces and precise hole patterns, while wire cutting can create accurate profiles and narrow clearances. Grinding provides a controlled finish on surfaces that require close flatness or dimensional control.
High-quality machining is especially important for progressive molds because the stations must work together. A small error in one component can affect the alignment of another component or change the way material flows through the die. Careful machining helps preserve the intended sequence and reduces the need for excessive adjustment during tryout.
Assembly and Tryout
After machining, the components are assembled into the complete mold. The assembly process includes fitting plates, installing punches and inserts, checking guide systems, setting clearances, and verifying the operation of moving elements. The die is then tested under controlled conditions.
Tryout allows the manufacturing team to evaluate the actual stamping process. Sample parts can be inspected for dimensions, surface condition, cracks, wrinkles, burrs, incomplete forming, and other defects. If necessary, the die can be adjusted or refined before delivery to the customer.
Experienced debugging personnel are important during this stage. They understand how changes in clearance, punch radius, forming pressure, feed position, or timing can affect the final part. Their practical knowledge complements the design and machining capabilities of the engineering team.
Modular Construction and Maintenance Benefits
Automotive stamping dies operate under repeated mechanical stress. Even a well-designed tool eventually requires preventive maintenance, replacement of wear parts, or adjustment of process elements. A modular die structure makes these activities more manageable.
Modular construction allows selected components to be removed without dismantling the entire mold. Replaceable inserts can be used in areas subject to concentrated wear, such as cutting edges, drawing surfaces, guide elements, or local forming features. This approach can reduce repair time and limit the cost of replacing large die sections.
Maintenance accessibility also supports better preventive care. Operators and technicians can inspect critical parts, clean scrap and contaminants, check fasteners, verify lubrication, and monitor wear before a serious failure occurs. Planned maintenance is generally less disruptive than emergency repair after a breakdown.
The modular approach is also useful when a customer needs engineering changes. Automotive programs may evolve during development, and certain features may require revision after testing or assembly evaluation. Replaceable sections can make selected modifications more practical than redesigning the entire die.
Quality Control and Production Stability
Quality control for progressive molds covers both the tooling and the parts produced by the tooling. During die manufacturing, critical dimensions, surface finishes, hole positions, clearances, and component fit must be checked. During tryout, the finished parts must be evaluated against the customer’s technical requirements.
Production stability depends on more than one inspection report. The feeding system, press condition, material consistency, lubrication, sensor settings, and operator procedures all influence the result. A robust mold should be designed to tolerate normal production variation while maintaining appropriate control of critical features.
For automotive motor housings, quality checks may include external dimensions, internal dimensions, height, flange geometry, wall thickness, hole location, surface condition, burr height, and assembly fit. The exact inspection plan depends on the customer’s drawing and application requirements.
Stable tooling also helps reduce quality-related waste. If a die produces inconsistent parts, the manufacturer may need to increase inspection frequency, sort components, rework parts, or scrap nonconforming material. A precision progressive mold helps reduce these secondary costs by supporting repeatable production from the beginning.
Company Manufacturing Strengths
Suzhou Shuangqisi Mold Equipment Co., Ltd. is a professional manufacturer of stamping dies and hardware parts that integrates design, manufacturing, and service. The company has approximately 60 technical staff and more than 15 years of experience in the mold industry. This combination of personnel, equipment, and practical experience supports projects that require both engineering capability and manufacturing discipline.
The company’s equipment base includes imported wire-cutting machines, CNC machining centers, more than ten grinding machines of various sizes, and 25 punch presses with capacities ranging from 80 tons to 400 tons. These resources provide a foundation for producing and testing a broad range of stamping dies and metal parts.
Its customer applications include servo drives, compressors, automotive components, and new-energy vehicle products. Experience across these sectors can be valuable because each application requires attention to different combinations of precision, strength, electrical function, heat management, assembly, and production volume.
The company also has experience in stamping automation equipment through its investment in Suzhou Keshuang Intelligent Technology Co., Ltd. This creates an opportunity to coordinate tooling and automation rather than treating them as completely separate projects. For customers seeking a complete production solution, the combination of progressive molds and automated feeding or transfer equipment can simplify project coordination.
A turnkey approach may include die design, mold manufacturing, press compatibility review, automation planning, debugging, and production support. This integrated service can help customers reduce the number of suppliers involved in a project and establish clearer responsibility for the complete stamping process.
Stamping Automation and Production Integration
Automation is an important complement to progressive molds. The die controls the forming sequence, while automation equipment manages material feeding, part transfer, scrap removal, monitoring, and other production functions. When these systems are designed together, the line can operate with improved coordination and reduced manual intervention.
Automation may include decoilers, straighteners, servo feeders, lubrication units, sensors, conveyors, collection systems, and control interfaces. The appropriate configuration depends on the strip material, coil size, part geometry, press type, target cycle rate, and factory layout.
For high-volume automotive production, automated feeding can improve pitch accuracy and reduce the risk of incorrect strip positioning. Automated monitoring can also stop the press when a fault is detected, helping prevent damage to the die and reducing the number of defective parts produced during an abnormal condition.
Integrated automation supports safer and more consistent operation. Operators can focus on setup, inspection, material loading, maintenance, and process supervision rather than repeatedly reaching into the production area to move parts. Safety design must still comply with the applicable equipment and workplace requirements.
Economic Value Over the Tooling Life Cycle
The value of a progressive mold should be evaluated over its full service life rather than only by its initial purchase price. Important cost factors include material utilization, press utilization, labor, setup time, maintenance, scrap, downtime, tooling replacement, and production output.
A well-designed die may require a higher initial investment than a simple single-operation tool, but its integrated process can reduce recurring production costs. Fewer handling steps, shorter cycle times, lower work-in-process inventory, and improved repeatability can contribute to a lower cost per part at sufficient production volumes.
Material efficiency is another important consideration. The strip layout should use material effectively while retaining enough carrier strength for reliable feeding. In high-volume production, scrap reduction can have a meaningful effect on operating costs, particularly when the raw material is expensive or the component requires a large blank.
Maintenance costs are also influenced by die construction. Replaceable wear components and accessible service areas can shorten maintenance activities and reduce the likelihood that a localized problem will require a complete tooling rebuild. This supports greater equipment availability and more predictable production planning.
Recommended Customer Development Process
Step One: Technical Requirement Review
The project should begin with a review of the part drawing, three-dimensional data, material grade, thickness, tolerances, surface requirements, production volume, and application. Information about the customer’s press, feeder, coil dimensions, and factory layout is also useful.
Step Two: Feasibility and Process Analysis
The tooling team evaluates whether the part is suitable for progressive stamping and determines the likely forming sequence. Potential risks such as excessive drawing depth, tight radii, springback, difficult material flow, or limited carrier space should be identified at this stage.
Step Three: Strip Layout and Die Design
The design team develops the strip layout, station sequence, die structure, cutting clearances, guide system, sensor arrangement, and maintenance plan. Customer feedback can be incorporated before machining begins.
Step Four: Tool Manufacturing
Die plates, inserts, punches, forming components, guide elements, and other parts are machined using suitable CNC, wire-cutting, grinding, and finishing processes. Critical dimensions are inspected throughout production.
Step Five: Assembly and Tryout
The mold is assembled and tested with the intended material and suitable press conditions. Sample parts are inspected, and required adjustments are made to achieve the target quality and production stability.
Step Six: Delivery and Production Support
After approval, the mold can be delivered with relevant technical information, maintenance guidance, and operating recommendations. Continued communication between the supplier and customer can help address process questions and support long-term performance.
Operating and Maintenance Recommendations
Correct operation is essential for protecting the die and maintaining part quality. The press should be set according to the approved operating parameters, including stroke, speed, shut height, feed pitch, and material specification. The strip should be straight, correctly positioned, and free from contamination that could affect feeding or forming.
Regular inspection should focus on cutting edges, forming surfaces, guide components, pilots, springs, sensors, fasteners, and scrap passages. Abnormal noise, increased burrs, dimensional drift, surface marks, or changes in press load may indicate wear or misalignment.
Lubrication should follow the conditions established for the specific material and forming process. Too little lubrication can increase friction and wear, while inappropriate or excessive lubrication may affect part cleanliness or downstream operations. The maintenance schedule should identify the correct lubricant and application method.
When a component reaches its service limit, it should be replaced or refurbished promptly. Continuing to operate with severely worn parts can damage adjacent components and increase the scope of repair. Proper storage and handling are also important when the mold is removed from the press or transported between facilities.
Comparison of Production Approaches
| Production Approach | Typical Characteristics | Advantages | Limitations |
|---|---|---|---|
| Progressive stamping | Multiple operations integrated into one continuous die | High output, repeatable positioning, reduced handling, strong automation potential | Higher initial design complexity and tooling investment |
| Single-operation stamping | One principal operation performed per die | Simple tooling concept and flexible for selected low-volume parts | More transfers, more setups, and potentially higher labor cost |
| Manual multi-stage production | Operators move parts between separate processes | Useful for prototypes, small batches, or changing product requirements | Lower consistency, slower output, and greater handling dependency |
| Machining from solid material | Material removed through cutting operations | Suitable for certain complex prototypes and low-volume components | Longer cycle time, greater material waste, and limited economic value for high volume |
| Transfer stamping | Parts are separated and transferred between forming stations | Suitable for larger or more complex components requiring individual handling | More transfer equipment and greater system complexity |
The progressive approach is particularly competitive when the component has a stable design, high annual demand, and multiple stamping operations that can be combined into one tool. It may not be the best choice for every part, but for automotive motor housings and small automotive components requiring continuous production, it offers a strong combination of productivity and control.
Why Choose an Integrated Tooling Supplier?
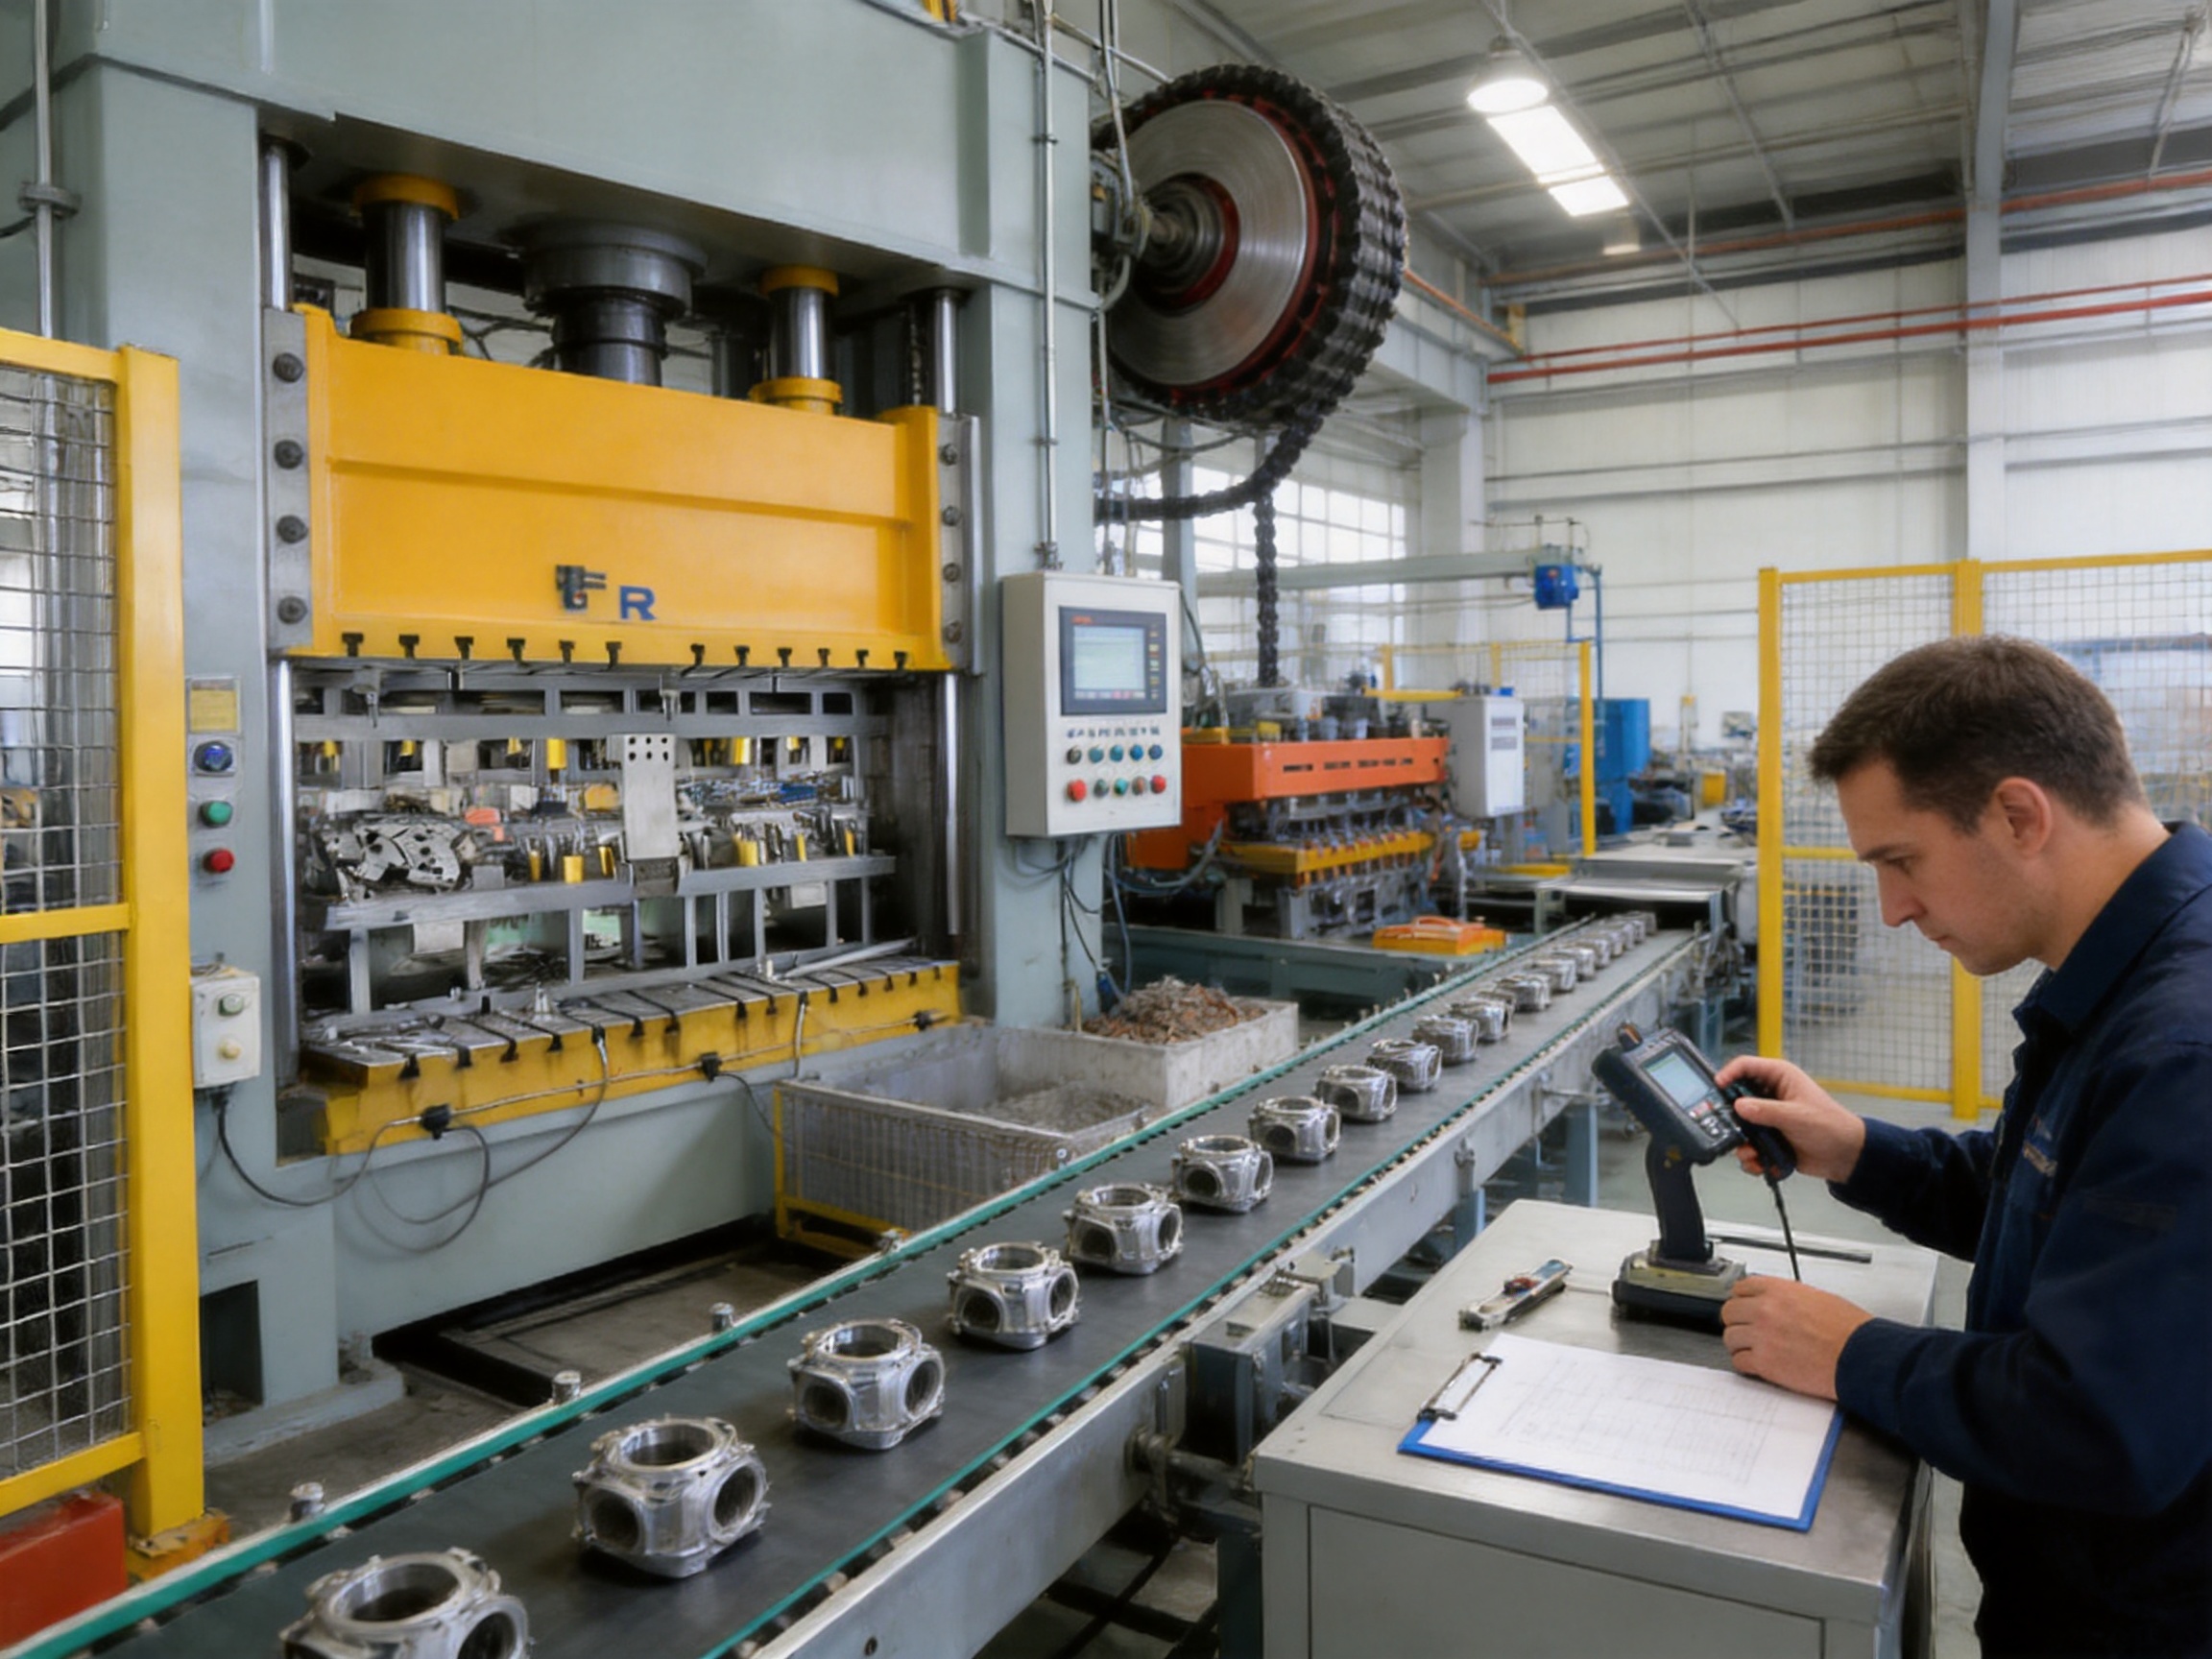
Selecting a supplier that can provide design, machining, assembly, debugging, and automation support can simplify the development of a stamping project. The customer can communicate technical requirements to one coordinated team, while the supplier can evaluate the relationships between the mold, press, feeder, and production process.
An integrated supplier can also identify practical issues earlier. For example, a die design may be technically sound but difficult to load into the customer’s press. An automation arrangement may meet the required cycle rate but lack sufficient access for maintenance. Coordinated engineering helps address these concerns before they create delays during installation.
The manufacturing capabilities of Suzhou Shuangqisi Mold Equipment Co., Ltd. support this integrated model. Its technical staff, precision machining resources, stamping capacity, and automation-related capabilities provide a foundation for complete solutions rather than isolated tooling supply.
The company’s approach emphasizes competitive pricing, quality control, customer value, and long-term technical development. Its experience serving customers in automotive, compressor, servo-drive, and new-energy-related applications demonstrates the ability to work with industrial components that require precision and reliable production performance.
Applications Beyond Motor Housings
Although the mold described here is focused on automotive motor housings and small automotive parts, the same progressive tooling principles can be applied to many other products. Potential applications include brackets, covers, shielding parts, terminals, electrical housings, fastening components, structural reinforcements, compressor parts, and components for electric drive systems.
The final application depends on the material, part shape, production volume, and required tolerances. A customized die must be developed for each component rather than assuming that one standard tool can serve all products. The supplier’s experience with different industries can help adapt the process to the specific technical requirements.
As vehicle platforms continue to evolve, manufacturers may require lighter materials, more complex geometries, tighter assembly requirements, and higher levels of automation. Progressive molds can be adapted to these trends through improved station design, precision machining, sensor integration, and modular construction.
Environmental and Resource Considerations
Efficient stamping can contribute to responsible resource use by reducing unnecessary material waste and limiting repeated heating or remanufacturing operations. Progressive dies are generally used with cold sheet forming, allowing manufacturers to produce parts through mechanical operations without the energy requirements associated with many thermal forming processes.
Material utilization depends heavily on the strip layout and component geometry. An experienced tooling team can evaluate part orientation, carrier width, pitch, and scrap separation to achieve a practical balance between efficient material use and stable production. The correct balance is important because an extremely narrow layout may reduce scrap but create feeding or structural problems.
Long tool life also supports resource efficiency. Durable die components reduce the need for frequent replacement and help maintain consistent production over an extended period. Preventive maintenance, repairable modules, and responsible management of worn parts can further improve the lifecycle performance of the tooling system.
Frequently Asked Questions
What type of parts is this progressive mold designed to produce?
The mold is designed primarily for automotive motor housings and small-sized automotive parts that require continuous stamping and forming. The exact part range depends on the approved design, material, dimensions, and production requirements.
What does “progressive” mean in stamping?
Progressive means that the metal strip advances through multiple stations inside one die. Each station performs a specific operation, and the component becomes more complete as it moves through the sequence.
Can the mold perform deep drawing?
Yes. The product category includes automotive and electric vehicle deep drawing dies, and the mold is engineered for forming applications such as motor housings. The number and arrangement of drawing stages depend on the part geometry and material properties.
How does the mold maintain dimensional accuracy?
Dimensional accuracy is supported by coordinated station design, precision-machined components, guide and pilot systems, controlled feeding, suitable clearances, and tryout adjustments. Correct press setup and regular maintenance are also necessary for stable production.
What materials are used to manufacture the die?
The mold uses high-hardness alloy steel components selected for wear resistance and long-term stamping performance. The final material and heat-treatment specifications are determined according to the working conditions, material being stamped, and required service life.
What is the benefit of modular construction?
Modular construction allows selected worn or damaged components to be replaced without rebuilding the complete die. This can shorten maintenance time, reduce repair cost, and help restore production more quickly.
Can the mold be used for high-volume production?
Yes. High-volume continuous production is one of the main purposes of the mold. Its integrated process, automation compatibility, durable construction, and repeatable forming sequence are suited to mass-production environments.
Does the supplier provide automation equipment?
The company has automation-related capabilities through its associated intelligent technology business and can provide stamping automation solutions. Depending on the project, this may include coordination between the mold, press, feeding system, and other production equipment.
What press capacity is available for testing or production?
The company operates punch presses ranging from 80 tons to 400 tons. The appropriate press depends on the component, material, die dimensions, forming force, and production requirements.
How can customers reduce downtime?
Customers can reduce downtime through modular die construction, preventive maintenance, regular inspection, correct lubrication, proper press setup, and early replacement of worn components. Automation monitoring can also help identify abnormal conditions before serious damage occurs.
Is the mold suitable for electric vehicle components?
Yes. The mold is categorized for automotive and electric vehicle deep drawing applications. It can be developed for components used in electric drive systems and other new-energy vehicle assemblies when the part design and production conditions are suitable.
What information is required for a quotation or technical evaluation?
Useful information includes the part drawing or three-dimensional model, material grade, material thickness, annual quantity, tolerance requirements, surface requirements, available press details, coil dimensions, and desired automation level. This information helps the engineering team evaluate feasibility and develop an appropriate process plan.
Conclusion
Progressive molds for automotive parts provide an effective manufacturing solution for companies that require high output, reliable quality, and efficient use of production resources. By integrating drawing, forming, piercing, trimming, and other operations into one continuous process, the mold reduces handling and supports stable, repeatable production.
For automotive motor housings, the advantages include uniform wall thickness, accurate fitting surfaces, controlled forming, high production efficiency, and compatibility with automated stamping lines. High-hardness alloy steel components improve wear resistance, while modular construction helps simplify maintenance and reduce production interruptions.
The manufacturing strength behind the mold is equally important. Integrated design, CNC machining, wire cutting, grinding, assembly, debugging, and press testing help ensure that the final tool is practical for real production conditions. The supplier’s technical staff, equipment resources, stamping capacity, and automation capabilities support a complete project approach.
For automotive and electric vehicle manufacturers, a well-engineered progressive mold can help improve production efficiency while maintaining strict component quality. When supported by proper material selection, accurate die design, careful tryout, preventive maintenance, and coordinated automation, it becomes a long-term production asset rather than simply a forming tool.
References
1. General principles of sheet metal stamping, progressive die design, and automotive component manufacturing.
2. Standard engineering practices for deep drawing, material flow control, die clearance, and forming sequence development.
3. Industrial guidance on preventive maintenance, inspection, and service-life management for stamping dies.
4. Technical information supplied for the progressive mold for automotive motor housings and small automotive parts.
5. Technical information supplied regarding the manufacturing equipment, stamping capacity, engineering personnel, and automation capabilities of the tooling supplier.
Product: Progressive molds for automotive parts
Previous Post
High-Precision Multi-Station Progressive Stamping Dies for Automotive, Electronics, and New Energy Manufacturing
Next Post
Precision Copper Busbar Stamping Parts for New Energy Vehicles
Our Products.
Start Your Business with an OEM Manufacturer Right Here!

Provide global customers with complete turn-key solutions
through
innovation!
QUICK LINKS
CONTACT INFO.
-
 +86-139 1308 8972
-

-
 No. 118 Yexin Road, Wujiang Economic Development Zone, Suzhou, China
Copyright © Suzhou Shuangqisi Mold Equipment Co., Ltd. All Rights Reserved. Custom Stamping Die Metal Stamping Die Manufacturers
