 English
 Español
 Deutsch
-

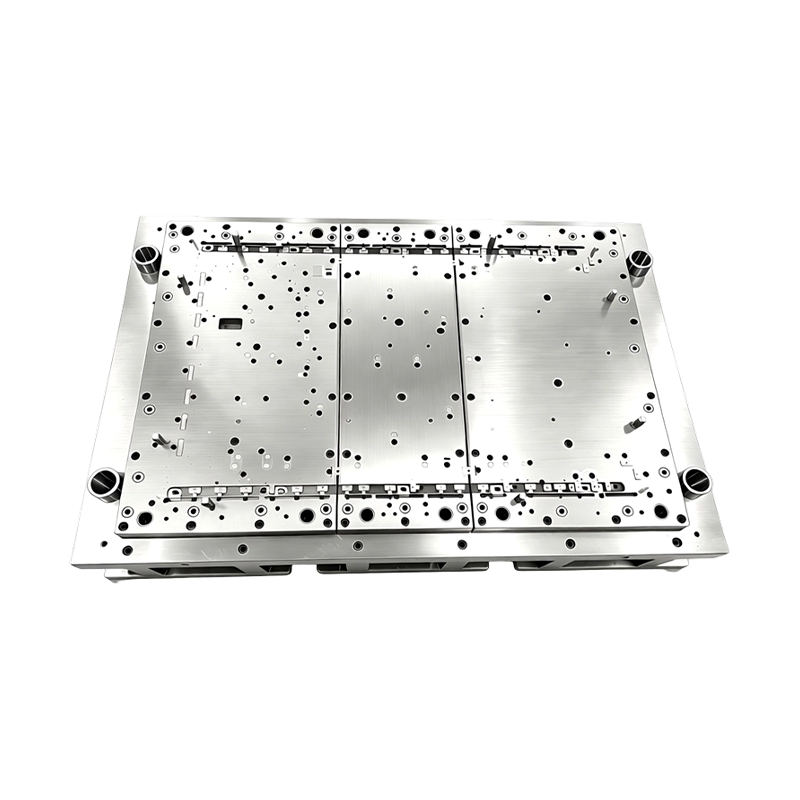
Progressive Stamping Die for Connector & Terminal Parts High Speed Progressive Stamping Die Precision Metal Hardware Stamping Tool mold for Connector Terminal Parts Automotive Components
Progressive Stamping Die for Connector & Termi...
-
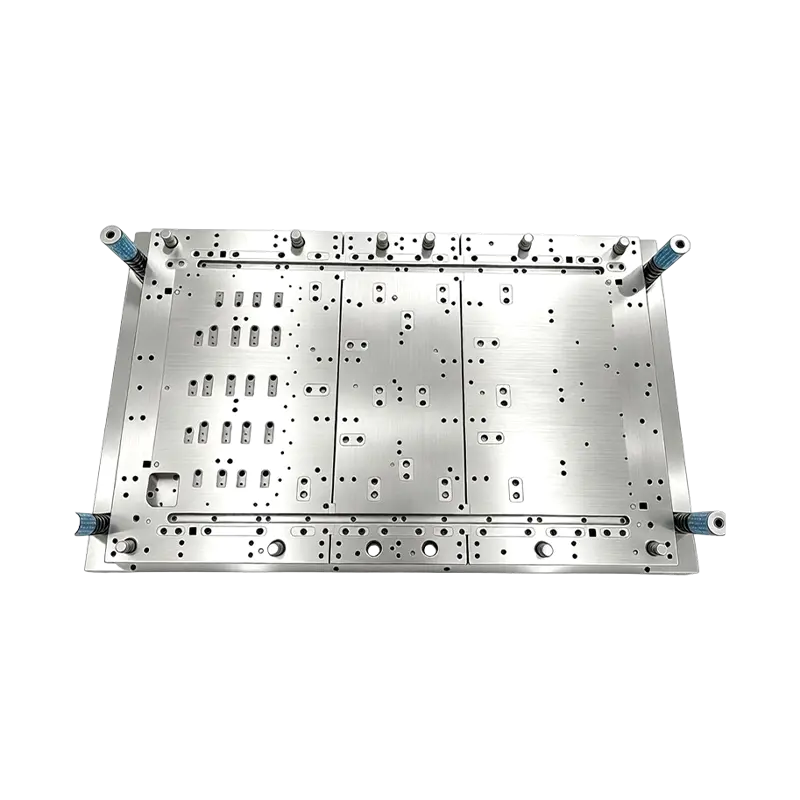
High Precision Stamping Die Multi Station Hardware Progressive Mold Tooling
Precision Metal Stamping Tool for Automotive &...
-

Long-Stroke Multi-Stage Progressive Die Automatic Strip Feed Progressive Die Long Travel Follow on Stamping Tool for Sheet Metal Hardware Press Moulding
Long-Stroke Multi-Stage Progressive DieOur custom ...
-
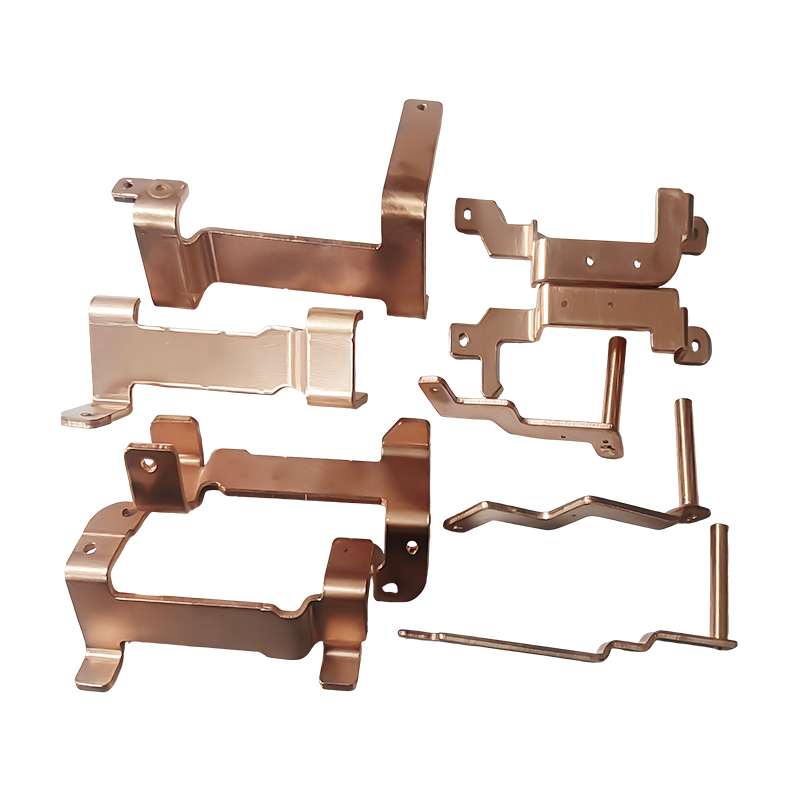
Multi-Station Progressive Stamping Die with Carbide Inserts Custom Multi Station Progressive Stamping Die Carbide Insert Metal Stamping Mold Tool for Equipment Appliances Device Hardware
High Speed Metal Stamping Tool for Precise Equipme...
-
New energy vehicle copper busbar stamping parts
New energy vehicle copper busbar stamping parts ar...
- E-mail us: [email protected]
- Call us: +86-139 1308 8972

Chen Siyi – Overseas Sales Manager
Home / Author / Chen Siyi – Overseas Sales Manager / Precision Copper Busbar Stamping Parts for New Energy Vehicles
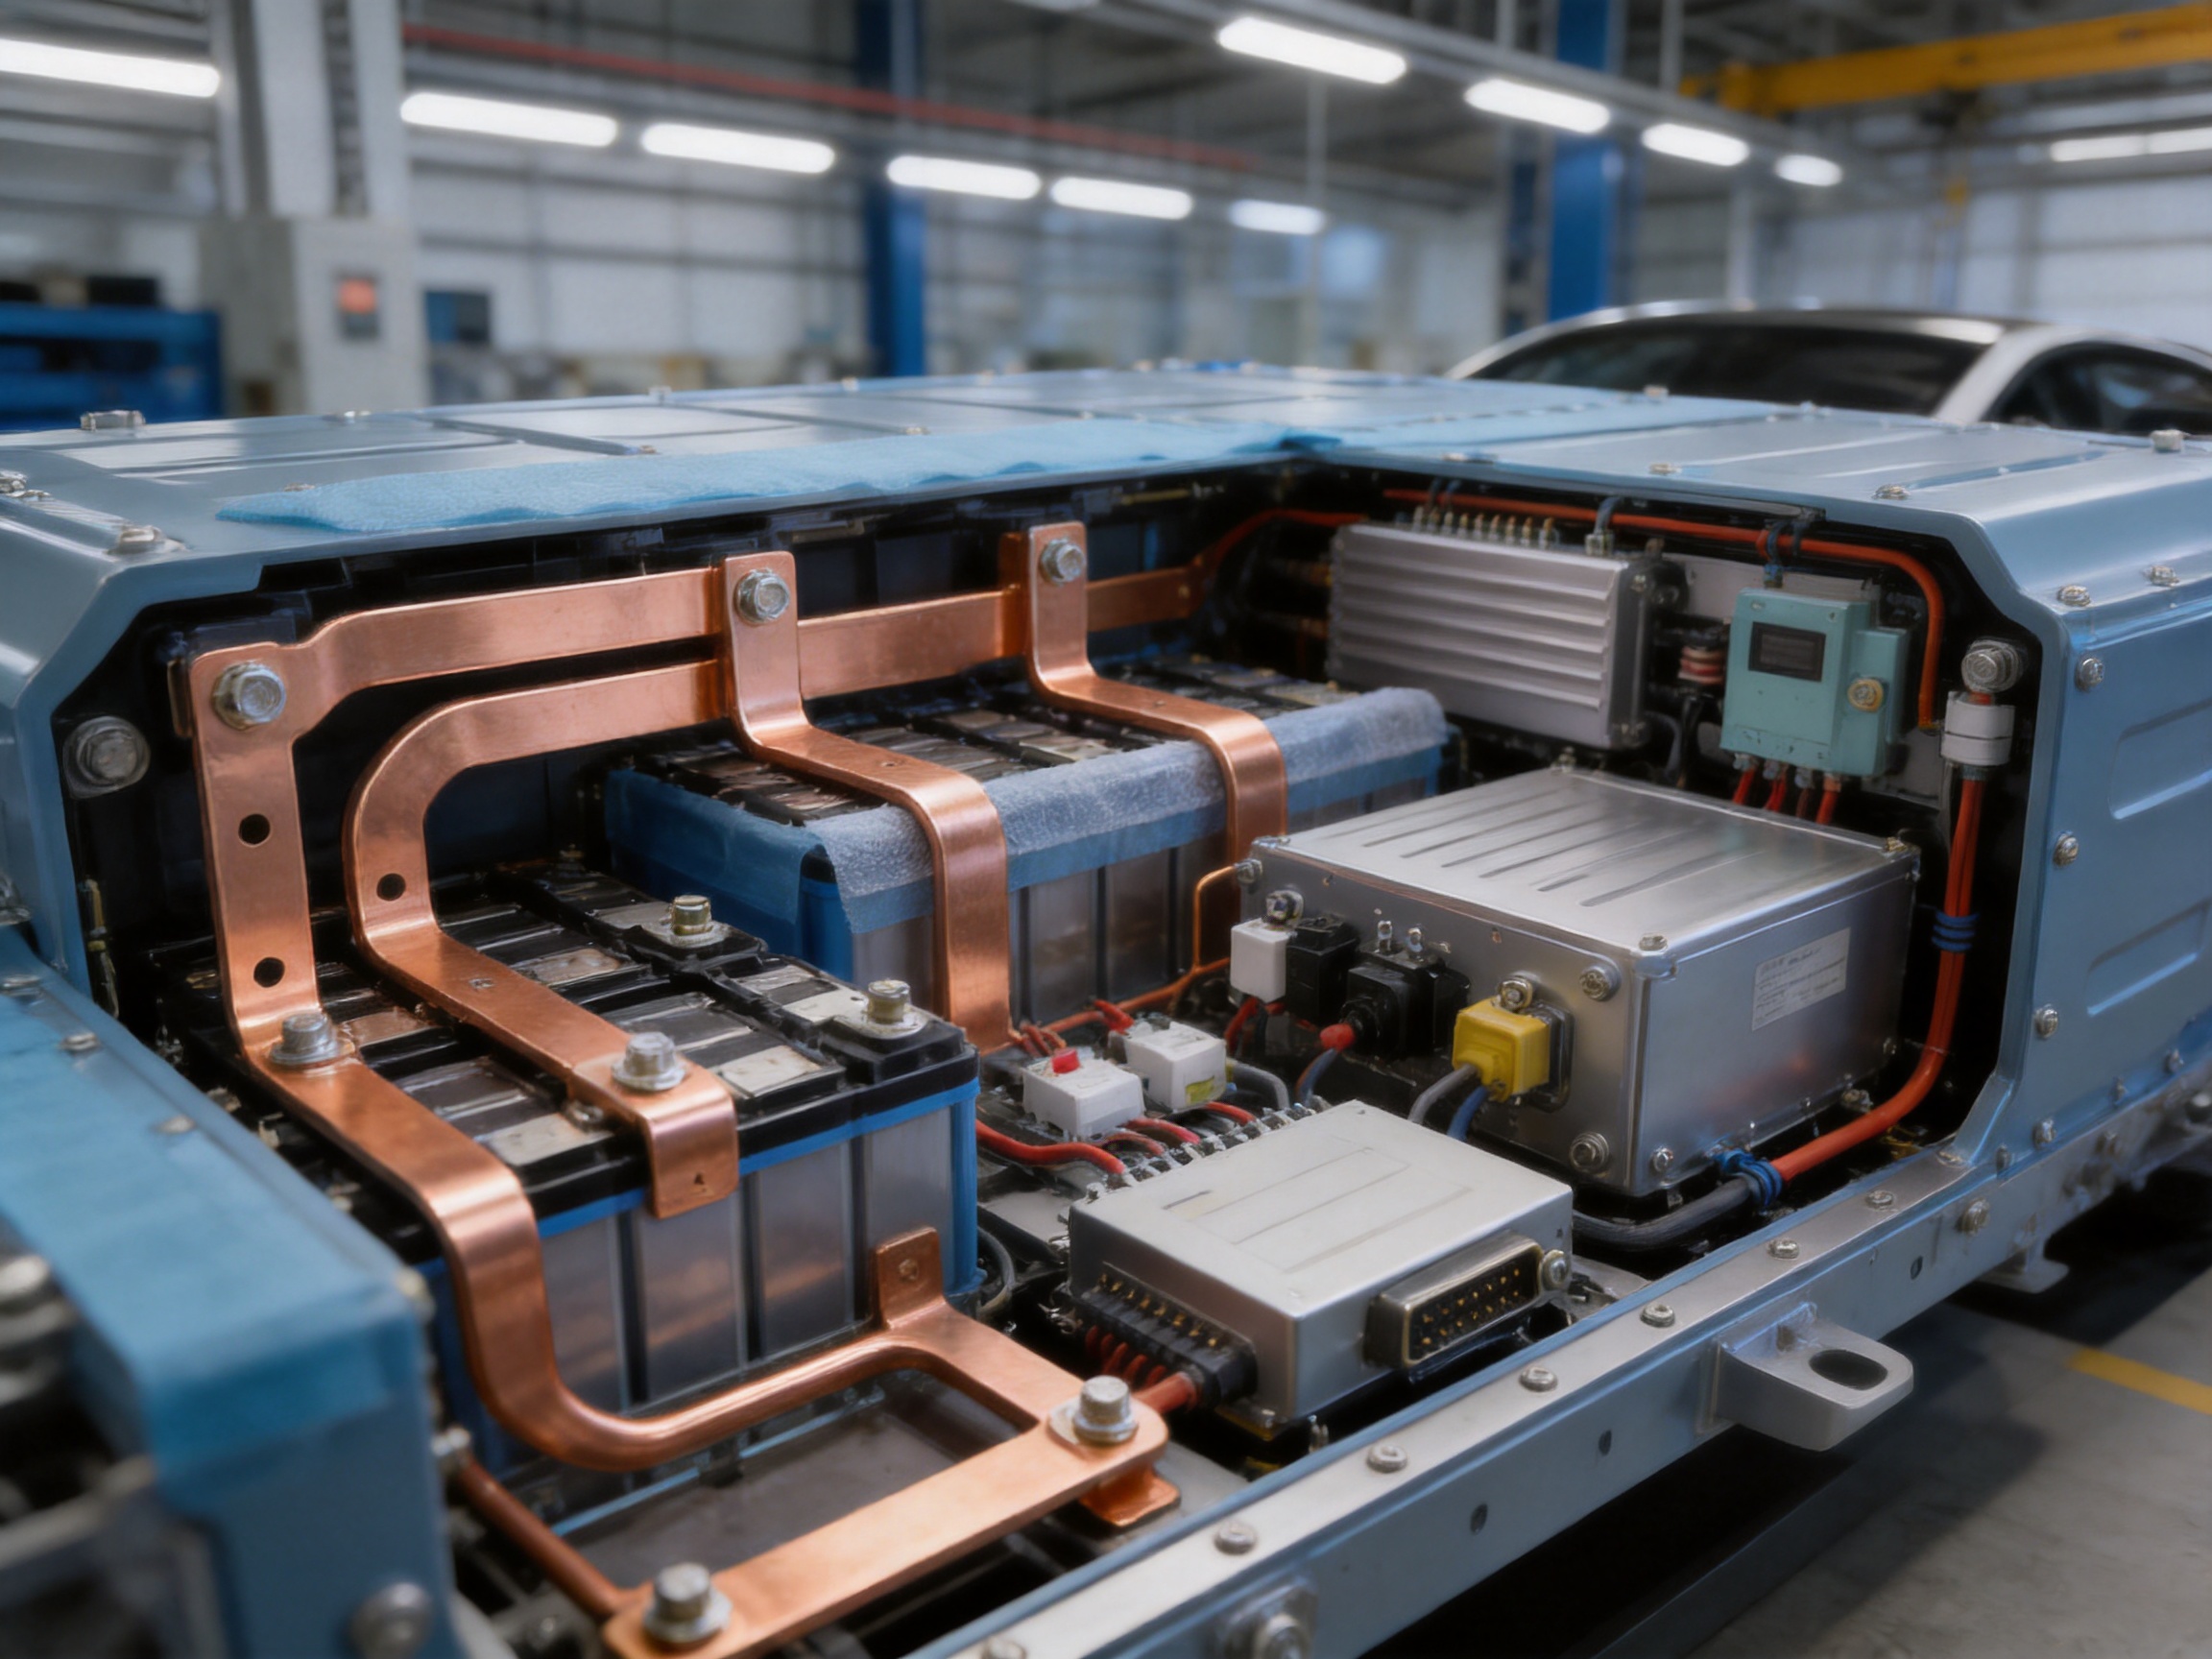
Precision Copper Busbar Stamping Parts for New Energy Vehicles
2026-10-18
The rapid growth of electric vehicles has created a strong demand for compact, reliable, and highly conductive power-distribution components. Among these components, copper busbars play a critical role in transferring electrical energy between battery packs, battery management systems, drive motors, DC/DC converters, inverters, charging systems, and other high-voltage assemblies. New energy vehicle copper busbar stamping parts provide a practical alternative to complex wiring harnesses while supporting higher current loads, improved packaging efficiency, and more consistent electrical performance.
Unlike conventional cable assemblies, a stamped copper busbar is a formed conductive component designed around the exact geometry of the vehicle’s electrical system. It can include bends, holes, slots, steps, terminals, connection platforms, and protective surface treatments in a single engineered part. This approach reduces unnecessary wiring, simplifies assembly, improves current-path consistency, and helps vehicle manufacturers make better use of limited battery-compartment and power-electronics space.
Precision manufacturing is essential because an EV busbar must satisfy several demanding requirements at the same time. It must carry current with minimal resistance, maintain stable contact performance, withstand vibration, tolerate wide temperature variations, resist corrosion, and remain dimensionally accurate during high-volume production. The manufacturing process must also protect the copper from deformation, surface damage, burr formation, and plating defects.
Suzhou Shuangqisi Mold Equipment Co., Ltd. develops and manufactures stamping dies, stamped metal parts, and stamping automation equipment for automotive and industrial applications. Its capabilities combine die design, precision machining, stamping production, process debugging, and automation integration. This integrated structure is particularly valuable for copper busbar projects, where product quality depends not only on the raw material but also on progressive die design, forming control, tooling durability, inspection methods, and production consistency.
New energy vehicle copper busbar stamping parts
Content
- 1 Why Copper Busbars Matter in Electric Vehicles
- 2 Material Selection for Stamped Copper Busbars
- 3 Precision Stamping Processes
- 4 Surface Treatments for Long-Term Reliability
- 5 Performance Advantages Compared with Conventional Wiring Solutions
- 6 Dimensional Accuracy and Quality Requirements
- 7 Tooling Design and Die Manufacturing Strengths
- 8 Press Capacity and Production Flexibility
- 9 Automation Integration for Busbar Production
- 10 Quality Management and Automotive Application Support
- 11 Cost and Production Efficiency
- 12 Applications in New Energy Vehicle Systems
- 13 Recommended Project Development Process
- 14 How the Product Creates Competitive Value
- 15 Frequently Asked Questions
- 15.1 What are new energy vehicle copper busbar stamping parts?
- 15.2 Why are copper busbars used instead of only wiring harnesses?
- 15.3 Which copper materials can be used?
- 15.4 What current range can these busbars support?
- 15.5 What dimensional accuracy is available?
- 15.6 Which surface treatments are available?
- 15.7 Can the busbars withstand automotive temperature and vibration conditions?
- 15.8 What stamping equipment is available for these products?
- 15.9 Can tooling and automation be supplied together?
- 15.10 How does the company control quality?
- 15.11 Can the product be customized?
- 15.12 What information should a customer provide for a quotation?
- 16 Conclusion
- 17 References
- 18 Product: New energy vehicle copper busbar stamping parts
Why Copper Busbars Matter in Electric Vehicles
An electric vehicle uses several high-current electrical pathways. Energy must move from the battery pack to the inverter and drive motor, while auxiliary systems receive power through DC/DC converters and related distribution modules. The battery management system monitors cell voltage, temperature, and state of charge, and it must remain connected to the battery through reliable electrical and mechanical interfaces.
Traditional wiring harnesses use flexible cables and multiple connectors to create these pathways. Although cables remain valuable for many applications, they can require substantial routing space and may involve numerous terminals, clips, protective sleeves, and assembly operations. Copper busbars provide a rigid and compact alternative where the electrical layout is relatively fixed.
A busbar is essentially a conductive metal path with a designed shape. Its cross-sectional area, length, bend geometry, mounting holes, and terminal locations are calculated according to the current, voltage, thermal, insulation, and packaging requirements of the application. Stamping technology allows these geometries to be produced efficiently and repeatedly, especially when the part is manufactured in medium or large quantities.
In high-voltage battery systems, busbars can connect battery modules, contactors, fuses, relays, current sensors, and external terminals. In power-electronics assemblies, they may connect inverters, capacitors, motor controllers, and charging units. Because each application has different space limitations and electrical requirements, custom stamping design is usually more suitable than a standard off-the-shelf component.
Reducing Electrical Resistance
High-purity copper is widely used for busbars because it combines excellent electrical conductivity with good formability. Materials such as C11000, C10100, and T2 copper can provide copper contents of 99.9% or higher, depending on the selected grade and specification. High conductivity helps reduce voltage drop and resistive heat generation along the current path.
The conductivity of copper can reach approximately 59.6 megasiemens per meter under appropriate material conditions. Its thermal conductivity can reach approximately 385 watts per meter-kelvin. These properties allow a well-designed busbar to carry substantial current while transferring heat away from connection areas and crowded electrical assemblies.
Lower resistance has several benefits. It can improve energy efficiency, reduce power losses, support more stable voltage delivery, and reduce the thermal burden on surrounding insulation and electronic components. In an EV, even small reductions in loss can become meaningful over repeated charging and driving cycles.
Improving Packaging Efficiency
Stamped busbars are designed to follow the architecture of the battery pack or power module. A three-dimensional formed part can pass around structural features, align with terminals, and connect separate electrical points without the routing space required by multiple cables.
This compact structure can help reduce the size and weight of an electrical assembly. It can also simplify protective covers and reduce the number of cable restraints. In applications where battery energy density and underbody space are important design objectives, the ability to integrate the conductor into a precisely formed shape is a major advantage.
Supporting High Current Loads
New energy vehicle copper busbar stamping parts can be engineered for current-carrying requirements ranging from approximately 30 amperes to 2,000 amperes, depending on the material thickness, width, cross-sectional design, cooling conditions, and application. This broad range allows stamped copper components to serve both low-current control connections and high-current battery or drive-system pathways.
Current capacity must never be determined by material selection alone. Engineers also evaluate continuous current, peak current, duty cycle, ambient temperature, contact resistance, ventilation, insulation, and the distance between conductive parts. A reliable supplier should review these factors before finalizing the busbar profile and die design.
Material Selection for Stamped Copper Busbars
Material selection directly affects conductivity, formability, spring behavior, mechanical strength, corrosion resistance, and plating compatibility. For this reason, copper grade should be selected according to the complete application rather than a single performance indicator.
C11000 Copper
C11000 is a commonly selected electrolytic tough-pitch copper grade. It offers high electrical and thermal conductivity and is suitable for many busbar, terminal, connector, and power-distribution applications. Its combination of conductivity and formability makes it compatible with a wide range of stamping operations.
When the design includes several bends, narrow sections, pierced holes, or formed terminals, the condition of the C11000 sheet or strip must be matched with the die and forming sequence. Excessive work hardening or an unsuitable temper may increase the risk of cracking around sharp bends or pierced features.
C10100 Copper
C10100 is an oxygen-free copper grade known for very high conductivity and excellent performance in demanding electrical applications. It may be considered when electrical purity and conductivity are especially important. Its use depends on the required mechanical properties, forming complexity, cost target, and availability of suitable material thicknesses.
T2 Copper
T2 copper is also widely used in electrical and industrial components. It provides a practical balance of conductivity, manufacturability, and material availability. For automotive busbar production, the selected T2 specification should be verified against the required chemical composition, temper, thickness tolerance, and customer quality standard.
Thickness and Temper Control
Busbar thickness is usually determined by current capacity, heat dissipation, available space, stiffness, and connection design. Thicker copper may improve current capacity and mechanical rigidity, but it also increases forming force and may require specialized die construction. Thinner material can reduce weight and simplify forming, but it may require additional reinforcement or a larger conductor width.
Temper affects forming behavior. Softer copper is easier to bend and form, while harder copper may provide greater mechanical stability after processing. The best selection depends on the geometry and the required balance between conductivity and structural performance.
Incoming material control should include verification of material grade, thickness, width, surface condition, hardness or temper, and supplier documentation. Consistent material quality helps stabilize die clearance, forming force, springback, plating adhesion, and final dimensional results.
Precision Stamping Processes
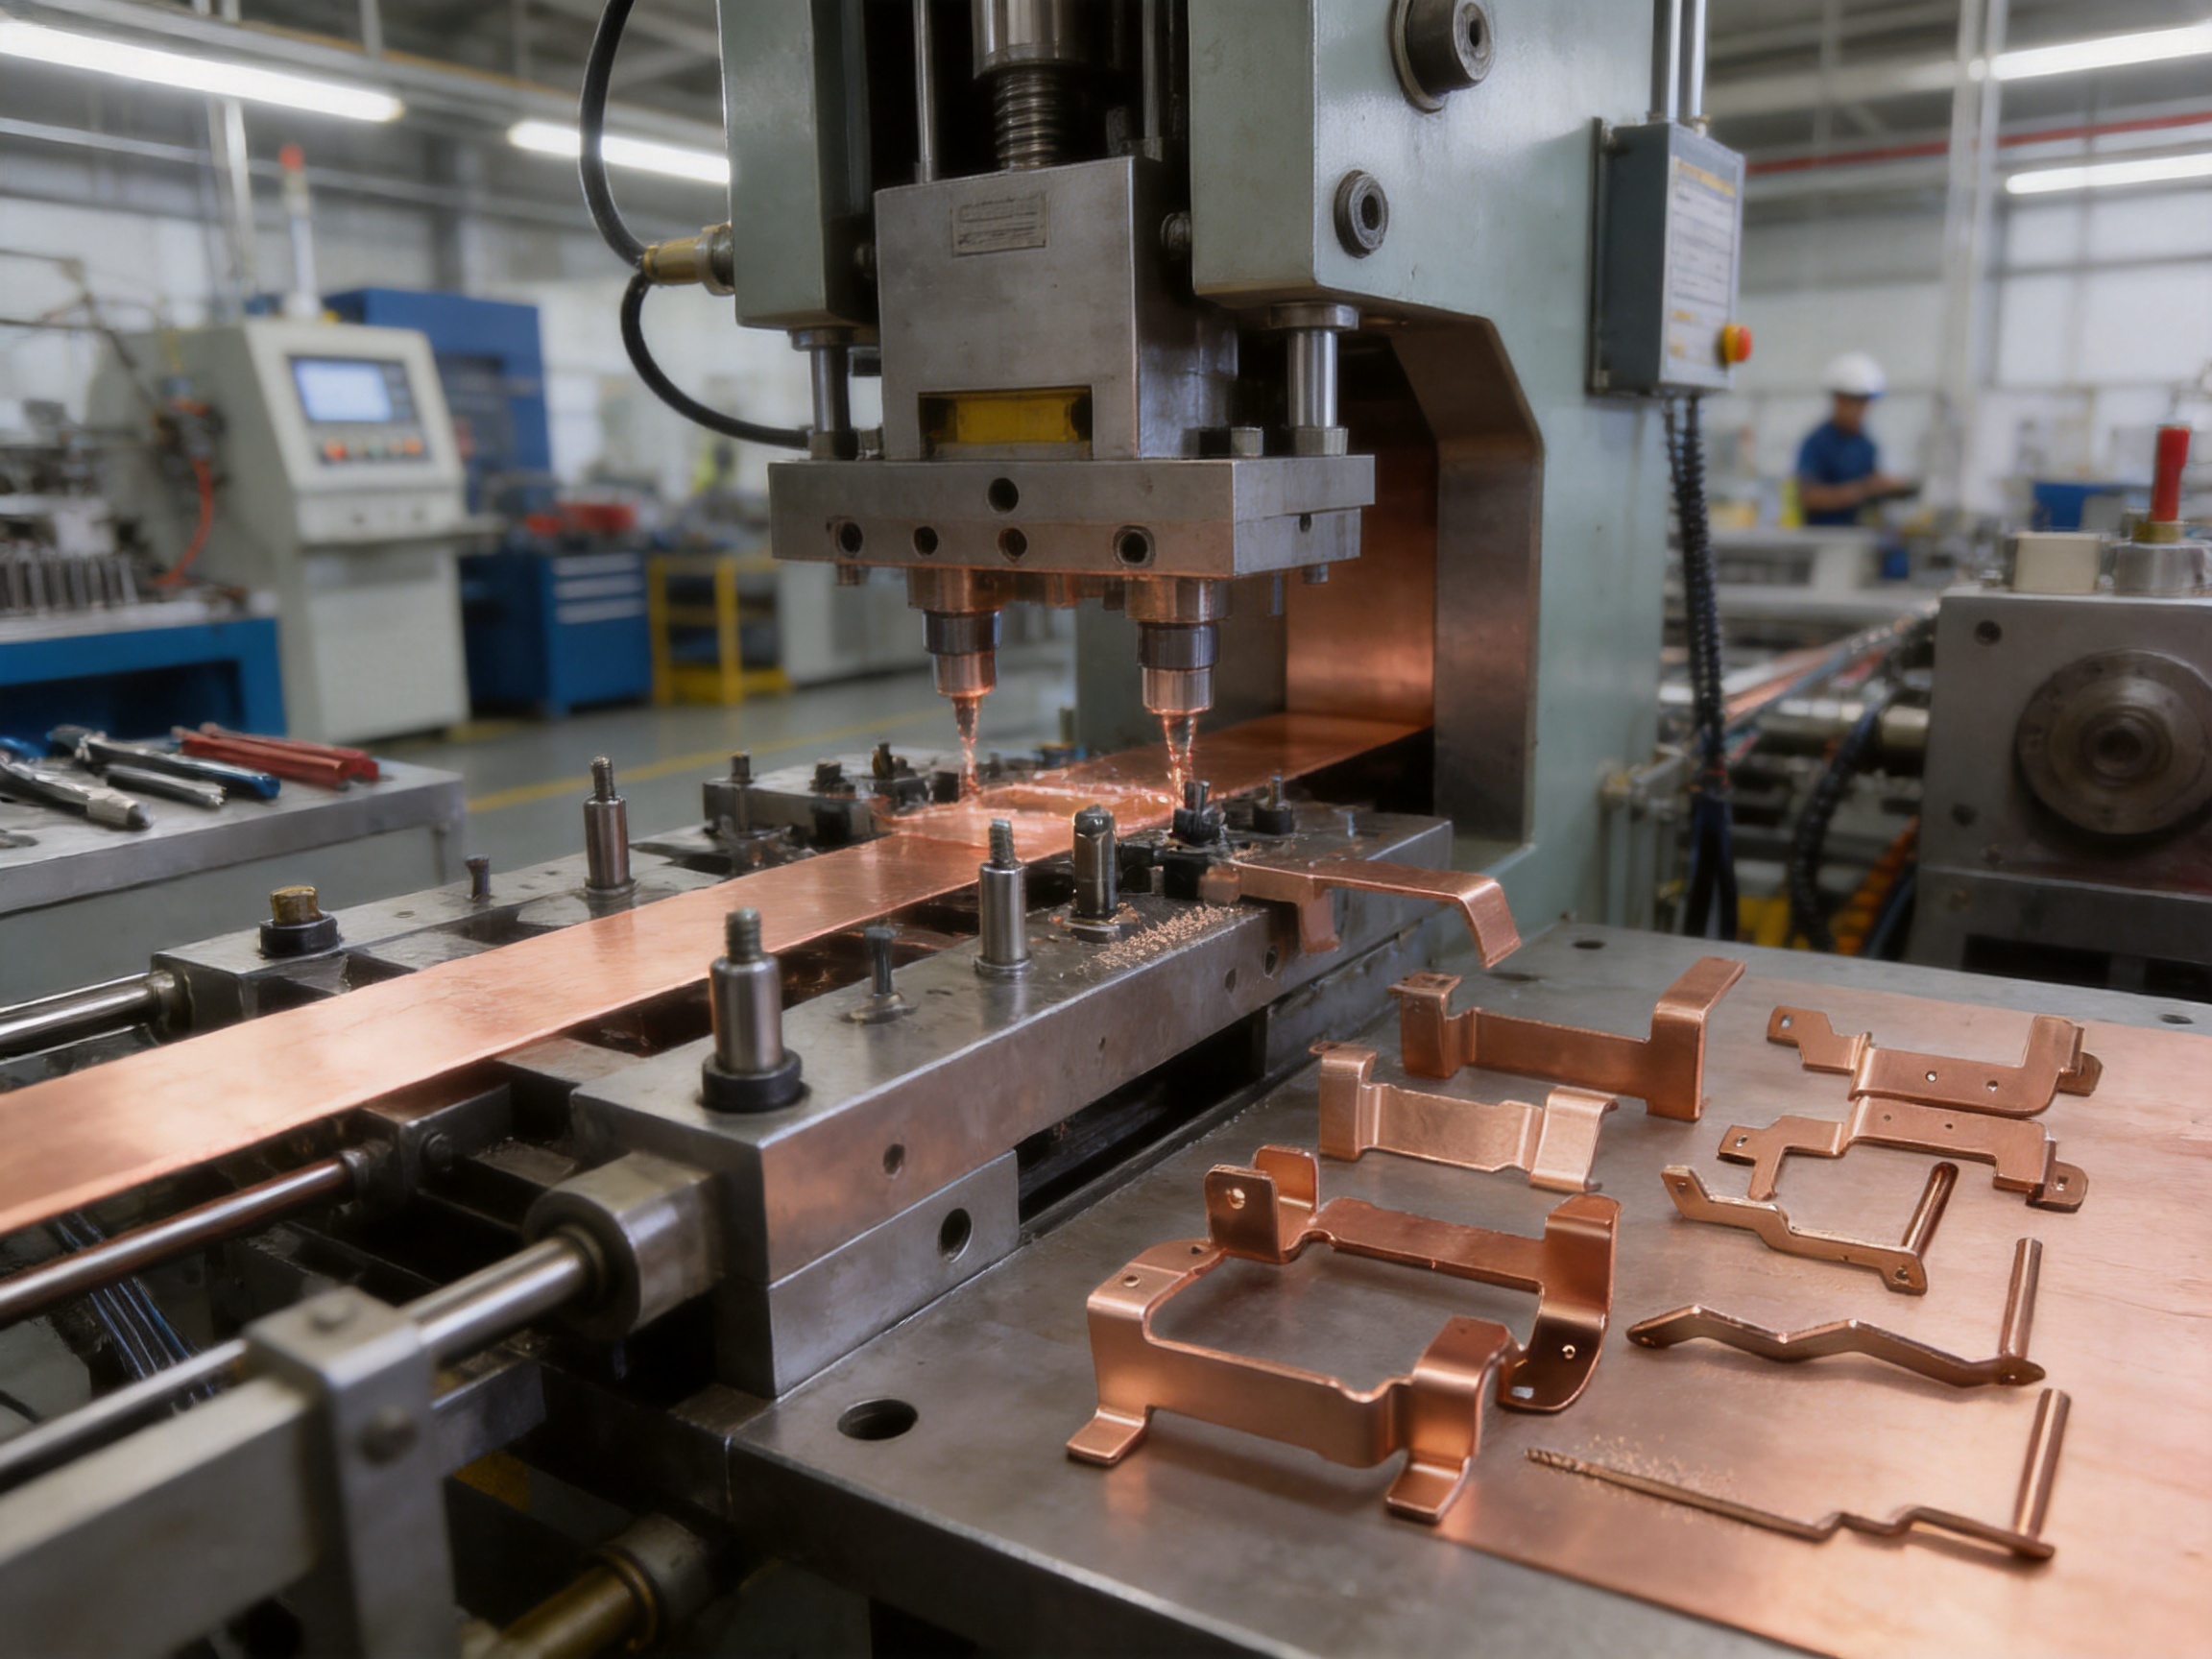
Producing a high-quality copper busbar requires more than simply cutting a copper sheet into shape. The complete process may include blanking, piercing, bending, embossing, forming, coining, trimming, deburring, cleaning, plating, inspection, and packaging. Each operation must be arranged to minimize deformation and preserve the electrical and mechanical functions of the finished component.
Product and Process Engineering
The process begins with a review of the product drawing and application requirements. Engineers evaluate the conductor width, thickness, bend radius, hole positions, terminal shape, contact surfaces, mounting features, insulation clearances, and plating zones.
During this stage, the part design is checked for manufacturability. Narrow bridges, excessively sharp corners, small holes, uneven forming loads, and difficult material flow can create production risks. Design-for-manufacturing recommendations may include adding suitable radii, adjusting hole-to-edge distances, changing the sequence of bends, or separating a difficult feature into controlled operations.
For automotive projects, process planning should also consider traceability, inspection access, tool maintenance, production volume, and future design changes. Early engineering coordination reduces the likelihood of expensive die modifications after the tooling has been completed.
Strip Layout and Material Utilization
When a busbar is produced from coil or strip material, the strip layout determines how the part is positioned through the die. Engineers optimize the pitch, carrier design, nesting pattern, and scrap bridges to balance material utilization with production stability.
A highly compact layout may reduce scrap but can make the strip more difficult to guide or may leave insufficient support around critical features. A slightly wider carrier may provide better stability and improve dimensional consistency. The correct layout is therefore a technical compromise between material savings, tooling strength, feeding reliability, and part quality.
Blanking and Piercing
Blanking creates the external contour of the busbar, while piercing produces holes, slots, windows, and other internal features. Copper is relatively ductile, so inappropriate punch and die clearance can result in burrs, rollover, distortion, or premature tool wear.
Clearance is selected according to material grade, thickness, hardness, and feature requirements. Critical connection holes may require particularly good roundness and positional accuracy. The punch edge condition, die support, strip guidance, and press alignment all influence the final result.
For high-current connection areas, burr direction and burr height are important. Excessive burrs can interfere with assembly, reduce creepage or clearance distance, damage insulation, or create stress concentration points. Controlled tooling and subsequent deburring or edge treatment may be required.
Bending and Forming
Three-dimensional busbars often require multiple bends and formed sections. The forming sequence is designed to prevent interference between previously formed areas and the die components. It also controls springback, which can affect terminal height, hole alignment, and contact pressure.
Springback depends on material temper, thickness, bend radius, forming direction, and local geometry. Tool compensation, staged forming, coining, or restrike operations may be used to achieve the required final shape. A carefully designed sequence avoids excessive stress and reduces the risk of cracks at the bend transition.
Forming surfaces must be smooth and accurately finished. Any sharp tool damage can mark the copper surface or create a defect that becomes more visible after plating. Lubrication and cleaning conditions should also be controlled so that they do not interfere with later surface treatment.
Coining and Contact Preparation
Some busbar designs require a flattened, raised, or coined contact zone. Coining can improve flatness, define a precise terminal surface, reduce local thickness variation, or create a reliable interface for a bolt, connector, sensor, or fuse.
Contact areas must be free of excessive scratches, contamination, oxidation, and burrs. Since contact resistance is affected by surface condition and clamping force, the contact preparation process should be validated through dimensional and electrical testing.
Deburring and Cleaning
Deburring removes or reduces sharp edges created during cutting and piercing. The method may involve mechanical brushing, tumbling, precision edge treatment, or a controlled secondary operation. The selected method must preserve the geometry of holes and terminals without rounding critical features excessively.
After forming, cleaning removes oil, particles, oxides, and other contaminants. Cleanliness is especially important before plating, insulation coating, welding, or assembly. Inadequate cleaning can reduce plating adhesion and increase contact resistance.
Surface Treatments for Long-Term Reliability
Copper naturally develops an oxide layer when exposed to air and moisture. Although the oxide layer may be thin, it can influence contact resistance, solderability, weldability, and long-term appearance. Surface treatment is therefore often applied to the areas that connect with terminals or other conductive components.
Tin Plating
Tin plating is commonly selected for copper busbars because it provides good electrical contact performance, corrosion protection, and compatibility with many automotive terminals. It can also support soldering and simplify assembly in certain designs.
A typical specified thickness may be approximately 3 to 5 micrometers, although the correct value depends on the application and customer requirements. Plating thickness should be controlled across important contact areas, corners, formed regions, and edges.
Nickel Plating
Nickel plating offers good corrosion resistance, wear resistance, and thermal stability. It may be appropriate where the busbar is exposed to elevated temperatures, mechanical contact, or a more demanding environmental condition. Nickel can also serve as a functional barrier layer in a multi-layer plating system.
Silver Plating
Silver has excellent electrical conductivity and can provide a low-resistance contact surface. It may be considered for high-performance applications where contact resistance, current density, and thermal behavior are particularly important. The cost and environmental requirements of silver plating should be evaluated against the expected performance benefit.
Plating Quality Control
Surface treatment quality depends on pretreatment, cleaning, activation, bath control, current density, rinsing, drying, and handling. Plating must be firmly bonded to the copper substrate and should not peel, blister, crack, or become uneven during forming and service.
Quality verification may include thickness measurement, visual inspection, adhesion testing, surface-resistance testing, corrosion testing, and sample-based environmental exposure. The inspection plan should distinguish between functional contact zones and areas where appearance or coating thickness has different priorities.
Performance Advantages Compared with Conventional Wiring Solutions
Copper busbar stamping parts offer several advantages over traditional wiring harnesses and manually fabricated conductive plates. These advantages are not universal for every vehicle circuit, but they are particularly valuable in fixed-layout, high-current, space-constrained applications.
| Performance Factor | Stamped Copper Busbar | Traditional Cable Harness | Practical Benefit |
|---|---|---|---|
| Current path | Short, rigid, and purpose-designed | Flexible cable with terminal interfaces | Can reduce unnecessary routing and connection points |
| Electrical resistance | Low resistance through a broad copper section | Depends on cable length, conductor size, and terminals | Supports efficient power transmission |
| Packaging | Can follow battery and module geometry | Requires bending radius and routing space | Improves space utilization |
| Assembly | May integrate holes, bends, and connection features | Often requires several cables, clips, and terminals | Can reduce assembly steps |
| Thermal behavior | High copper thermal conductivity and broad surface area | Heat depends on cable construction and installation | Supports heat dissipation in compact areas |
| Production repeatability | Controlled by dedicated stamping dies | Can depend more heavily on cutting, crimping, and routing | Improves consistency in high-volume production |
| Mechanical structure | Rigid and dimensionally defined | Flexible and more vulnerable to movement if poorly secured | Helps maintain stable connection geometry |
One of the most important advantages is reduced connection complexity. Every additional connector, crimp, joint, or cable transition may introduce electrical resistance, assembly variation, and a potential failure point. A stamped busbar can combine several functions into one accurately formed component, although it may still require terminal hardware, insulation, sensors, or protective covers.
Busbars can also improve automated assembly. Their holes and edges are controlled by the stamping die, allowing fixtures and robotic systems to locate them consistently. This repeatability supports torque-controlled fastening, automated inspection, and traceable production records.
Another advantage is design integration. A busbar can be manufactured with mounting tabs, grounding points, sensor interfaces, stepped sections, and multiple connection positions. Combining these functions reduces the need for separate brackets or manually positioned conductors.
Dimensional Accuracy and Quality Requirements
New energy vehicle copper busbar stamping parts may require dimensional accuracy in the approximate range of ±0.05 to ±0.2 millimeters, depending on the feature and the application. A hole used for a precision terminal may have a tighter tolerance than a non-critical external edge. The appropriate tolerance must be defined on the drawing according to assembly and electrical requirements.
Dimensional control begins with the die. Punch and die alignment, guide-post accuracy, insert quality, press rigidity, strip feeding, and forming compensation all affect the final part. It continues through production with first-article inspection, process checks, tool-condition monitoring, and final sampling.
Important Inspection Features
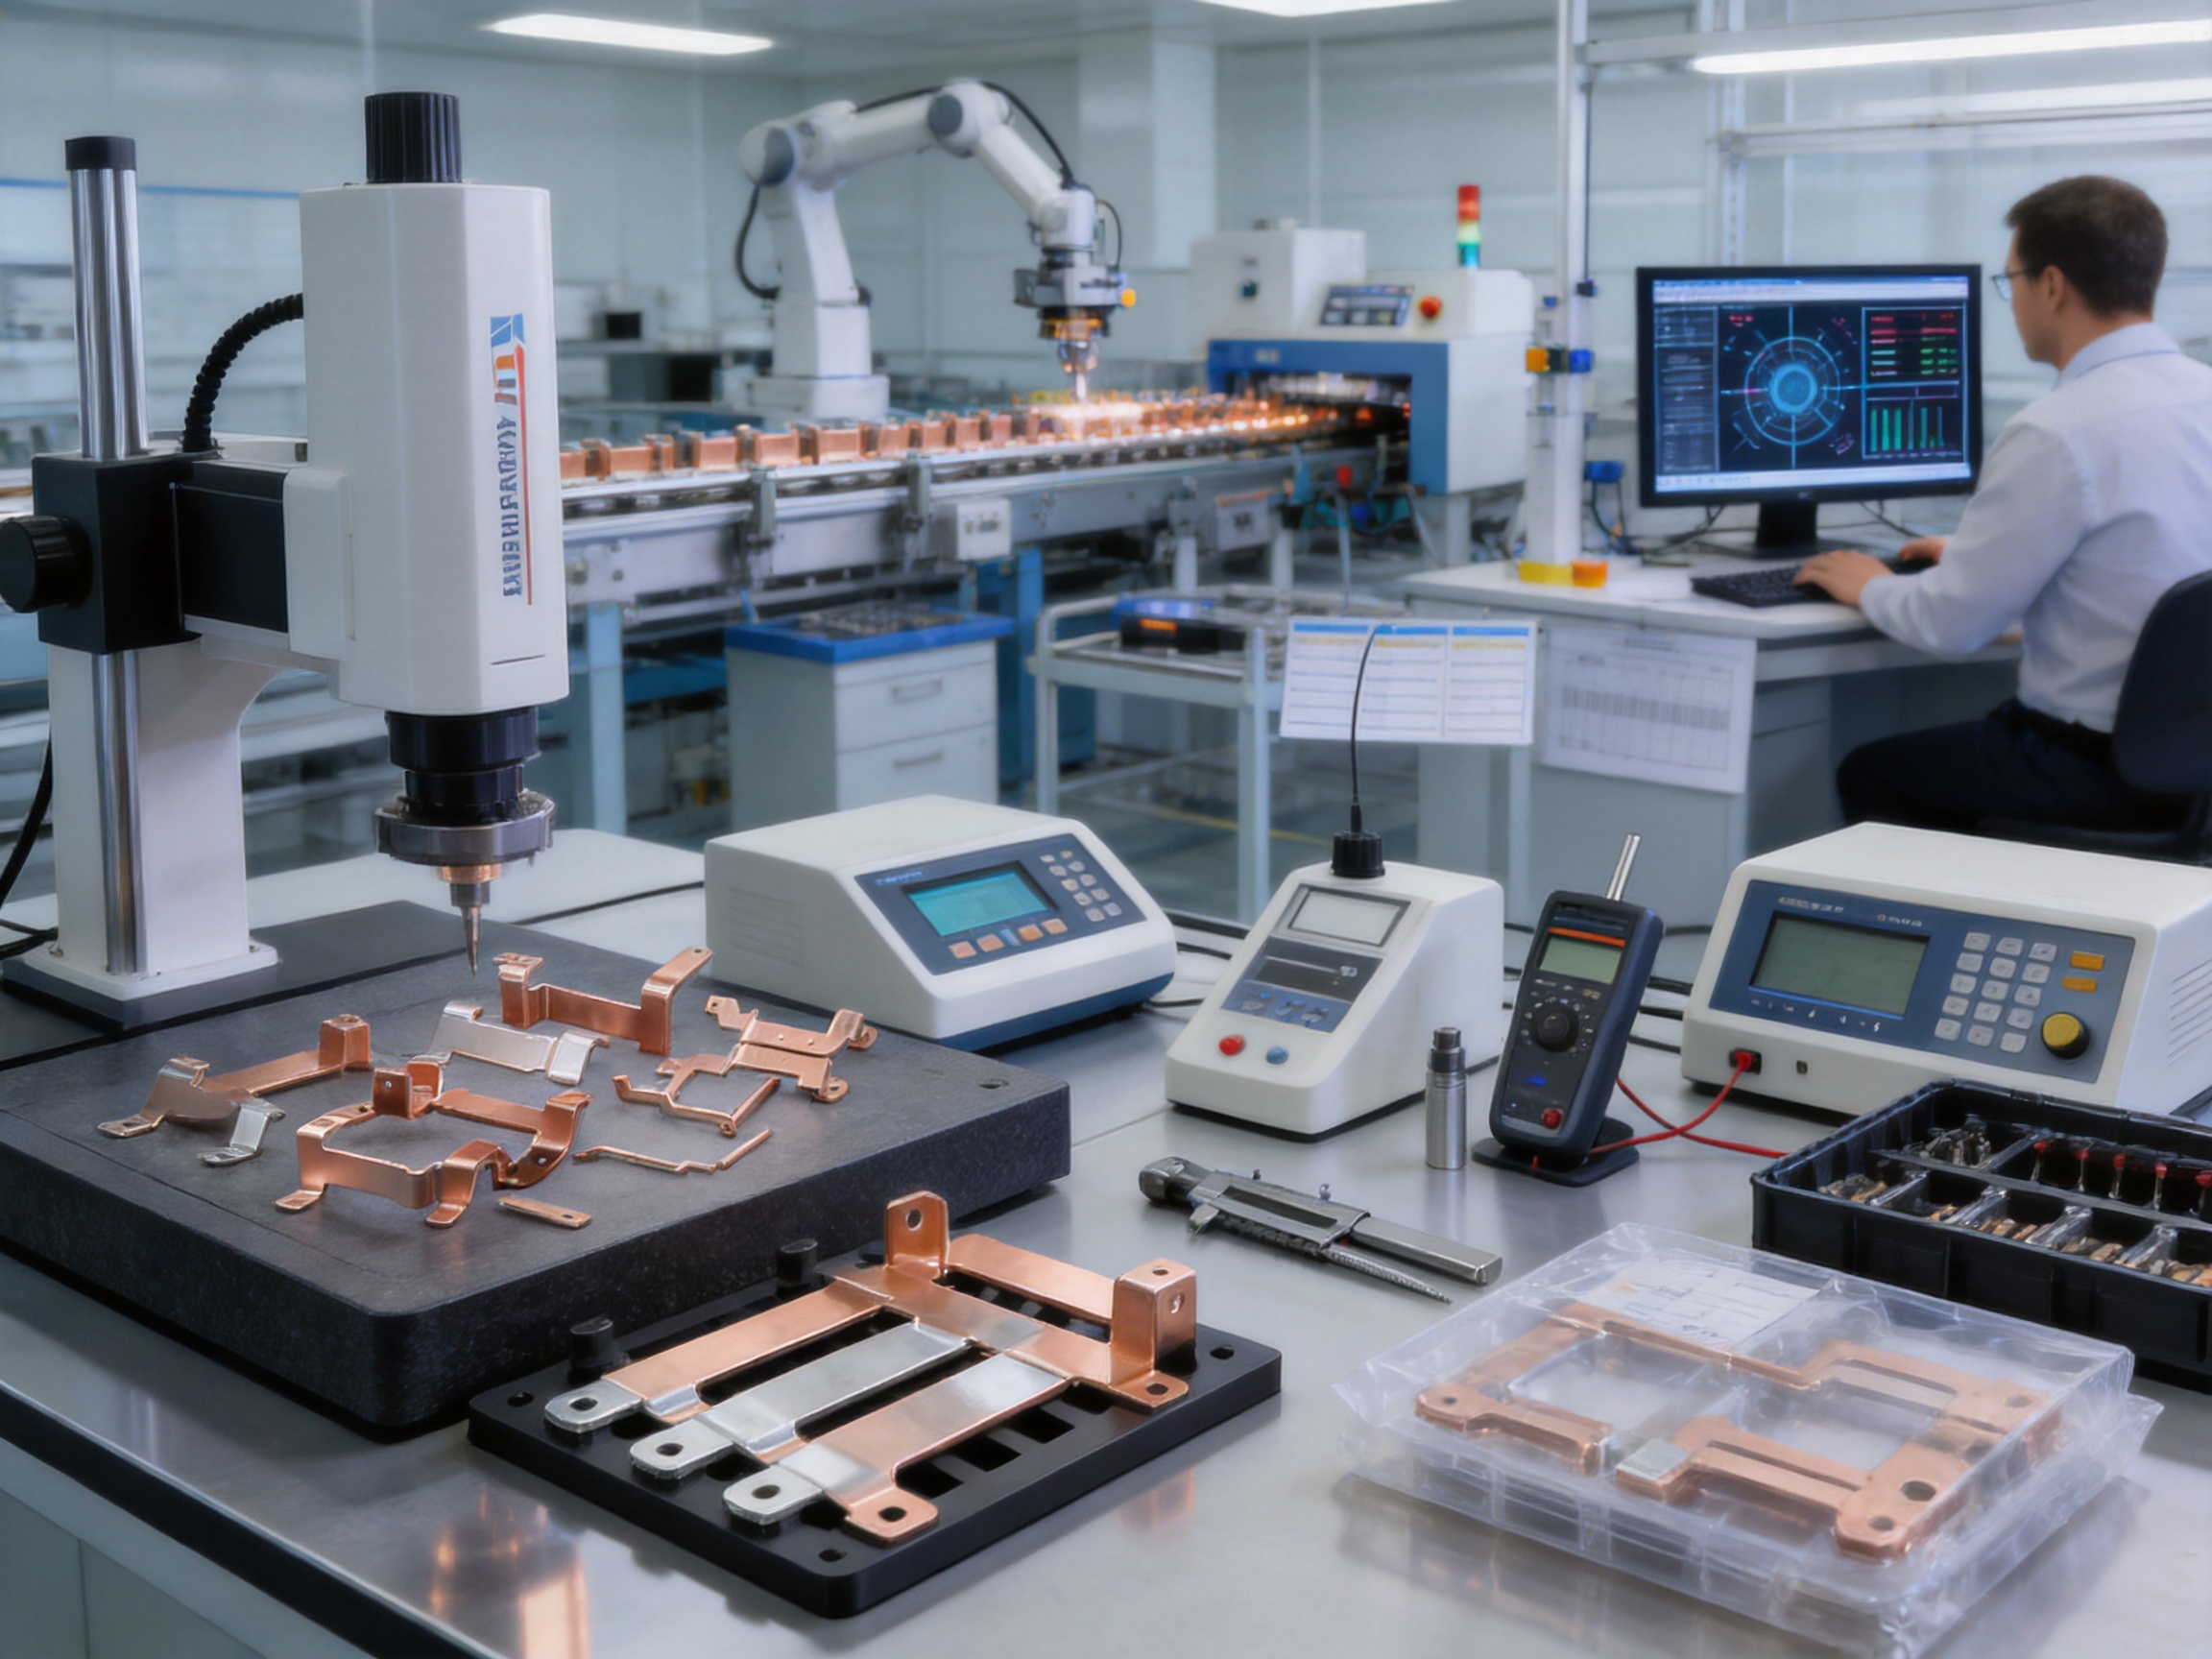
Typical inspection features include overall length and width, hole diameter, hole position, bend angle, terminal height, flatness, material thickness, burr height, plating thickness, surface condition, and contact resistance. Critical dimensions should be measured using suitable gauges, coordinate measuring equipment, optical systems, or dedicated inspection fixtures.
Flatness is especially important where the busbar is mounted against a battery module, electrical housing, cooling plate, or insulation component. Excessive warpage can create assembly stress, uneven clamping, or insufficient contact pressure.
Hole position is also critical. A slight positional error may prevent a bolt or connector from entering correctly, or it may force the busbar into an unintended position during assembly. For multi-point connections, the accumulated positional relationship between holes may be more important than the isolated tolerance of any single feature.
Electrical Inspection
Electrical tests may include resistance measurement, continuity testing, insulation-distance verification where applicable, and high-current temperature-rise testing. Contact resistance should be evaluated with the intended fastening method, surface treatment, hardware, and clamping force.
Temperature-rise testing helps confirm that the busbar remains within the permitted thermal range during continuous and peak current operation. Test conditions should reflect the actual application, including ambient temperature, enclosure conditions, neighboring components, and cooling provisions.
Mechanical and Environmental Testing
Automotive busbars may be exposed to vibration, shock, thermal cycling, humidity, salt spray, chemical agents, and repeated expansion and contraction. A robust validation program evaluates whether the part retains its dimensions, plating adhesion, electrical performance, and connection integrity after environmental exposure.
The stated operating range for the product can extend from approximately -40 degrees Celsius to 125 degrees Celsius, subject to the exact material, plating, insulation, and vehicle application. The final specification should be confirmed through application-specific validation rather than assumed from a general material rating.
Tooling Design and Die Manufacturing Strengths
The stamping die is the central manufacturing asset for a precision busbar. A well-designed die improves dimensional consistency, production speed, material utilization, tool life, and maintenance efficiency. An unsuitable die may produce burrs, uneven forming, unstable feeding, premature wear, and excessive scrap.
Suzhou Shuangqisi Mold Equipment Co., Ltd. specializes in stamping die design and manufacturing as well as stamped hardware production. Its technical organization includes approximately 60 technical staff, supported by experienced operators and debugging personnel. This combination allows product engineering and production engineering to be coordinated rather than treated as completely separate activities.
Precision Machining Resources
The company is equipped with imported wire-cut electrical discharge machines, CNC machining centers, more than ten grinding machines of different sizes, and other precision machine tools. These resources support the production of die bases, inserts, punches, forming components, guide structures, and replacement parts.
Wire cutting is useful for producing accurate profiles, narrow slots, and complex hard-material components. CNC machining centers support efficient production of die plates, cavities, mounting surfaces, and structural elements. Grinding machines help achieve the surface finish and dimensional precision required for sliding, forming, and cutting components.
Having these capabilities within an integrated manufacturing organization can shorten communication cycles and improve control over tool quality. It also makes it easier to implement design changes, repair worn components, and adjust the die during process debugging.
Die Structure for Copper Materials
Copper stamping dies must be designed with attention to material softness, friction, burr generation, and surface protection. Cutting edges require suitable hardness and wear resistance, while forming surfaces must be polished and carefully aligned to avoid marking the copper.
Die components may include precision punches, replaceable inserts, guiding elements, lifters, pilots, strippers, forming blocks, and restrike stations. The design is selected according to the part shape, material thickness, production volume, press capacity, and maintenance strategy.
For complex busbars, a progressive die can combine several operations in one continuous strip process. For lower-volume or very large parts, a transfer die, compound die, or multiple single-operation tools may be more suitable. The best choice is determined by annual demand, part complexity, automation requirements, and investment expectations.
Tool Debugging and Process Stabilization
Tool debugging is not limited to producing one acceptable sample. It involves adjusting feeding, pilot timing, forming depth, stripper pressure, die clearance, lubrication, part separation, and inspection conditions until the process is stable across repeated production cycles.
Experienced debugging personnel can identify whether a defect originates from the die, the material, the press, the feed system, or the forming sequence. This diagnosis helps prevent temporary adjustments that only mask the problem. A stable process should achieve consistent quality without excessive manual correction.
Press Capacity and Production Flexibility
The company operates 25 punch presses ranging from approximately 80 tons to 400 tons. This press range supports different busbar sizes, material thicknesses, die structures, and production requirements.
Press selection affects more than nominal force. Engineers also evaluate stroke length, shut height, bed dimensions, feed direction, speed, slide parallelism, die weight, and automation compatibility. The press must provide sufficient capacity for the maximum forming and cutting loads while maintaining accurate operation throughout the production cycle.
A broad press range allows production to be matched more closely with the product. Small or medium parts can be manufactured on an appropriately sized machine, while larger or more heavily formed busbars can be assigned to higher-capacity equipment. This improves utilization and avoids forcing every project into one standard production configuration.
Production flexibility is useful for both prototype development and mass production. Initial samples may require controlled trial runs, process adjustments, and engineering verification. Once the design is approved, the same process can be optimized for consistent output, automated feeding, and reduced cycle time.
Automation Integration for Busbar Production
Stamped copper busbars are well suited to automation because their geometry can be controlled by the die and their production cycle can be repeated at high speed. Automation may include decoiling, straightening, servo feeding, in-die sensing, transfer systems, part separation, vision inspection, stacking, and packaging.
Through its investment in Suzhou Keshuang Intelligent Technology Co., Ltd., the company also provides stamping automation equipment. This creates an opportunity to coordinate the die and automation system from the early design stage instead of adding automation after the die has already been completed.
Benefits of Integrated Automation
Integrated automation can improve production stability by controlling material feeding and reducing manual handling. It can also reduce the risk of scratches, contamination, mixed parts, and incorrect orientation. Automated systems support repeatable cycle timing and can record production data for traceability.
In high-volume automotive production, automation can help maintain output while controlling labor requirements. It may also improve workplace safety by keeping operators away from moving die areas and reducing repetitive handling operations.
Automation can be designed around the finished busbar’s geometry. For example, a system may orient formed parts, separate connected components, check hole presence, measure critical edges, or place parts into trays with controlled contact protection. The appropriate solution depends on production volume and inspection requirements.
In-Process Monitoring
Modern stamping automation can include sensors for material presence, strip position, double-sheet detection, press overload, die protection, and part ejection. These systems help stop the press before a major tooling or product problem occurs.
Vision systems can verify the presence of holes, tabs, plating differences, missing features, or incorrect part orientation. Force monitoring can identify unusual cutting or forming conditions. These controls do not replace engineering judgment, but they provide valuable early warning and support consistent production.
Quality Management and Automotive Application Support
Automotive customers require stable processes, documented inspection, traceability, and controlled change management. The company’s stated compliance framework includes IATF 16949, RoHS, and ISO-related requirements. The exact certification scope and customer-specific requirements should be confirmed during project evaluation.
IATF 16949-based practices emphasize risk analysis, process control, corrective action, supplier management, measurement-system evaluation, and continuous improvement. For busbar production, these principles can be applied through process flow diagrams, control plans, failure mode analysis, inspection standards, and production records.
Risk Prevention
Potential failure modes for a copper busbar may include incorrect material grade, insufficient conductivity, excessive burrs, poor plating adhesion, hole misalignment, wrong bend angle, surface damage, cracking, inadequate contact area, and mixed part numbers.
Preventive controls may include material certificates, barcode identification, first-piece approval, die-protection sensors, automated dimensional inspection, plating verification, electrical testing, and final packaging checks. Each control should be connected to a specific risk and acceptance criterion.
Traceability
Traceability can connect the finished busbar with its material batch, production date, press, die, operator or production team, plating batch, inspection results, and packaging lot. This information is valuable when investigating a quality concern or managing a design change.
Good traceability also supports controlled product development. When a material temper, plating thickness, or forming sequence is changed, the effect can be compared with previous production data. This reduces uncertainty during optimization.
Customer-Specific Development
Different vehicle platforms may use different current ratings, connection structures, coatings, insulation systems, and validation procedures. A capable supplier should be able to adapt its tooling, inspection, and automation approach to each project rather than relying on one fixed standard.
The company has supplied molds and products for applications associated with servo drives, compressors, and new energy vehicles. Experience across these industries can support understanding of high-current conductive components, precision stamping, thermal requirements, and production cost control.
Cost and Production Efficiency
Cost competitiveness in busbar manufacturing depends on the complete production system. Material utilization, die life, press efficiency, cycle time, rework rate, plating cost, packaging, logistics, and inspection requirements all influence the final price.
Because copper is a valuable raw material, strip layout optimization can produce meaningful savings. However, material utilization should not be improved at the expense of unstable feeding, fragile carriers, or difficult part separation. A balanced layout usually provides better long-term value than the lowest theoretical scrap percentage.
Durable tooling reduces maintenance interruptions and replacement costs. Replaceable cutting inserts and forming components can allow targeted repair instead of rebuilding an entire die. Proper lubrication, cleaning, inspection, and scheduled maintenance further extend tool life.
Automation may require an initial investment, but it can reduce manual operations and stabilize output over the life of the program. The economic benefit is strongest when production volumes are high and the product geometry is stable. For lower volumes, modular automation or semi-automatic solutions may provide a better balance.
An integrated supplier can also reduce hidden project costs. When die design, stamped-part production, automation, and debugging are coordinated by one technical organization, the customer may spend less time resolving interface problems between separate vendors.
Applications in New Energy Vehicle Systems
Battery Packs
Battery packs use busbars to connect cells, modules, contactors, fuses, current sensors, and external terminals. The design may include narrow sensing sections, high-current links, and insulated areas within the same assembly.
Battery busbars must be positioned accurately because they often operate near insulation barriers and protective covers. Their shape must accommodate thermal expansion, vibration, service access, and the assembly sequence of the battery module.
Battery Management Systems
The battery management system requires electrical connections for monitoring and control. Some BMS-related conductors carry lower current, while others connect to high-current portions of the battery architecture. Stamped parts can be designed with separate electrical functions and mounting references.
In certain designs, a busbar assembly may combine power distribution with voltage-sensing or temperature-sensing interfaces. Such integration can reduce the number of separate parts, although electrical isolation and signal integrity must be carefully validated.
Drive Motors and Inverters
Power electronics and motor-drive systems require conductive paths capable of handling high current and rapid changes in electrical load. Busbars can connect capacitors, inverters, terminals, and motor phases while maintaining a compact internal layout.
These components may experience significant heat and vibration. Material selection, plating, fastening, insulation, and mechanical support must therefore be considered together. A rigid busbar can also help maintain a predictable electrical geometry within the inverter housing.
DC/DC Converters and Charging Systems
DC/DC converters distribute energy between high-voltage and low-voltage systems. On-board chargers and charging modules also contain high-current pathways that benefit from low resistance and compact packaging.
Stamped busbars can be customized to fit housings, cooling structures, and connector interfaces. Their repeatable geometry supports automated assembly and helps maintain consistent clearance between conductive and non-conductive components.
Recommended Project Development Process
A successful busbar program typically begins with a clear technical exchange between the vehicle or component manufacturer and the stamping supplier. The customer should provide product drawings, material requirements, current ratings, operating temperatures, environmental conditions, plating specifications, annual demand, and validation expectations.
Step One: Requirement Review
The supplier reviews electrical, mechanical, thermal, dimensional, environmental, and commercial requirements. Any unclear tolerance, plating zone, bend condition, or assembly interface should be identified before tooling begins.
Step Two: Manufacturability Analysis
Engineers evaluate whether the product can be formed reliably using the selected material and process. Recommendations may involve geometry changes, radii, hole dimensions, carrier positions, forming sequence, or inspection datum selection.
Step Three: Die and Automation Design
The die structure, strip layout, press selection, feed system, sensors, and part-handling method are developed together. This integrated design reduces the risk that the finished die will be difficult to automate or inspect.
Step Four: Tool Manufacturing
Precision machining, wire cutting, grinding, heat treatment where applicable, fitting, polishing, and assembly are completed according to the approved design. Critical components are inspected before final die assembly.
Step Five: Trial Stamping and Debugging
Trial production confirms material flow, cutting quality, forming accuracy, feeding stability, and part separation. Adjustments are made until the process meets the required technical and quality conditions.
Step Six: Sample Approval
Samples are measured and tested. Dimensional reports, material information, surface-treatment records, and functional test results may be provided for customer approval. Any customer comments are incorporated through controlled revisions.
Step Seven: Mass Production and Continuous Improvement
Once approved, production follows the established control plan. Tool maintenance, process audits, inspection records, and customer feedback support continuous improvement throughout the project lifecycle.
How the Product Creates Competitive Value
The competitive value of new energy vehicle copper busbar stamping parts comes from the combination of material performance, precision forming, surface protection, and manufacturing integration. A low-cost part that cannot maintain dimensional or electrical performance will not provide lasting value. The strongest solution is one that performs consistently from prototype through high-volume production.
Compared with manually formed copper plates, precision-stamped parts can provide better repeatability, faster production, and more consistent connection geometry. Compared with complex cable harnesses, they can reduce routing space, lower assembly complexity, and create shorter current paths. Compared with poorly integrated tooling projects, a supplier that combines die manufacturing and automation can reduce development risk and improve production readiness.
The product also supports vehicle design flexibility. Engineers can create busbars that follow unusual battery-module contours, fit around structural elements, or provide multiple connection points within a limited envelope. Surface treatments can then be selected according to corrosion, contact, temperature, and assembly requirements.
For customers, the supplier’s advantages include an established mold-making foundation, in-house precision machining equipment, a broad press range, experienced technical personnel, stamping production capability, and access to automation equipment development. These resources support a turnkey approach in which the customer can obtain tooling, stamped parts, process debugging, and automation solutions from a coordinated team.
Frequently Asked Questions
What are new energy vehicle copper busbar stamping parts?
They are conductive copper components formed through stamping and related processes for use in electric and hybrid vehicle electrical systems. They connect batteries, motors, inverters, battery management systems, converters, chargers, sensors, and other power-distribution components.
Why are copper busbars used instead of only wiring harnesses?
Copper busbars provide a rigid, compact, and low-resistance current path. They can be designed to match the exact geometry of a battery pack or power module, reducing routing space and potentially reducing the number of cables, terminals, and assembly operations.
Which copper materials can be used?
Common options include C11000, C10100, and T2 copper. The appropriate grade depends on conductivity, formability, mechanical requirements, thickness, surface treatment, operating temperature, and application cost targets.
What current range can these busbars support?
The product range can support approximately 30 to 2,000 amperes, depending on conductor dimensions, copper grade, thermal conditions, duty cycle, connection design, and cooling. The final current rating must be confirmed through engineering analysis and application testing.
What dimensional accuracy is available?
Depending on the feature and product design, dimensional accuracy may be controlled within approximately ±0.05 to ±0.2 millimeters. Critical holes, terminals, bend heights, and contact surfaces should receive individual tolerances based on assembly requirements.
Which surface treatments are available?
Tin, nickel, and silver plating are common options. A typical plating thickness may be approximately 3 to 5 micrometers, but the actual requirement depends on contact resistance, corrosion conditions, temperature, wear, and customer specifications.
Can the busbars withstand automotive temperature and vibration conditions?
They can be designed for demanding automotive environments, including an approximate operating range from -40 degrees Celsius to 125 degrees Celsius. Validation should include application-specific vibration, thermal cycling, humidity, corrosion, and electrical testing.
What stamping equipment is available for these products?
The manufacturing organization operates punch presses ranging from approximately 80 tons to 400 tons. This range supports different material thicknesses, part sizes, die structures, and forming requirements.
Can tooling and automation be supplied together?
Yes. The company provides stamping dies and stamping automation equipment, allowing die design, press integration, feeding, inspection, and part handling to be coordinated as part of a turnkey solution.
How does the company control quality?
Quality control can include material verification, die debugging, first-article inspection, dimensional measurement, burr inspection, plating verification, electrical testing, process monitoring, traceability, and final inspection. Customer-specific control plans can be developed according to the project requirements.
Can the product be customized?
Yes. Busbars can be customized in material grade, thickness, width, bend geometry, hole pattern, plating type, plating thickness, insulation interface, current capacity, packaging, and inspection requirements.
What information should a customer provide for a quotation?
Useful information includes a two-dimensional drawing or three-dimensional model, material specification, annual volume, prototype quantity, current rating, operating temperature, plating requirement, tolerance requirements, assembly method, testing standard, and expected delivery schedule.
Conclusion
New energy vehicle copper busbar stamping parts are essential components for efficient and reliable EV power distribution. Their high-purity copper construction provides excellent electrical and thermal conductivity, while precision stamping creates compact geometries that fit modern battery packs, inverters, motors, converters, and charging systems.
Compared with conventional wiring solutions, properly engineered busbars can reduce resistance, improve packaging efficiency, simplify assembly, and support high-current transmission. Tin, nickel, or silver plating can further improve corrosion resistance and contact performance. With controlled forming, accurate holes and bends, and suitable inspection, the parts can meet the demanding mechanical, thermal, and electrical requirements of vehicle applications.
Suzhou Shuangqisi Mold Equipment Co., Ltd. supports these products through an integrated combination of stamping die design, precision machining, punch-press production, process debugging, quality control, and automation development. Its technical staff, machining resources, 80-ton to 400-ton press capacity, and turnkey tooling and automation capabilities provide a strong foundation for customized busbar projects.
For vehicle manufacturers and electrical-system suppliers, the most valuable partner is not simply a source of copper parts. It is a manufacturing team capable of translating electrical and mechanical requirements into a stable die, a controlled stamping process, a validated surface treatment, and an efficient production system. That combination helps transform copper busbar designs into dependable components for the next generation of electric mobility.
References
1. International Automotive Task Force. IATF 16949: Quality Management System Requirements for Automotive Production and Relevant Service Parts Organizations.
2. International Organization for Standardization. ISO 9001: Quality Management Systems—Requirements.
3. International Electrotechnical Commission. Standards and technical guidance concerning conductive materials, electrical connections, and power-distribution components.
4. Automotive Industry Action Group. Automotive Production Part Approval Process and related quality-planning guidance.
5. Copper Development Association. Technical information on copper conductivity, thermal conductivity, forming, and electrical applications.
6. Society of Automotive Engineers. Technical guidance concerning electric vehicle electrical systems, environmental durability, vibration, and high-voltage component validation.
7. RoHS Directive. Restrictions on the Use of Certain Hazardous Substances in Electrical and Electronic Equipment.
8. General engineering principles for precision sheet-metal stamping, progressive die design, copper forming, plating control, and automotive component inspection.
Product: New energy vehicle copper busbar stamping parts
Previous Post
Progressive Molds for Automotive Parts: Precision, Efficiency, and Reliable High-Volume Production
Next Post
High-End Oven Stamping Parts: Precision, Heat Resistance, and Reliable Manufacturing for Advanced Oven Systems
Our Products.
Start Your Business with an OEM Manufacturer Right Here!

Provide global customers with complete turn-key solutions
through
innovation!
QUICK LINKS
CONTACT INFO.
-
 +86-139 1308 8972
-

-
 No. 118 Yexin Road, Wujiang Economic Development Zone, Suzhou, China
Copyright © Suzhou Shuangqisi Mold Equipment Co., Ltd. All Rights Reserved. Custom Stamping Die Metal Stamping Die Manufacturers
